Veining
Veining
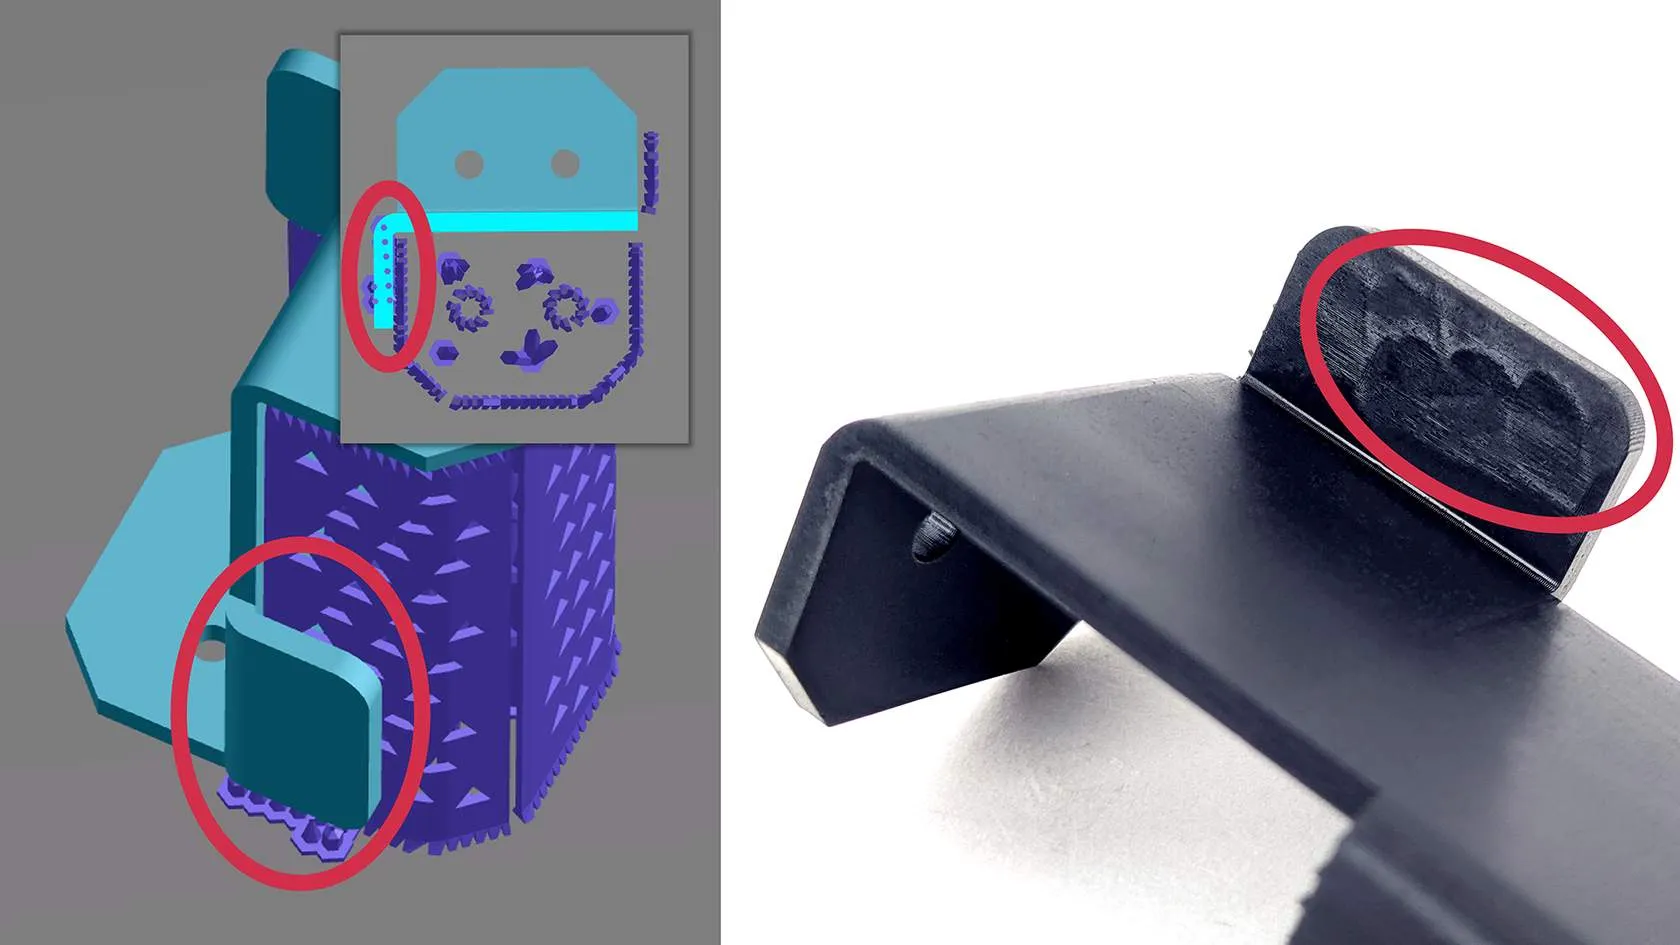
Organic ridges on part in the build direction.
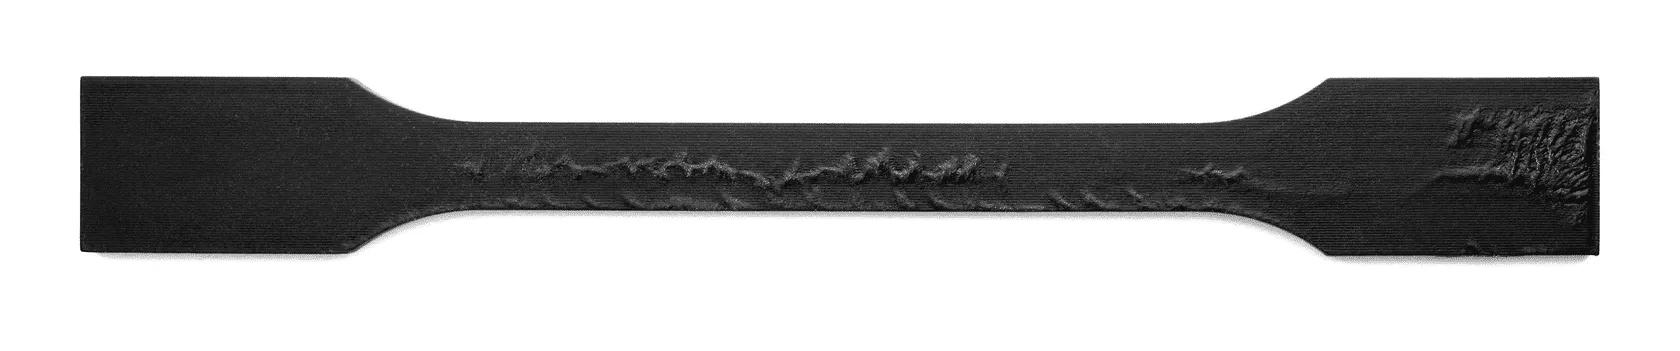
How to Identify
Veining can be diagnosed as follows:
- Ridges on part along the build direction (Z axis).
- Can be wandering or straight.
- May be wavy especially for larger, flat surfaces.
- This is an uncommon defect.
- An extreme form of this defect is called Caping
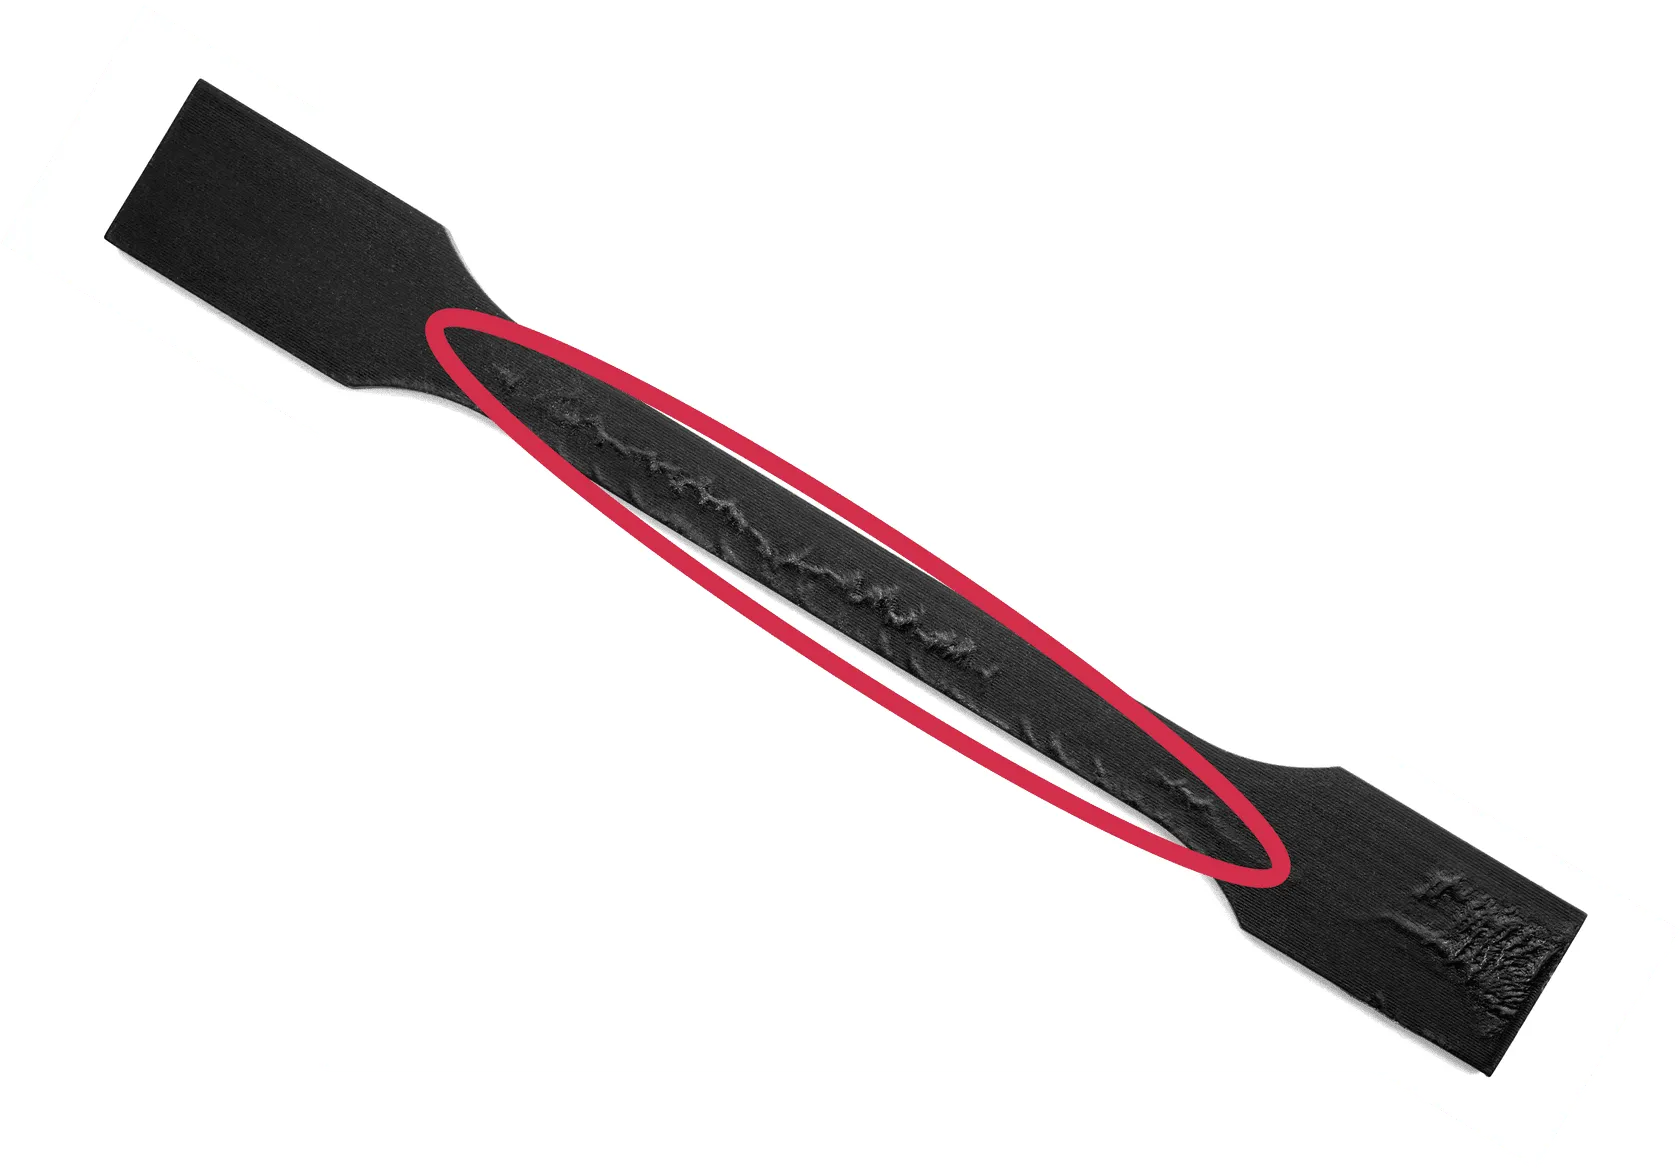
Cause - Inconclusive

Cause - Inconclusive
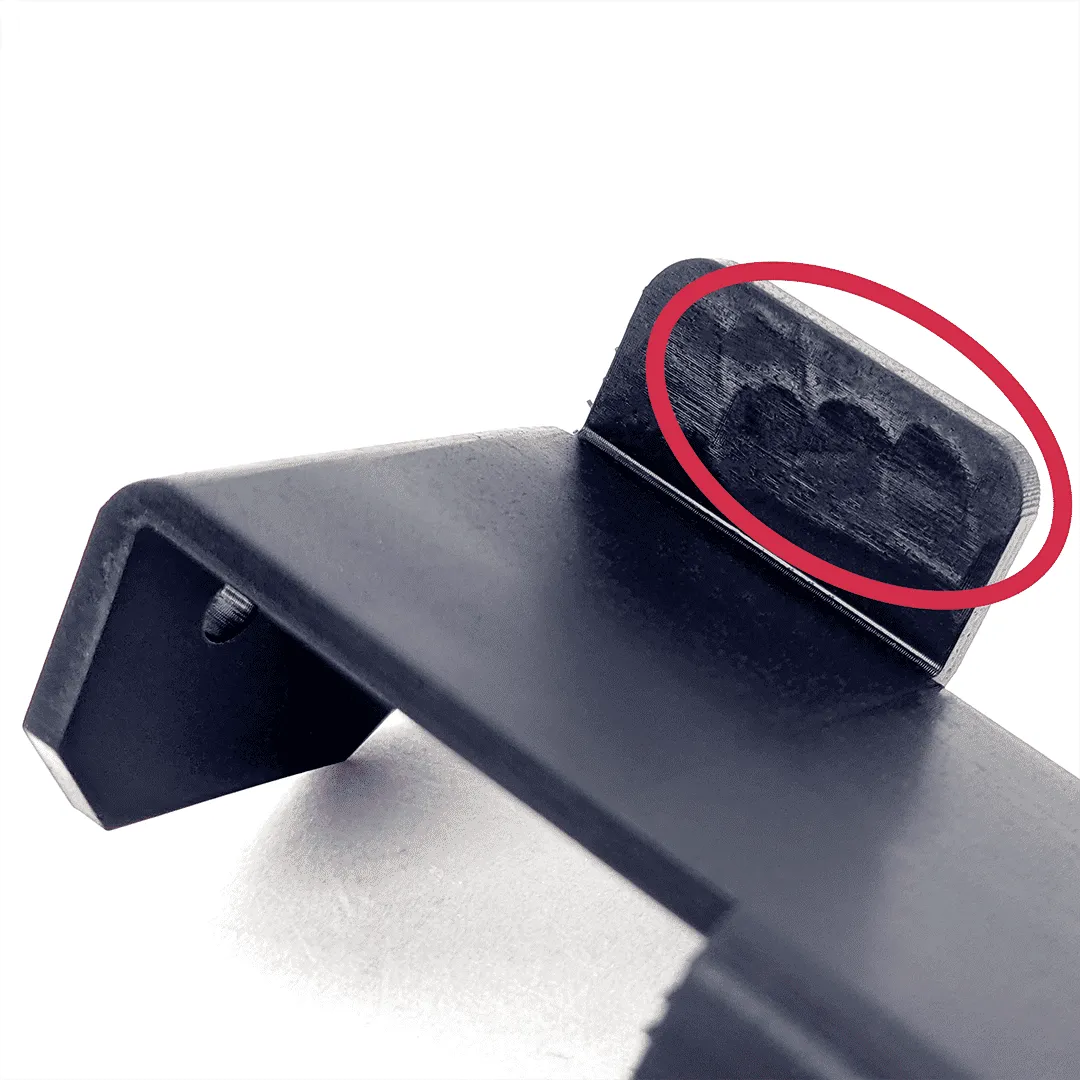
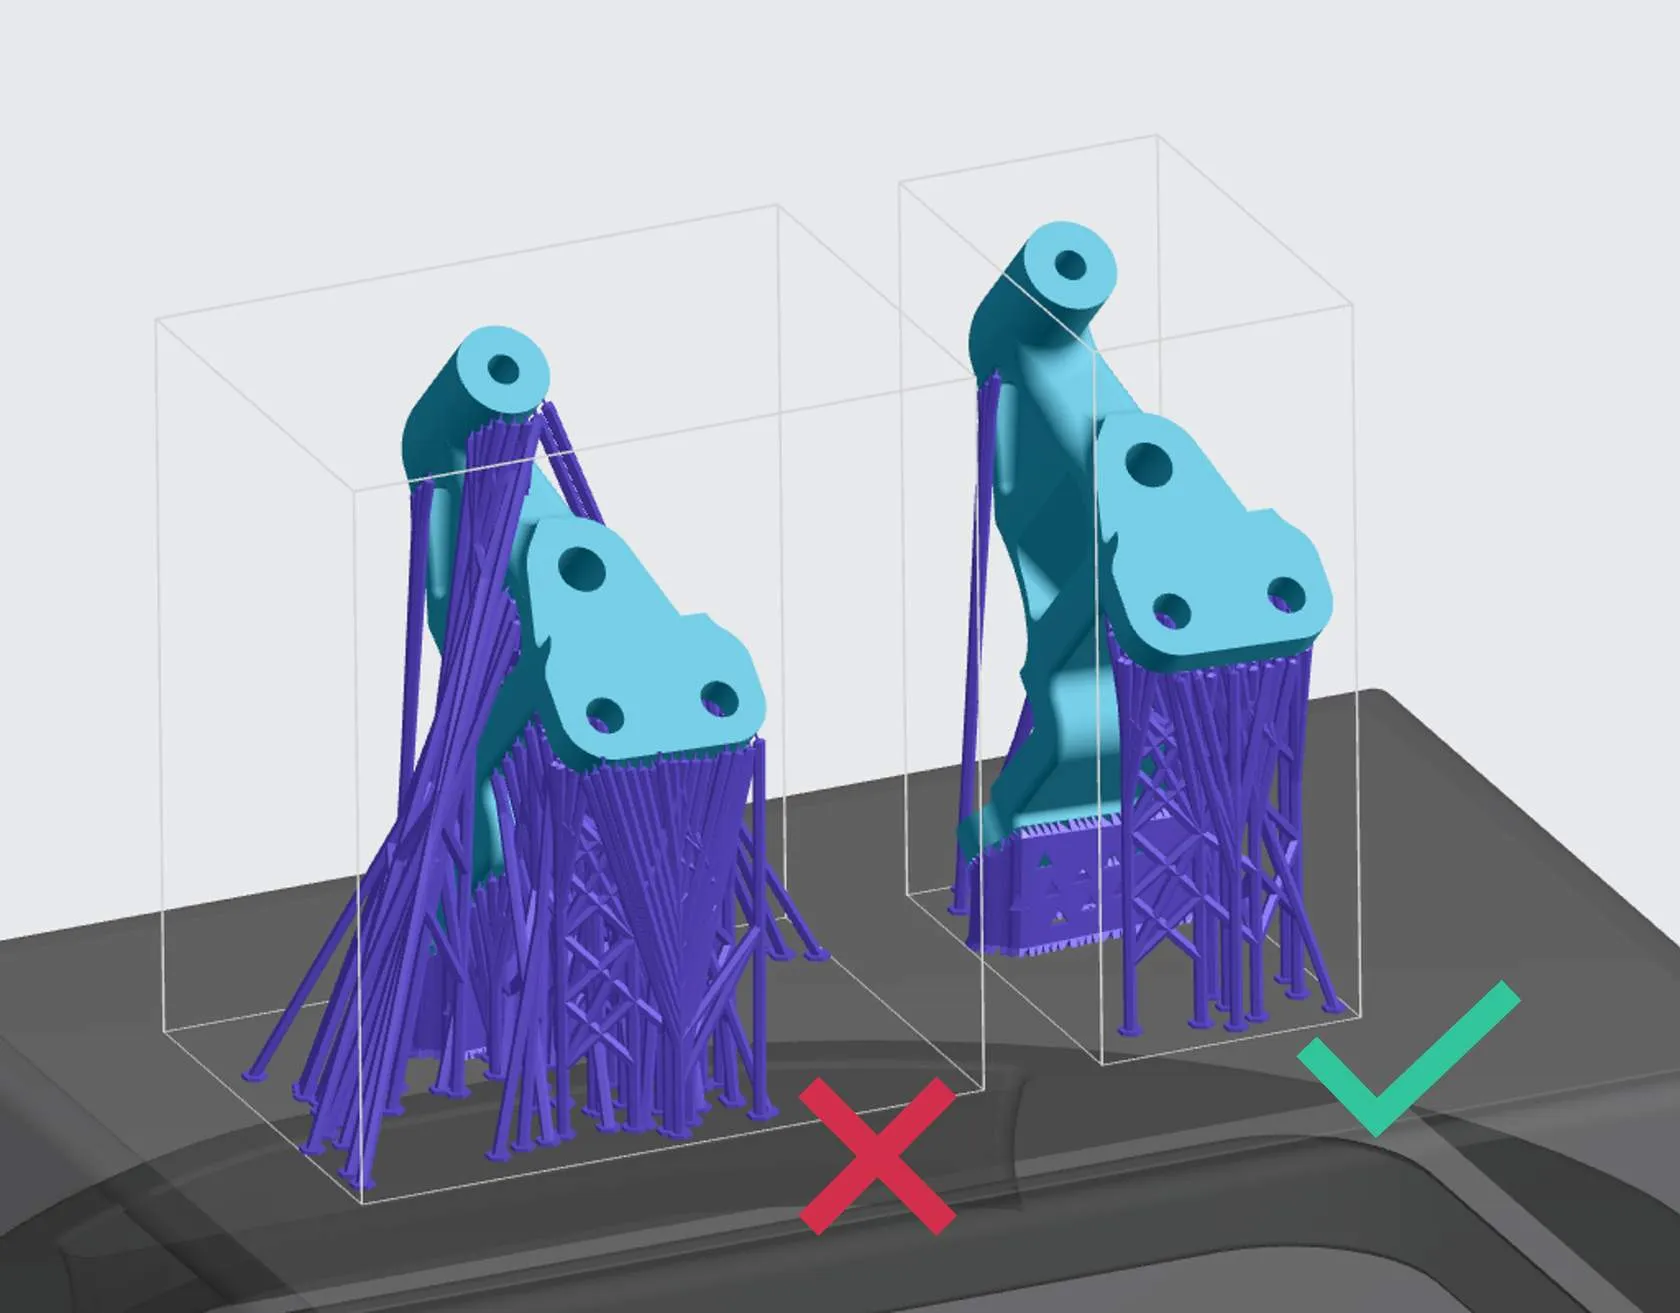
Cause - Supports too close to surface
Troubleshooting
It is recommended that you review all the possible solutions before taking action to ensure you are pursuing the best course of action.
If the best course of action is not apparent, try the troubleshooting options in the order listed. Refer here for more tips.
Print Preparation or Part Design Adjustments
The following solutions will address print or part-related causes of the defects. Choose among the suggested actions below and select the best approach for your application. Usually only one type of adjustment is needed.
If problems persist, please reach out to Carbon Support.
Explanation & Causes
Explanation
- Parts, features and/or supports are too close together restricting resin flow.
- Slow moving resin heats up making it more susceptible to curing from stray UV light.
- This condition is magnified over time as resin heats up over the course of the build.
Causes
- Print Preparation or Part Design
- Print Plan Adjustments
Print Preparation or Part Design
How the part is oriented, supported, or designed is causing the defect.

Root Issue | Problem | Why Defect Presents |
Supports | Over-supported | Parts that are over-supported provide less space for resin to flow properly throughout the build causing light to scatter. |
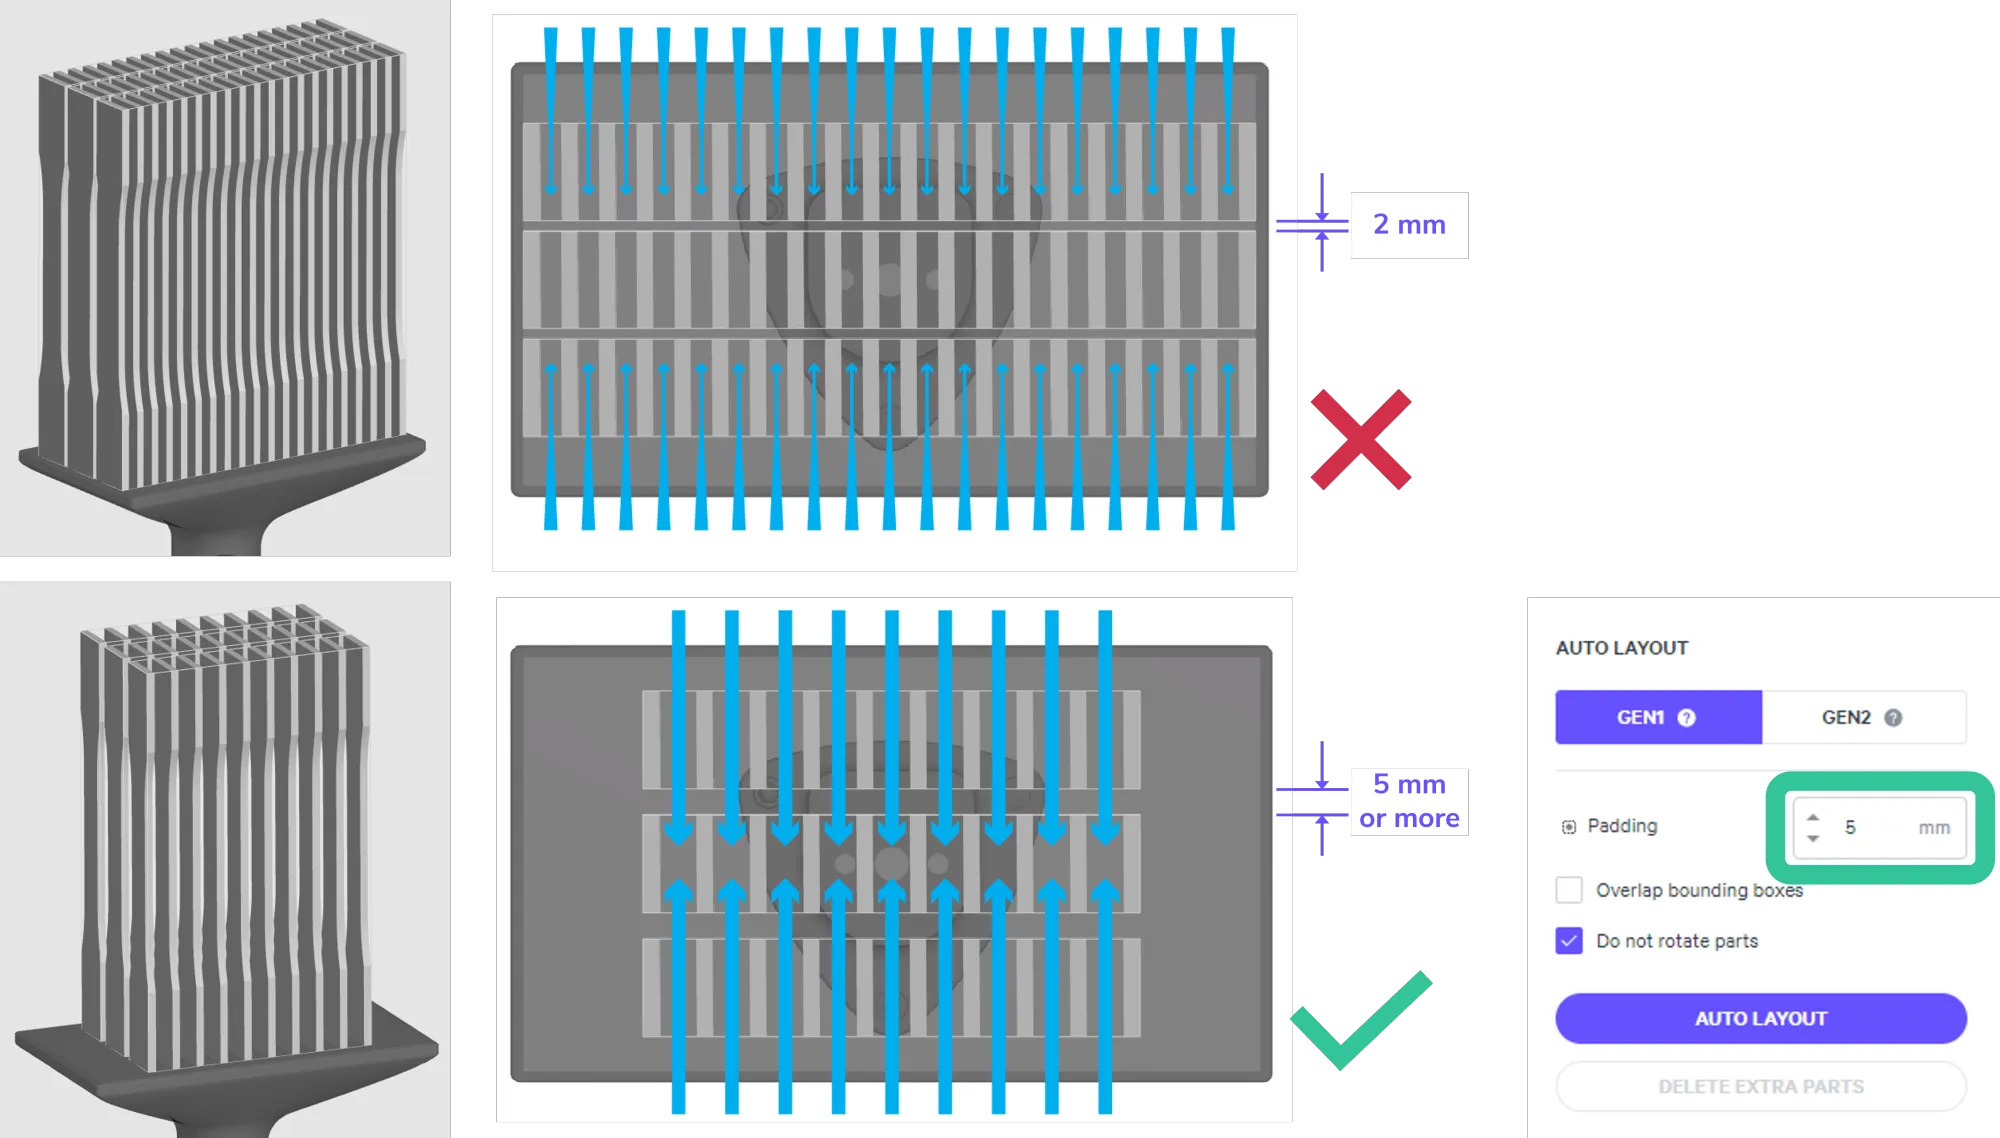
Layout | Parts too dense on platform | Padding between parts is to small for resin to flow properly throughout the build causing light to scatter. |
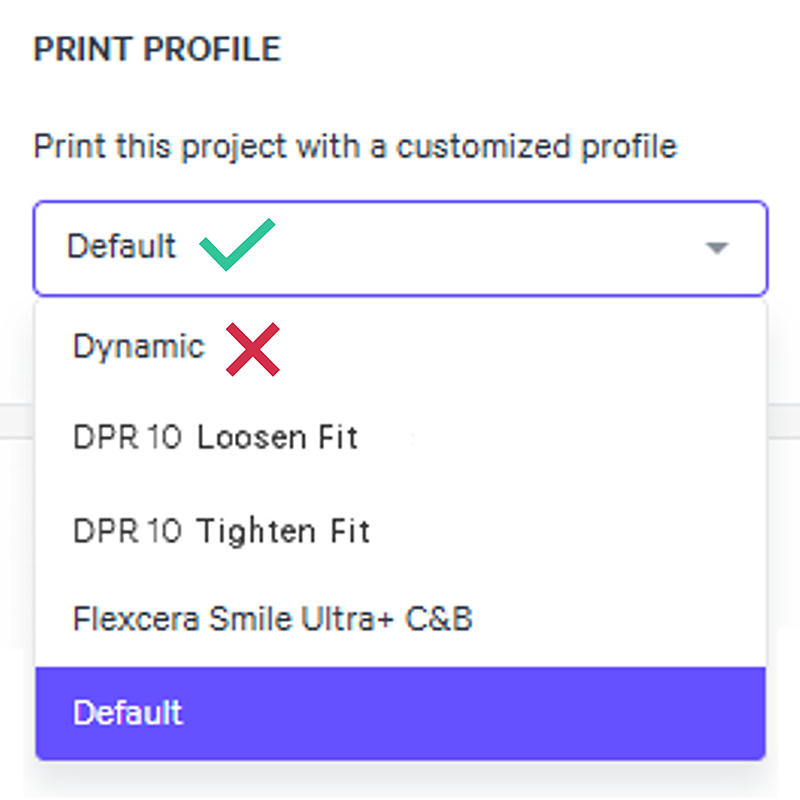
Print Profile | Print too fast in Dynamic | A shortened print gives less time for resin flow to all areas of the build causing light to scatter. For M1 and M2 printers |
Print Plan Adjustments
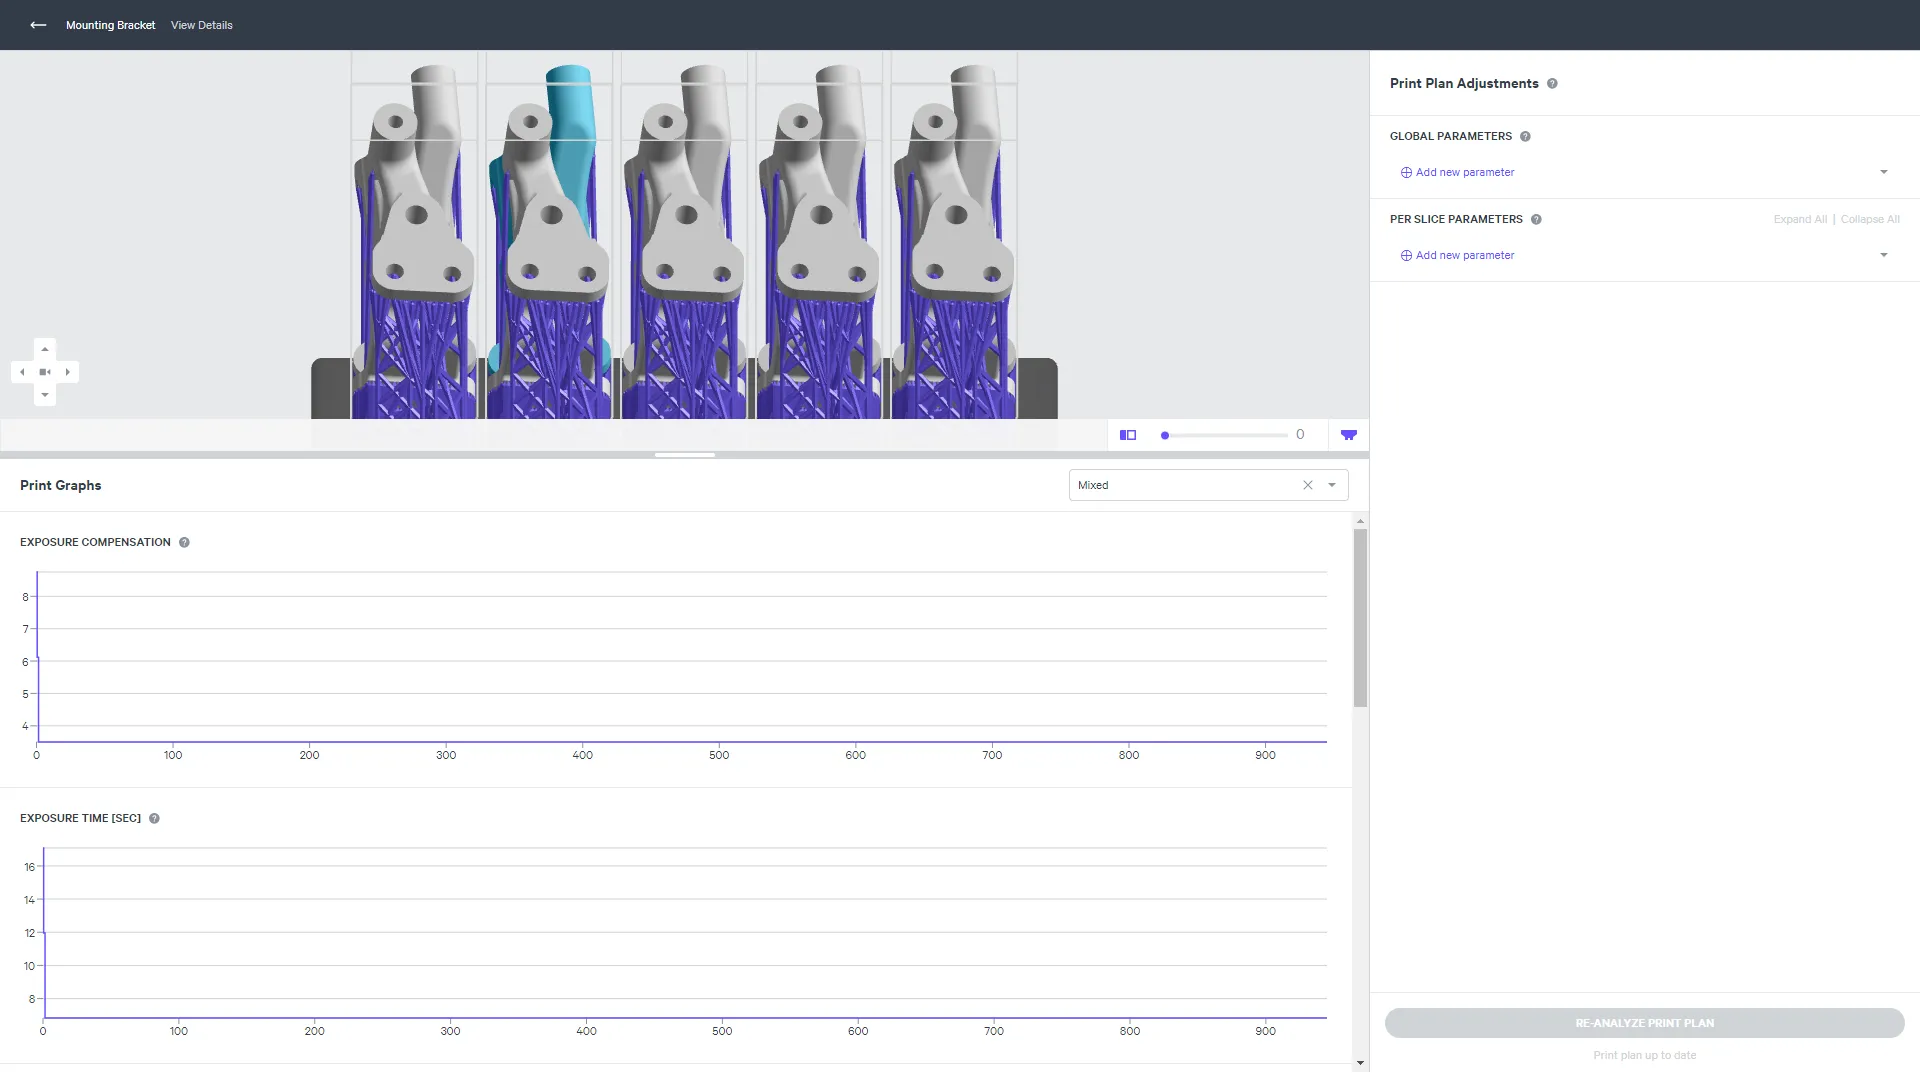
Print Plan Adjustments adjust the print plan to optimize mid to high volume production and/or address part defects.
In doing so, adjustment may both prevent or cause defects. Below are adjustments that can cause this defect.
Printing Stage | Parameter Type | Type of Adjustment | Why Defect Presents |
4 Settle Down | Delay Timing | Decrease | A shortened settle down stage gives less time for resin flow to all areas of the build causing light to scatter. |