Vacuum Line
Vacuum Line
An unvented volume creates lines on a surface by moving thin walls under the pressure differential.
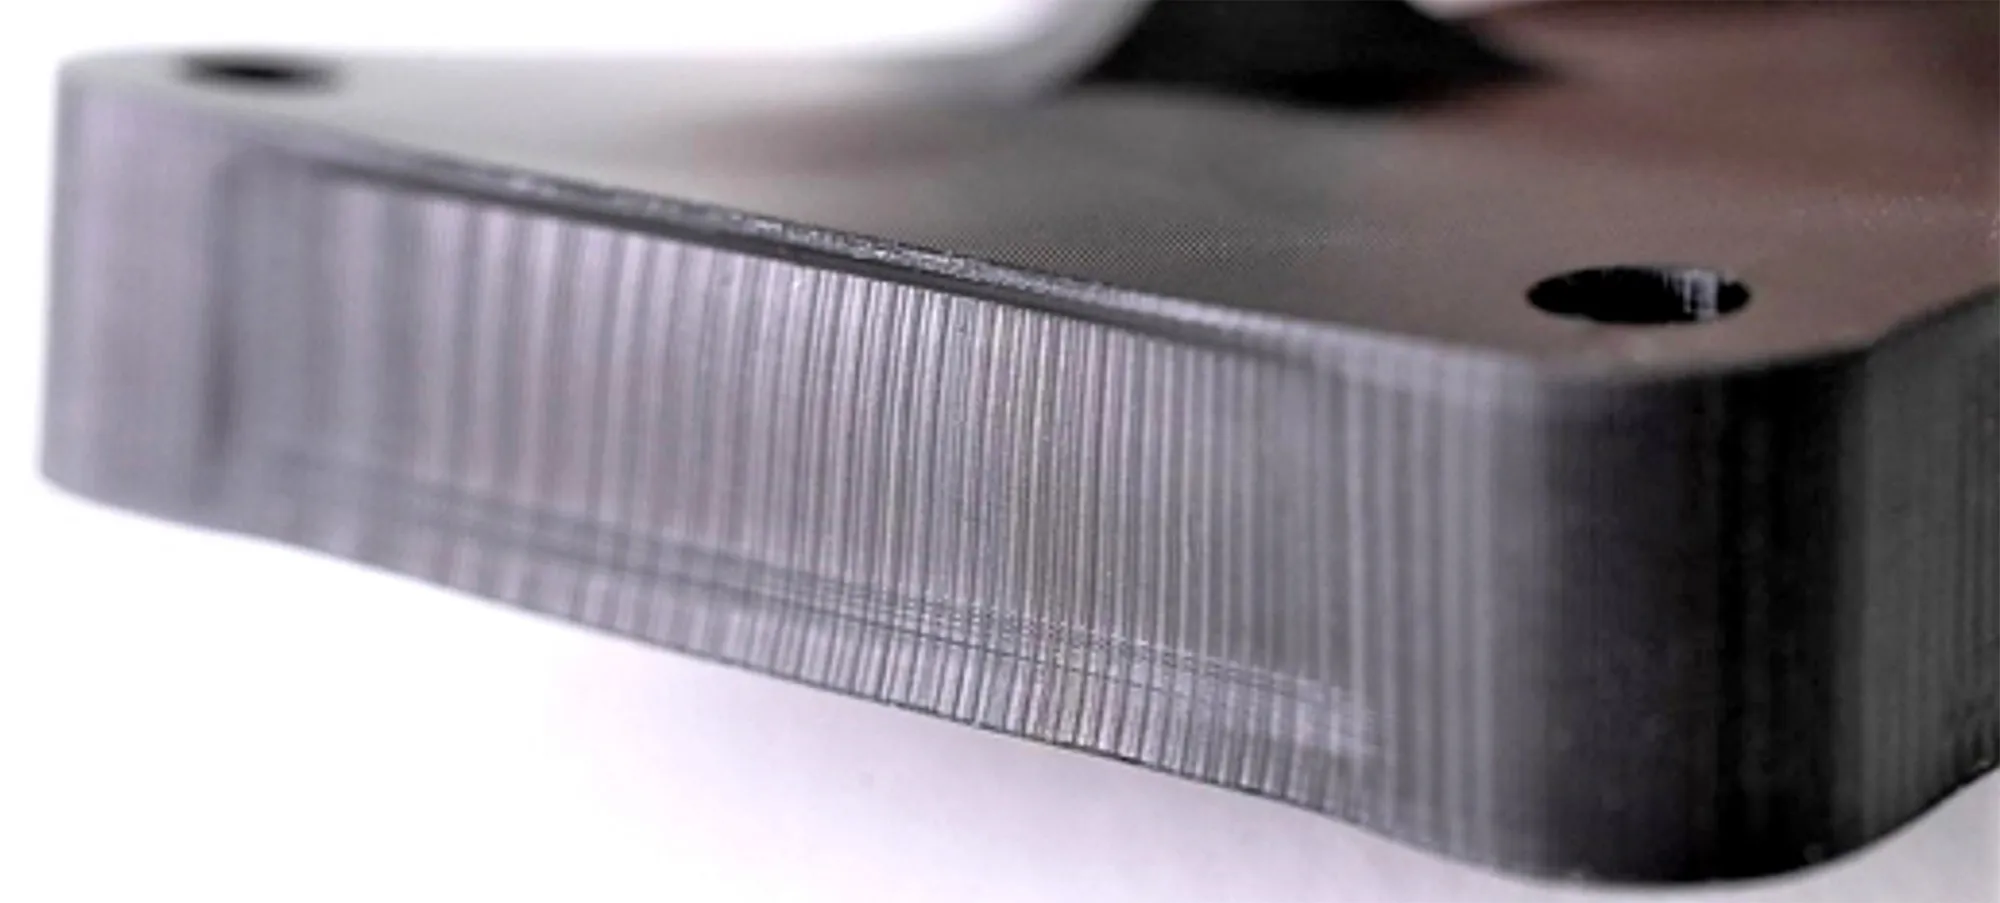
How to Identify
Vacuum lines can be diagnosed as follows:
- Vacuum lines are a defect specific to unvented volumes.
- The line(s) appear horizontal relative to the platform.
- Thin walls are most likely to present this defect. The walls will appear to be pulled in towards the trapped volume along the vacuum line.
When the geometry transitions from a thin wall to a large cross section surrounding an unvented volume, a Cross Section Line can occur in conjunction with the Vacuum Line defect. Both defects may need to be addressed.
In extreme conditions, the Blow Out defect may also occur along vacuum lines.
Cause - Unvented Volume
Solution - Print Preparation or Part Design
- The upper line is occurring in conjunction with a cross section line defect.
- The lower lines are vacuum lines only.
Cause - Unvented Volume
Solution - Print Preparation or Part Design
- The upper line is occurring in conjunction with a cross section line defect.
- The lower lines are vacuum lines only.
Cause - Unvented Volume
Solution - Print Preparation or Part Design
- The blow out defect is also occurring in this example.
Troubleshooting
It is recommended that you review all the possible solutions before taking action to ensure you are pursuing the best course of action.
If the best course of action is not apparent, try the troubleshooting options in the order listed. Refer here for more tips.
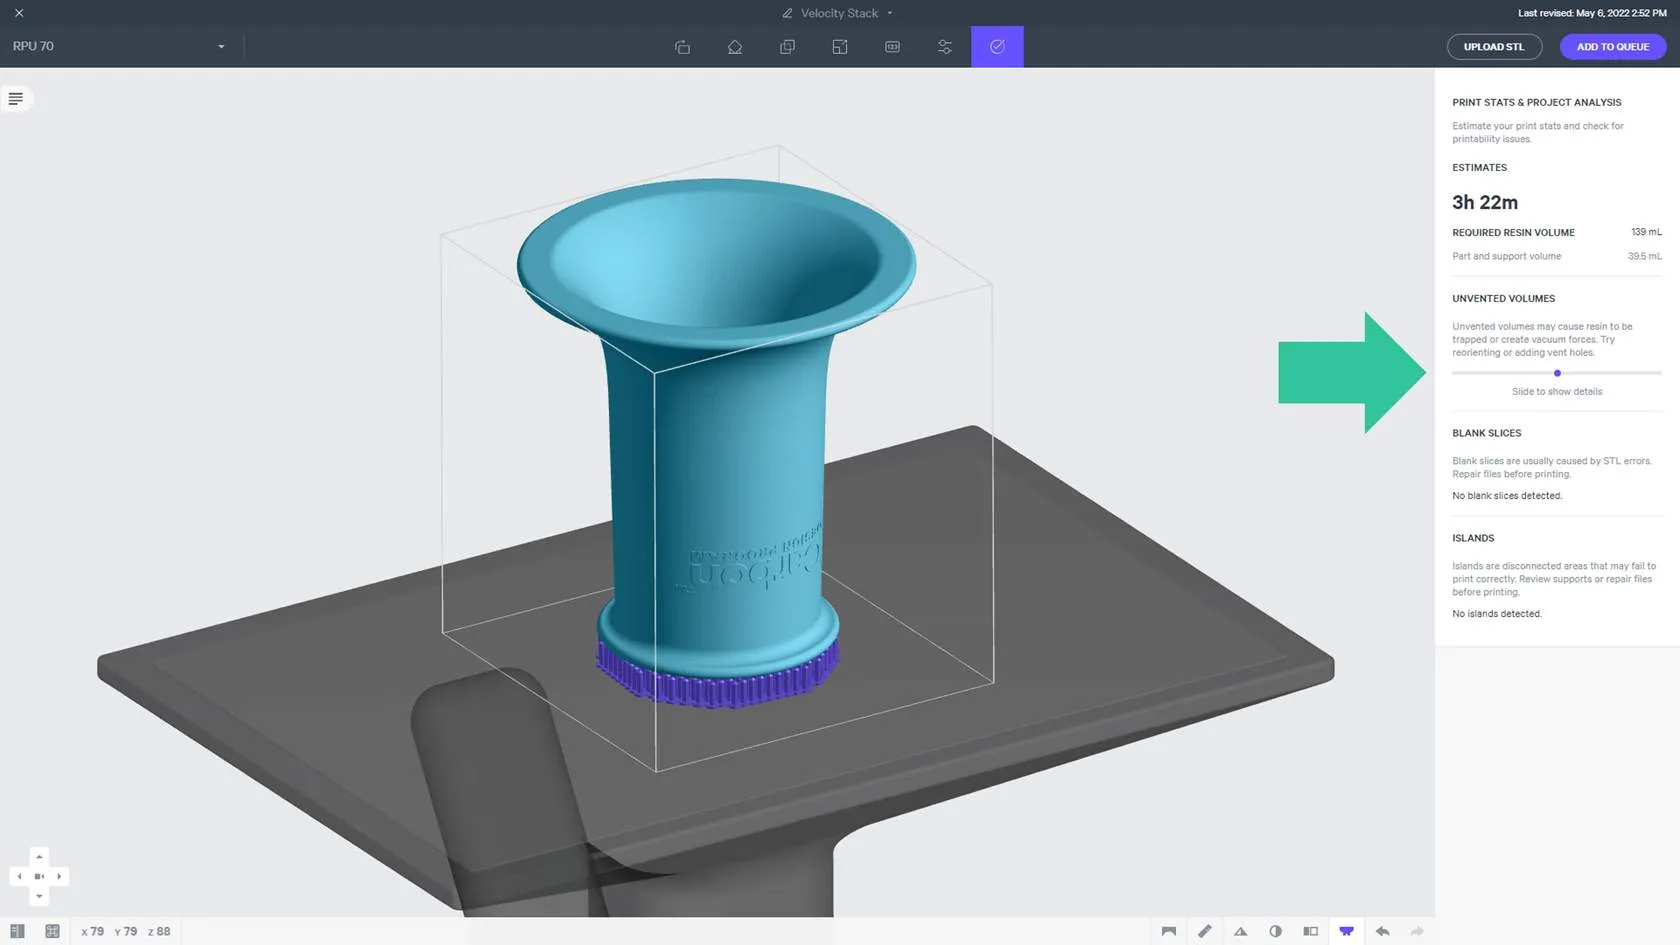
Verify if your project contains an unvented volume.
- Project Analysis in the printer software will alert you if you have an unvented volume.
- If you do have an unvented volume, proceed to the Print Preparation or Part Design Adjustments troubleshooting options below. If you do not have an unvented volume, refer to the Identify a Defect guide to identify a different defect.
Print Preparation or Part Design Adjustments
The following solutions will address print or part-related causes of the defects. Choose among the suggested actions below and select the best approach for your application. Usually only one type of adjustment is needed.
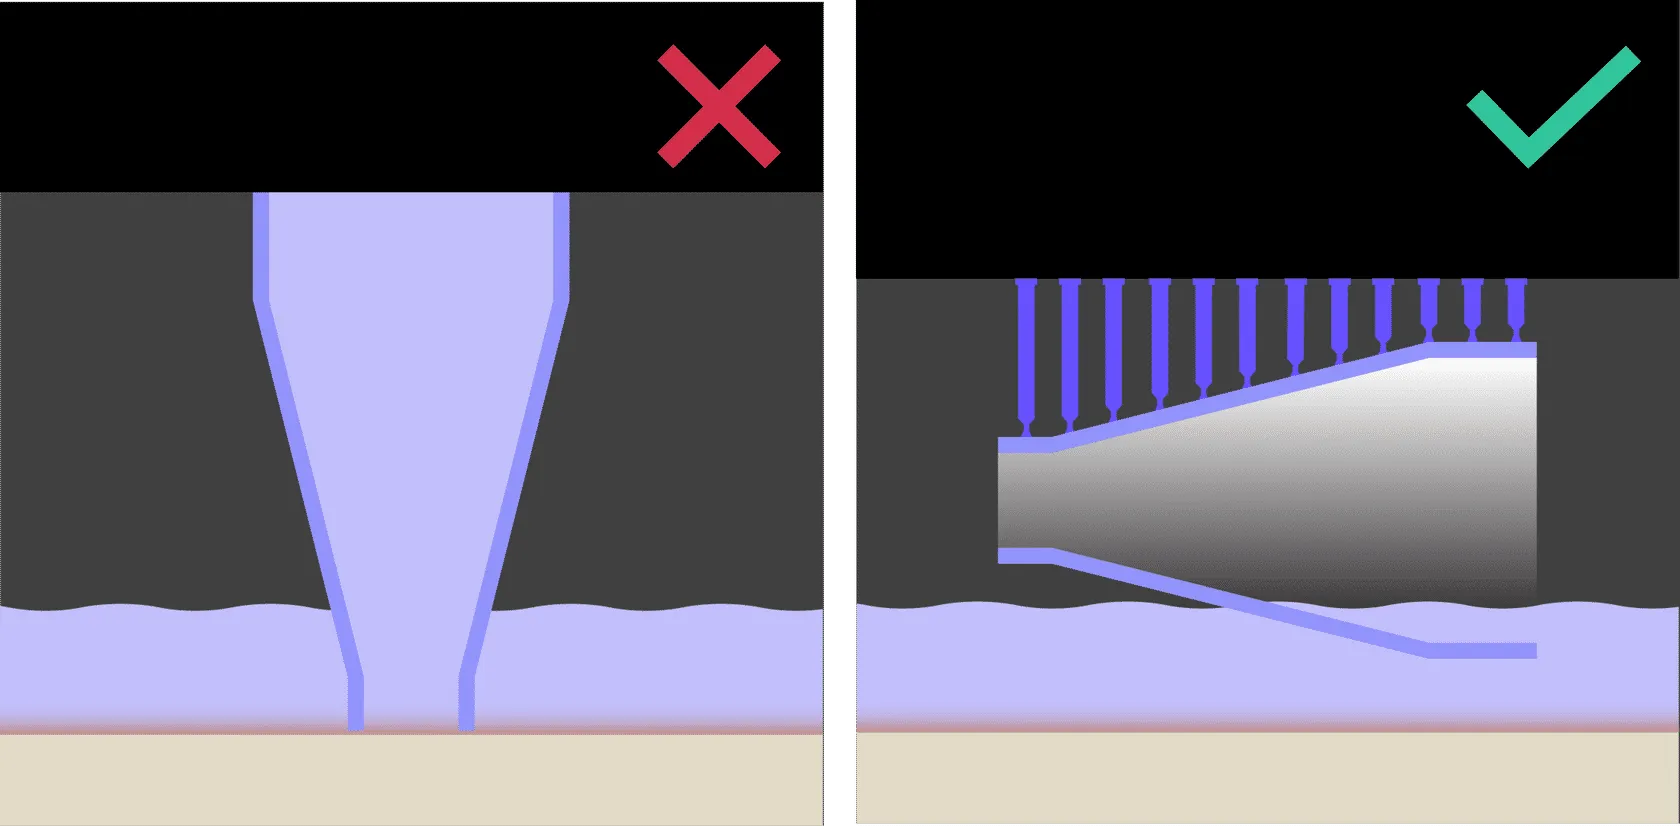
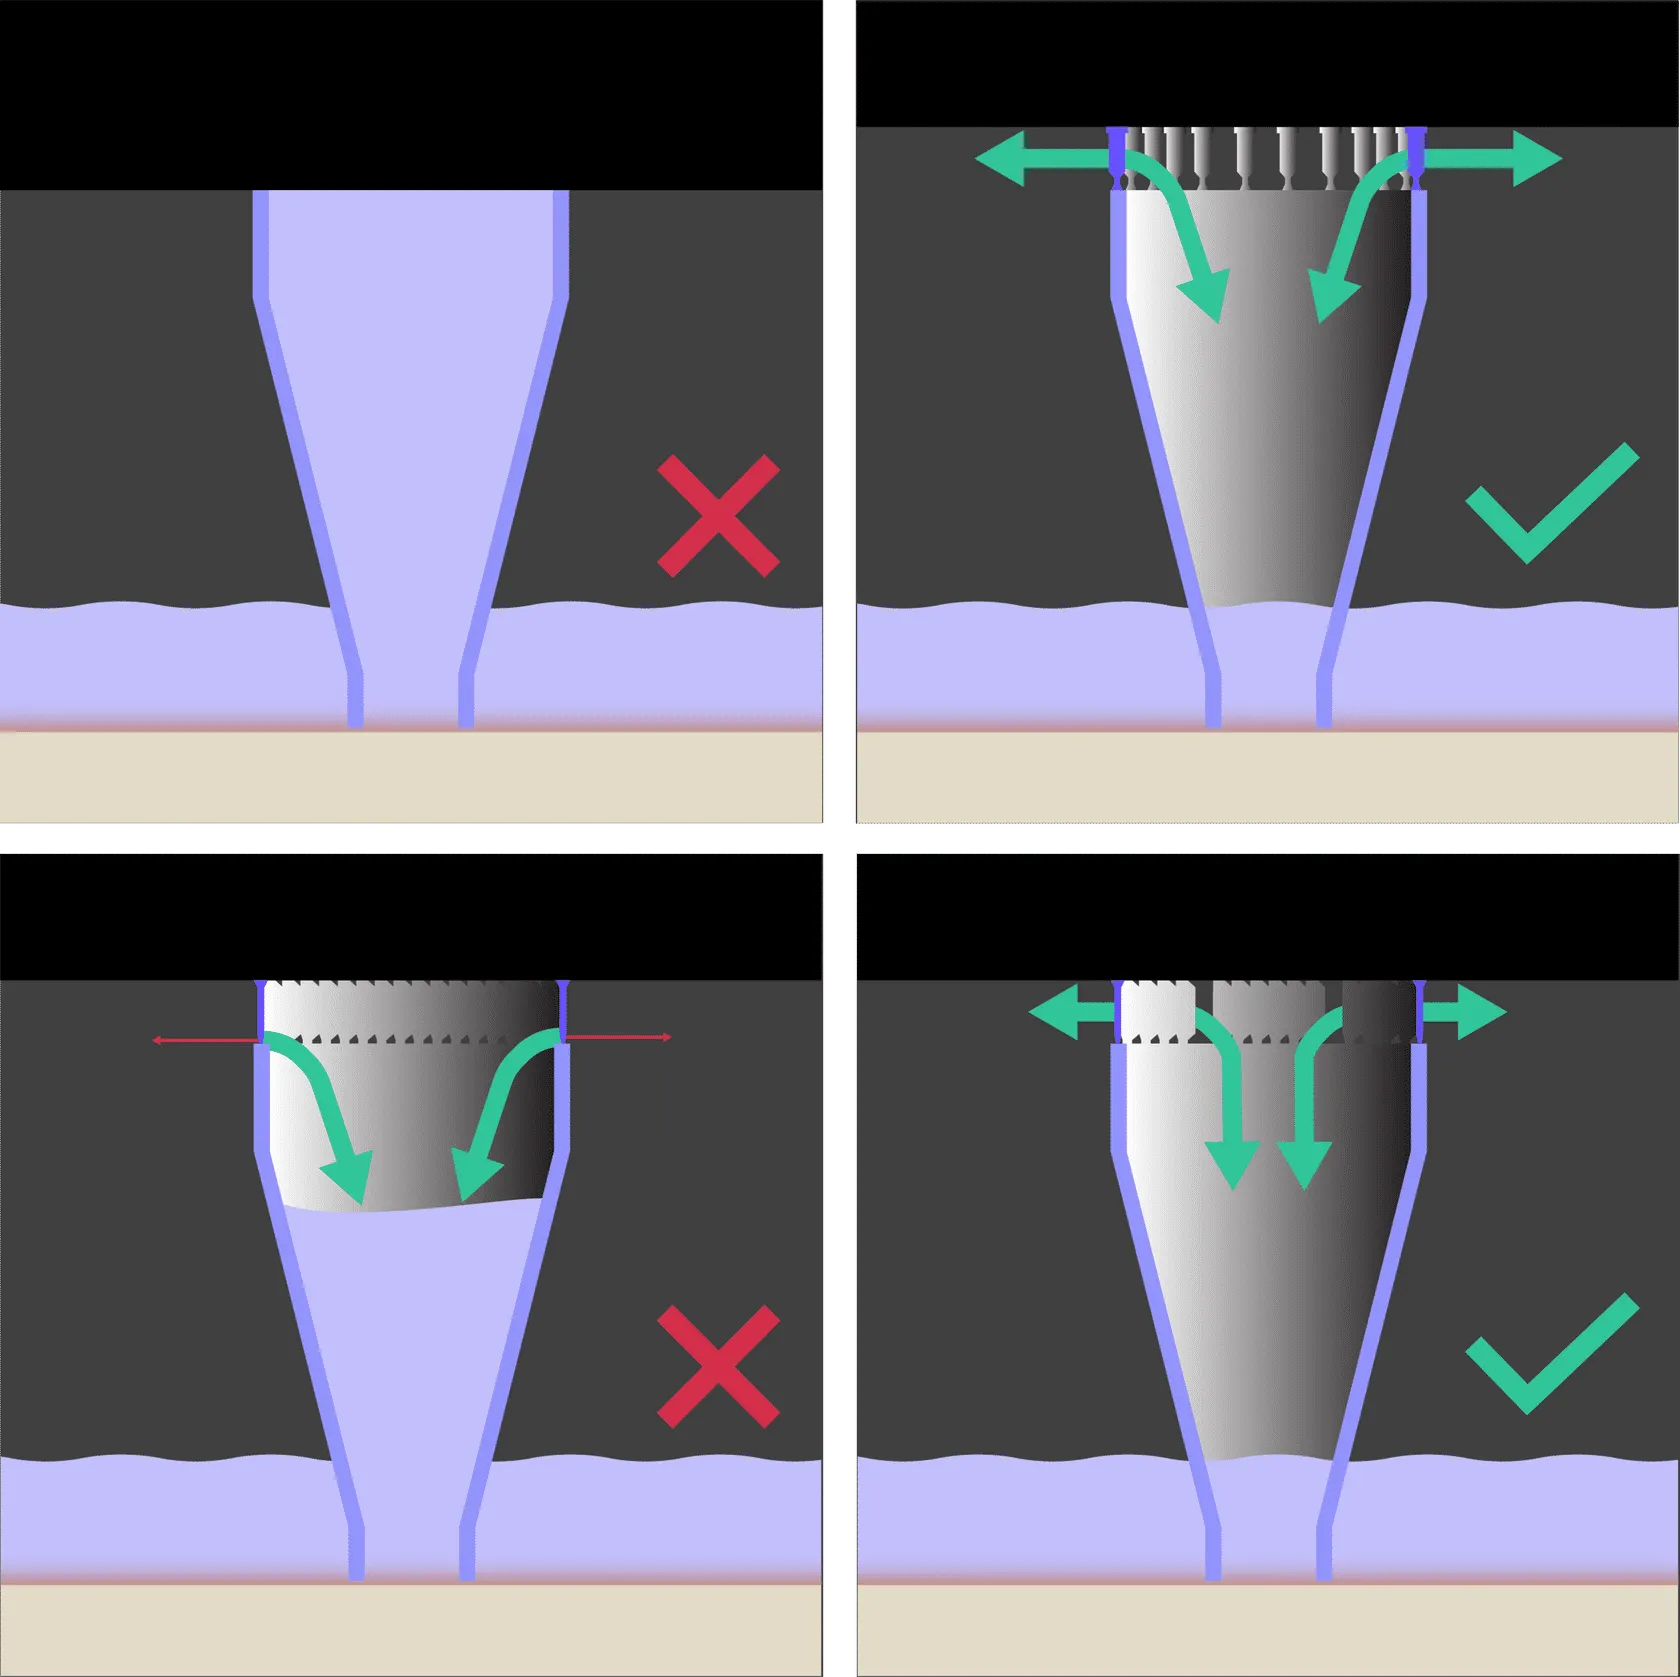
- Unvented Volume
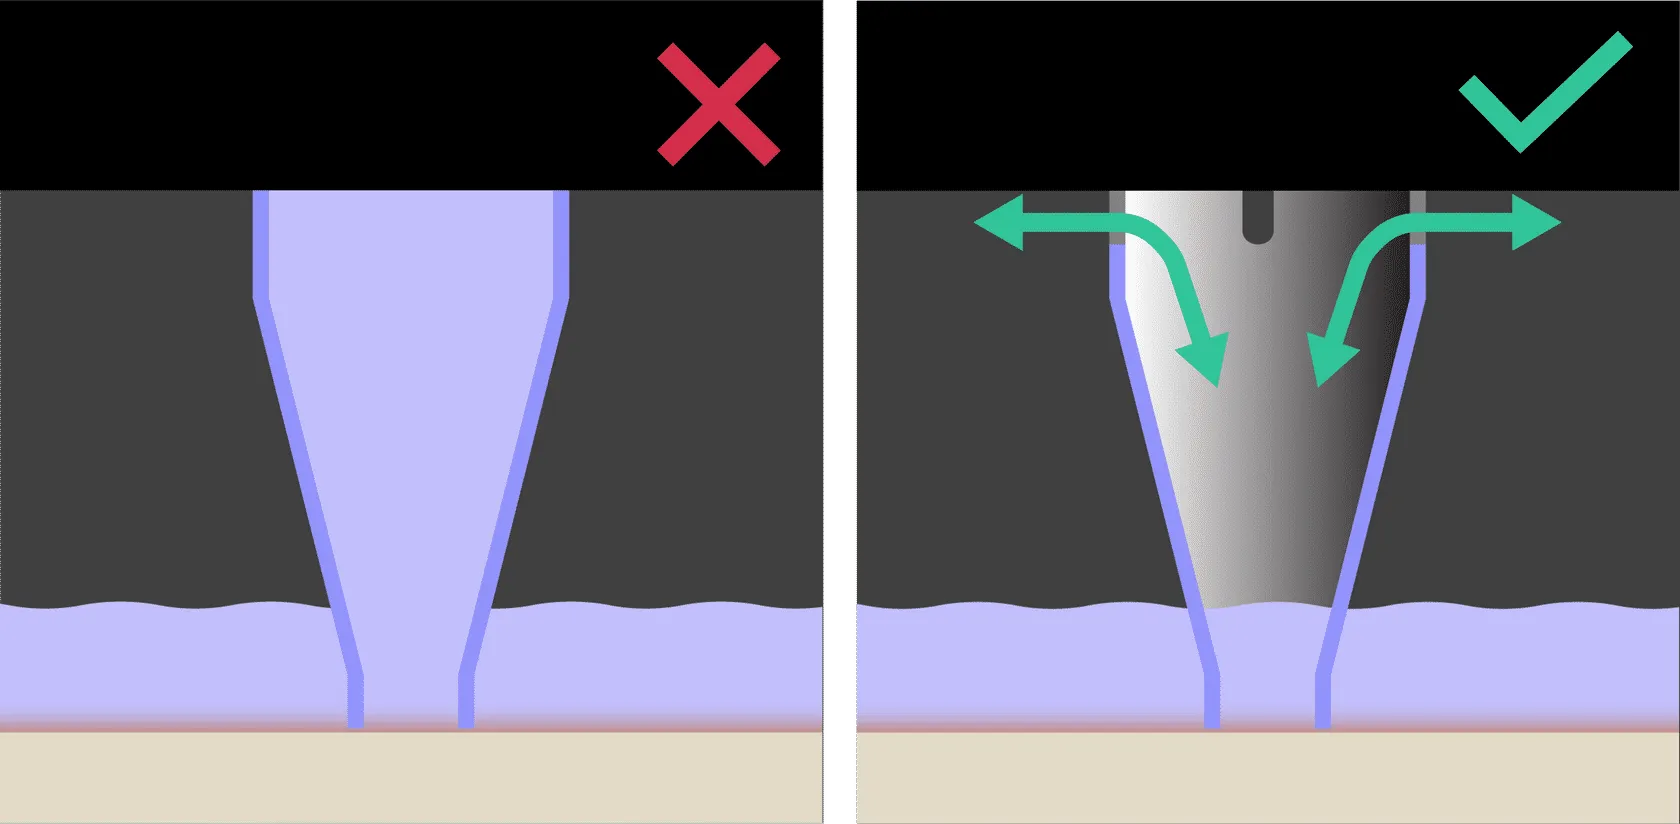
- Add vent holes in the part, at or near the platform, to vent the trapped volume
Reference DLS Design Guidelines for drain/vent hole guidelines.
If problems persist, please reach out to Carbon Support.
Explanation & Causes
Explanation
An unvented volume has a pressure differential inside versus outside the trapped volume. The walls surrounding the trapped volume will be pulled inwards by the low pressure as the platform moves up during pumping, causing wall deformation. Some of the pressure may relax as the platform pumps back down to the curing position, thus the walls continue to deform as the print progresses often resulting in more than one vacuum line as the print proceeds.
Reference DLS Printer Dynamics for more information on pumping up and down during printing.
- Thin walls in conjunction with a large trapped volume are the most likely to experience vacuum lines.
- More susceptible to unvented volumes:
- EPU due to its low green strength.
- L1 printer due to larger suction forces.
Causes
Print Preparation or Part Design
How the part is oriented, supported, or designed is causing the defect.

Root Issue | Problem | Why Defect Presents |
Unvented volume | A horizontal line along the part. | The pressure differential causes the walls surrounding an unvented volume to move while the platform moves up and down during printing. |