Keystone KeyGuard
Overview
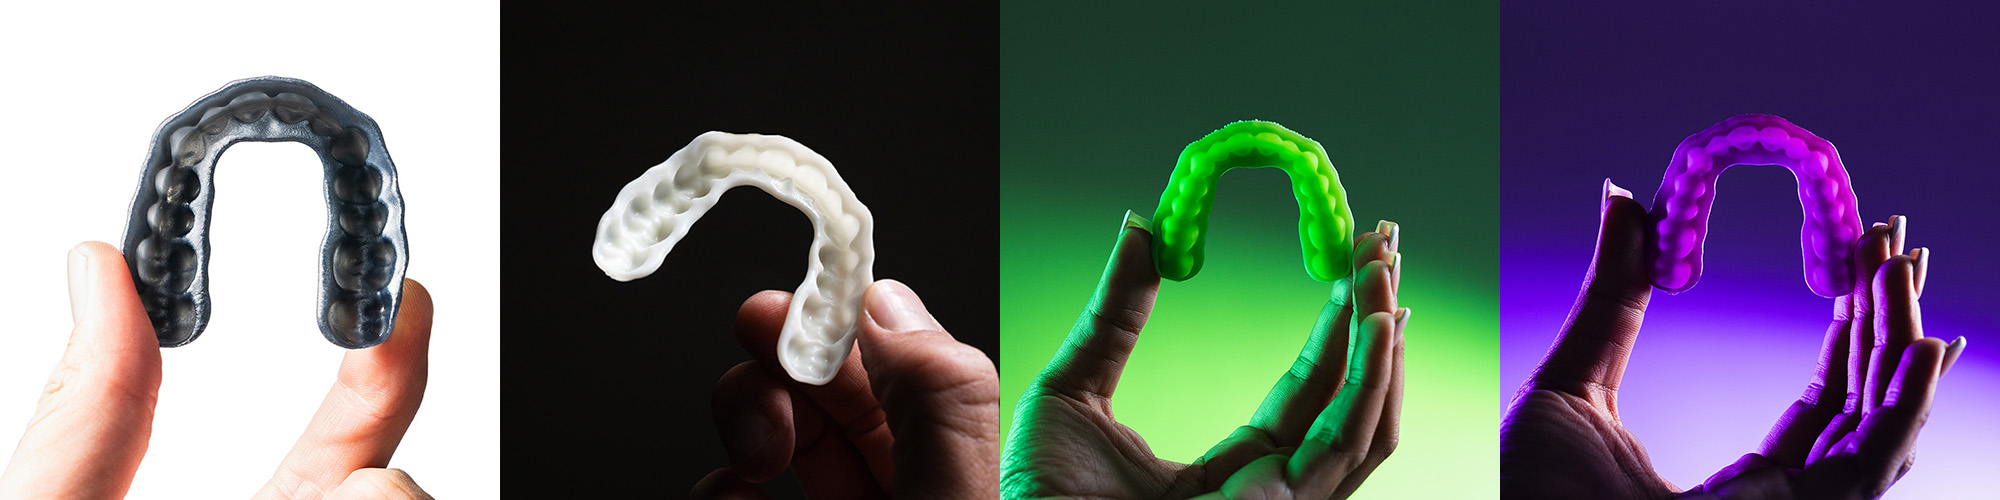
Keystone KeyGuard™ by Keystone Industries® is a biocompatible photopolymer resin for the fabrication of custom-made athletic mouth guards.
Keystone KeyGuard™ is available in black, white, purple and green.
This course will cover digital prep of your splints and night guards to properly prepare them for printing.
This resin is not currently compatible with the AO Polishing Cassette.
Resource Links
Protocol
This downloadable handout provides important usage information, including instructions about storage and post-processing. Print it out and bring it into the lab!
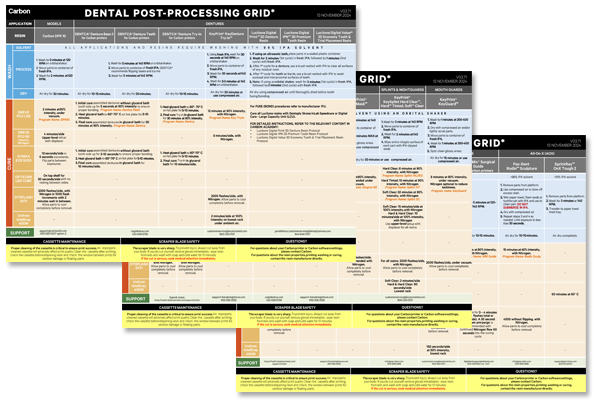
Dental Post-Processing Grids
One of our most popular downloads! This table provides washing and curing instructions for all supported dental resins.
Print it and use it in the lab as a quick reference.
German/Deutsch
Spanish/Español
Design Recommendations
- Carbon does not make mouth guard design recommendations.
- Users should follow design guidance provided in the manufacturer instructions for use (IFU).
General Orientation & Support Information
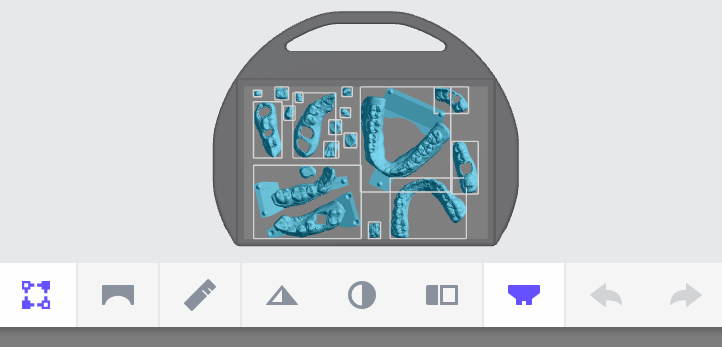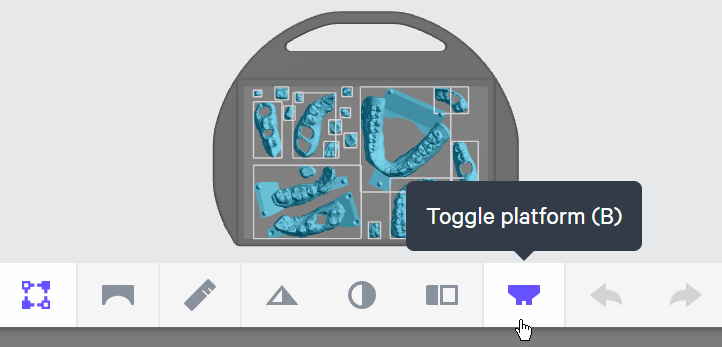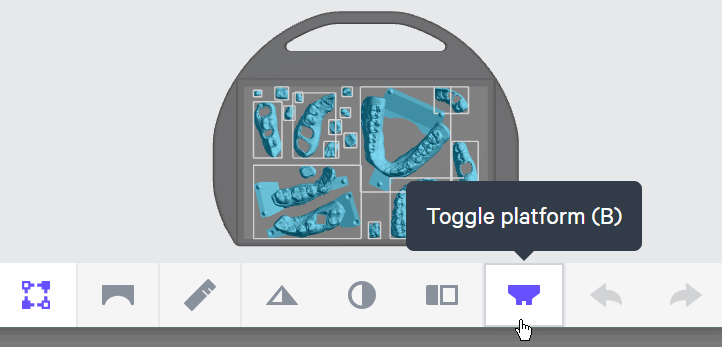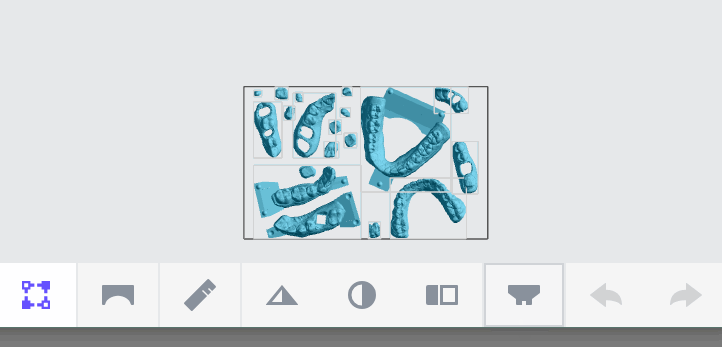
Hide the Platform
Use Toggle platform (or press B) to hide the platform before orienting parts. This will make it easier to see overhangs and place supports.
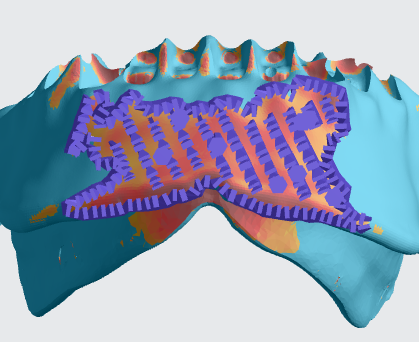
Use Patch and Fence tools to create supports
Patch tool
- The Patch tool speeds up support creation by automatically supporting an area with just a few clicks. It is useful for supporting larger areas of overhang that would take longer to support manually.
- It is often useful to support your parts with this tool before manually adding supports.
Fence tool
- Fence supports are manually placed by the user and are best suited on linear overhangs or smaller areas.
- Fences provide stability while leaving smaller nubs than the default Bars option.
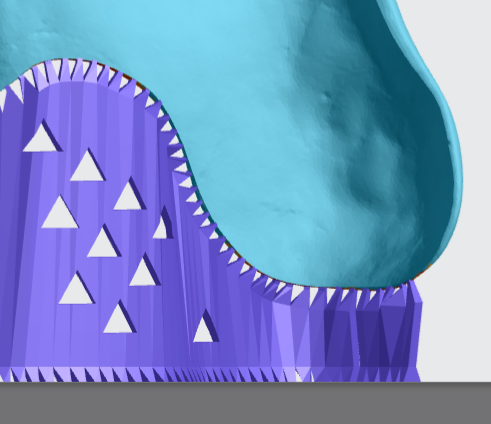
Review Supports in Printer UI course for more information.
Orienting
Keyprint KeyGuard resin offers flexibility when orienting and supporting digital models. Carbon encourages experimentation within the provided guidelines to determine what works best for your lab.
The following information applies to all colors.
Orient the mouth guard
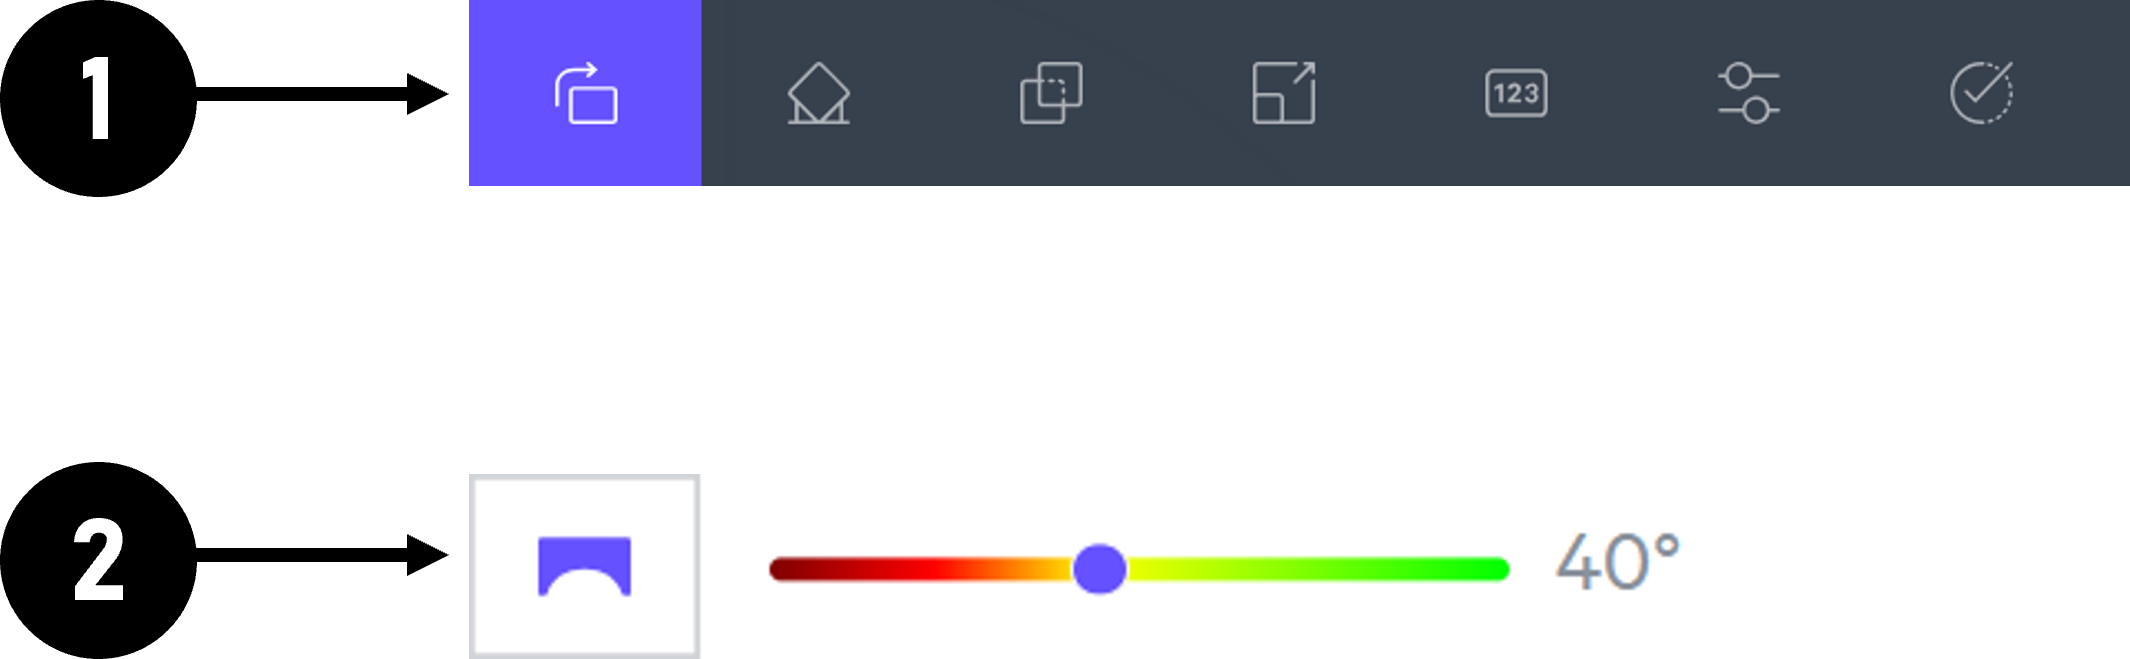
1. Click on Orient or Shift + O in the top bar in the printer interface.
2. In the lower right corner of the bottom bar, turn on Overhang Detection or V key and set to 40 degrees. Areas that need support will appear red.
3. Orient the mouth guard so it is about parallel to the platform.
4. Rotate the model at least 75 degrees from horizontal with the anterior facing the platform.
90 degrees (perpendicular to the platform) is the recommended orientation.
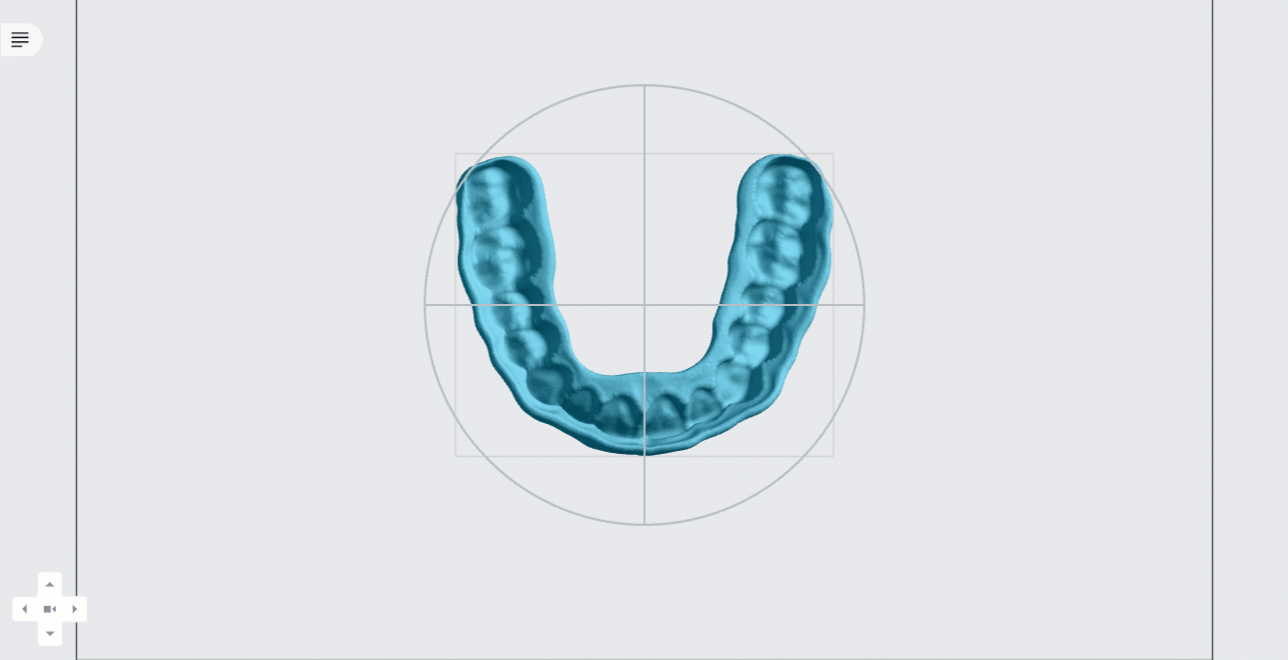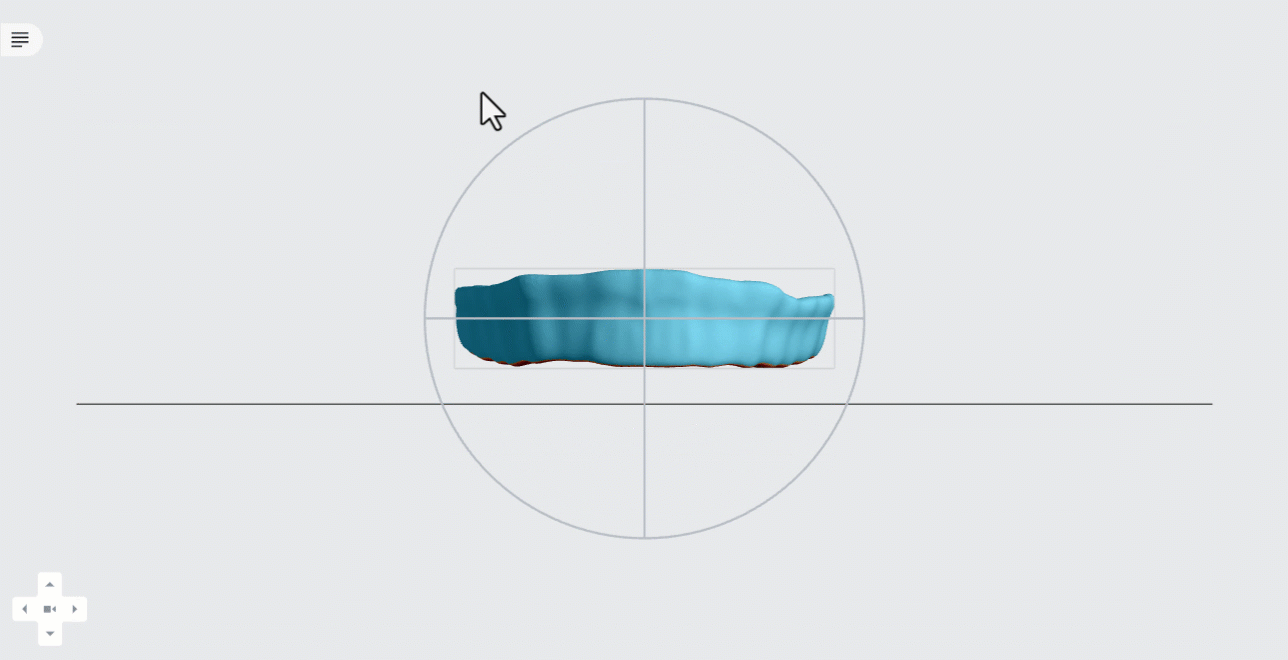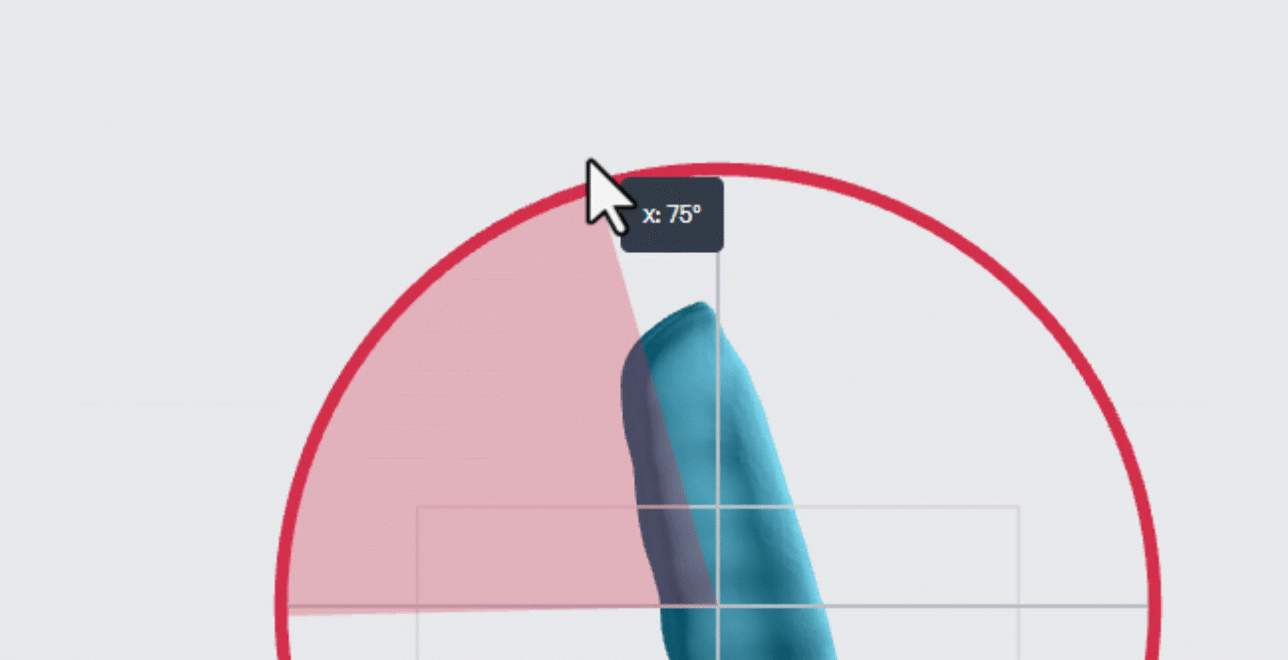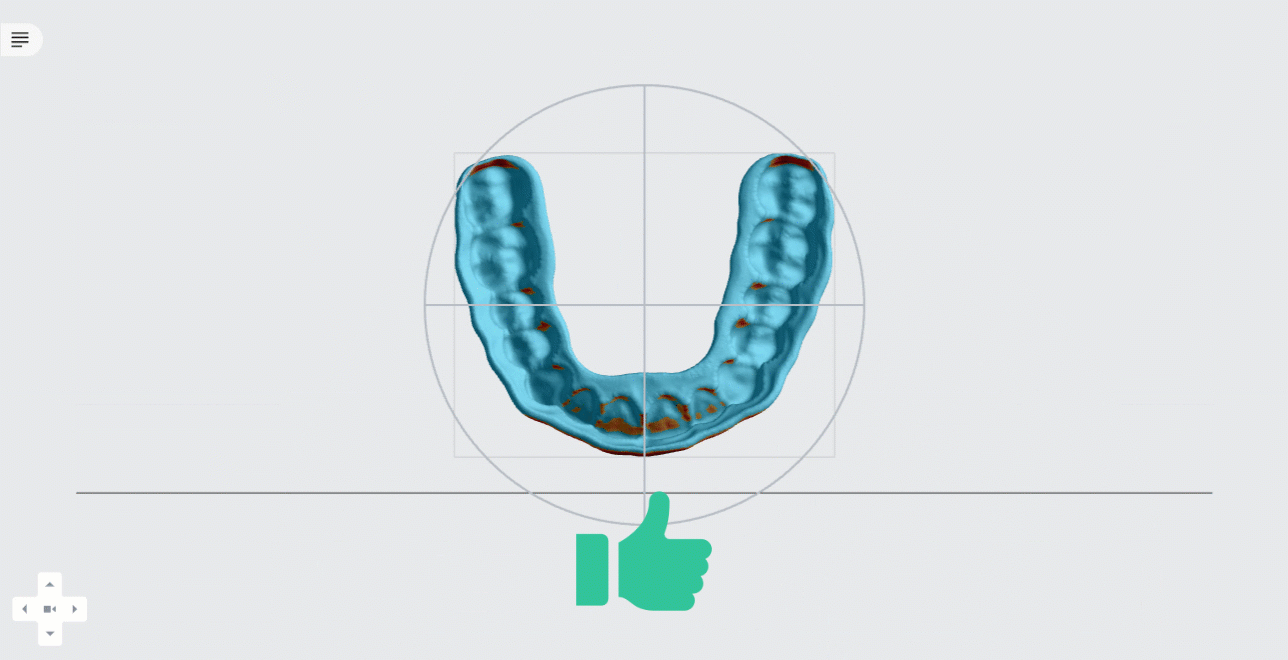
Surfaces that have overhangs will require supports. Supported surfaces will require finishing to ensure proper seating.
Supporting
Enter Support mode
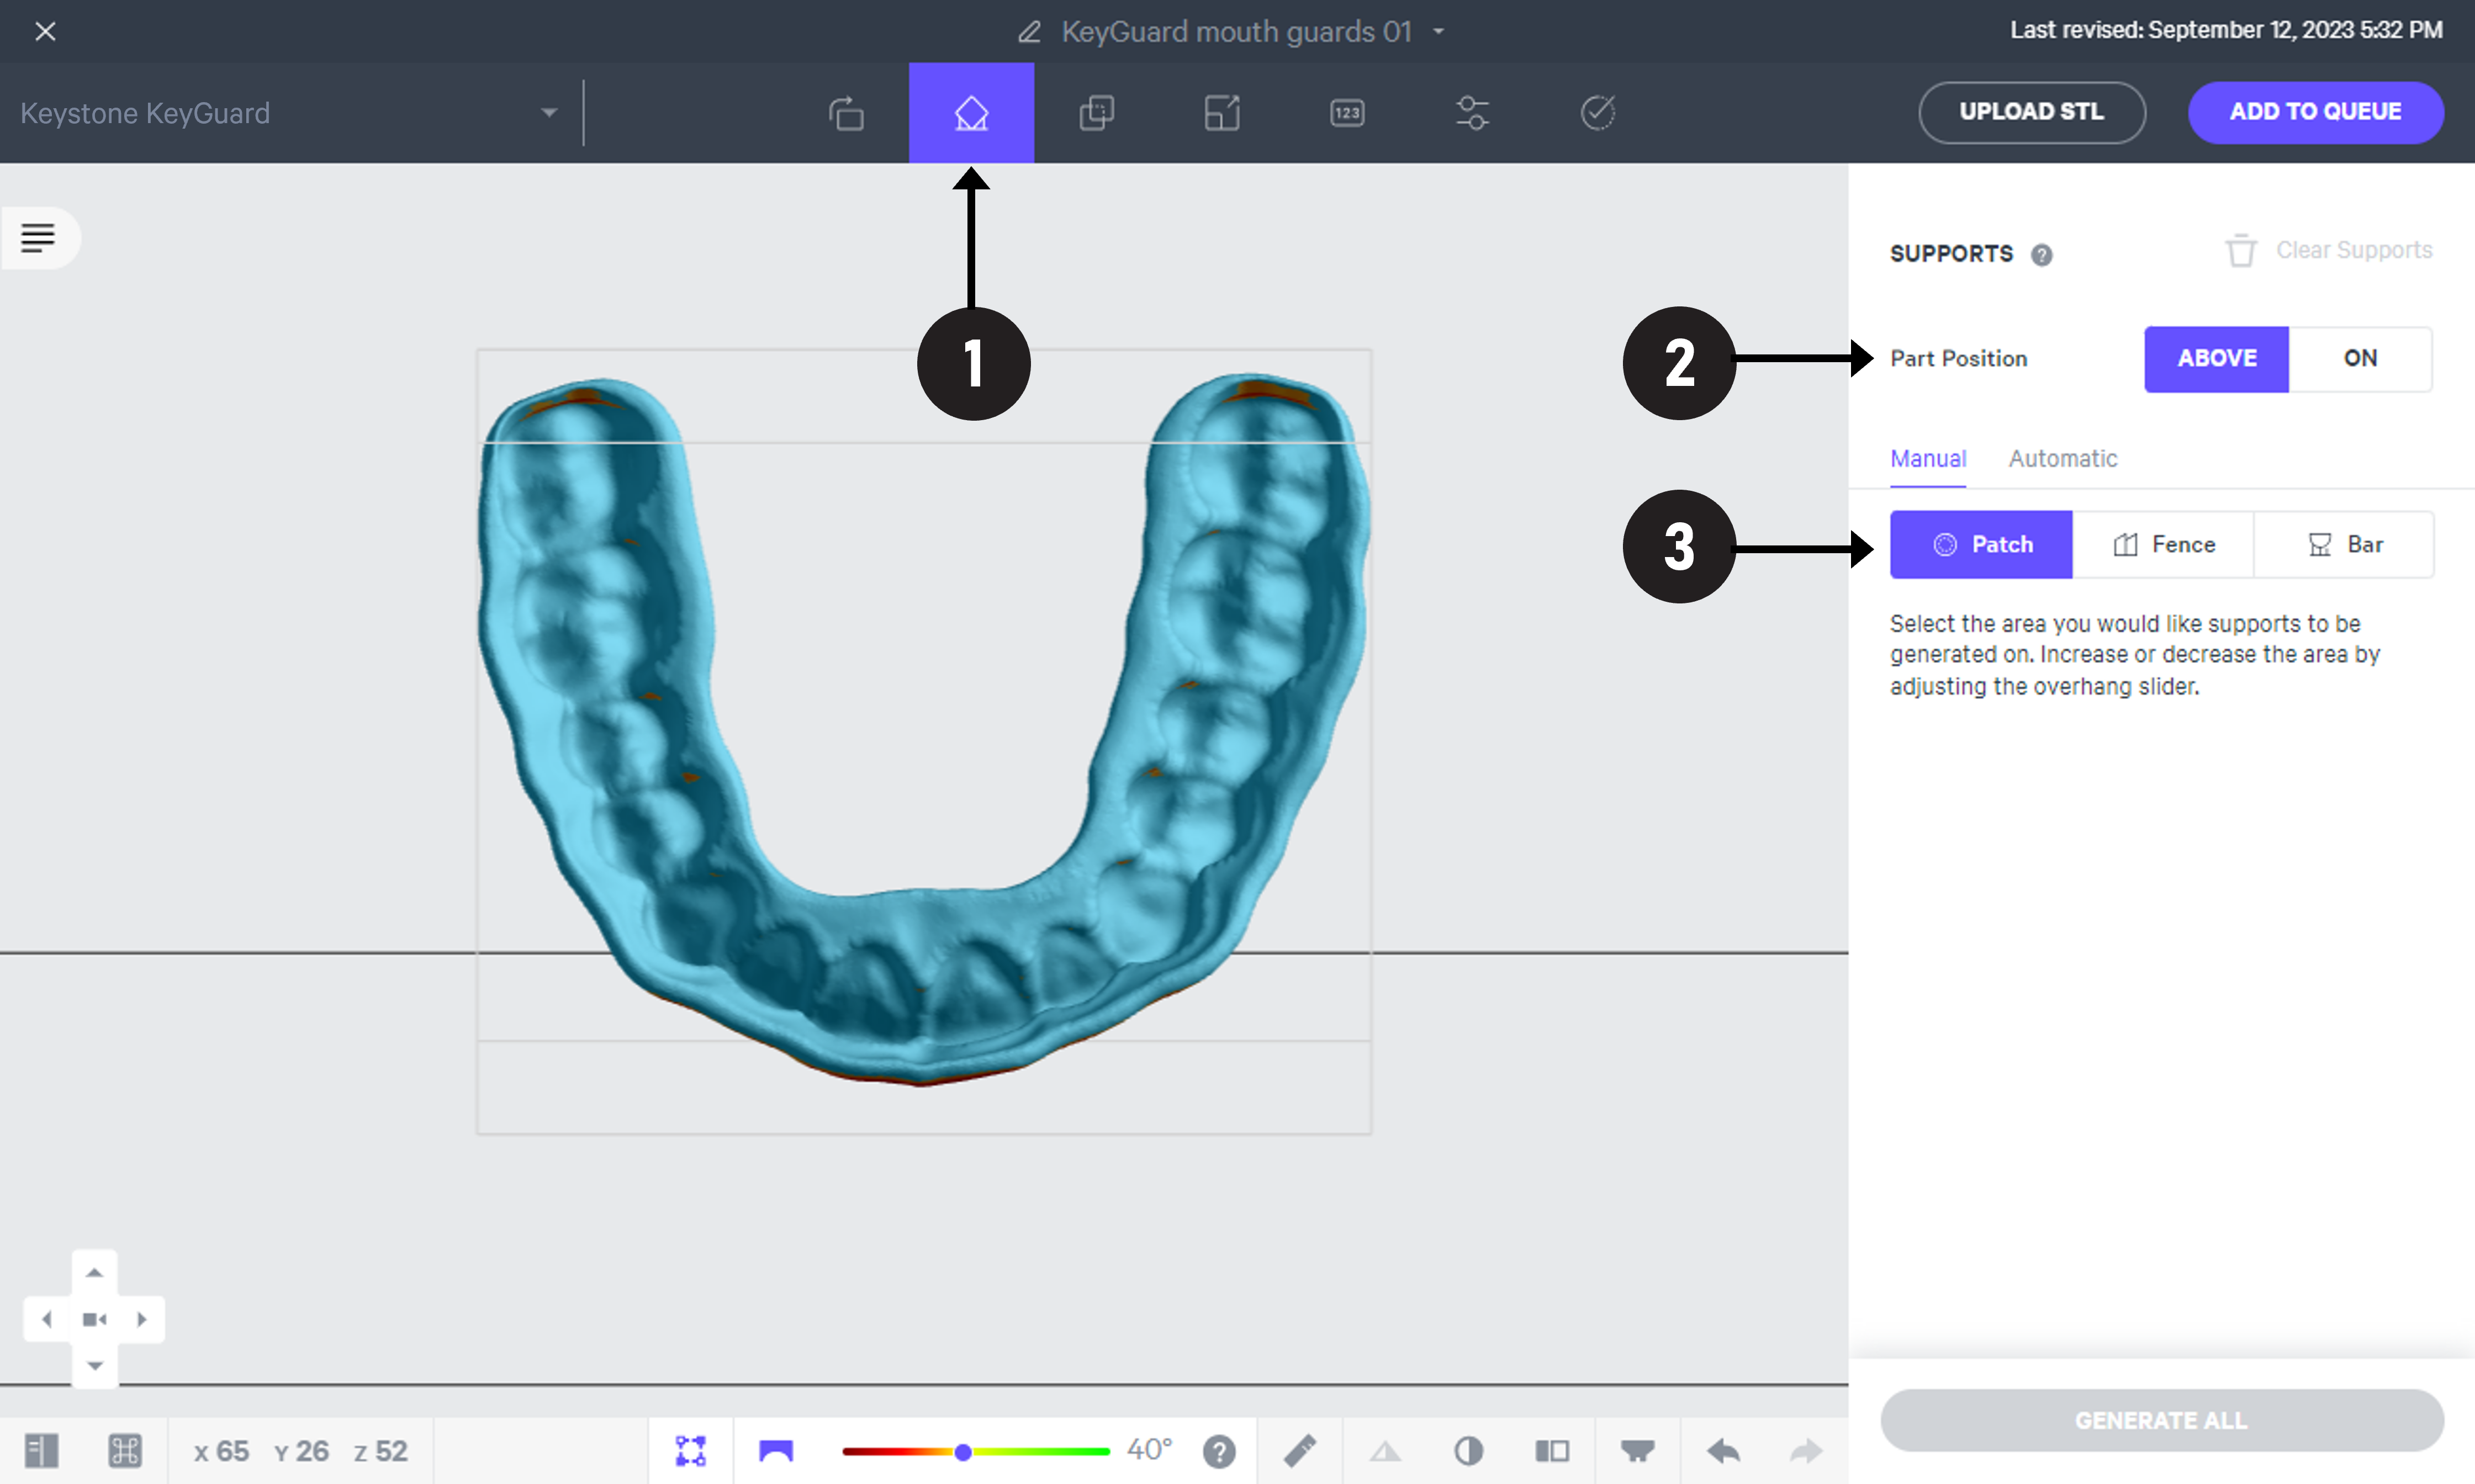
- Click Support in the dark gray bar at the top of screen.
- Under Position, select Above Platform to lift parts off the platform.
- Click the Manual tab and make sure Patch is selected.
Add supports
- Under the Patch tab, adjust the Overhang to between 40 and 60 degrees.
- Select a value to ensure that the patch covers the red overhangs on the anterior surface.
- In the Primary Support Type dropdown menu, select Bar or Fence. Bars tend to provide a stronger connection to the platform. Fences are easier to remove and require less finishing than other support types.
- Enter a Spacing value between 2 and 4 mm.
- Make sure the Boundary Fence checkbox is selected.
- Margin value should be 0 mm.
- Click Generate All to create the supports.
Example of well-supported mouth guard

Nesting

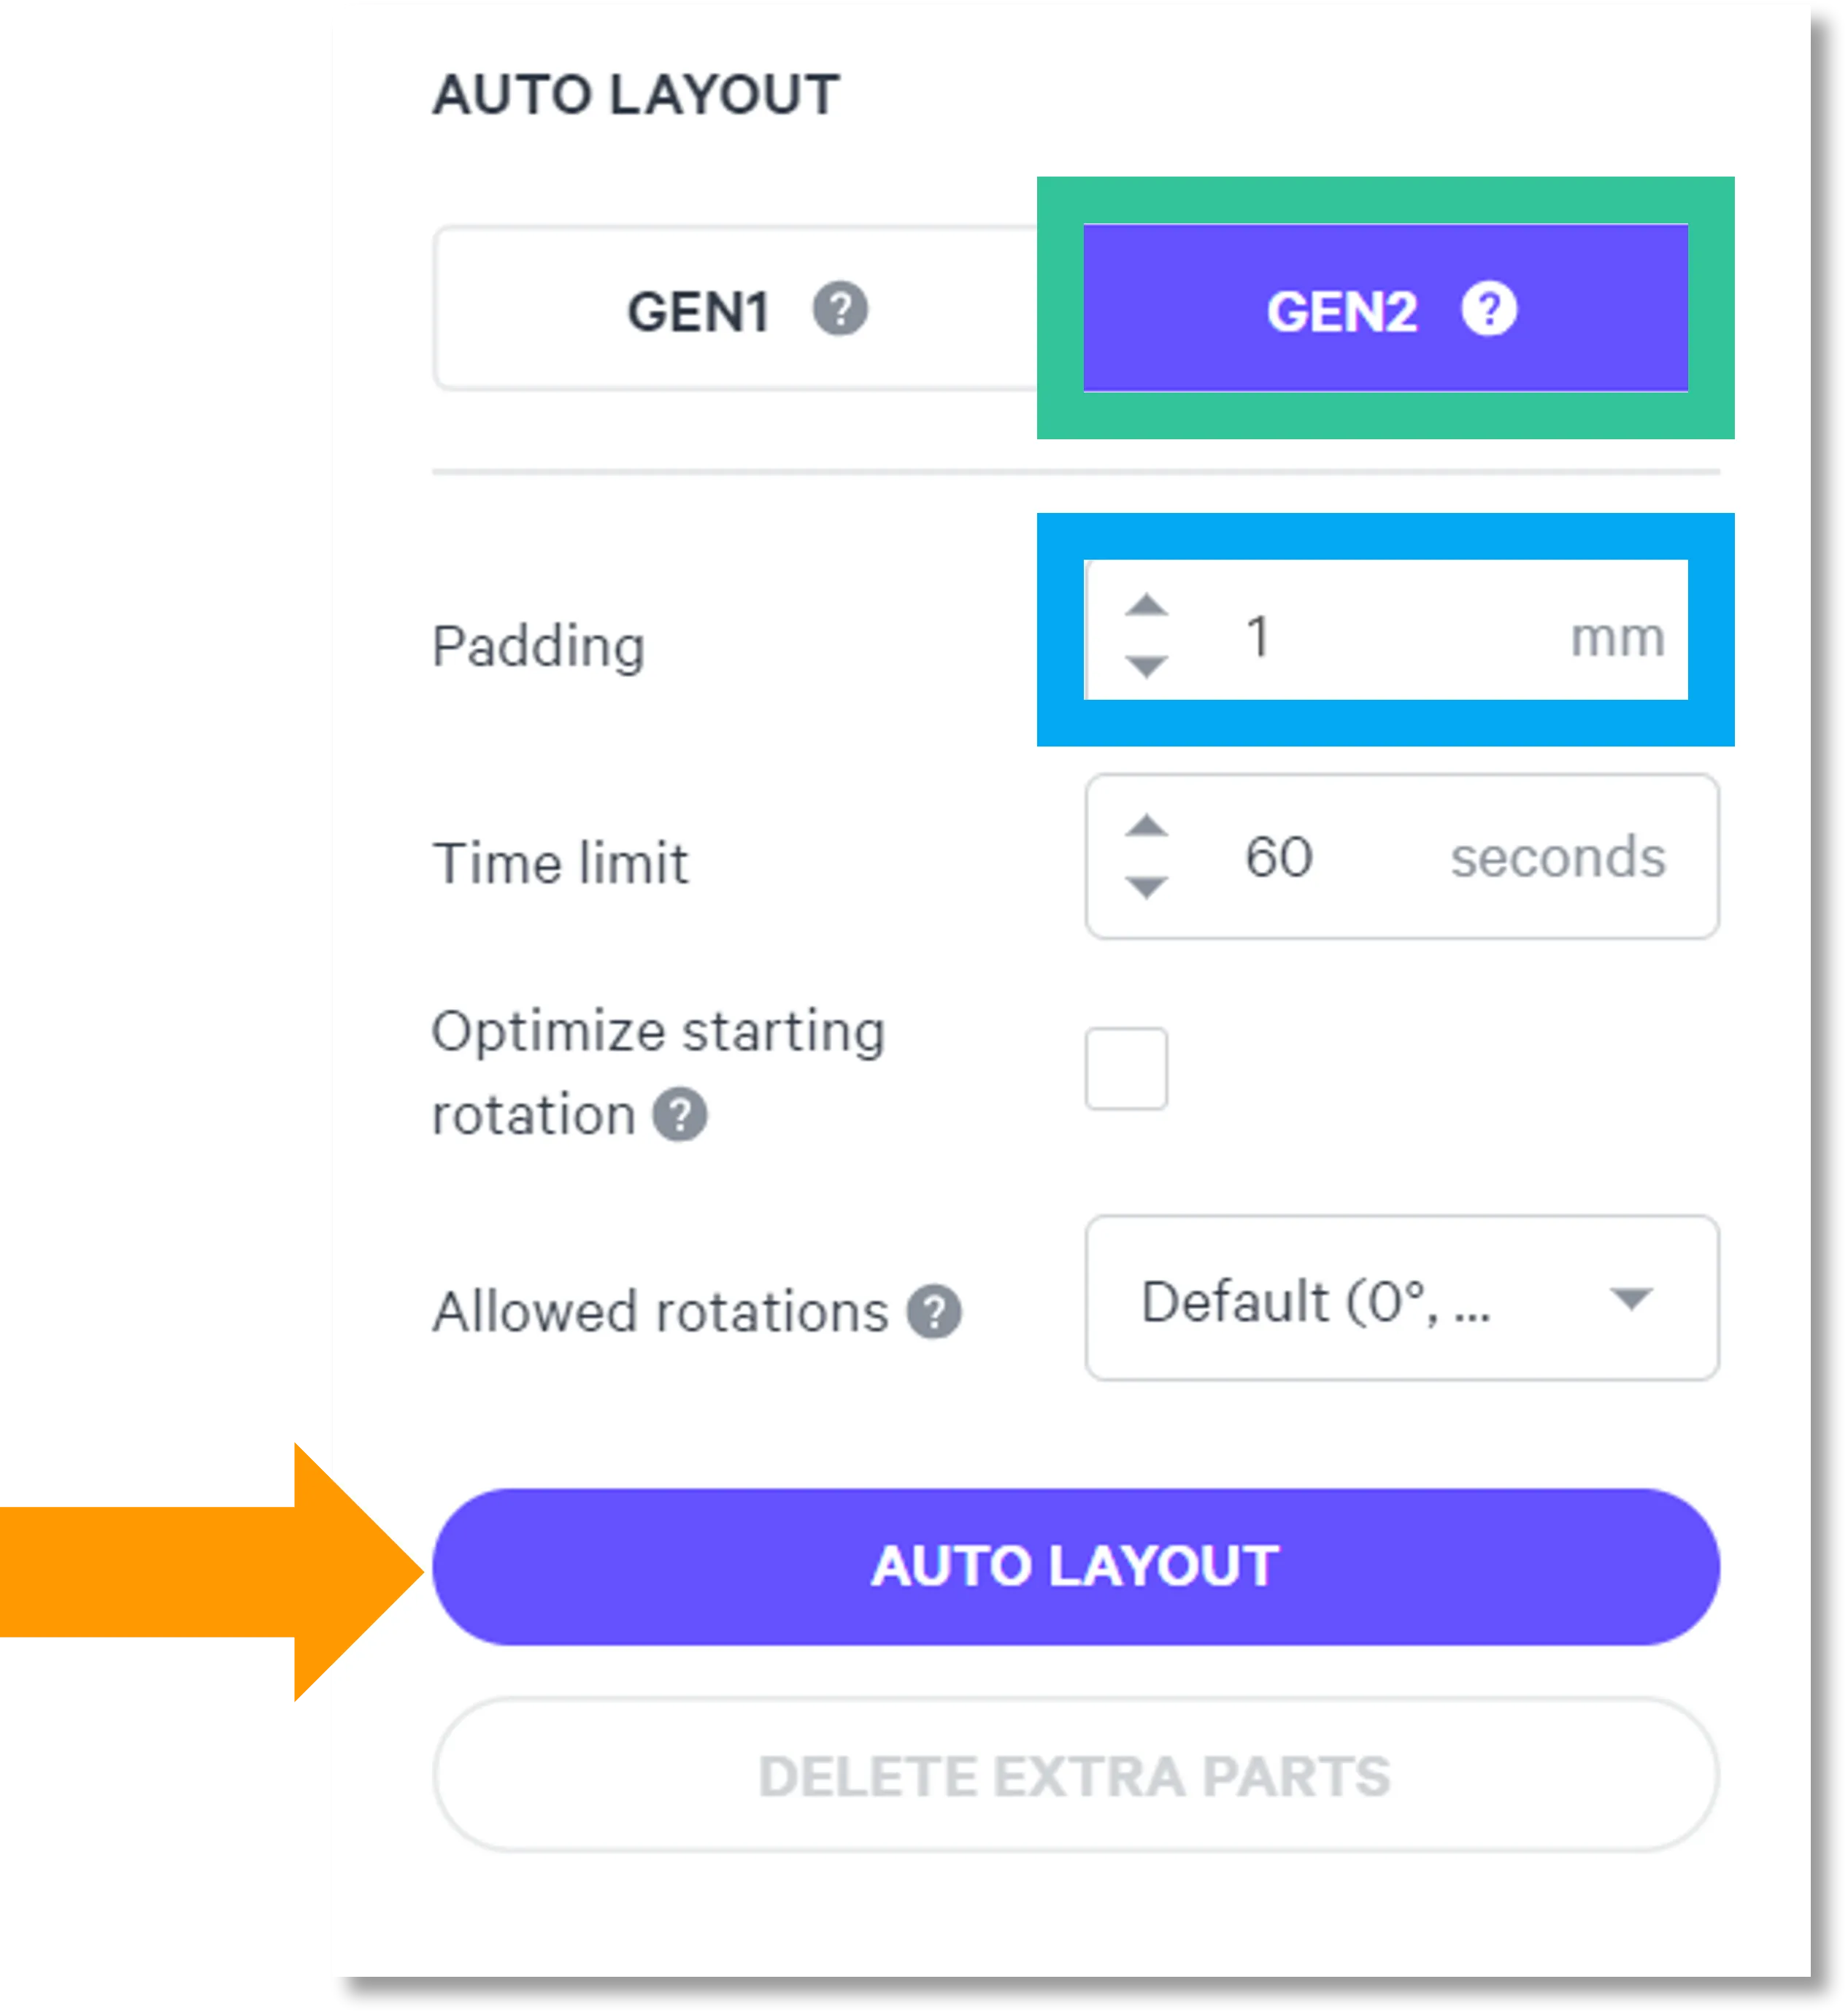
- Select the Layout tab (Shift + L) in the top menu bar.
- Under Auto Layout, select Gen2.
- Gen2 usually gives the most effecient packing for dental devices.
- Enter at least 1 mm in Padding.
- Models require a minimum of 1 mm of space between them.
- Leave Optimize starting rotation unchecked.
- This leaves your parts in their previous orientations.
- Leave Allowed rotations at the default setting.
- This gives the software maximum flexibility to fit the most possible parts on the build platform.
- Press the Auto Layout button to arrange your parts.
If necessary, nesting can be changed manually:
- Click and drag parts to adjust their position.
- Modify Z rotation by using the Spin tool or manual rotations under the Orient tab (Shift + O).
- Use the Part List tab as needed to more easily select models and focus on them.
Print Preparation
Print Controls
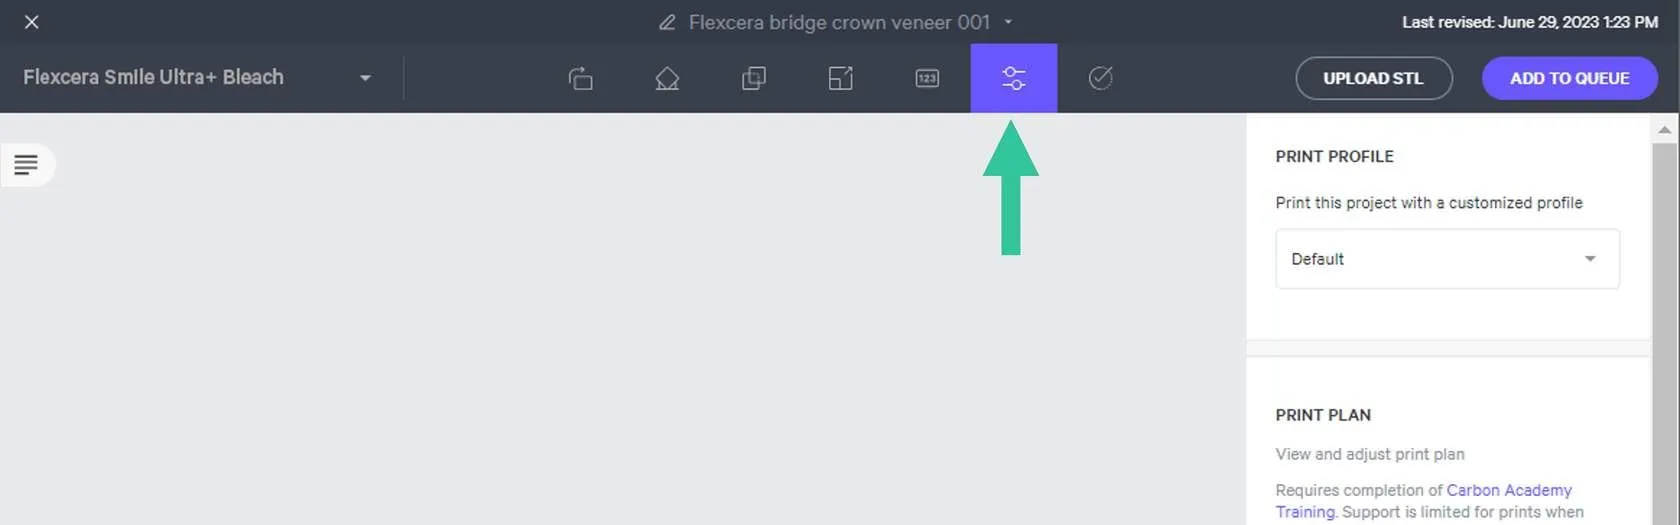
Click Print Controls or Shift + P in the top menu bar.
Slicing
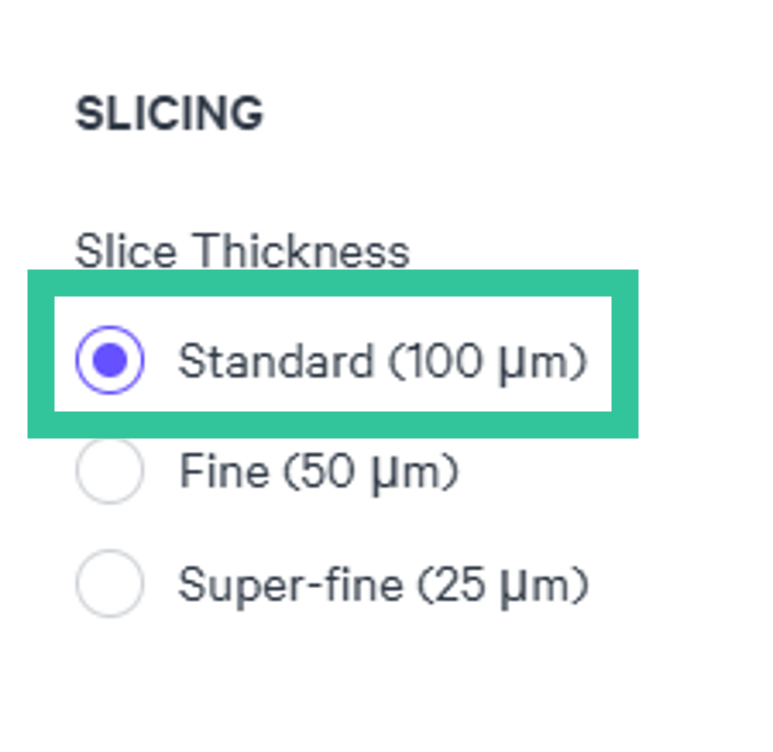
- Slice Thickness should be Standard (100 µ).
- Reducing the slice thickness by choosing the Fine (50 µ) or Super-fine (25 µ) settings will increase print time and may reduce part quality and accuracy.
Project Analysis
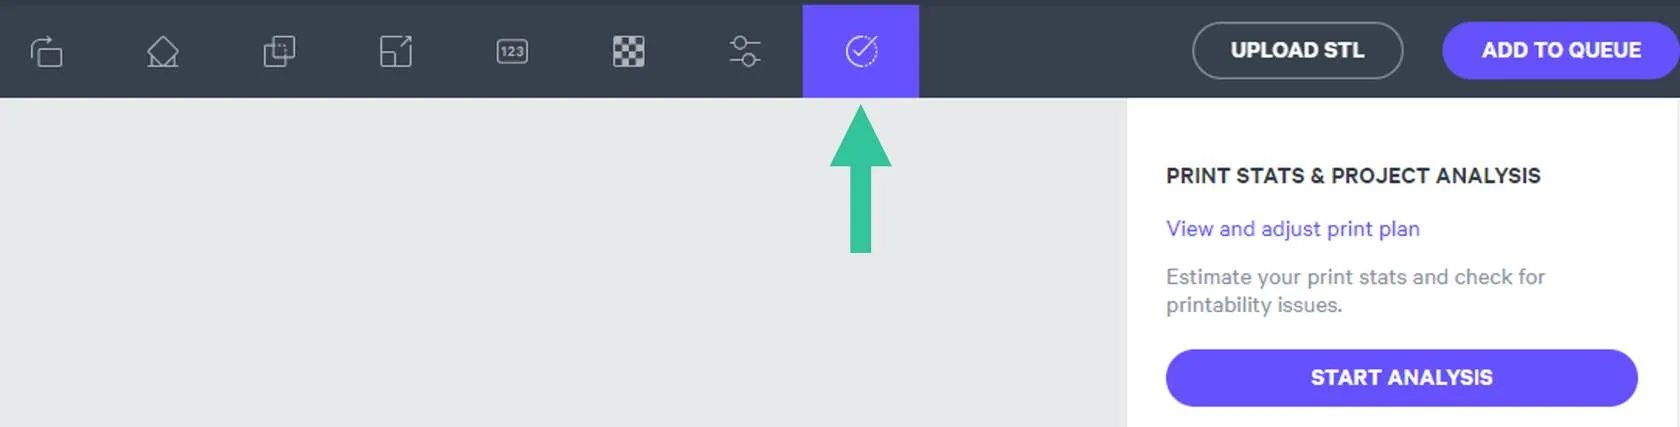
- Select the Project Analysis tab.
- Click Start Analysis and wait for the processing to complete.
- Note the required resin volume and print time.
- Click Add to Queue.
Manufacturer Instructions for Use
Questions & Support
For questions about the resin properties, printing, washing or curing your parts, please contact the Keystone support team:
- Submit support ticket: [email protected]
For questions about your Carbon printer or Carbon software settings used for this resin, please contact Carbon:
- Email: [email protected]
- Phone:
- U.S. and Canada 1-650-285-6307 option 2
- Germany +49 6102 5790849
- UK +44 (0) 2082 647484
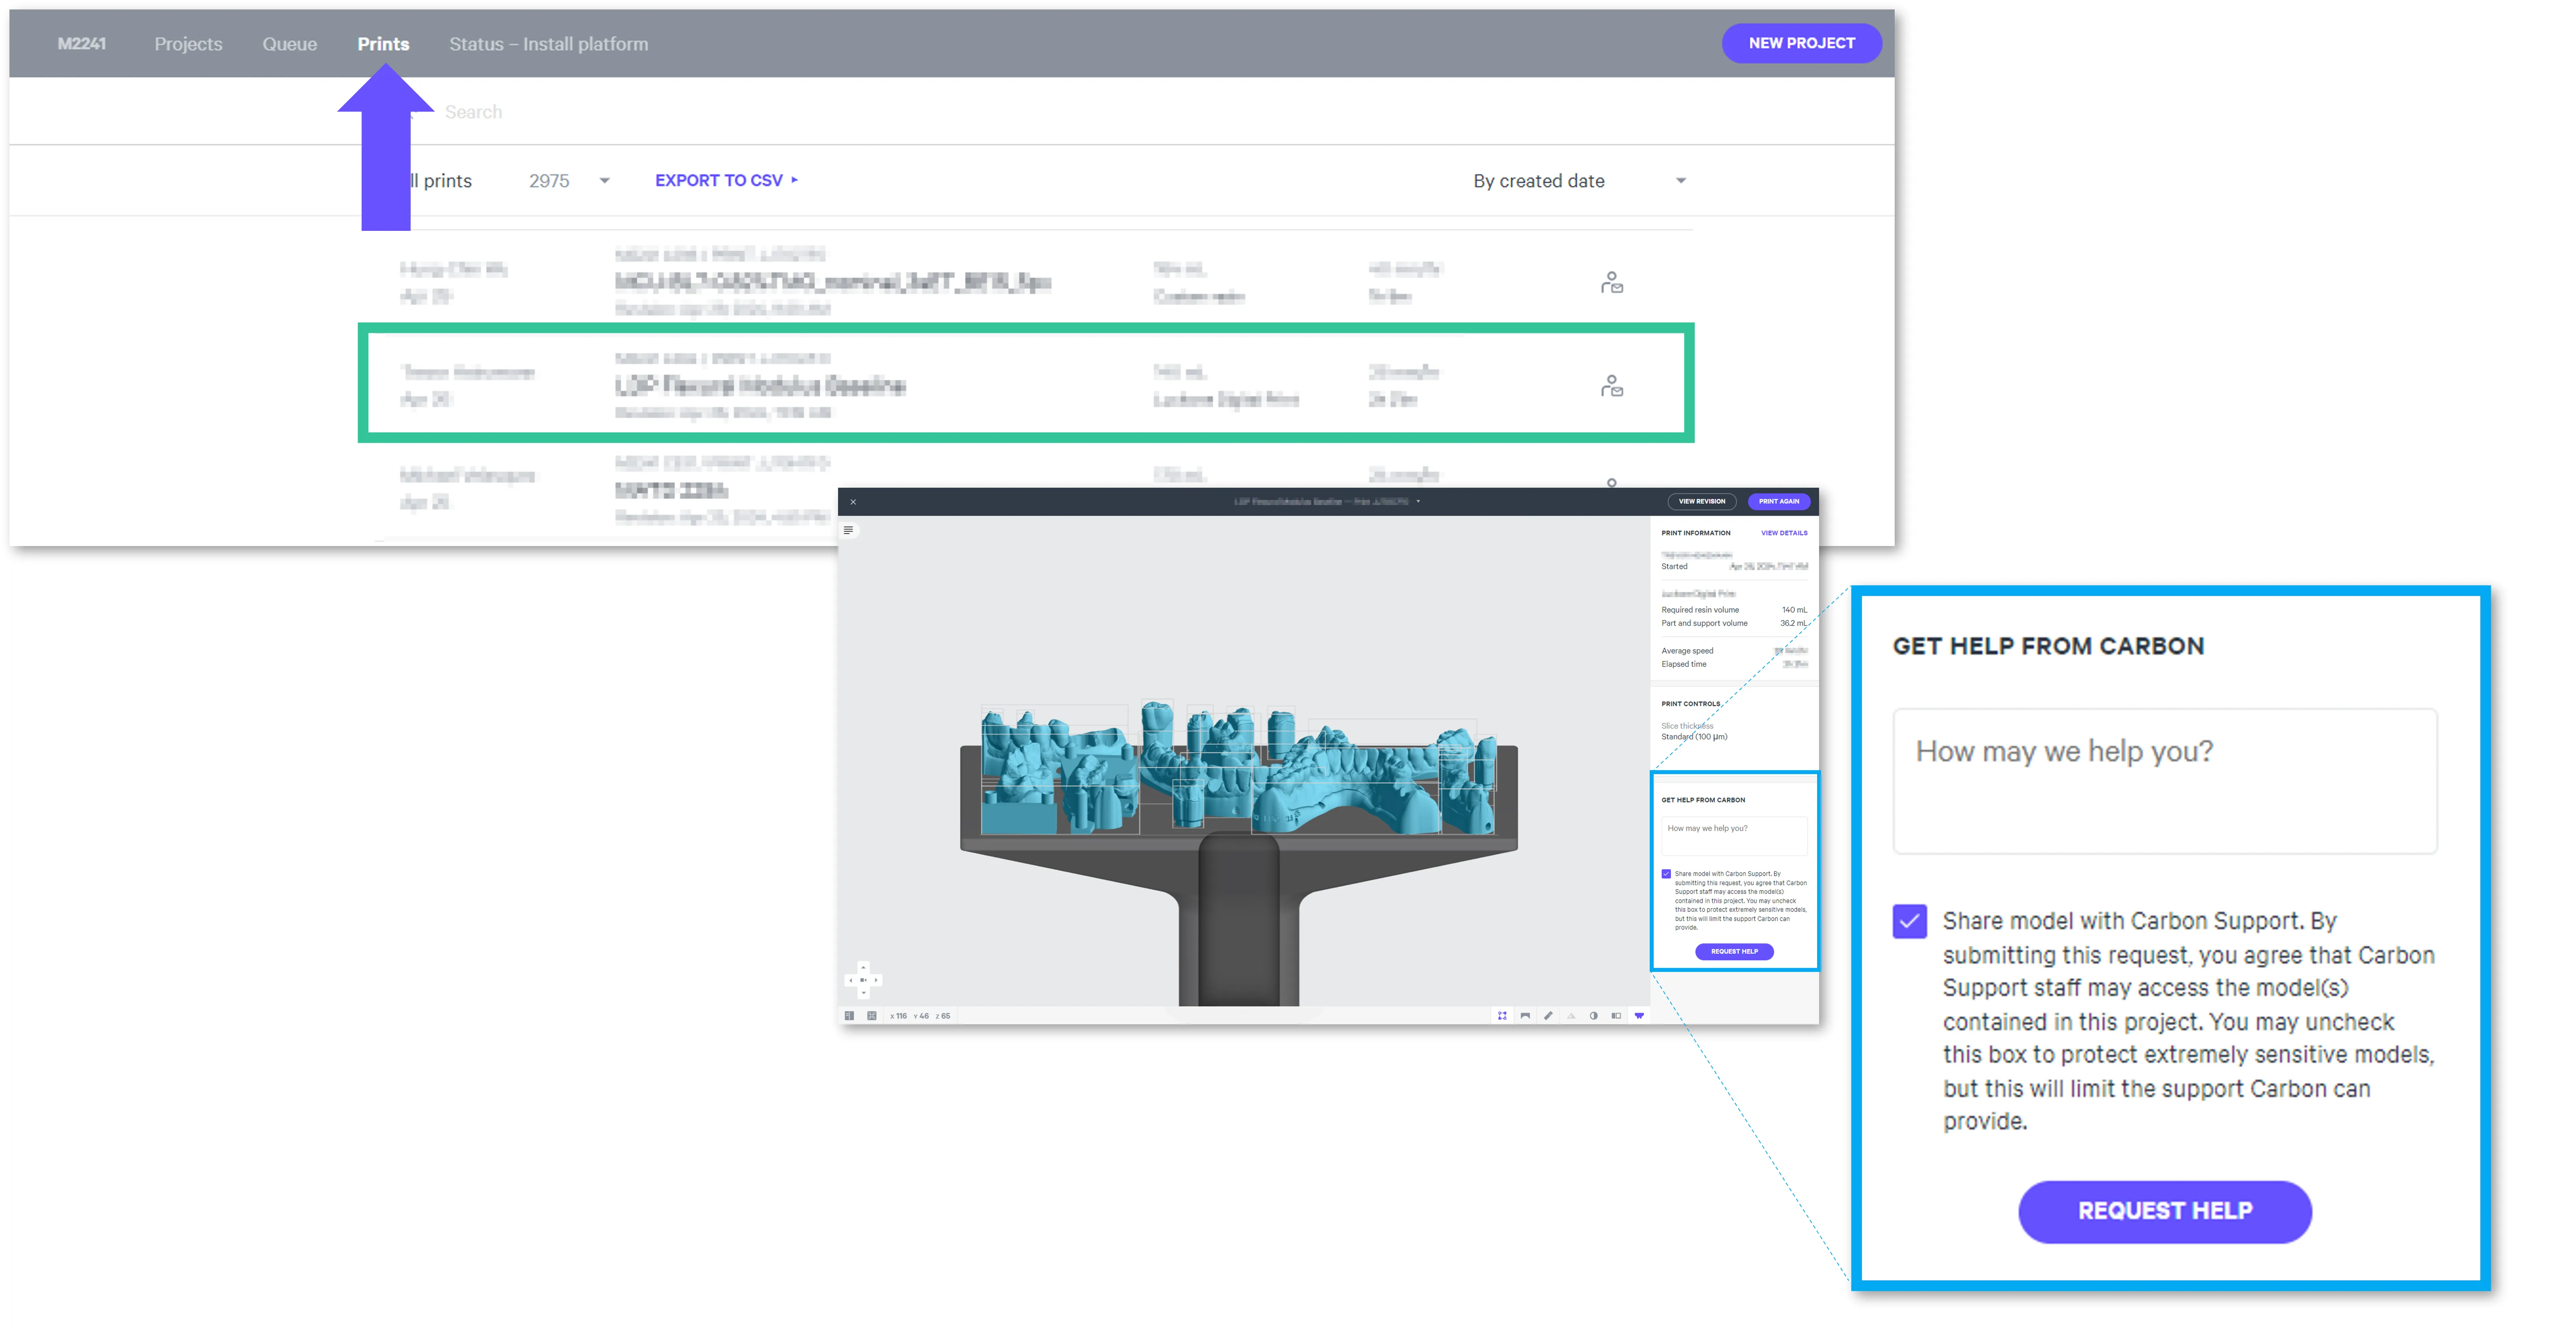
- Printer UI: On the dashboard, select the Prints tab. Select one of the printed projects. Click Request Help in the lower right corner.