Resin Starvation
Resin Starvation
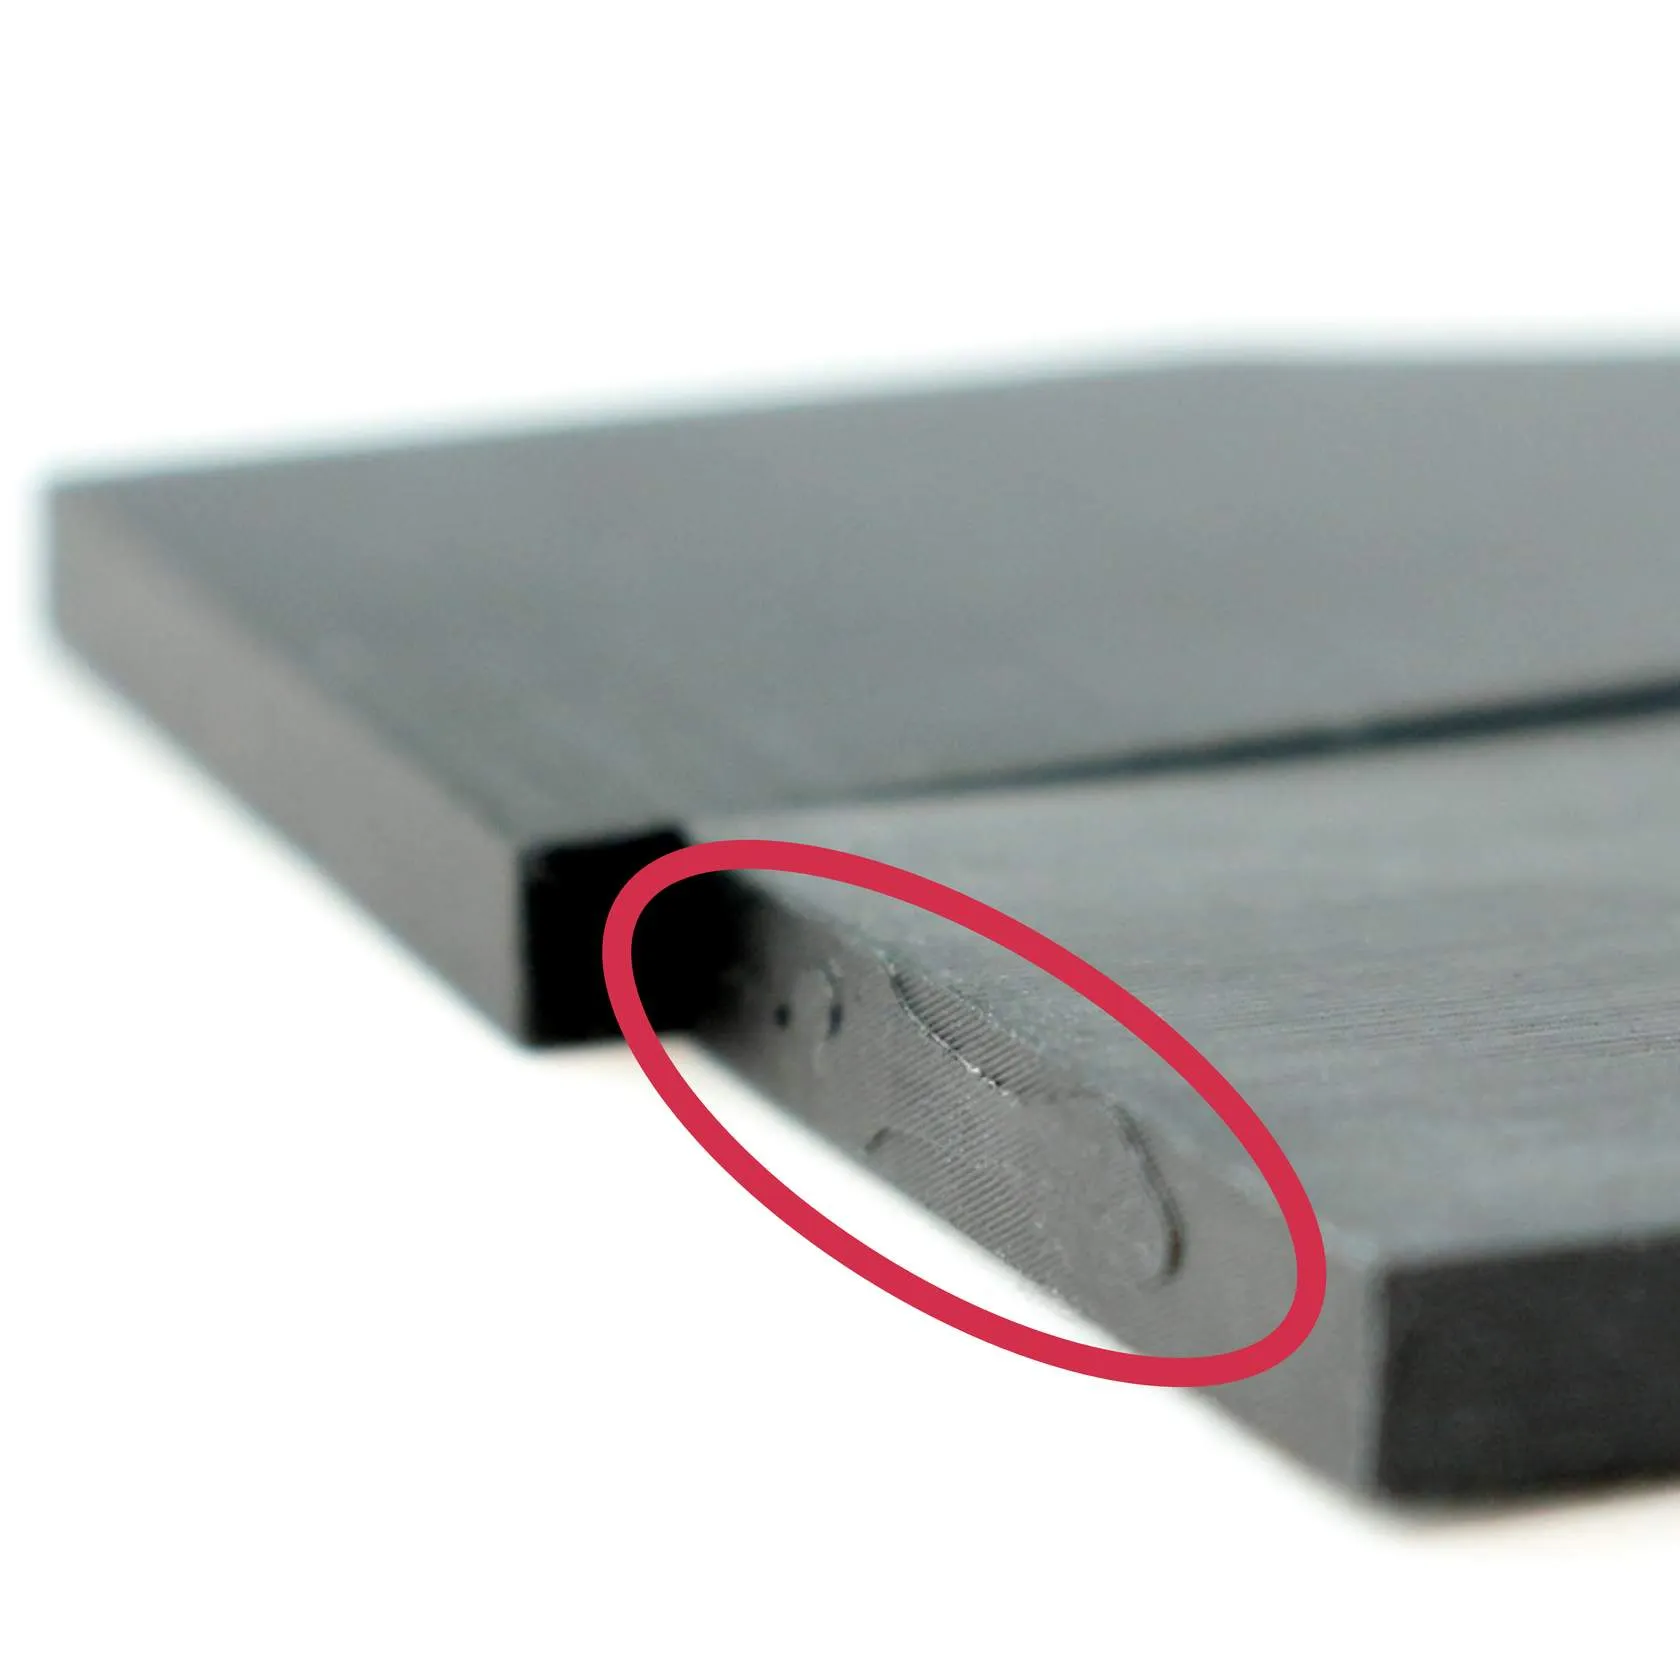
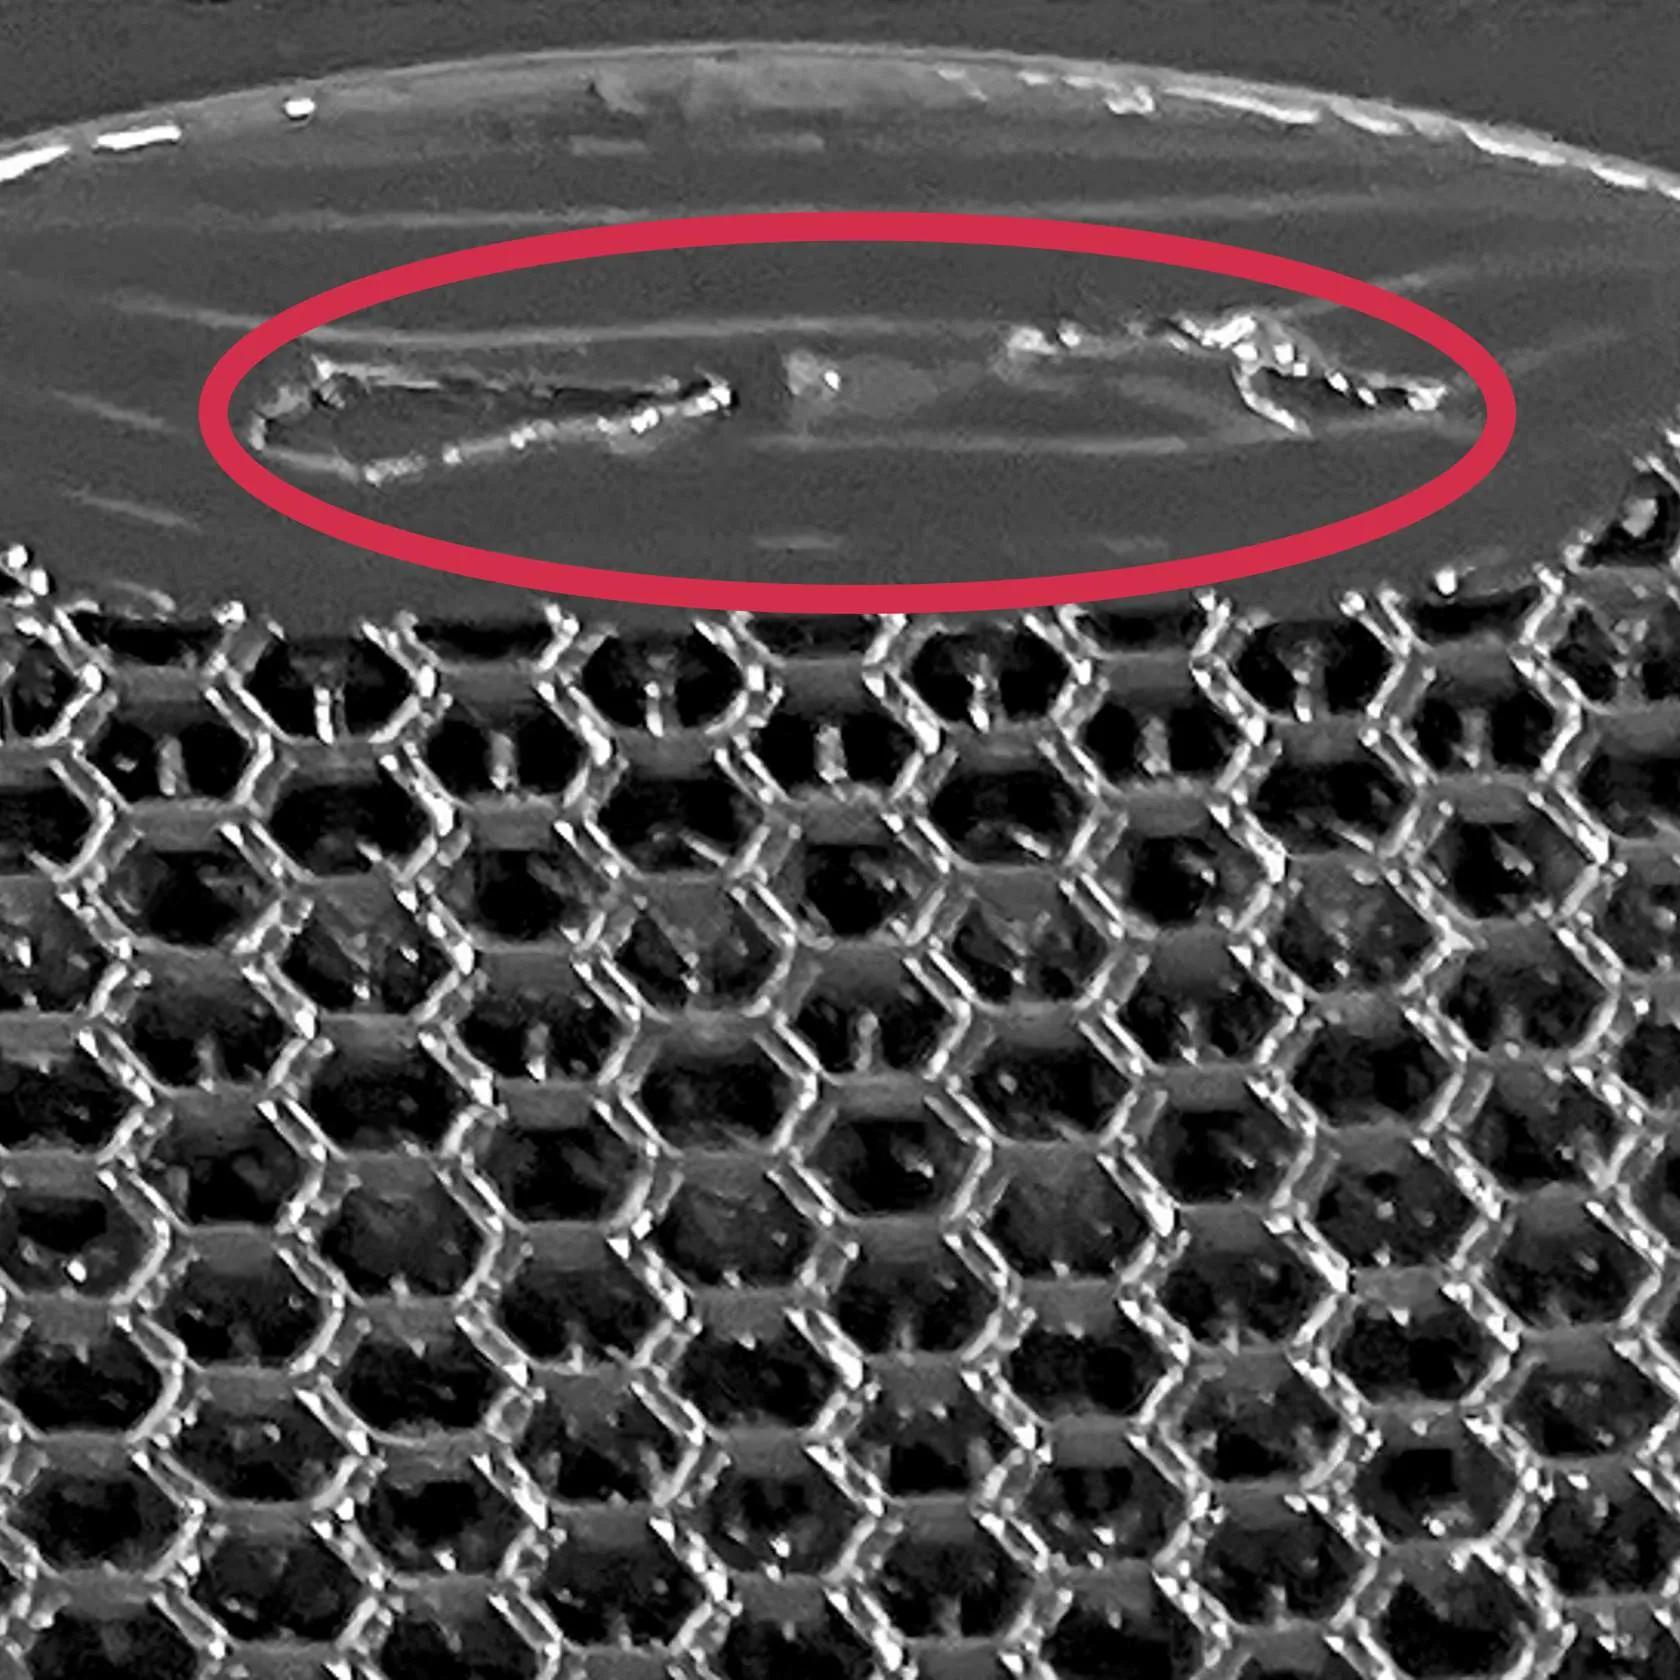
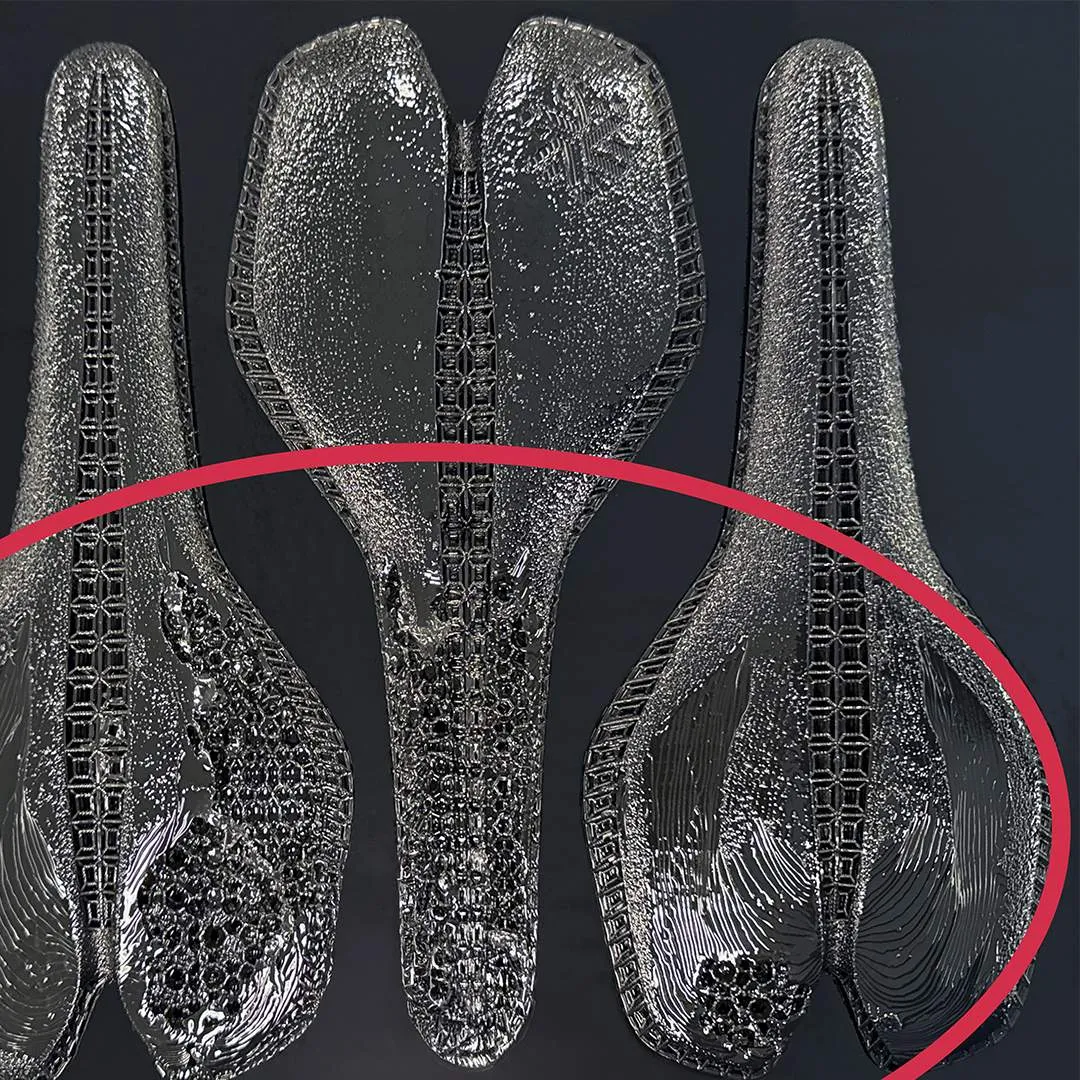
Resin runs out during a print or is locally starved due to part geometry.
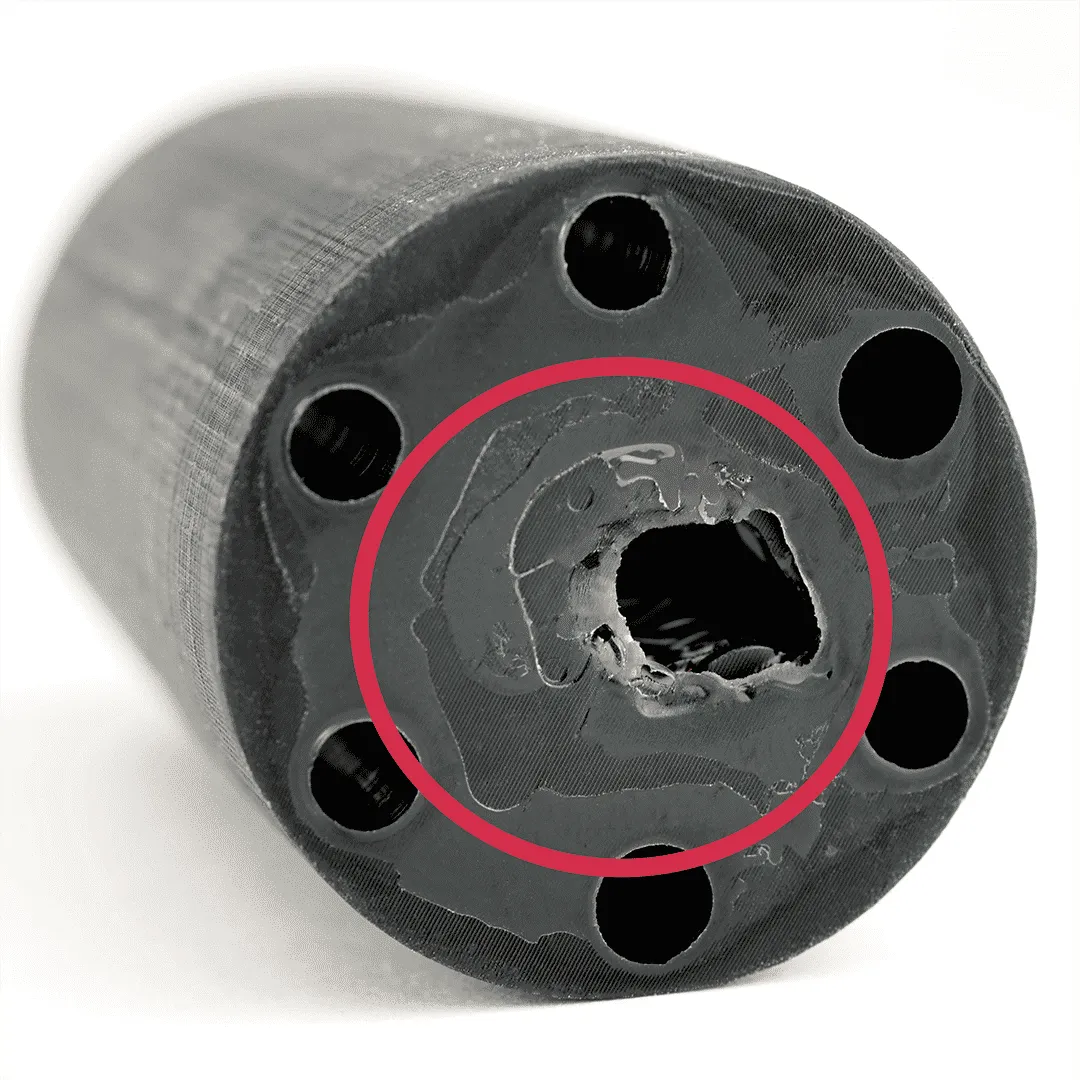
How to Identify
Resin Starvation can be diagnosed as follows:
- Window is not fully covered with resin at print’s end.
- Part feature(s) are missing or did not fully resolve.
Voids is a defect that can appear similar as it arises from similar circumstances.
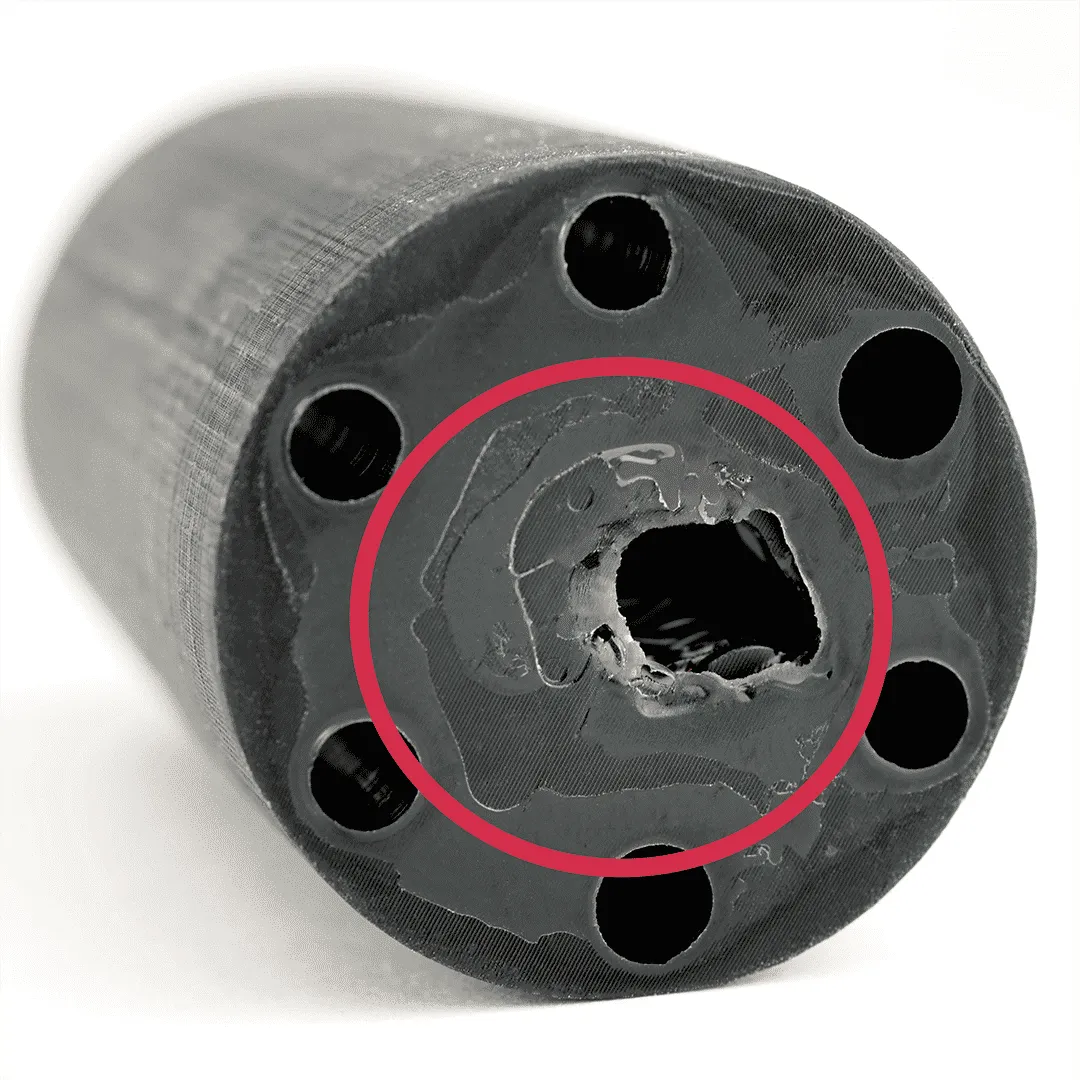
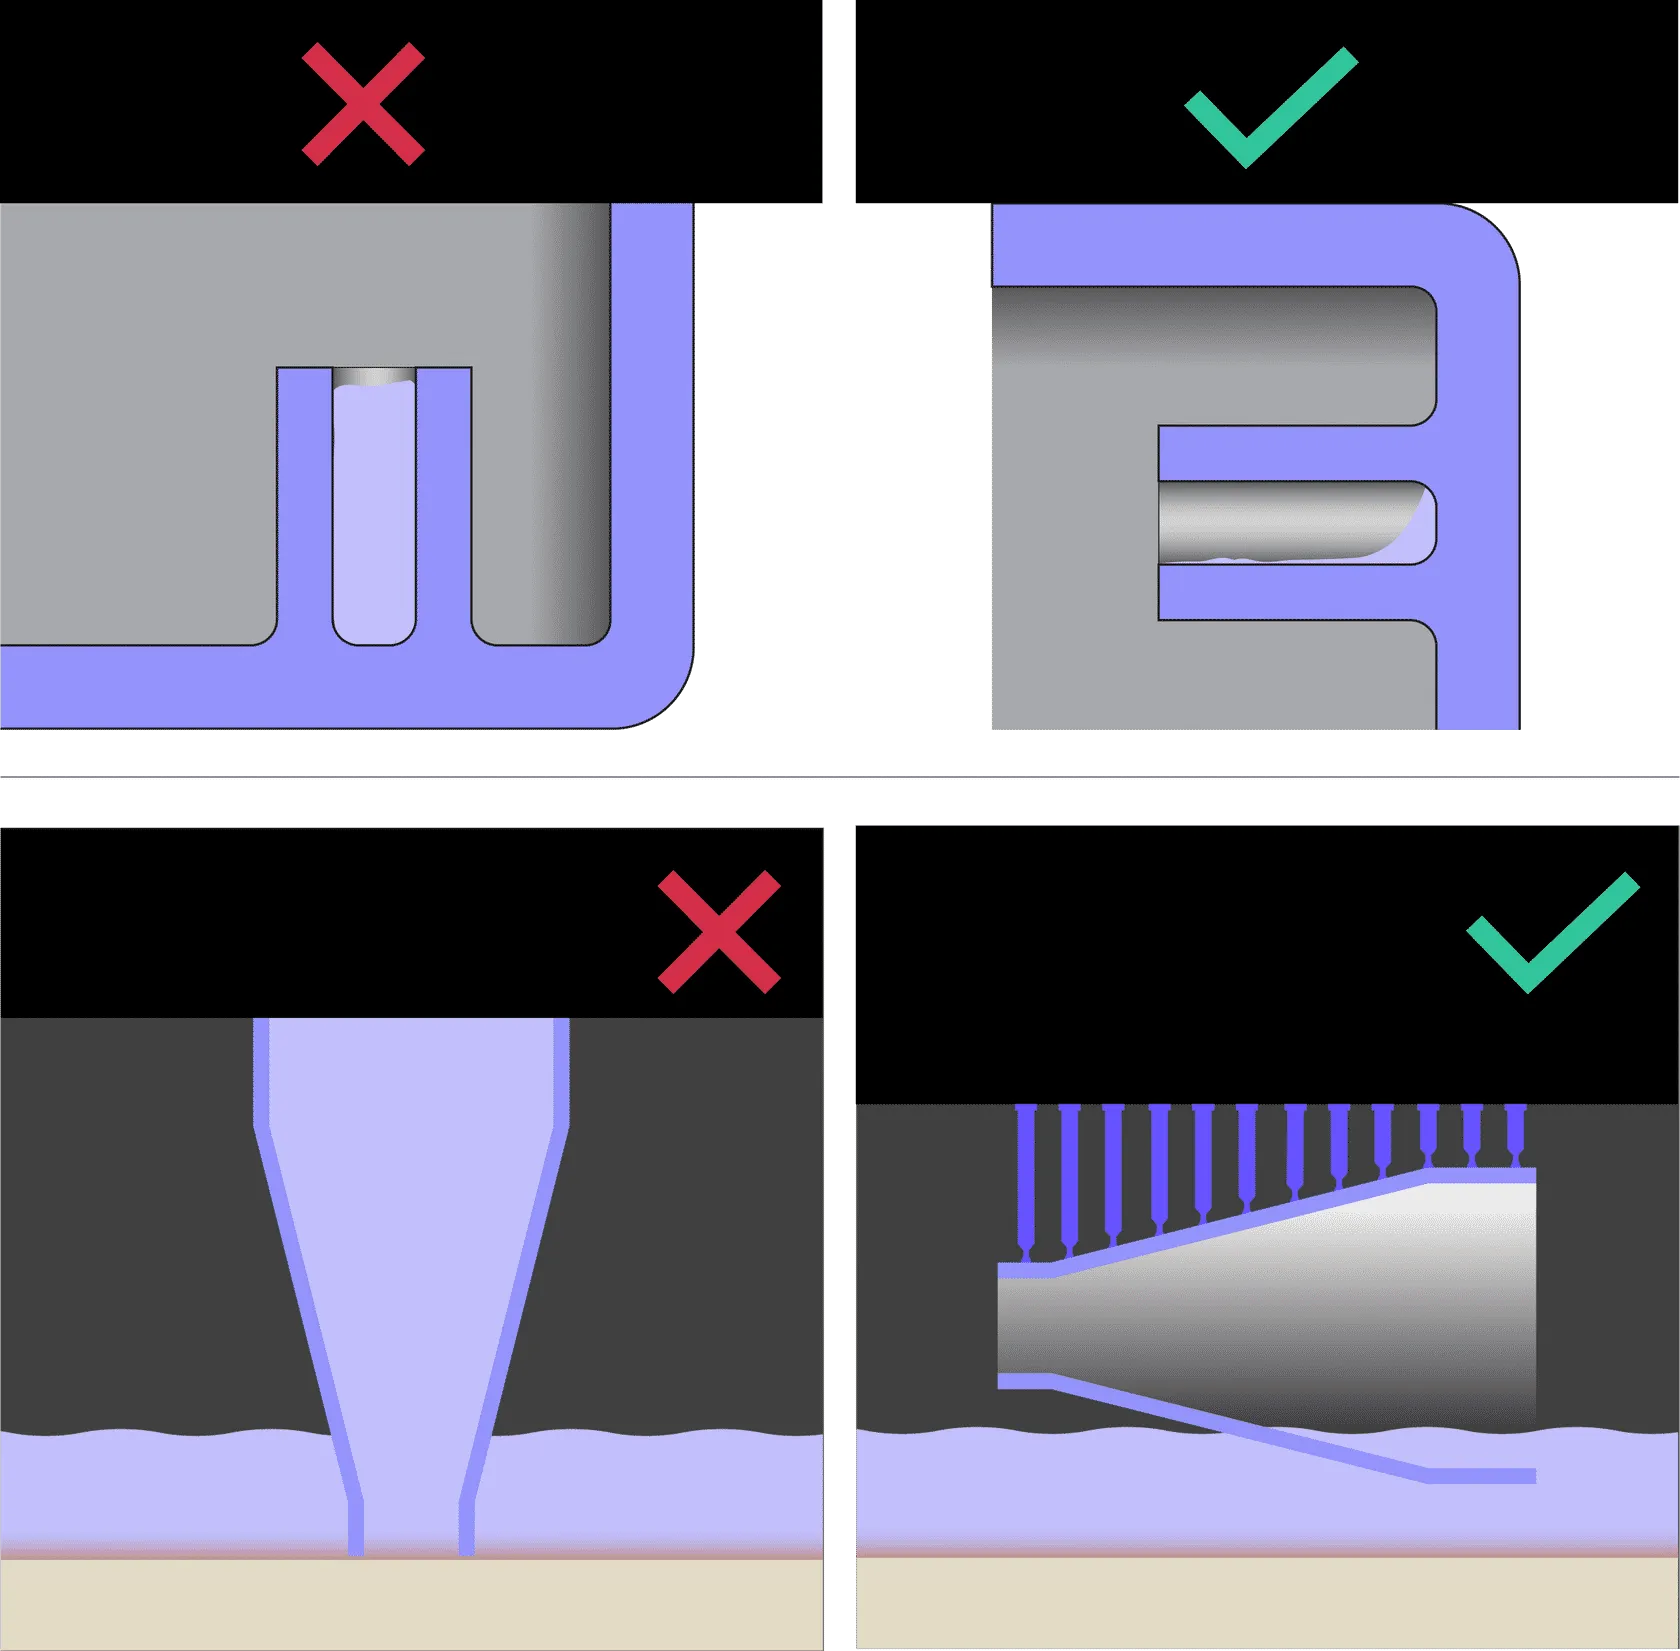
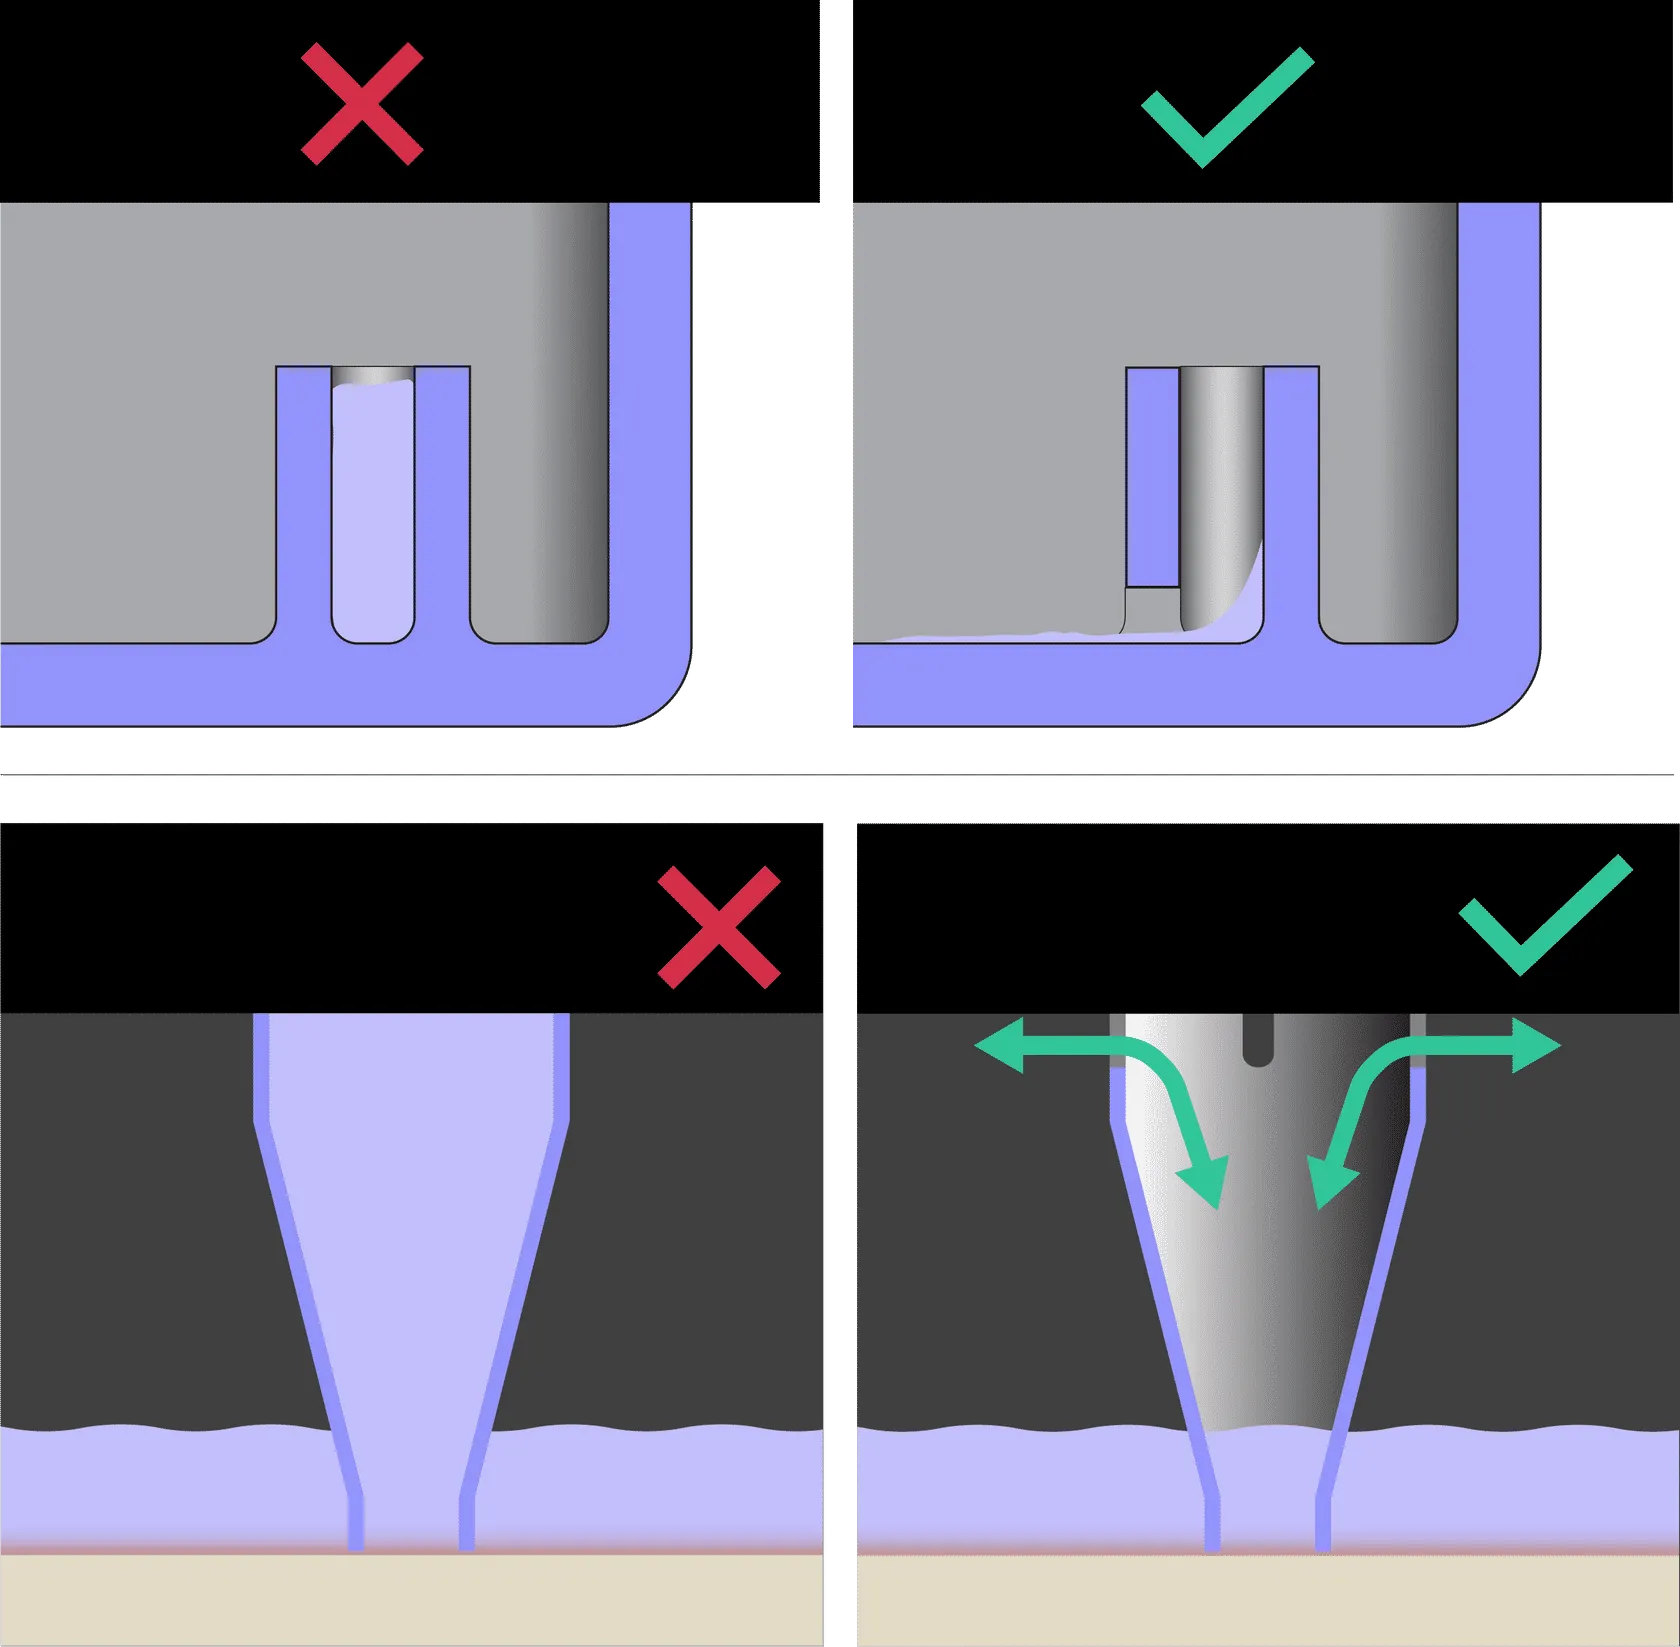
Cause - Unvented Volume
Solution - Print Preparation or Part Design
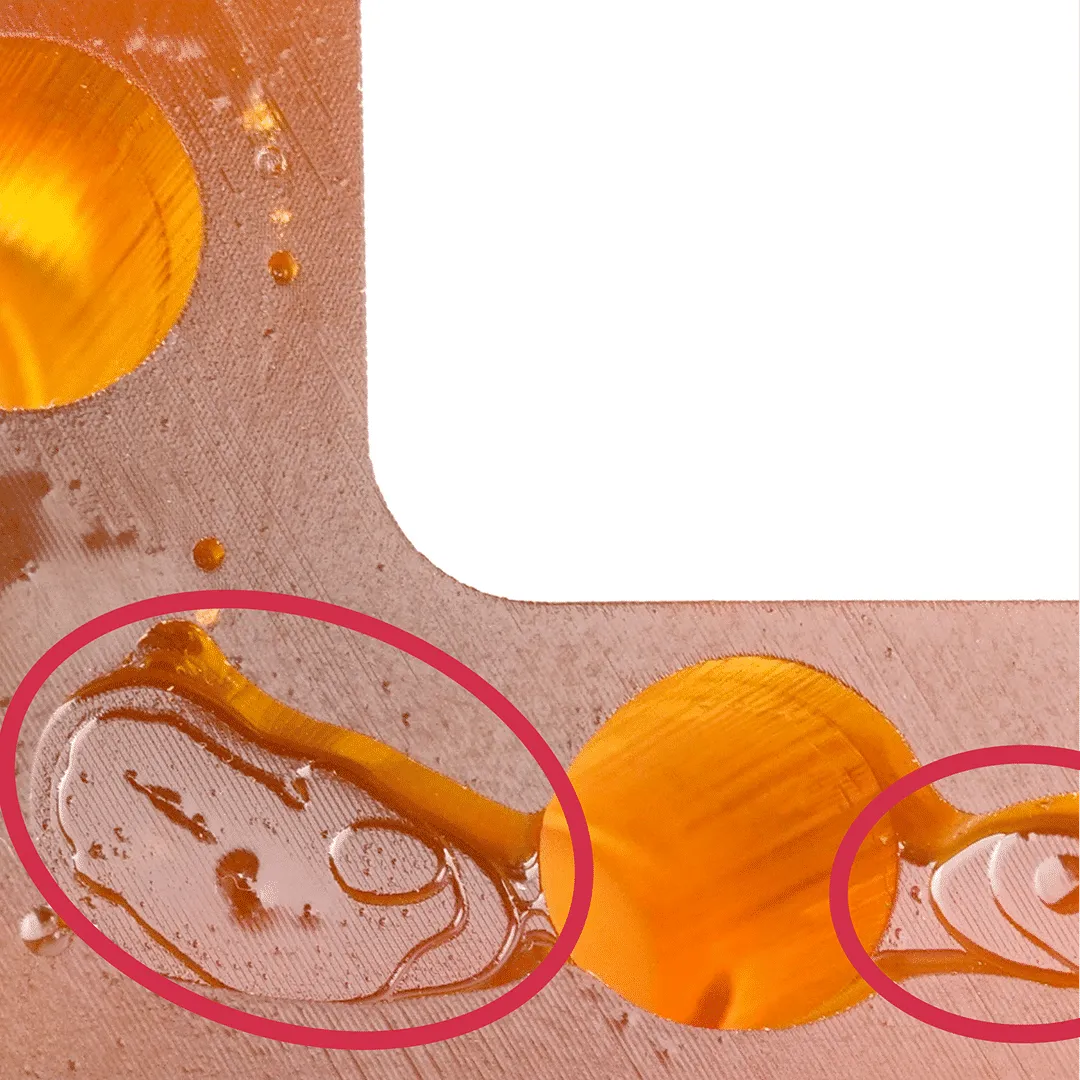
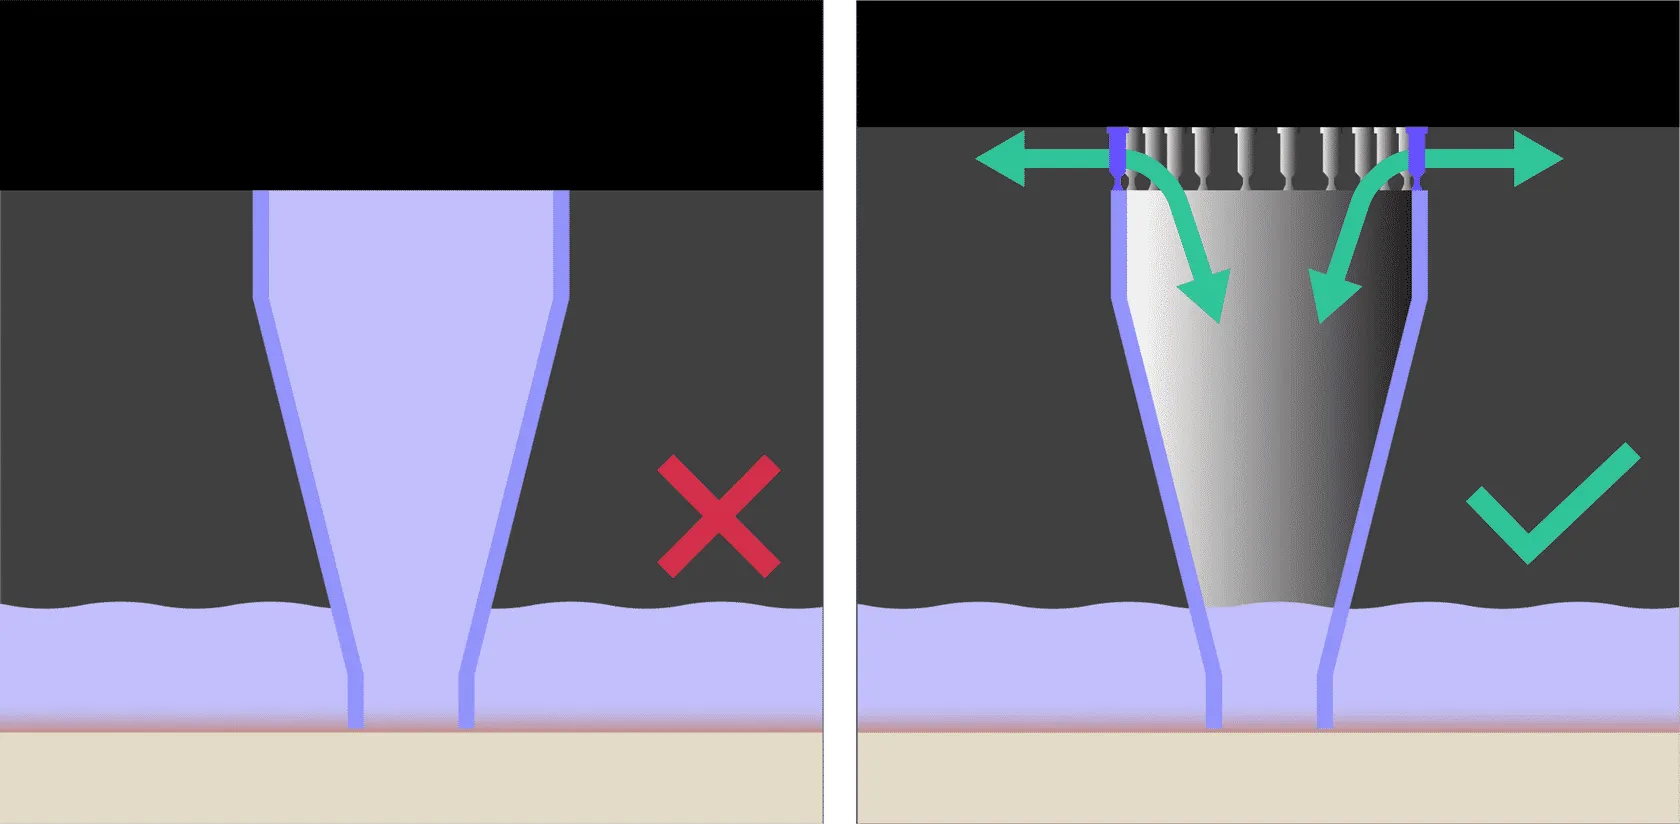
Cause - Part Geometry
Solution - Print Preparation or Part Design
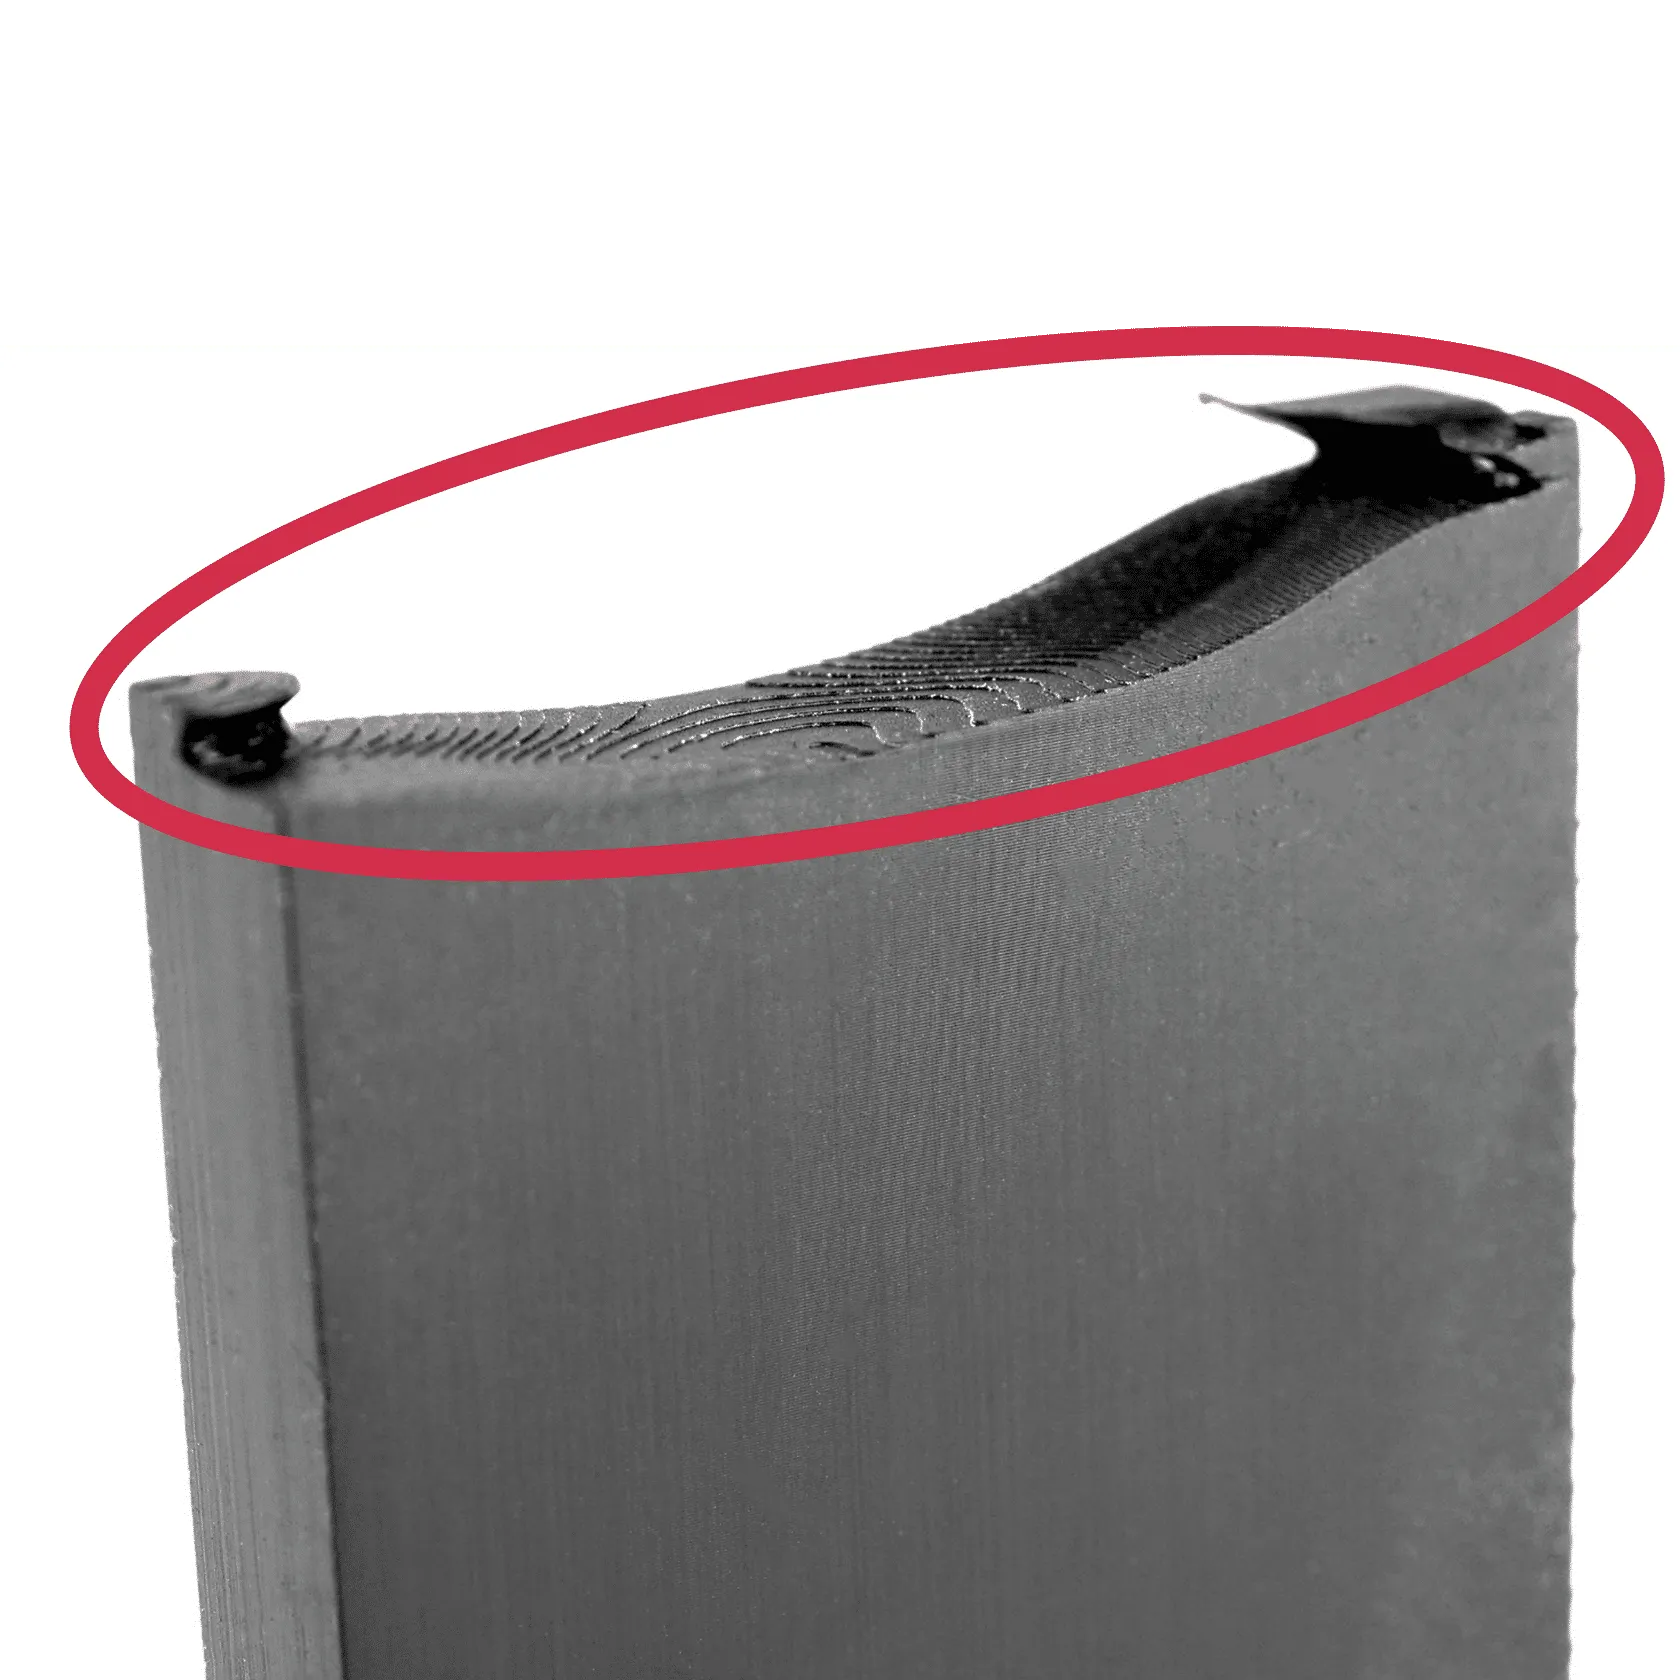
Cause - Inconclusive
Cause - Inconclusive
Cause - Inconclusive
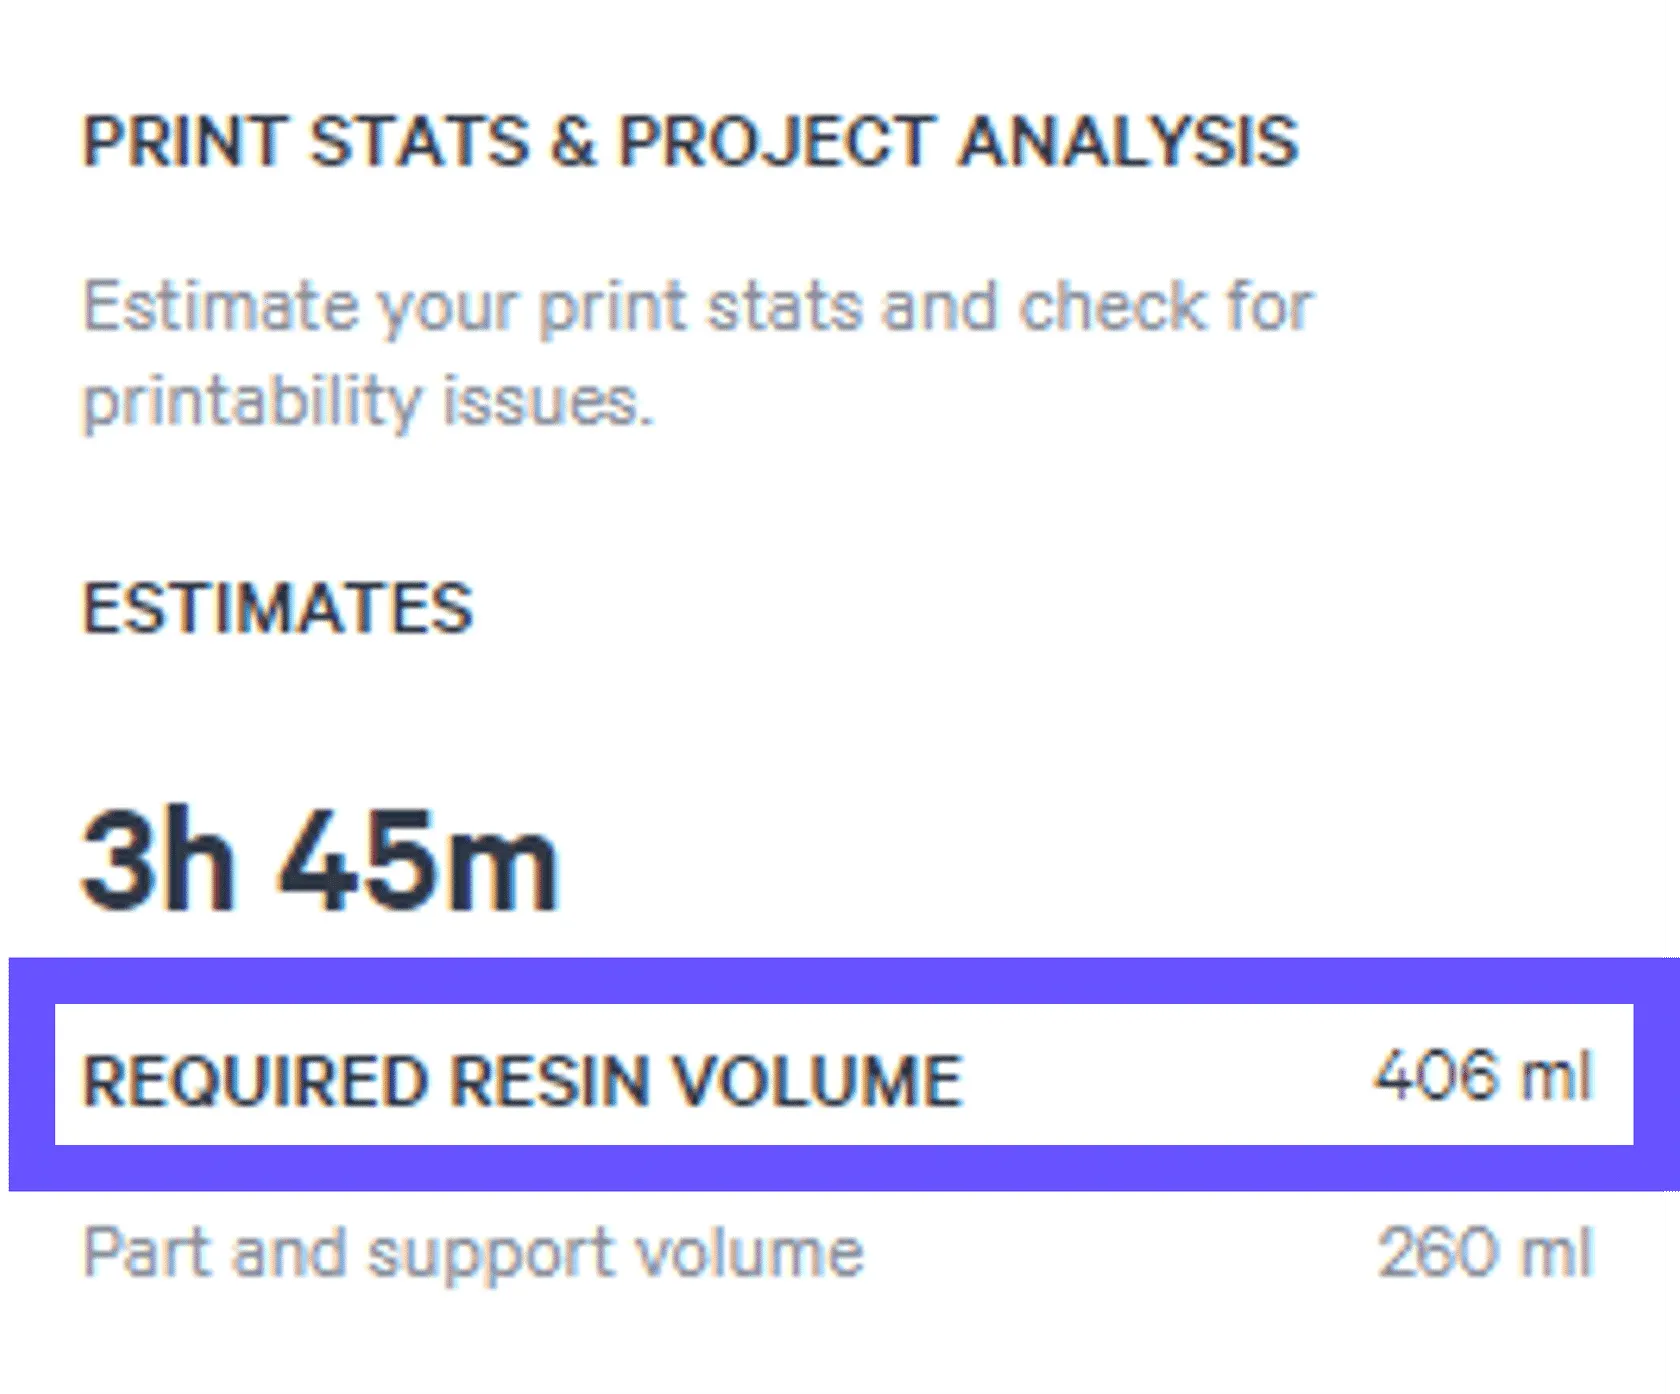
Cause - Resin Amount
Solution - Resin Check
Troubleshooting
It is recommended that you review all the possible solutions before taking action to ensure you are pursuing the best course of action.
If the best course of action is not apparent, try the troubleshooting options in the order listed. Refer here for more tips.
Process, Material, and Hardware Checks
If any of these conditions apply to your print, take the corrective action and reprint to see if the problem is resolved.
Diagnostics
If the above checks & actions did not resolve the issue or do not apply to your print, the following diagnostics may further inform what is causing the issue.

Print Preparation or Part Design Adjustments
The following solutions will address print or part-related causes of the defects. Choose among the suggested actions below and select the best approach for your application. Usually only one type of adjustment is needed.
If problems persist, please reach out to Carbon Support.
Explanation & Causes
Explanation
Resin starvation can occur during a print if:
- Not enough resin was dispensed.
- The printer is not level, most noticeable with an L1 printer.
- Features in the geometry prevent a large volume of resin from draining, such as unvented volumes. This can also lead to localized areas of starvation from restricted resin flow, as opposed to a lack of enough resin in the cassette.
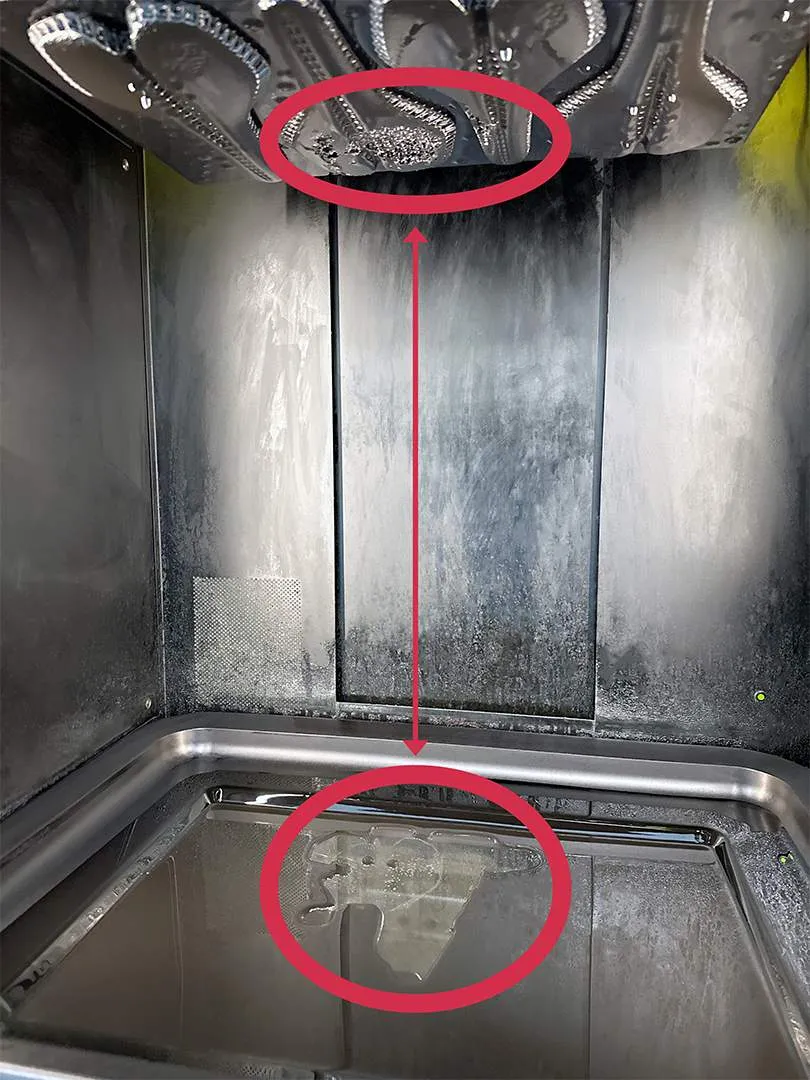
Causes
Print Preparation or Part Design
How the part is oriented, supported, or designed is causing the defect.

Root Issue | Problem | Why Defect Presents |
|---|---|---|
Part Geometry | Resin is not draining from part features. | Certain geometries, such as manifolds, can trap resin during printing if the part is not oriented or designed to drain the resin. |
Part Geometry | Straw effect | Holes in the part geometry can pull in resin during the pump up stage from suction forces. |
Unvented Volume | Resin trapped in unvented volume. | Resin cannot drain from an unvented volume because the pressure differential holds the resin inside the enclosed volume. |
Hardware
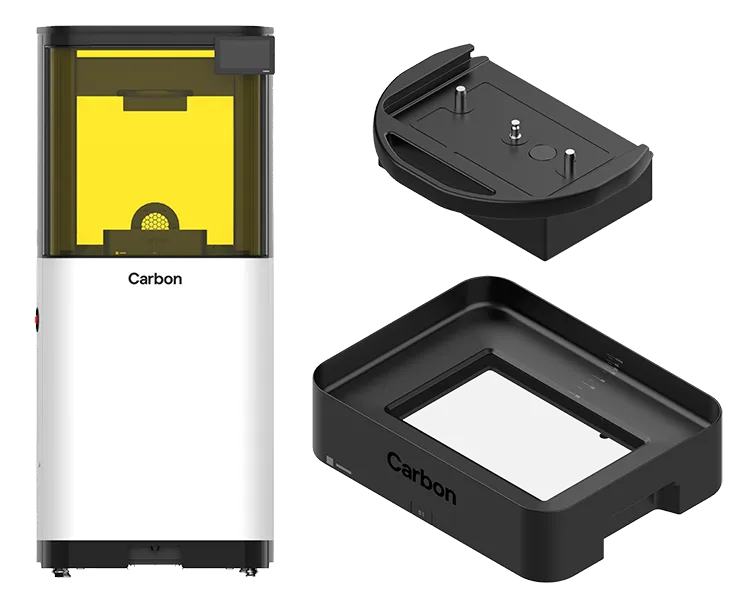
The printer, cassette, or platform is dirty or requires maintenance to resolve the defect.
Occasionally, a defect may indicate the printer requires servicing by a Carbon engineer.
Root Issue | Problem | Why Defect Presents |
|---|---|---|
Leveling | Resin level is too low in one area of cassette | If the printer is not level, the resin may not cover the window if it's pooling on one side or area of the cassette. |
Resin
The printing material is expired, beyond the printing range in its pot-life, or has been improperly mixed, causing abnormalities in the print.
Root Issue | Problem | Why Defect Presents |
|---|---|---|
Dispensing | Not enough resin was dispensed | The recommended resin volume is meant to cover the window fully during printing in addition to providing the material for the part & support volume. |
Print Plan Adjustments
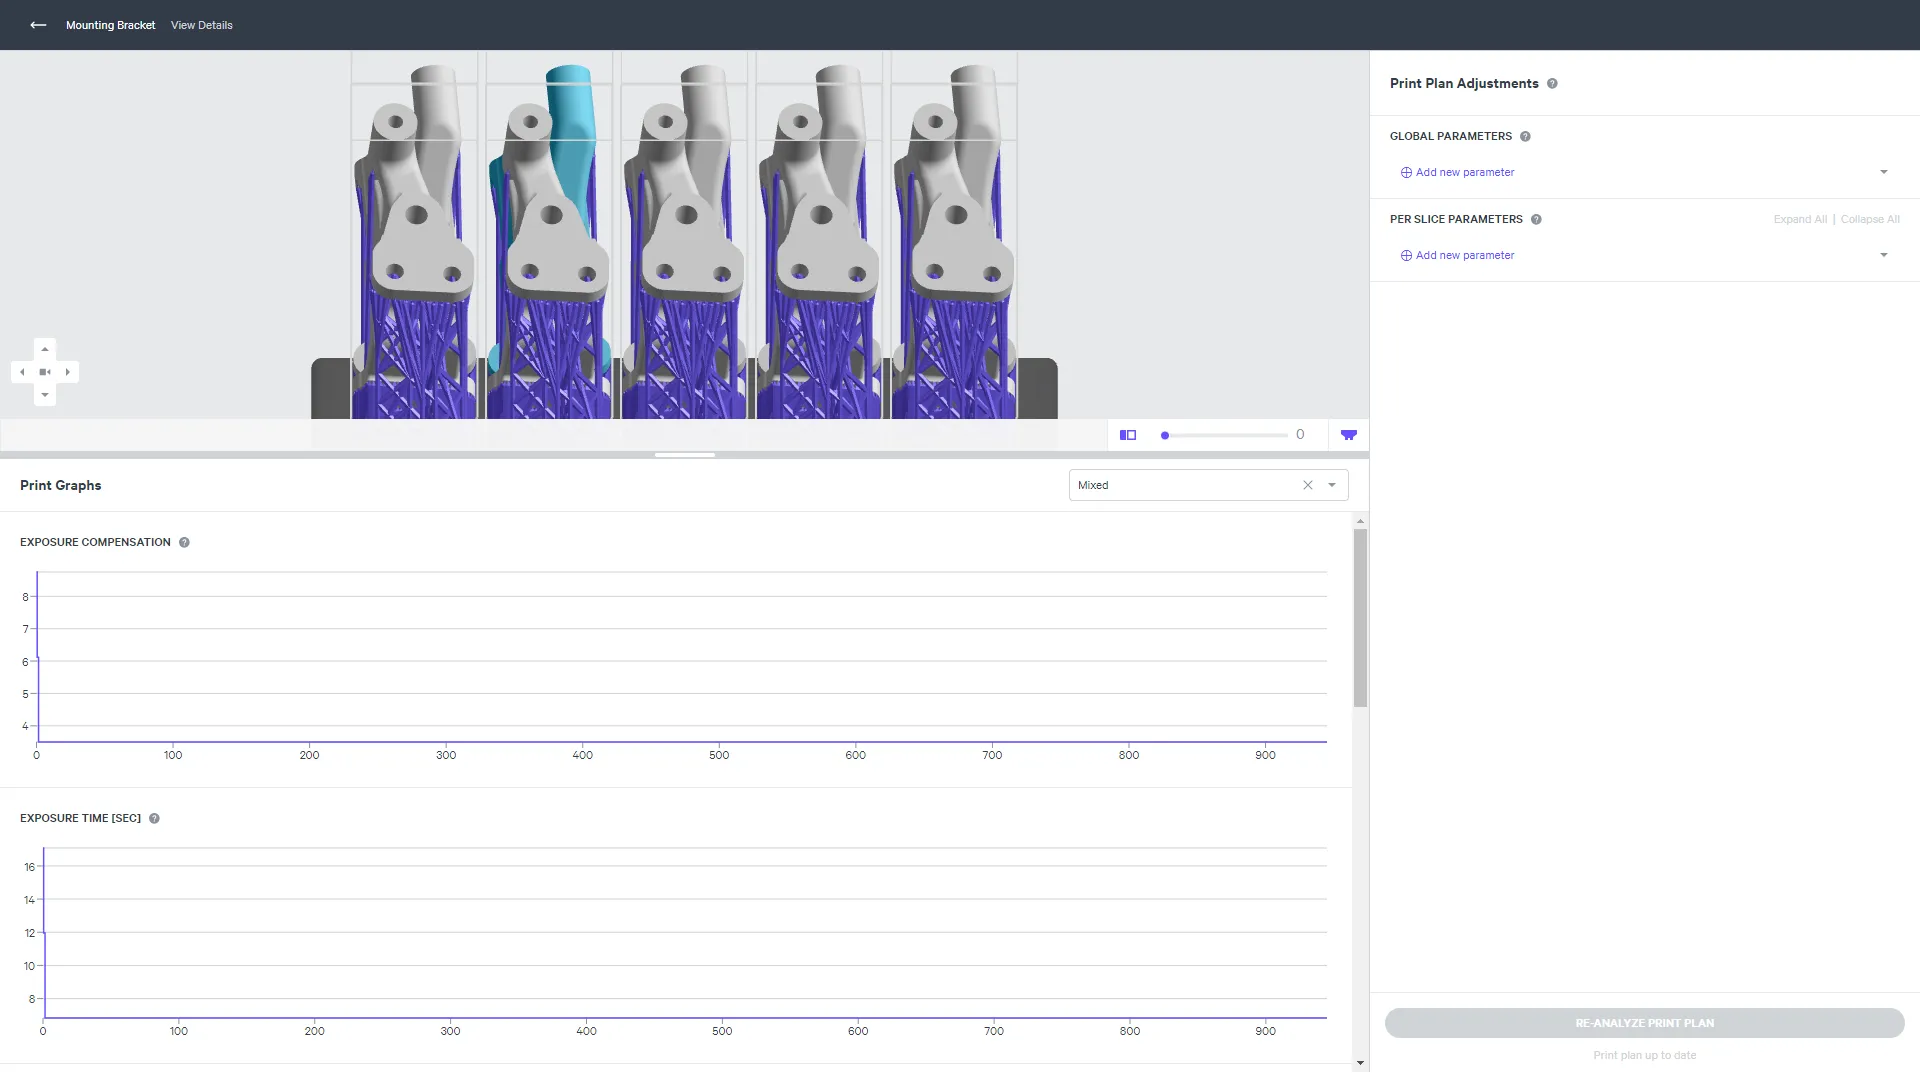
Print Plan Adjustments adjust the print plan to optimize mid to high volume production and/or address part defects.
In doing so, adjustment may both prevent or cause defects. Below are adjustments that can cause this defect.
Printing Stage | Parameter Type | Type of Adjustment | Why Defect Presents |
|---|---|---|---|
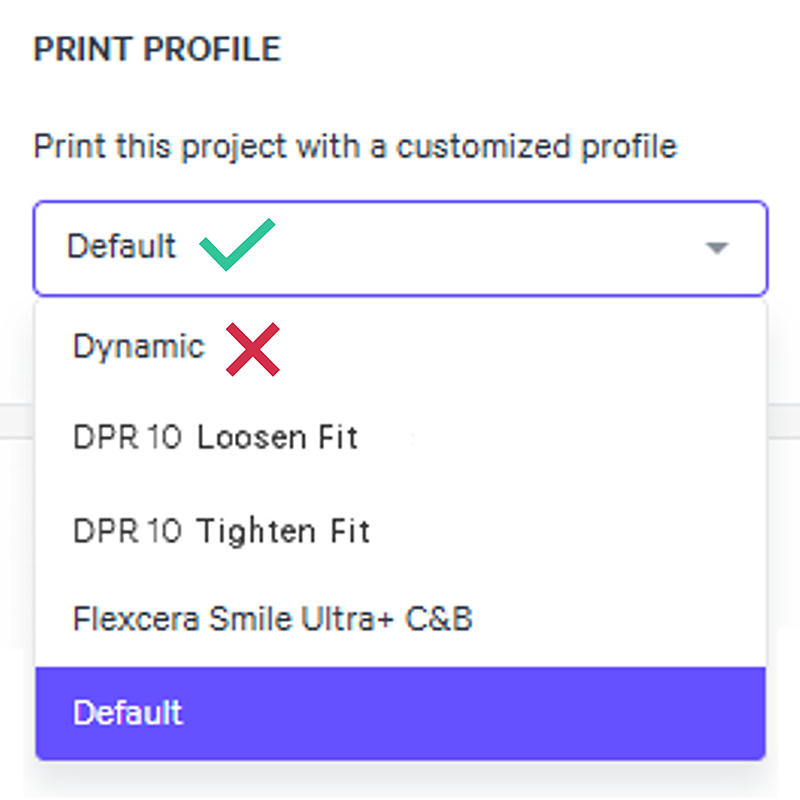
1 Pump Up | Pump Height | Decrease | A decrease in the pump height can limit how much resin can flow out of part geometries that hold resin. |
2 Settle Up | Delay Timing | Decrease | A shortened settle up stage limits the amount of time resin can flow out of part geometries that hold resin. |