Witness Line
Witness lines
Changes in resin flow dynamics cause witness lines.

How to Identify
Witness lines can be diagnosed as follows:
- Thin lines on part surface.
- Lines appear horizontal (parallel to the build platform).
- Lines appear on all sides of the part.
- Visual artifacts that can be seen but not felt by hand.
Cause - Inconclusive
Cause -
Sudden change in print speed via Print Plan Adjustments
Cause -
Sudden change in print speed via Print Plan Adjustments
Cause -
Sudden change in print speed via Print Plan Adjustments
Troubleshooting
It is recommended that you review all the possible solutions before taking action to ensure you are pursuing the best course of action.
If the best course of action is not apparent, try the troubleshooting options in the order listed. Refer here for more tips.
Print Preparation or Part Design Adjustments
The following solutions will address print or part-related causes of the defects. Choose among the suggested actions below and select the best approach for your application. Usually only one type of adjustment is needed.
- Tilt parts at an angle.
- Keep multiples of the same part in the same orientation.

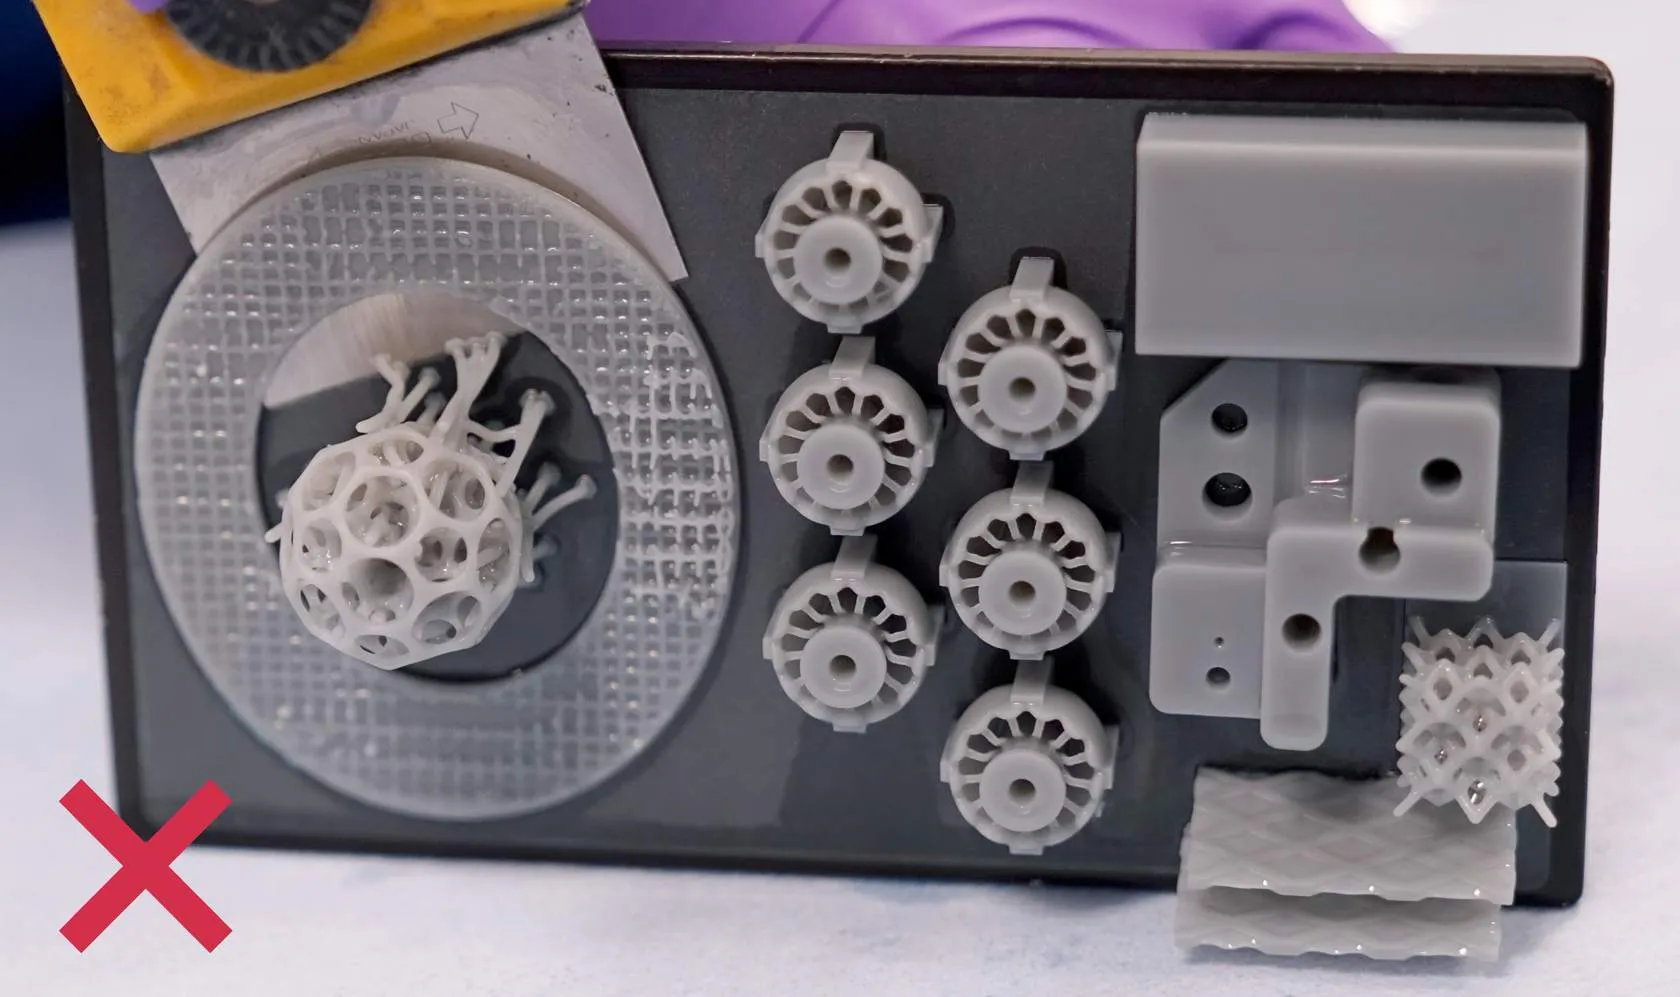
If problems persist, please reach out to Carbon Support.
Explanation & Causes
Explanation
Changes in resin flow dynamics affect the speed and direction of resin flow, which can cause subtle changes on the surface finish of the part. The primary conditions where this can occur:
- Flow changes caused by different part configurations:
- Printing different part geometries simultaneously.
- Or printing the same part in multiple orientations.
- Platform moving above the surface of resin in the cassette.
- A sudden change in the print plan.
Different Part Configurations
As these part of varying height finish printing, a new resin flow condition is created.
Platform Position
Early in the build, the platform is immersed in the resin, which has a large influence on the dynamics of resin flow. Later in the build, the platform exits the resin and only the parts themselves influence resin flow, which is less turbulent than than the platform.
Print Plan Sudden Change
When the print plan suddenly changes in speed or platform movement, the resin flow also changes suddenly.
Causes
Print Preparation or Part Design
How the part is oriented, supported, or designed is causing the defect.

Root Issue | Problem | Why Defect Presents |
Orientation | Change in cross section is parallel to platform | When a cross section changes suddenly from one slice to the next, the dynamics of resin flow also change suddenly. Tilting parts at an angle so cross section changes gradually can mitigate the issue. |
Parts are in different orientations | Keeping all parts at the same orientation keeps flow conditions consistent. | |
Layout | Different geometries on one build. | Different part geometries will change the resin flow dynamics as different parts finish printing. This can be an efficient way to test different part geometries to save resin and printing time, but is it not an advised production solution. |
Print Plan Adjustments
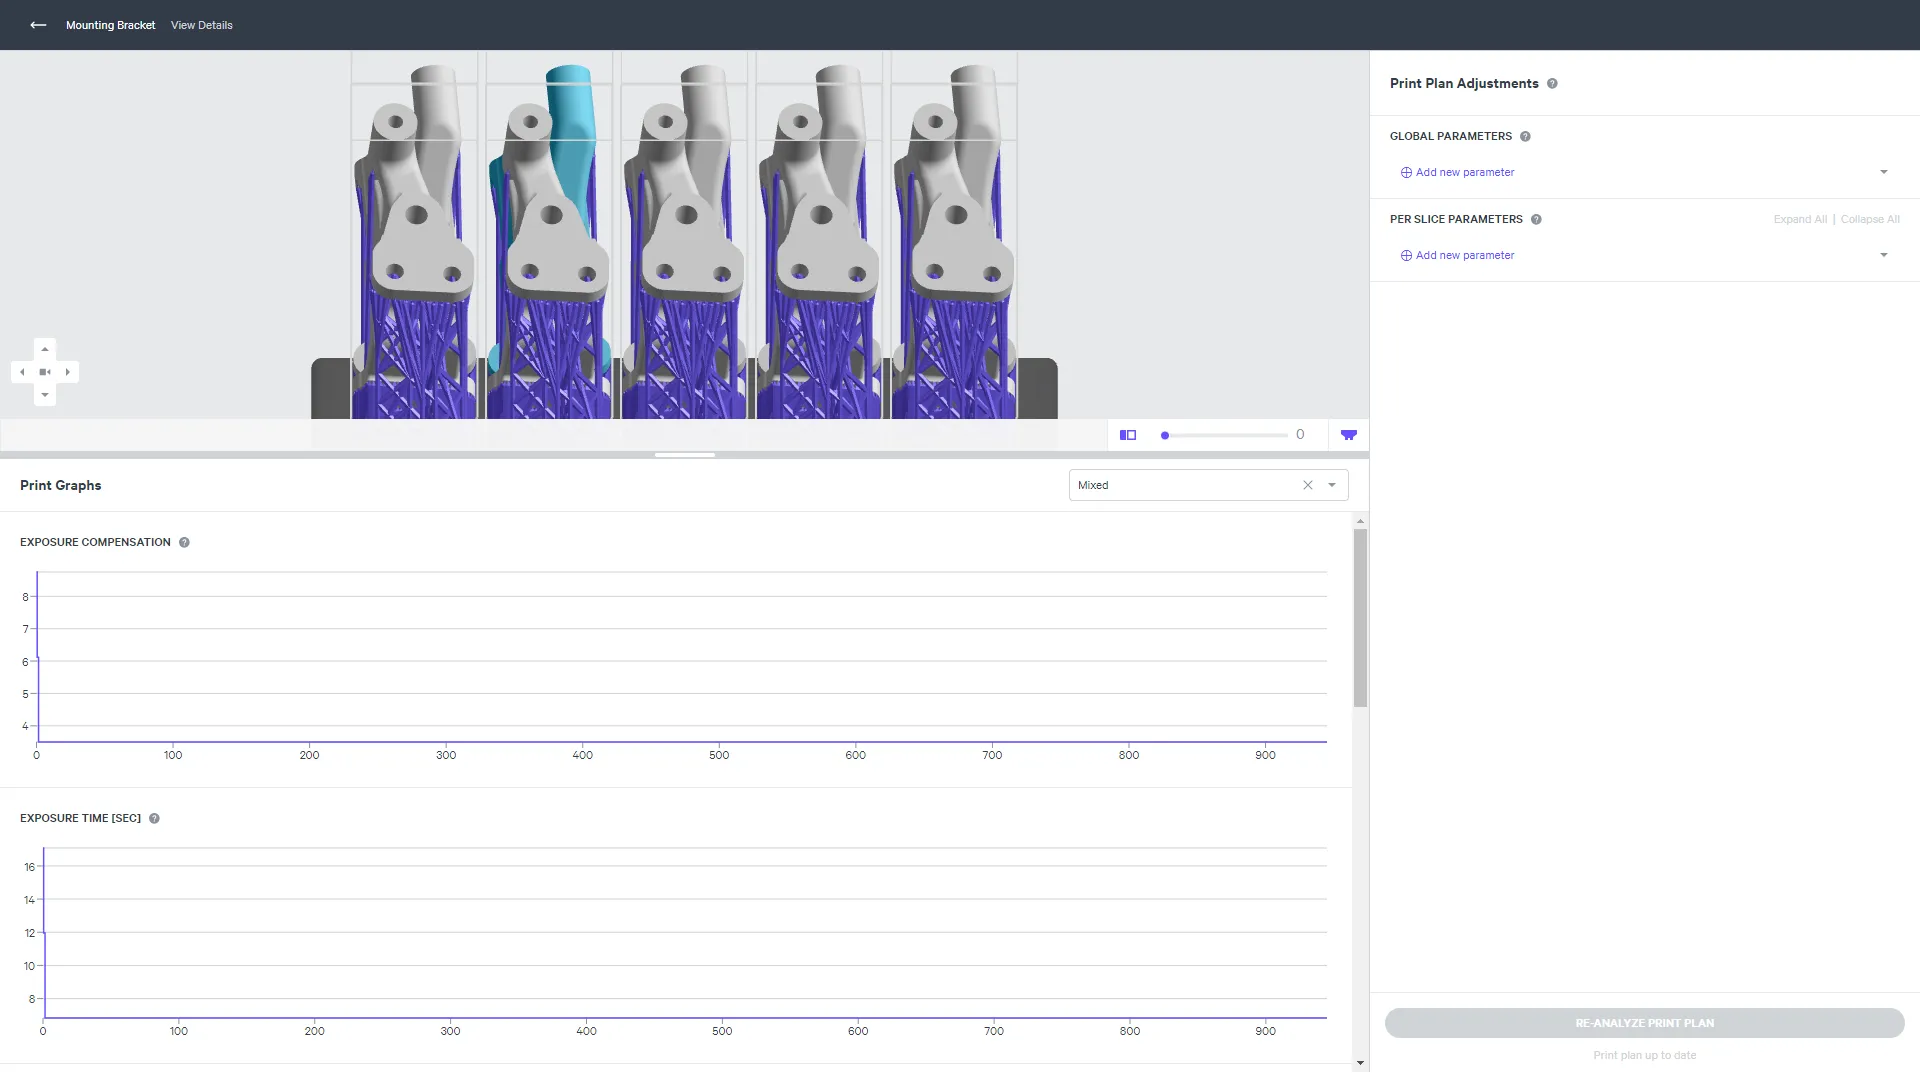
Print Plan Adjustments adjust the print plan to optimize mid to high volume production and/or address part defects.
In doing so, adjustment may both prevent or cause defects. Below are adjustments that can cause this defect.
Printing Stage | Parameter Type | Type of Adjustment | Why Defect Presents |
1 Pump Up 2 Settle Up 3 Pump Down 4 Settle Down | Any | Sudden increase or decrease | Sudden changes in flow dynamics can follow any sudden change in speed or platform movement. |
3 Pump Down | Platform Speed | Increase | A quick pump down speed can cause more disturbance in resin flow. |
4 Settle Down | Delay Timing | Decrease | Less time for the settle down stage means resin has not had enough time to recover from changes in flow dynamics. |