Cracking - Medial Axis
Cracking - Medial Axis
Cracks/fissures form along the medial axis flow lines.
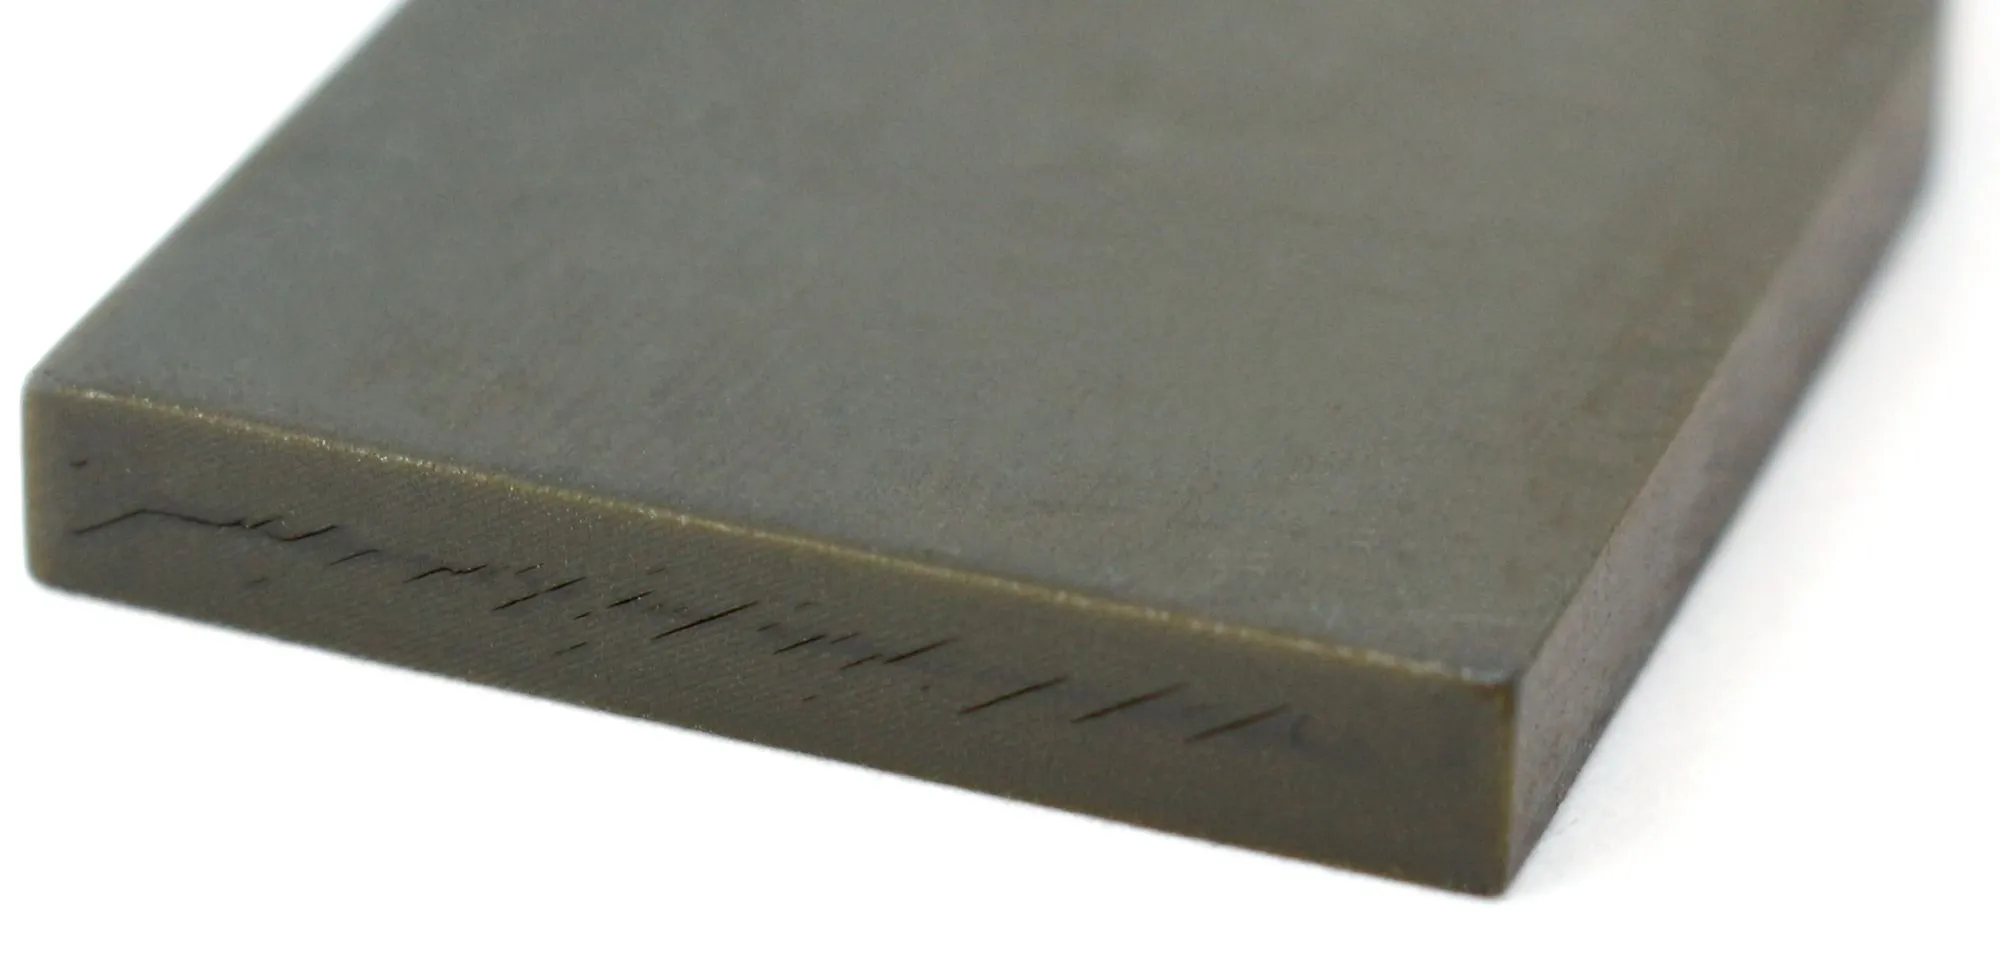
How to Identify
Medial axis cracking can be diagnosed as follows:
- Cracks appear as thin, dark lines running along medial axis flow lines.
- Medial axis flow lines occur on surfaces parallel to the platform, facing the window.
- Lines appear after baking. Parts look fine off of the printer and after washing.
Medial axis cracking is differentiated by other types of cracking by where it occurs on the part. This is an orientation-based form of cracking that occurs solely along medial axis lines on flat surfaces facing the window. Reference Cracking - Bulk and Cracking - Excessive Solvent for other types of cracking.
Cause - Inconclusive
Cause - Inconclusive
Cause - Inconclusive
Troubleshooting
It is recommended that you review all the possible solutions before taking action to ensure you are pursuing the best course of action.
If the best course of action is not apparent, try the troubleshooting options in the order listed. Refer here for more tips.
Process, Material, and Hardware Checks
If any of these conditions apply to your print, take the corrective action and reprint to see if the problem is resolved.
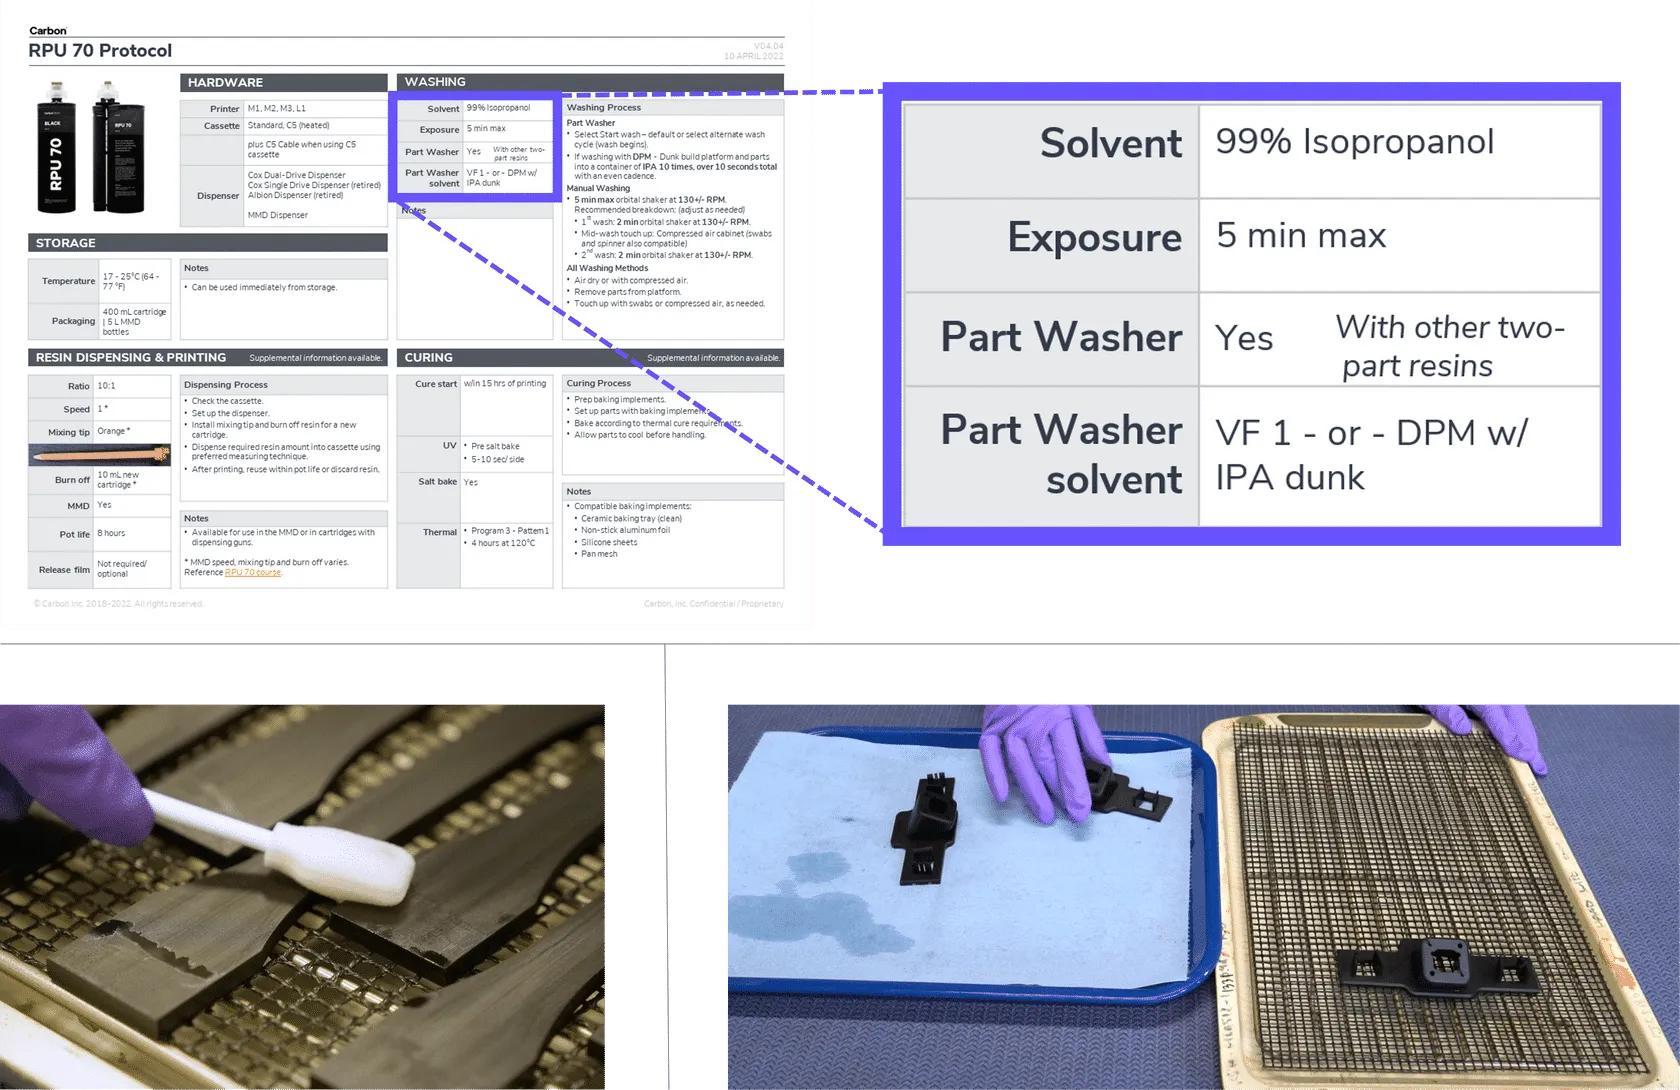

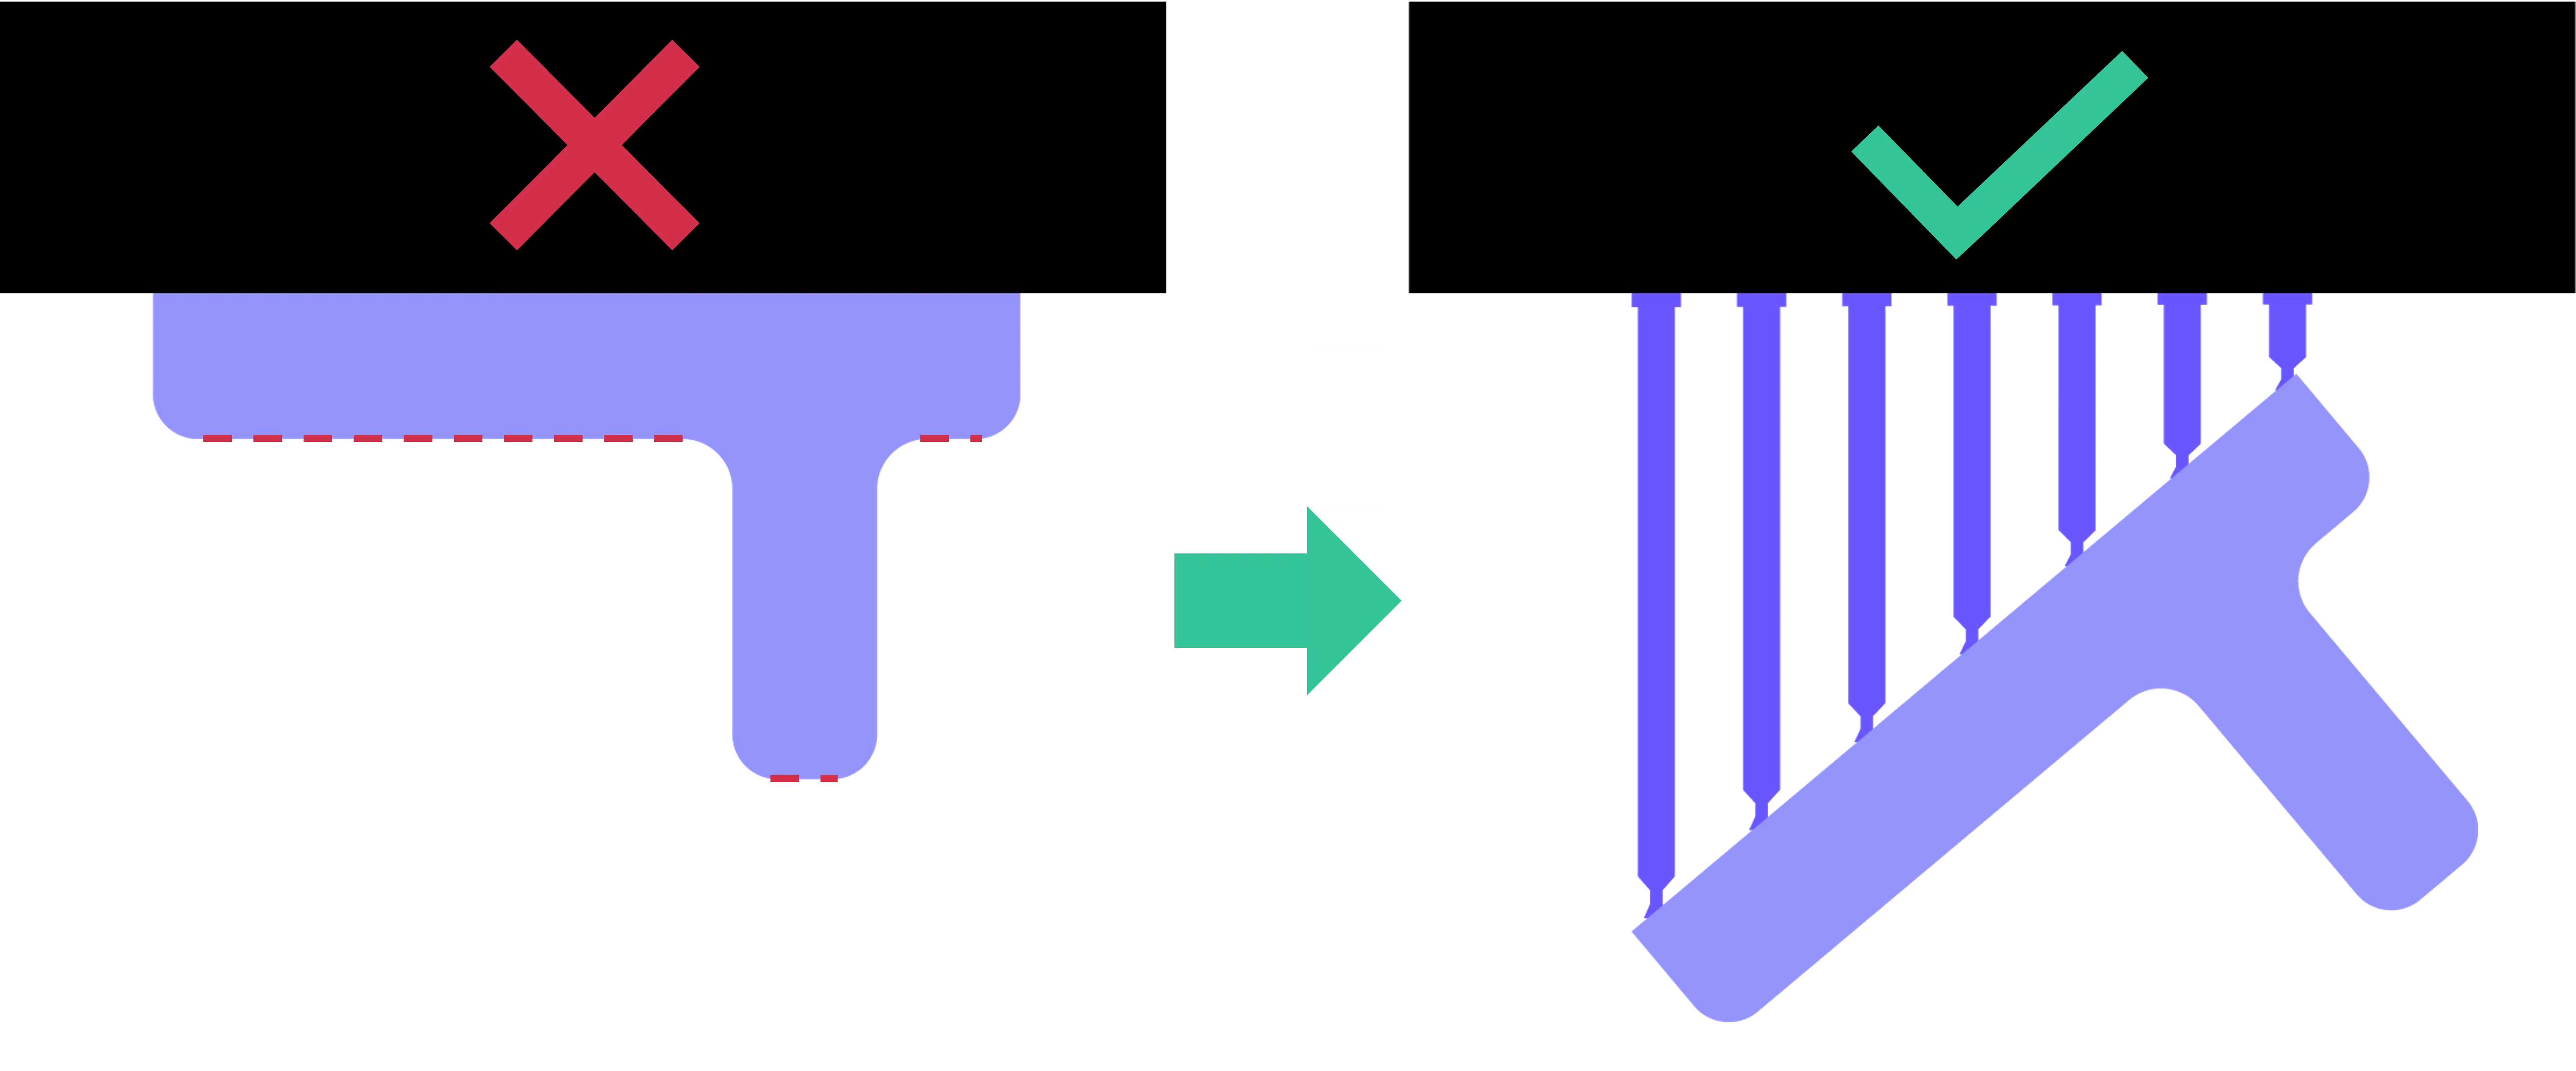
Print Preparation or Part Design Adjustments
The following solutions will address print or part-related causes of the defects. Choose among the suggested actions below and select the best approach for your application. Usually only one type of adjustment is needed.
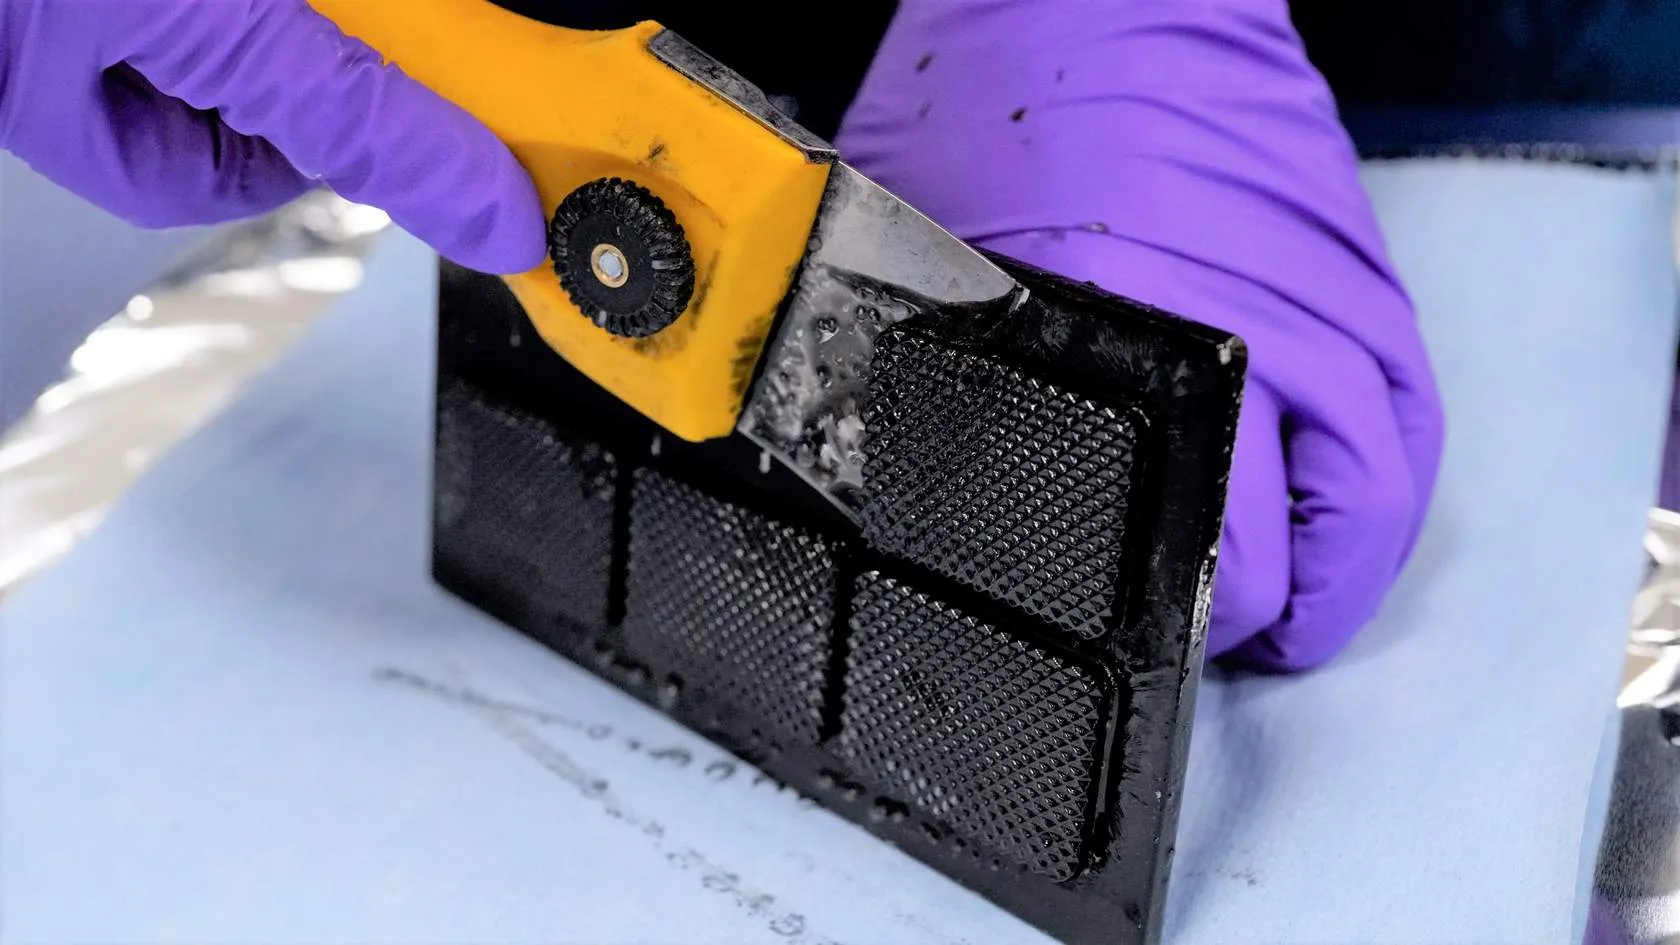
If problems persist, please reach out to Carbon Support.
Explanation & Causes
Explanation
Medial axis cracking occurs along the medial axis flow lines on surfaces parallel to and facing the window. Resin flows in from all sides of a part, and where those varying flow directions meet is the medial axis flow lines. These lines act as weak points in the material where stress during the chemical changes of baking can cause cracks.
The most susceptible conditions of medial axis cracking are:
- Large surfaces parallel to and facing the window
- Excessive solvent exposure
- Brittle resins: CE and EPX

Causes
Post-Processing
How the part is handled in post-processing is causing the defect.
Root Issue | Problem | Why Defect Presents |
|---|---|---|
Washing | Solvent exposure | Too much solvent exposure weakens the material, making stress points weaker. |
Baking | Wrong bake schedule | The most common resins for medial axis cracking are the brittle resins (EPX) that use a ramping program to raise the temperature slowly and prevent thermal shock. |
Print Preparation or Part Design
How the part is oriented, supported, or designed is causing the defect.

Root Issue | Problem | Why Defect Presents |
|---|---|---|
Orientation | Surfaces parallel to and facing the window | Medial axis lines only occur on surfaces parallel to and facing the window. These lines are weak points that can crack under stress. |
Print Plan Adjustments
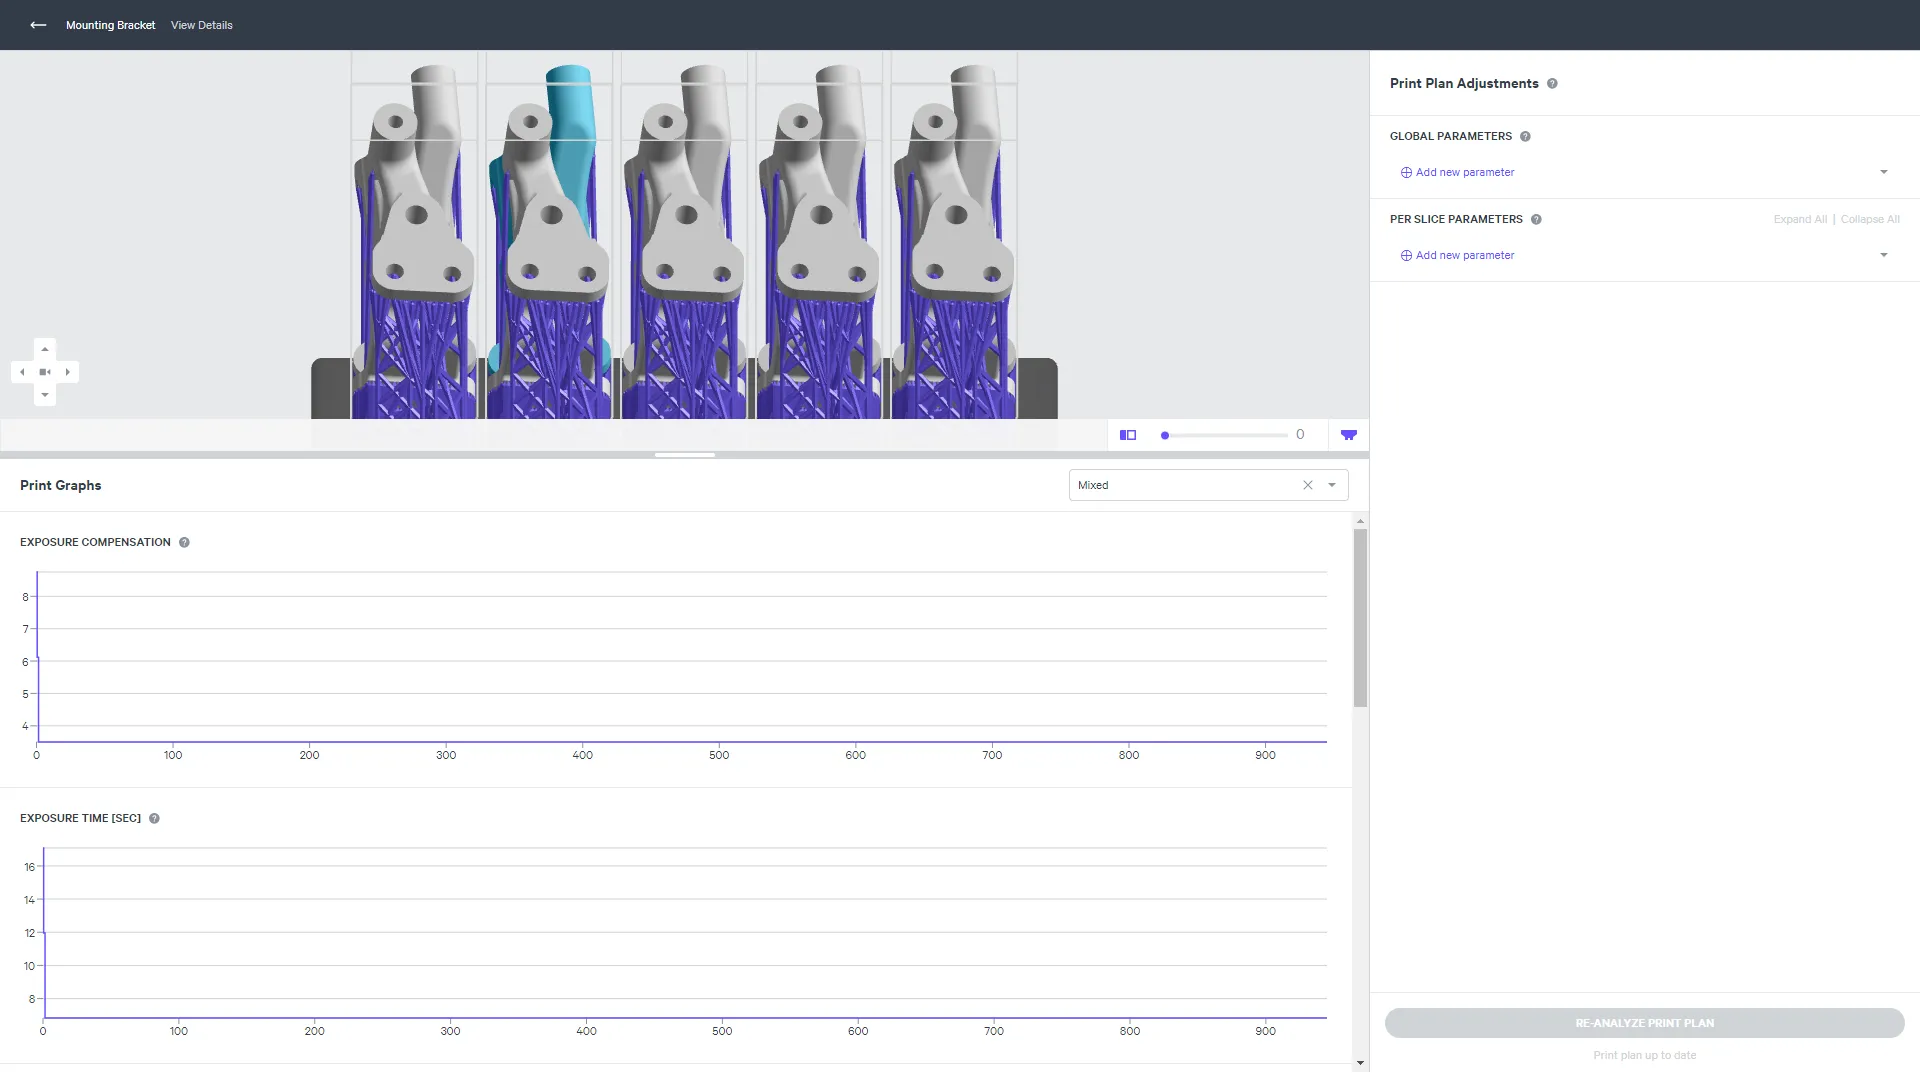
Print Plan Adjustments adjust the print plan to optimize mid to high volume production and/or address part defects.
In doing so, adjustment may both prevent or cause defects. Below are adjustments that can cause this defect.
Printing Stage | Parameter Type | Type of Adjustment | Why Defect Presents |
|---|---|---|---|
1 Pump Up | Pump Height | Decrease | A shorter pump height may not provide enough time for resin to relax into the medial axis flow lines, leaving them weaker as a result. |