Carbon FP3D
September 29 2025 - FDA approval. IFU updated and SDS available.
Overview
FP3D (manufactured by Keystone Industries®) is a two-part resin developed for producing flexible removable partial dentures.
Engineered using Carbon’s proprietary dual-cure chemistry, FP3D sets a new industry standard by delivering a unique combination of durability, stain resistance, dimensional accuracy, and flexibility.

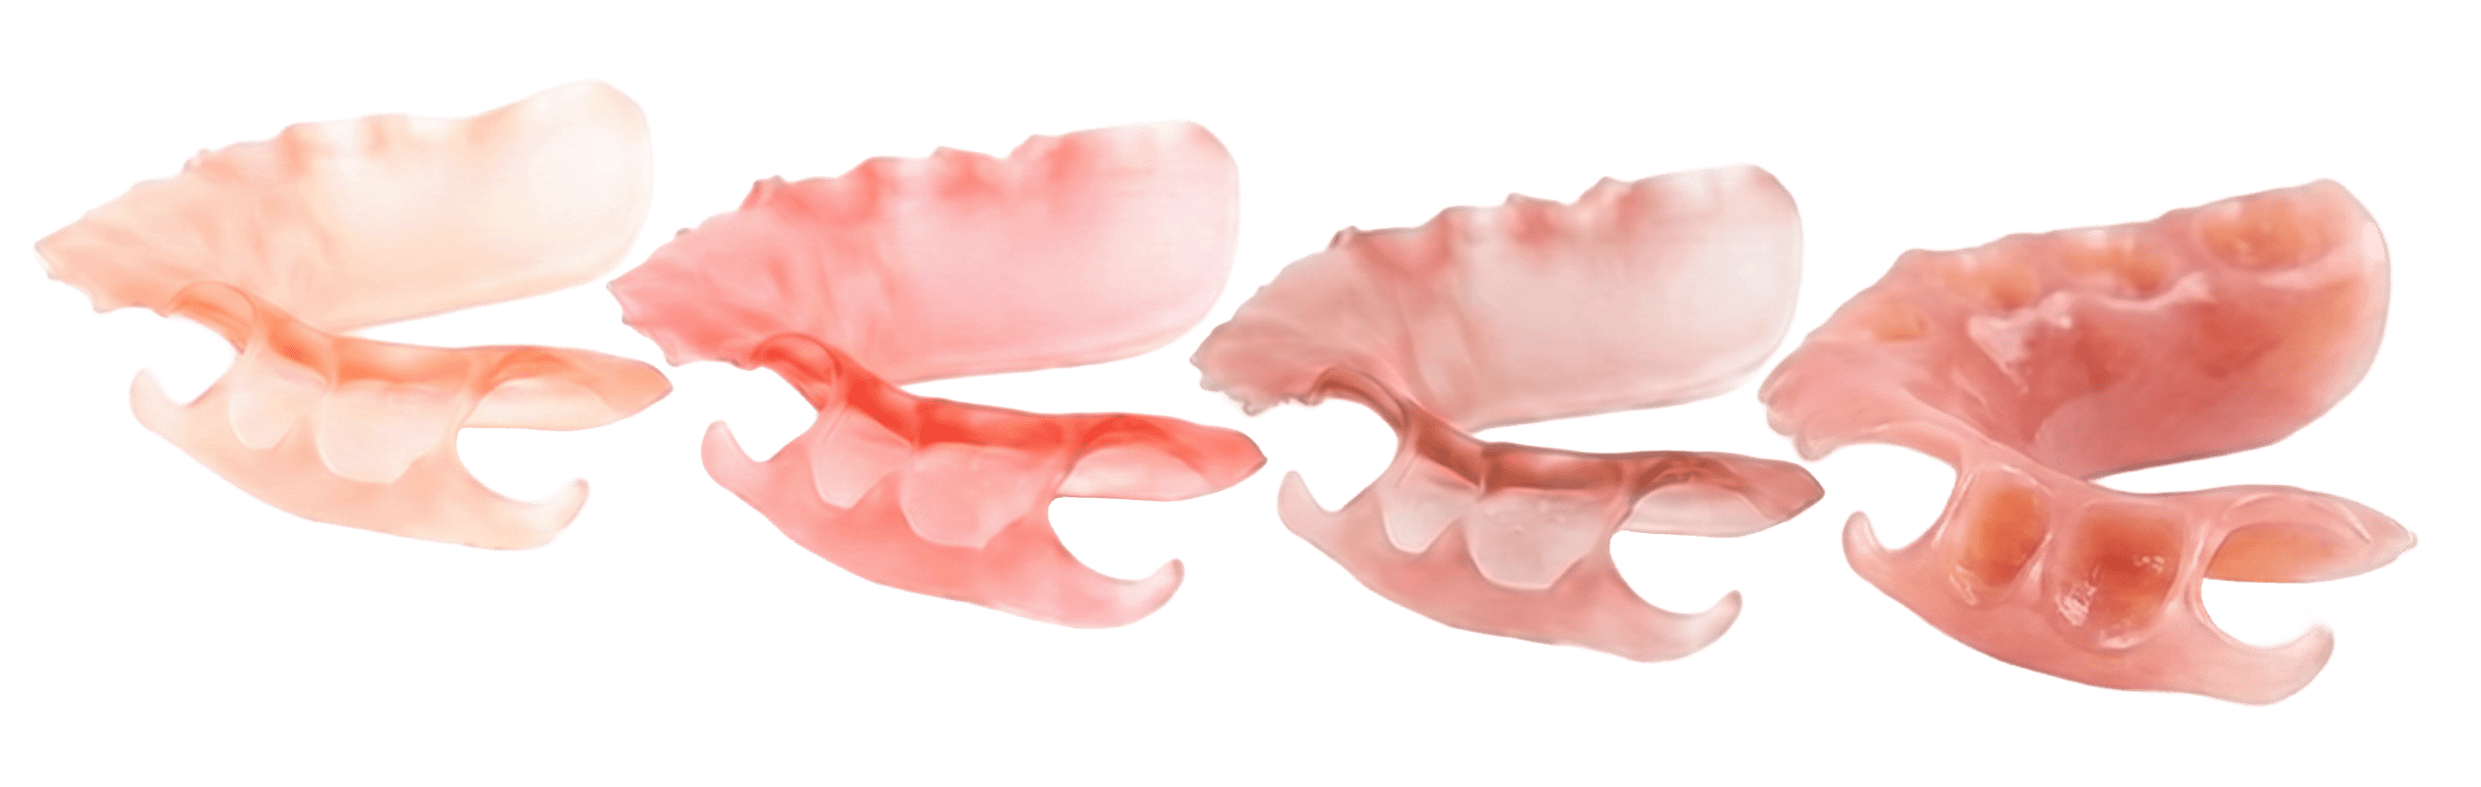
Beyond its material strengths, FP3D easily integrates into Carbon’s digital denture workflow, assisting in reliable, economical, and quick production.
This resin is compatible with the AO Polishing Cassette.
Two-part Resin
Carbon's two-part resins differ from the one-part resins used throughout the dental industry in a few important ways.

- The two components (Part A & Part B) of FP3D are stored in separate chambers in a cartridge, similar to an epoxy you may purchase at a hardware store.
- The components are combined at the time of use by using a battery-powered dispenser and a disposable mixing tip.
- Once combined, FP3D has an 8 hour life span called a pot life. After the resin has aged beyond its pot life, it is not suitable for printing and should be disposed.
- After printing, two-part resins require thermal curing (baking) in a convection oven.
- To preserve clasps and fine features, partials must be packed in salt during the baking process.
- Some salt will stick to parts during baking and must be washed off afterwards.
Required Equipment
Carbon's two-part resins require equipment that will be new to most dental labs.
Cox Dual-Drive Dispenser
A powered dispenser is required to push the resin components out of the cartridge and through a disposable mixing tip.
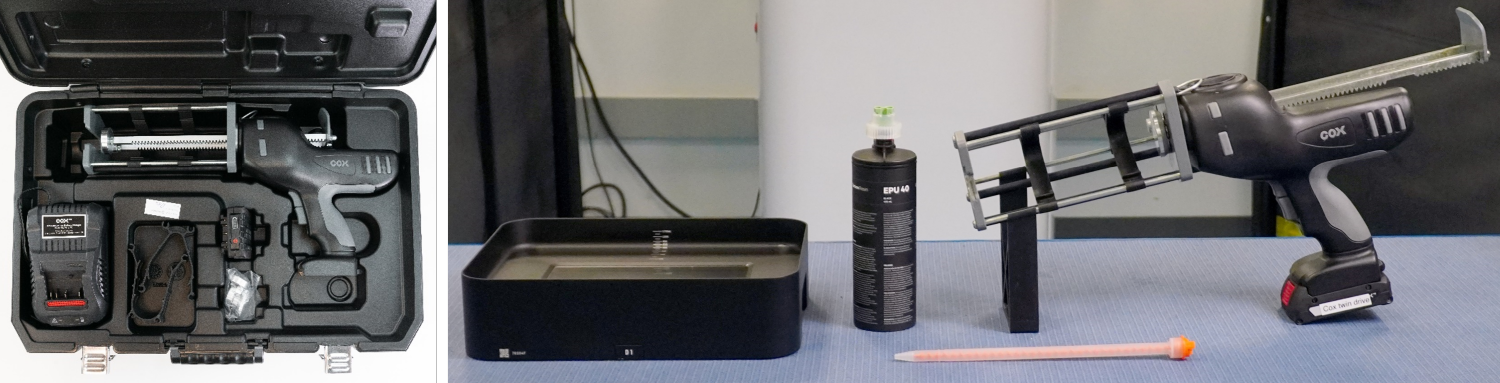
Go to Cartridge Dispensing for more information.
Yamato Convection Oven
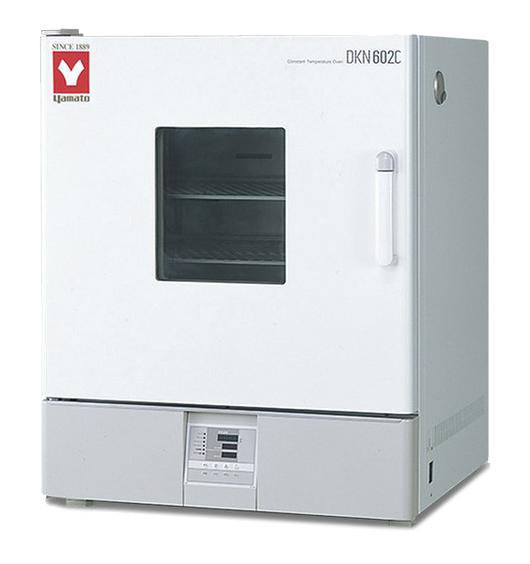
Like all of Carbon's two-part resins, FP3D partial dentures require thermal curing in a convection oven to attain their ultimate mechanical properties.
See Yamato Convection Oven for more information including programming and operating instructions.
The Yamato Convection Oven has ventilation and electrical infrastructure requirements. See the facility requirement checklist for your printer for specific information.
The oven must be ordered from Carbon (PN 101807) because only this model includes the required hardware. This item is available form the Carbon Shop.
Condenser for High-Volume Production
If you will be using approximately 100 liters or more annually, you will need to install a condenser to prevent buildup in the ventilation ducting.
Download the handout below for more information.
Salt Baking Equipment
Salt baking requires a variety of supplies and equipment including
- Powder grain salt - supports parts during thermal curing
- Baking pans - oven-safe pans that hold the salt and parts
- Salt strainer - strains out clumps of salt or other large particulates that can negatively affect part accuracy
- Foil - covers the pan and contains salt during baking
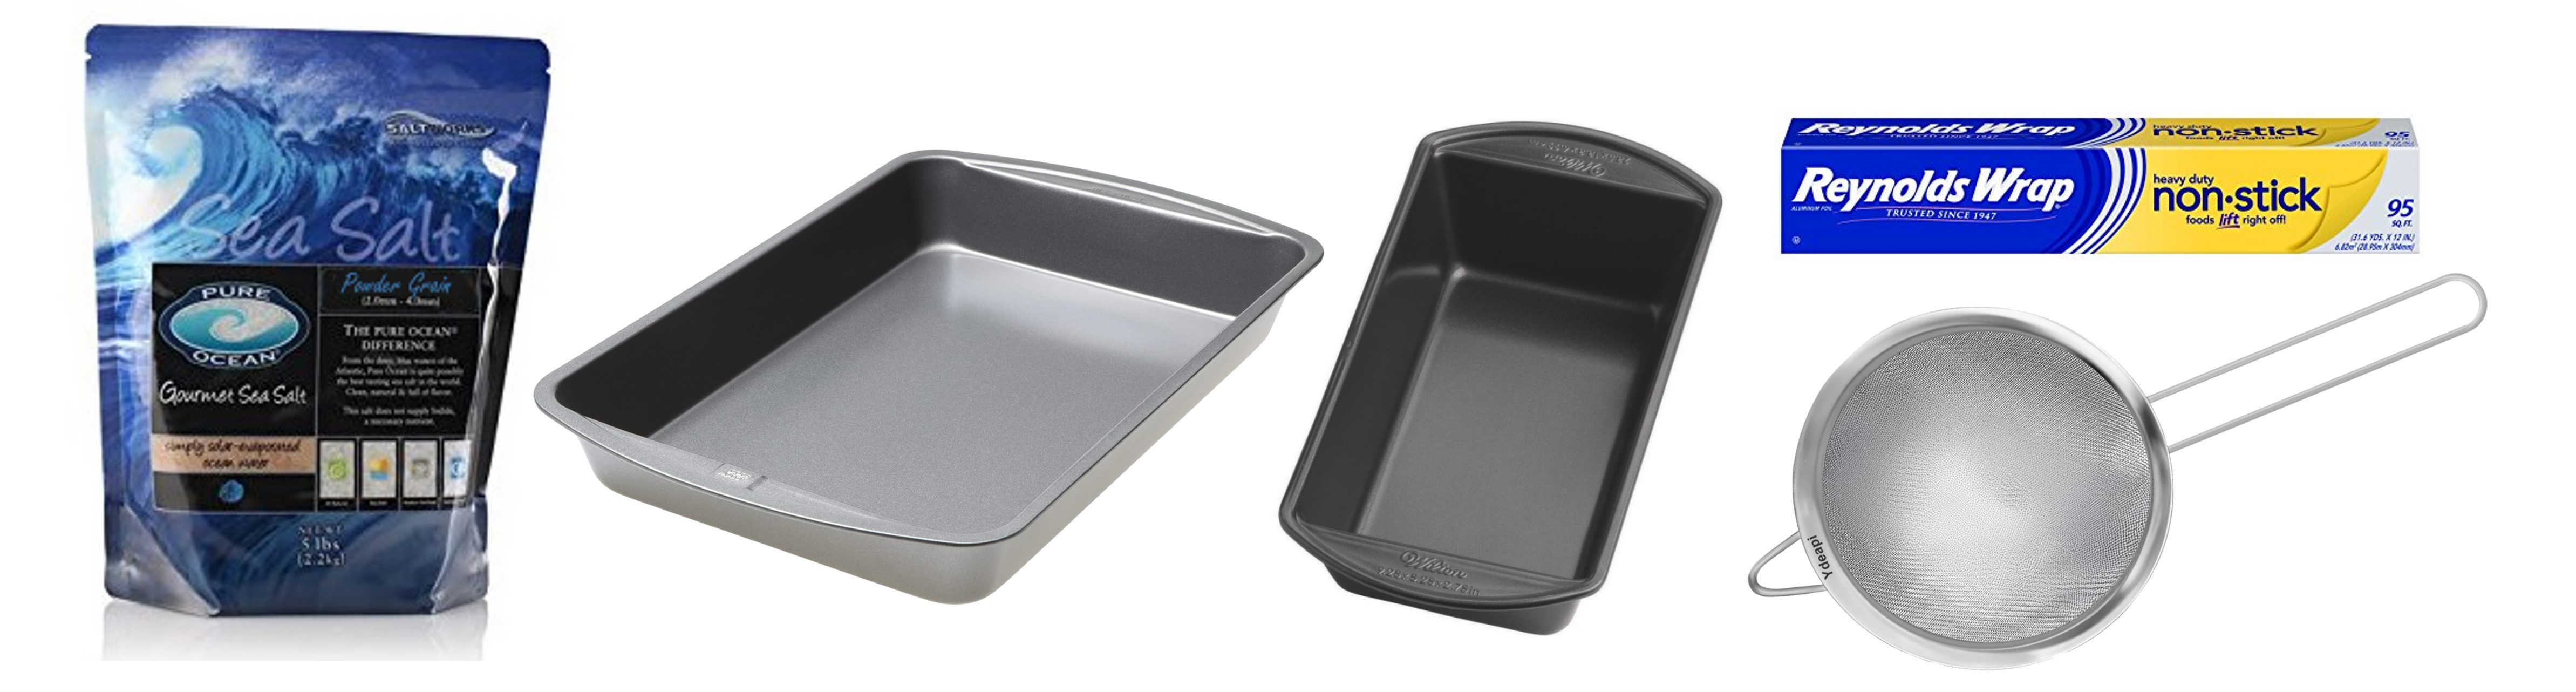
See Salt Baking for more information.
The above items and more are all available on the Accessories & Supplies page.
Resource Links
Promotional Content
Design
Follow these design recommendations for partial dentures to be printed with FP3D.
- Wall thickness should be 1 - 3 mm.
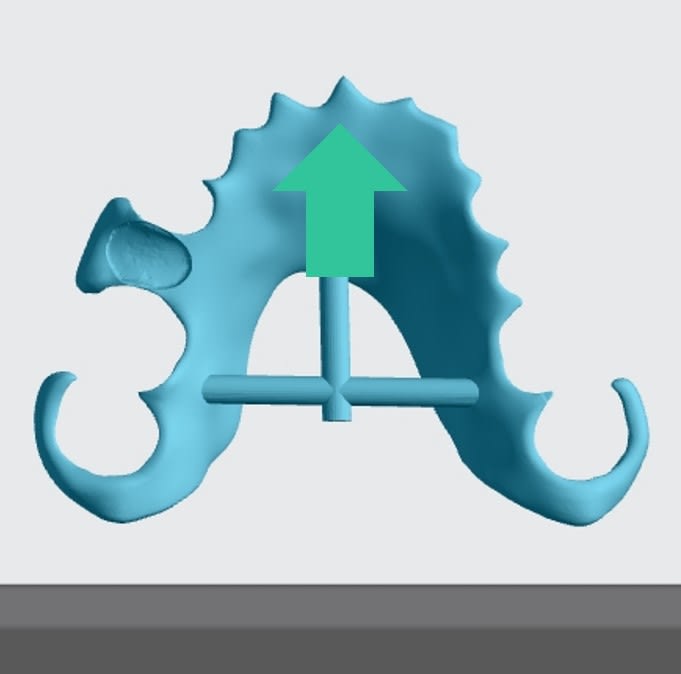
- Incorporate T-bars to prevent splaying of parts during curing.
- Add T-bars to all full arch partial geometries (uppers and lowers) to achieve the best accuracy.
- T-bars should be equivalent to the median thickness of the partial denture.

Digital Preparation
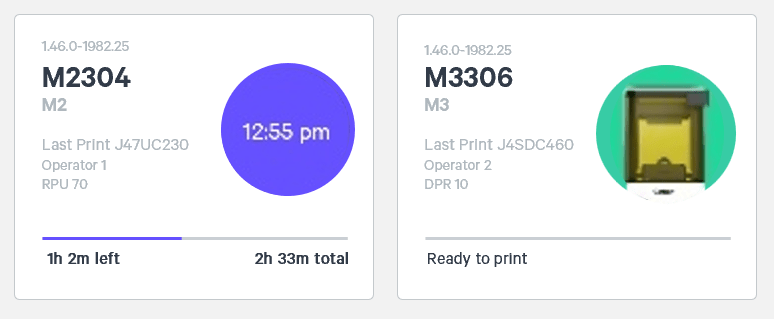
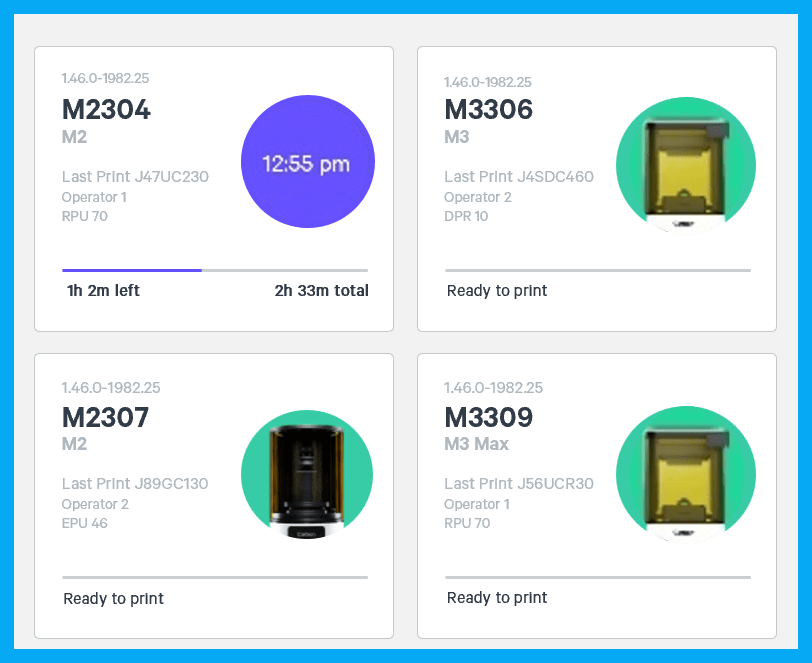
Connect to Printer
Connect to the printer software using your web browser.
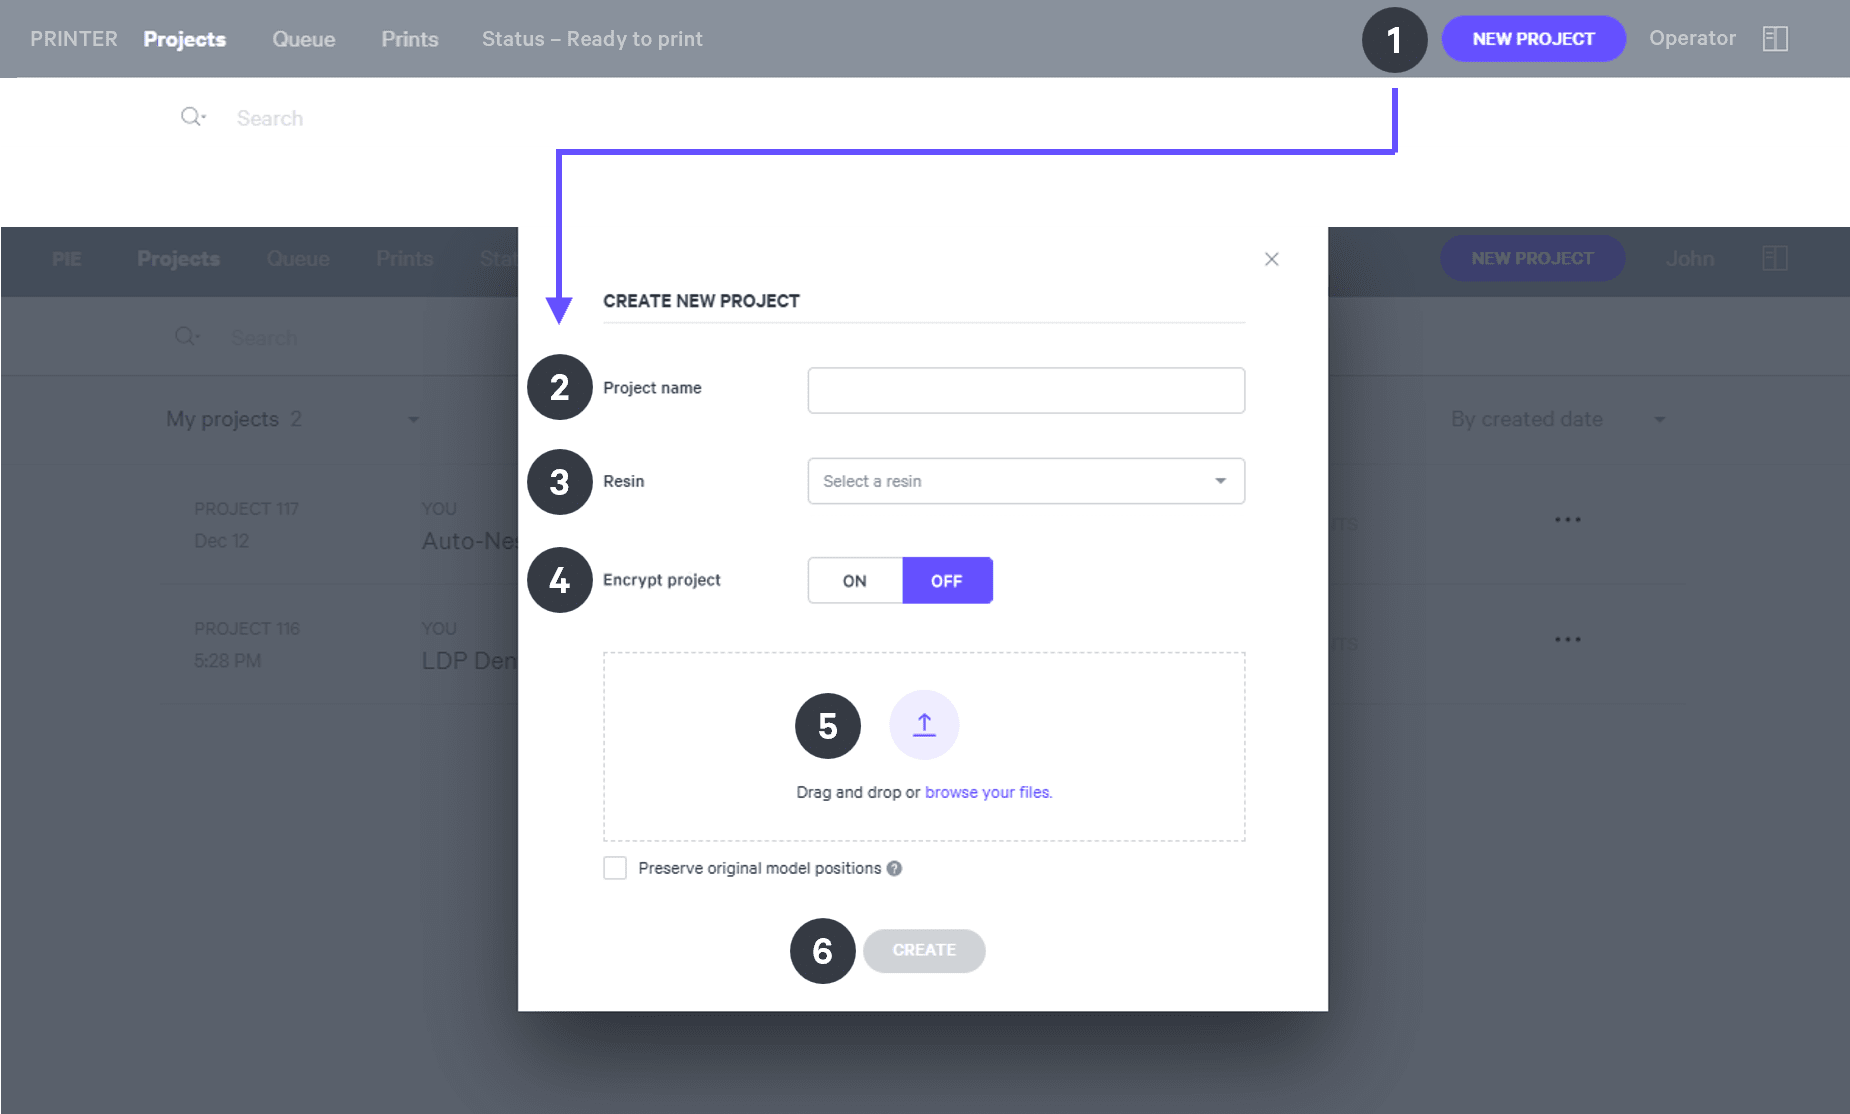
Create Project
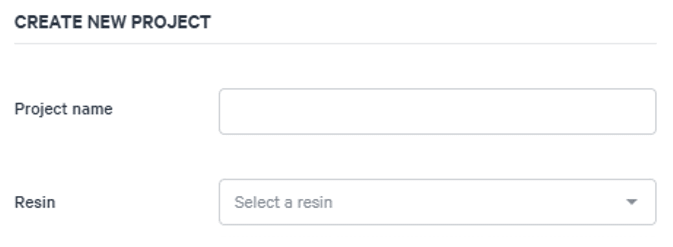
After you have chosen the printer, you must create a new project.
Orientation
For detailed information about orienting parts, read Orient.
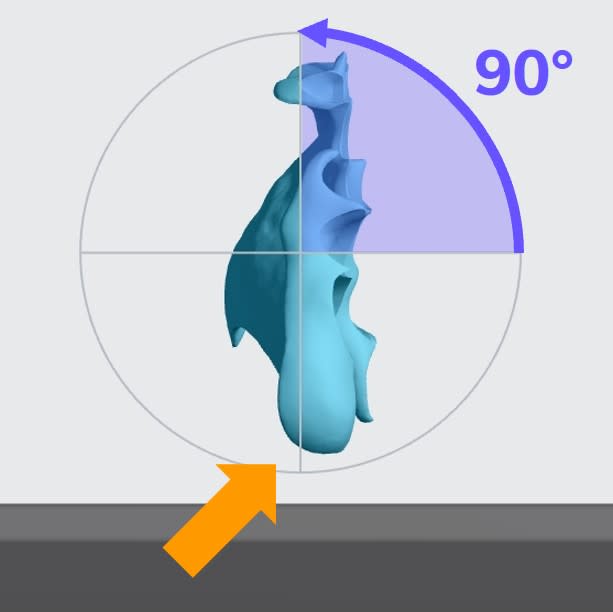
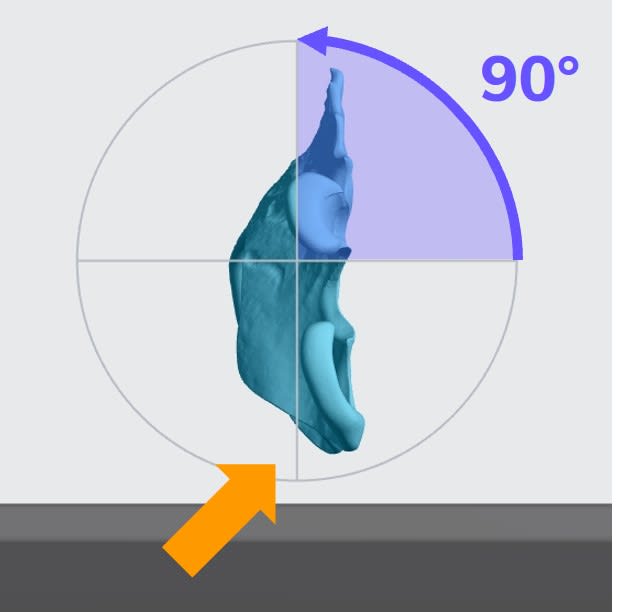
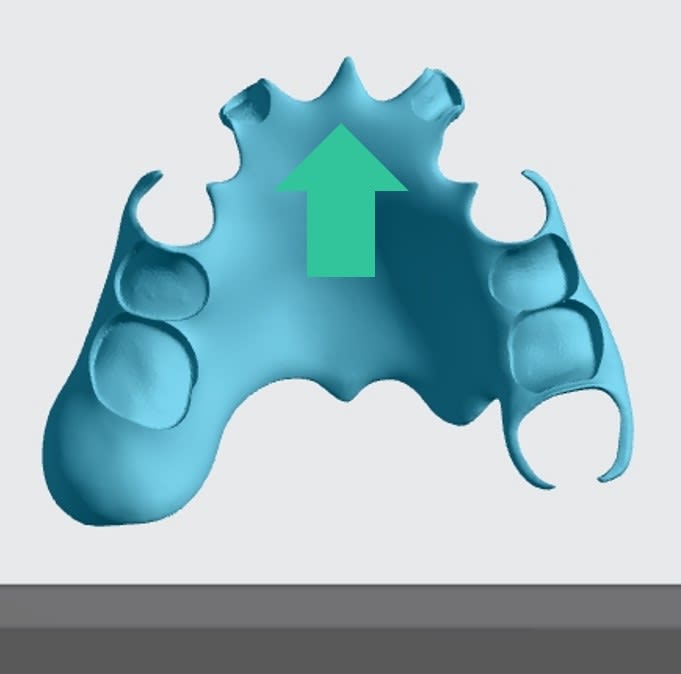
Orient partials vertically with the posterior at the platform (anterior rotated away from the platform).
Upper Partial
Lower Partial
Supporting
See Supports for detailed information.
Select the Supports tab in the top bar or press Shift + S.

In the bottom bar, toggle Overhang Detection on and set the angle to 40 degrees.

Also in the bottom bar, set Toggle Platform to off.
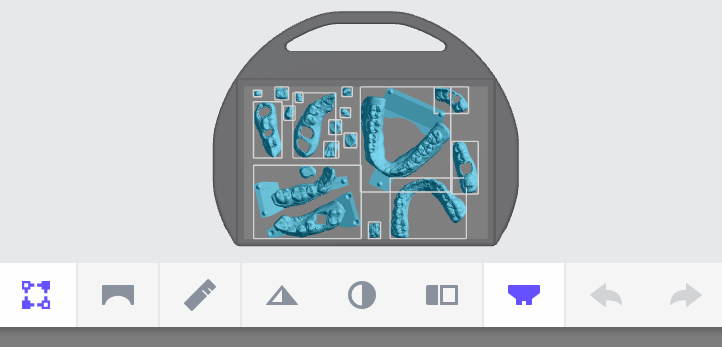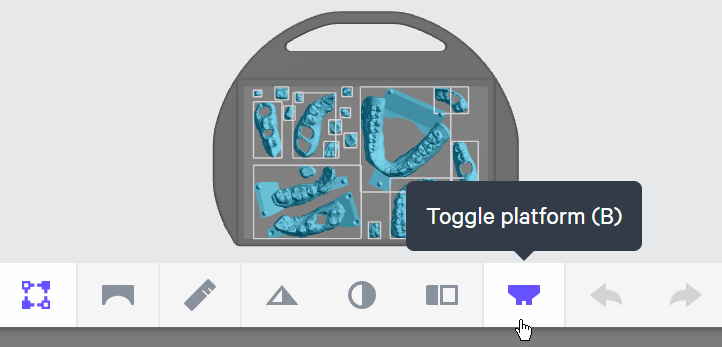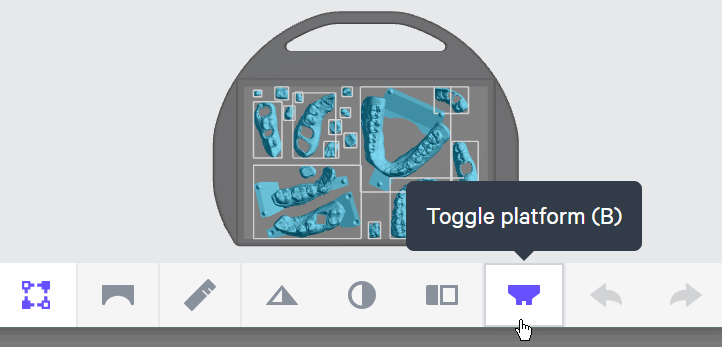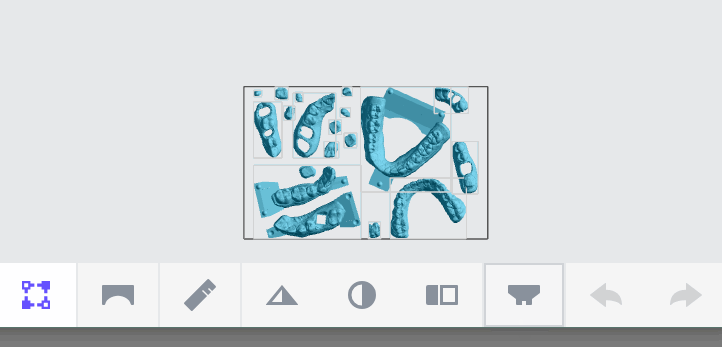
Set Part Position to Above.

Support posterior edges with fences.
- Avoid adding supports to intaglio surfaces.
- Add fences to horizontal T-bars.
- Do not add fences to areas higher than about 30 mm above the platform. These areas require bar supports.
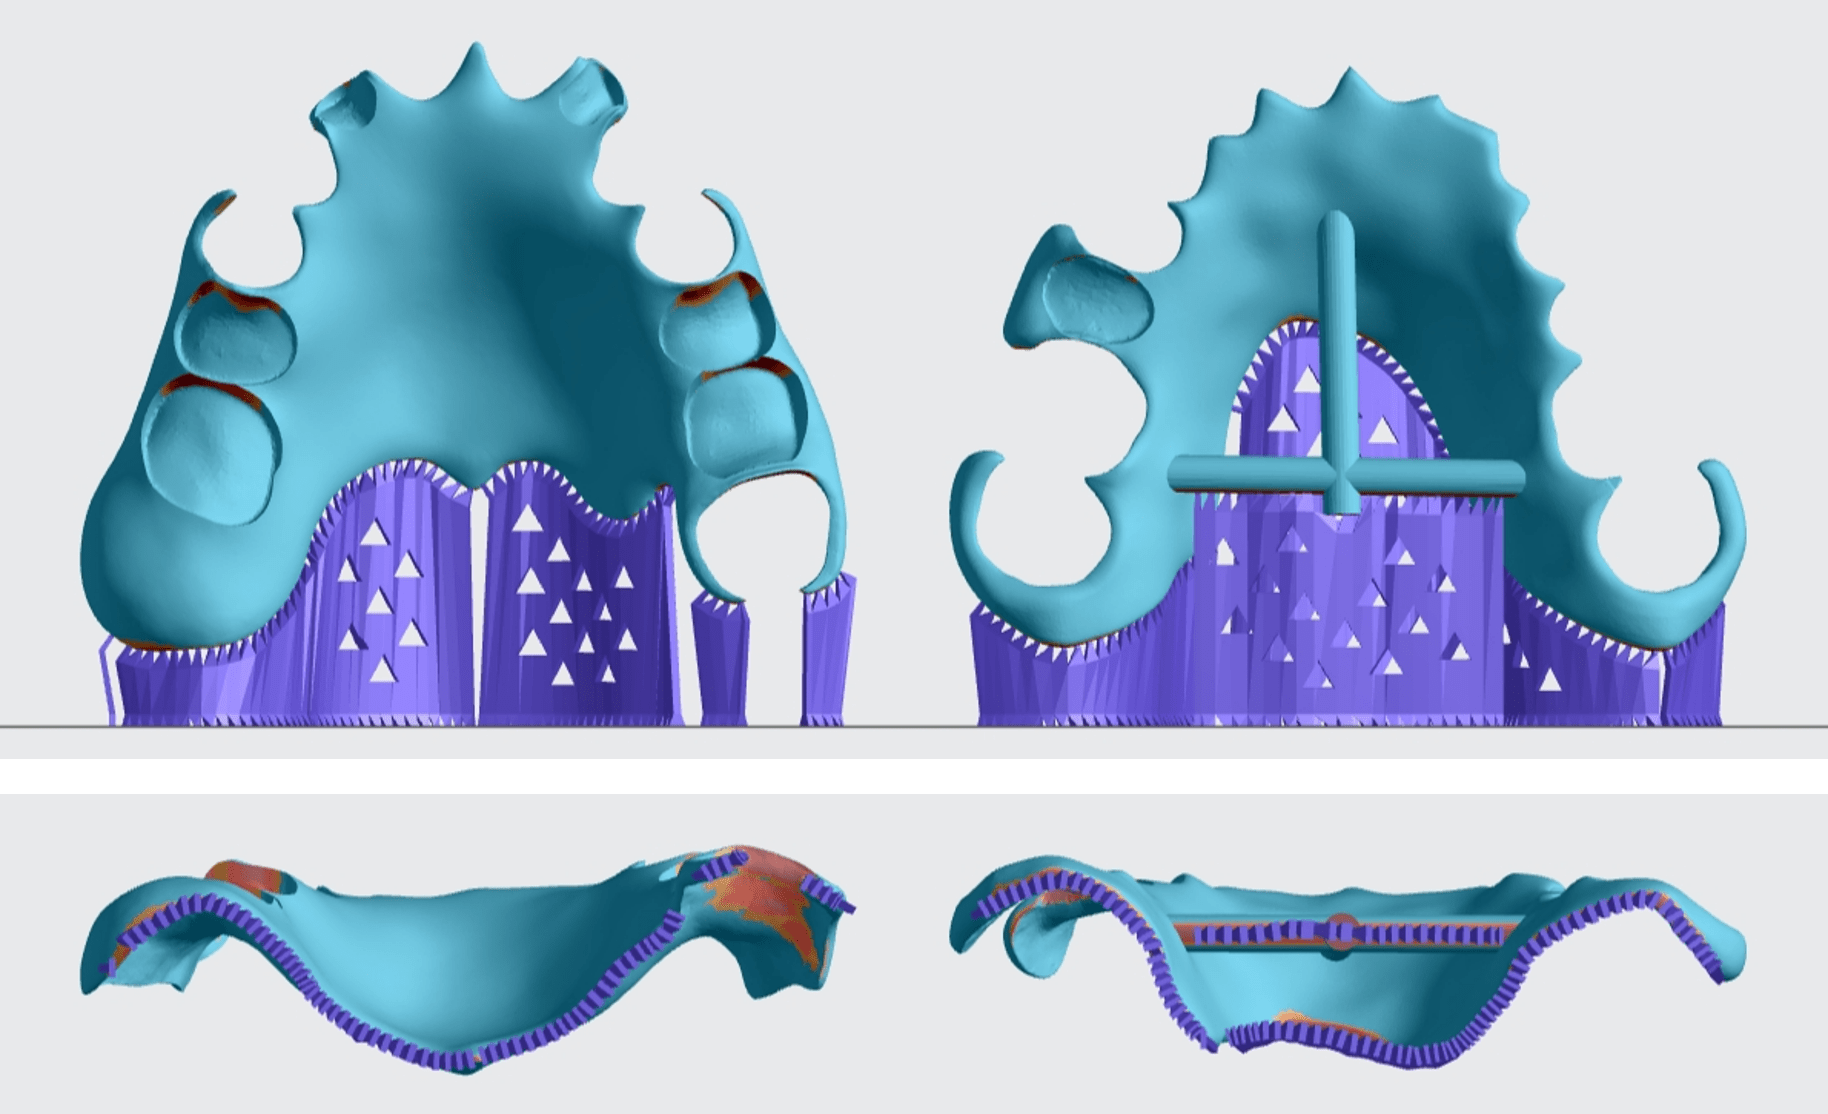
Add bar supports.
- Support overhangs that are more than 30 mm above the platform.
- Add bars to any overhangs where fences did not generate.

- Add bars to reinforce fences that support clasps or other delicate features.

For best accuracy, do not under-support clasps.
Nesting
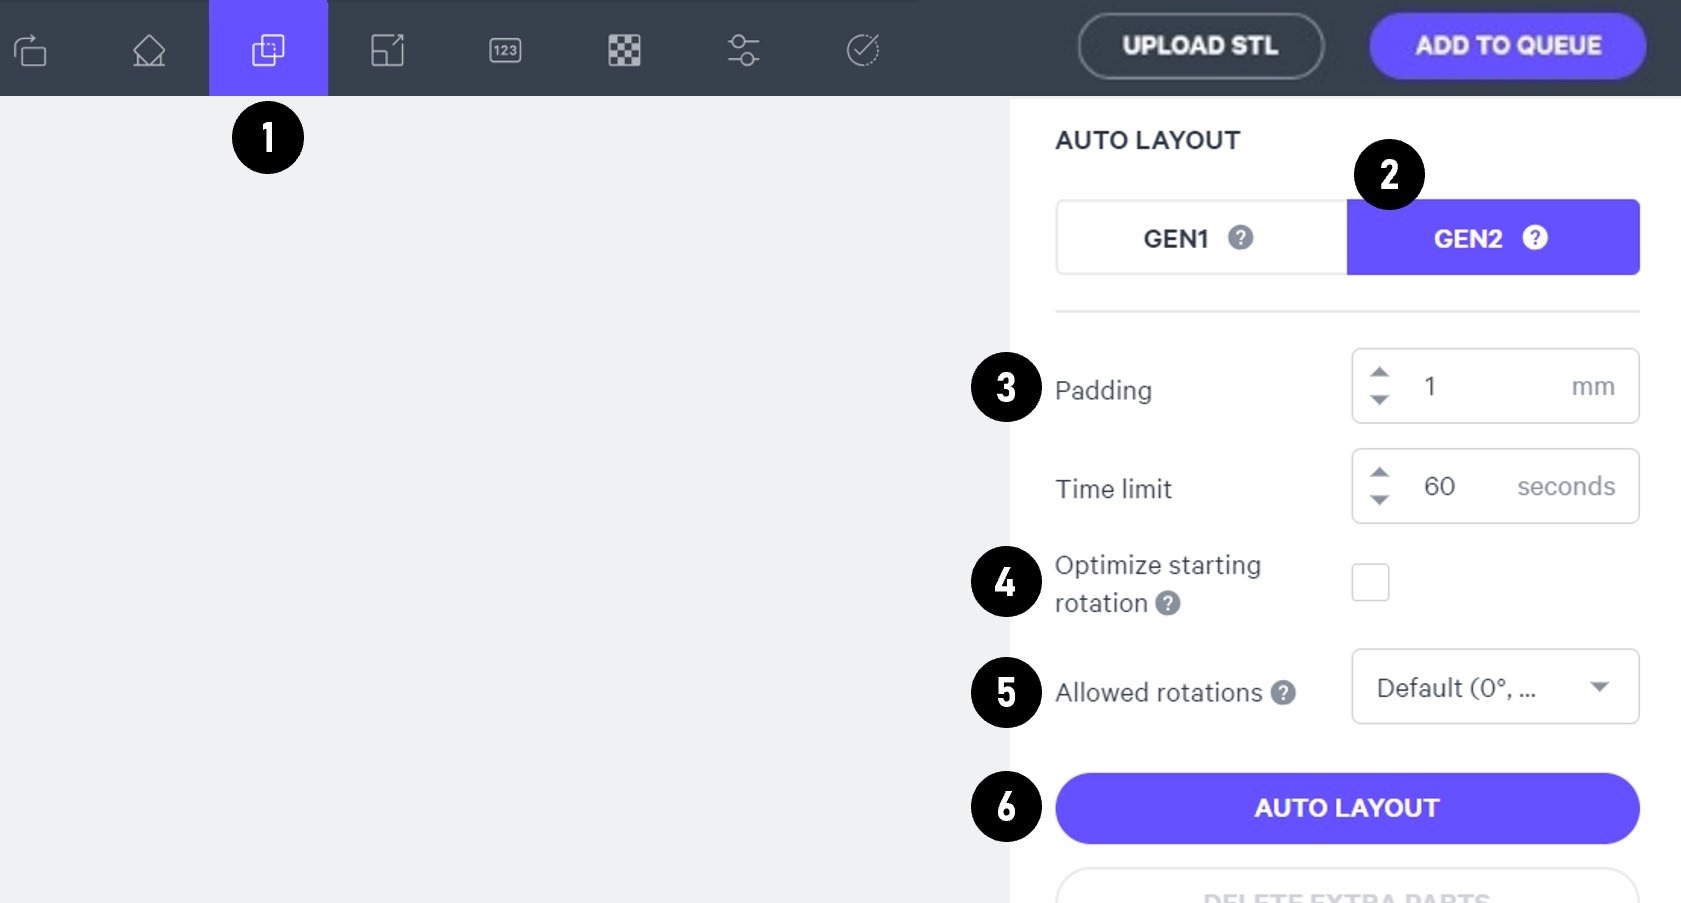
Select the Layout tab (Shift + L) in the top menu bar.
Under Auto Layout, select Gen2.
Gen2 usually gives the most efficient packing for dental devices.
Enter at least 1 mm in Padding.
Models require a minimum of 1 mm of space between them.
Leave Optimize starting rotation unchecked.
This leaves your parts in their previous orientations.
Leave Allowed rotations at the default setting.
This gives the software maximum flexibility to fit the most possible parts on the build platform.
Press the Auto Layout button to arrange your parts.
If necessary, nesting can be changed manually:
- Click and drag parts to adjust their position.
- Modify Z rotation by using the Spin tool or manual rotations under the Orient tab (Shift + O).
- Use the Part List tab as needed to more easily select models and focus on them.
Print Controls
Click Print Controls or Shift + P in the top menu bar.

Slicing
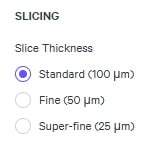
Set Slice Thickness to Standard
- FP3D Standard Slice Thickness = 100 µm
- AO-Polish FP3D Standard Slice Thickness = 50 µm
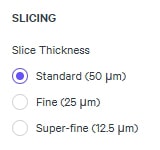
Reducing the slice thickness below the default standard slicing will increase print time and may reduce part quality and accuracy.
Project Analysis
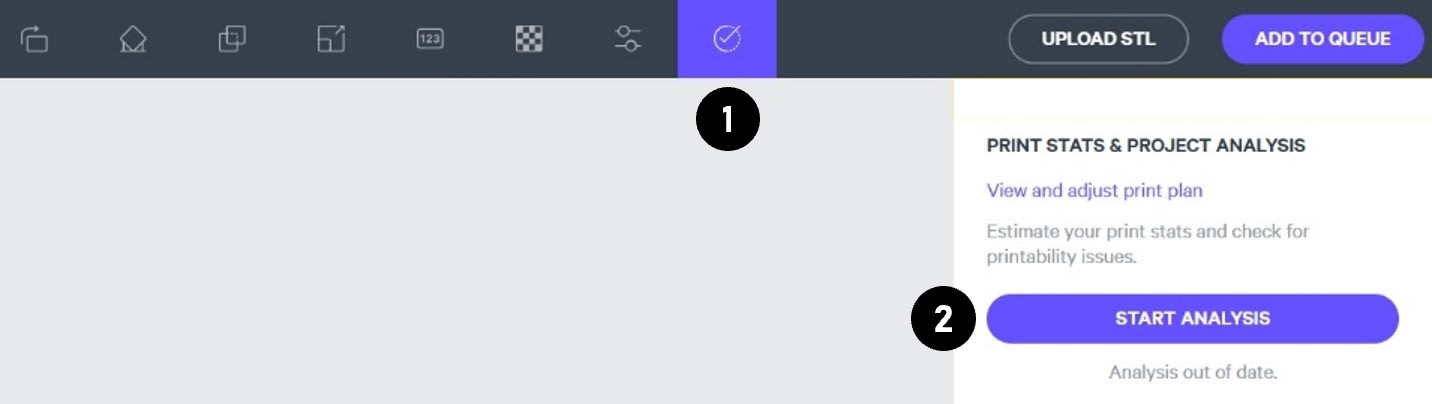
On the top menu bar, select the Project Analysis tab (Shift + A).
Press Start Analysis.
After a short time, the result of the project analysis will be displayed. Note the print time and the required resin volume.
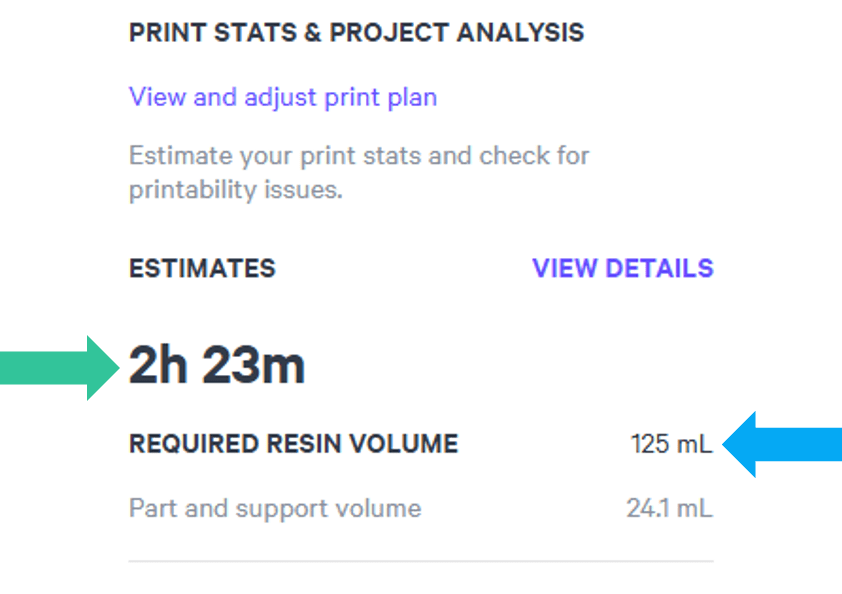
Click Add to Queue.
Printing and Post-Processing Video
This video shows the entire workflow from dispensing resin through washing and salt baking.
Resin Dispensing
Dispensing the two-part resin FP3D is very different from pouring out one-part resins. In particular, the 8 hour pot life is a variable that needs to be kept in mind.
Read Cartridge Dispensing for detailed information about setup and operation of the Cox Dual-Drive Dispenser.
Set up the Cox Dual Drive Dispenser.
- Check the battery.
- Install E:F ratio plates.
- Set speed to 1.
Install the orange mixing tip on the cartridge.
- Replace the mixing tip 8 hours after the initial dispense as the resin reaches the end of its pot life.
Slide the cartridge into the dispenser.

Place the shroud over the mixing tip.
Dispense and discard approximately 10 mL of resin for new cartridges. This standard procedure is known as burn off.
If you are experiencing discoloration in your parts, we advise the following:
- Ensure that you are following proper burn off procedure and dispensing at the speed specified in the IFU.
- If discoloration persists, burn off resin for every dispense, not just new cartridges.
Dispense the required resin into the cassette.
Printing
Install the cassette with the newly dispensed resin in the printer.

Mix resin in cassette using silicone spatula.
- This mixing helps ensure color accuracy.
Mix resin before every print, including after initial dispense.
Start printing.
When printing is complete, remove the platform to begin post processing.

See Printing for more information.
Washing
The washing process for FP3D is similar to washing most one-part dental resins.
FP3D has a total maximum solvent exposure time of 5 minutes.
Remove the printed parts from the platform.

Remove the supports from the parts.
Supports are easily removed manually.

Using a blue shop towel can help keep sticky resin off of your gloves.

First wash.
- Add parts to washing container of fresh IPA.
- Place container on orbital shaker and wash parts for 2 minutes at 140 RPM.

Detailed cleaning.
- Remove parts from IPA.
- Wet a toothbrush with IPA and remove any liquid resin from tooth pockets, intaglio surfaces or anywhere that resin can be trapped.

Second wash.
- Place parts in container of fresh IPA.
- Place container on orbital shaker and wash parts for another 2 minutes at 140 RPM.
Dry the parts.
- Place parts on clean surface to dry.
- Alternately, use compressed air to dry parts.
Curing
FP3D parts must be packed in salt and thermally cured (baked) in a Yamato convection oven.
Thermal curing must be started within 8 hours of printing.
Parts must be fully clean and completely dry before baking.
Program the Yamato convection oven.
Before parts can be cured, the oven must be programmed with the appropriate temperatures and timings for curing FP3D.
- Follow the instructions in Oven Programming to program your oven.
- Find the precise settings for curing FP3D in the handout under Resin Programs for the Yamato Oven.
Add salt to the baking tray.
- Use a fine mesh strainer to add salt to a 75 mm (3 inch) deep baking tray.

- Add approximately 50 mm (2 inches) of salt.
- Shake and/or tap the tray to make the surface of the salt relatively flat.

Replace salt after 10 curing cycles to ensure part cleanliness.
Place the parts in salt.
Parts must be completely dry before placing in salt.
- Place each part intaglio side up in the salt.

- Gently nestle each part into the salt so that all down-facing surfaces are supported by the salt.
Using excess force will deform the part.

Cover the parts with salt.
- Using the sifter, add about 25 mm (1 inch) of salt on top of the parts.
- To enable even heat distribution during baking, the parts should have the same amount of salt above and below them.
- Shake and/or tap the tray to ensure the parts are settled in the salt.

Cover tray with aluminum foil.
- Cover tray with aluminum foil.
- If necessary, write identifying information on a metal tent sign and place it on top of the foil.

Bake the parts.
- Place covered tray in the oven.
- Start the FP3D bake program:
- 15 minute ramp to 120° C
- Hold at 120° C for 10 hours.
Remove the parts from the oven.
The tray and interior of the oven will be hot. Use caution when removing items from the oven.
- Wearing heat-resistant gloves, remove the pan from the oven and allow it to cool (~27° C).
- Alternately, parts may be allowed to cool inside the oven.
FP3D parts will change color after baking.

Rinse
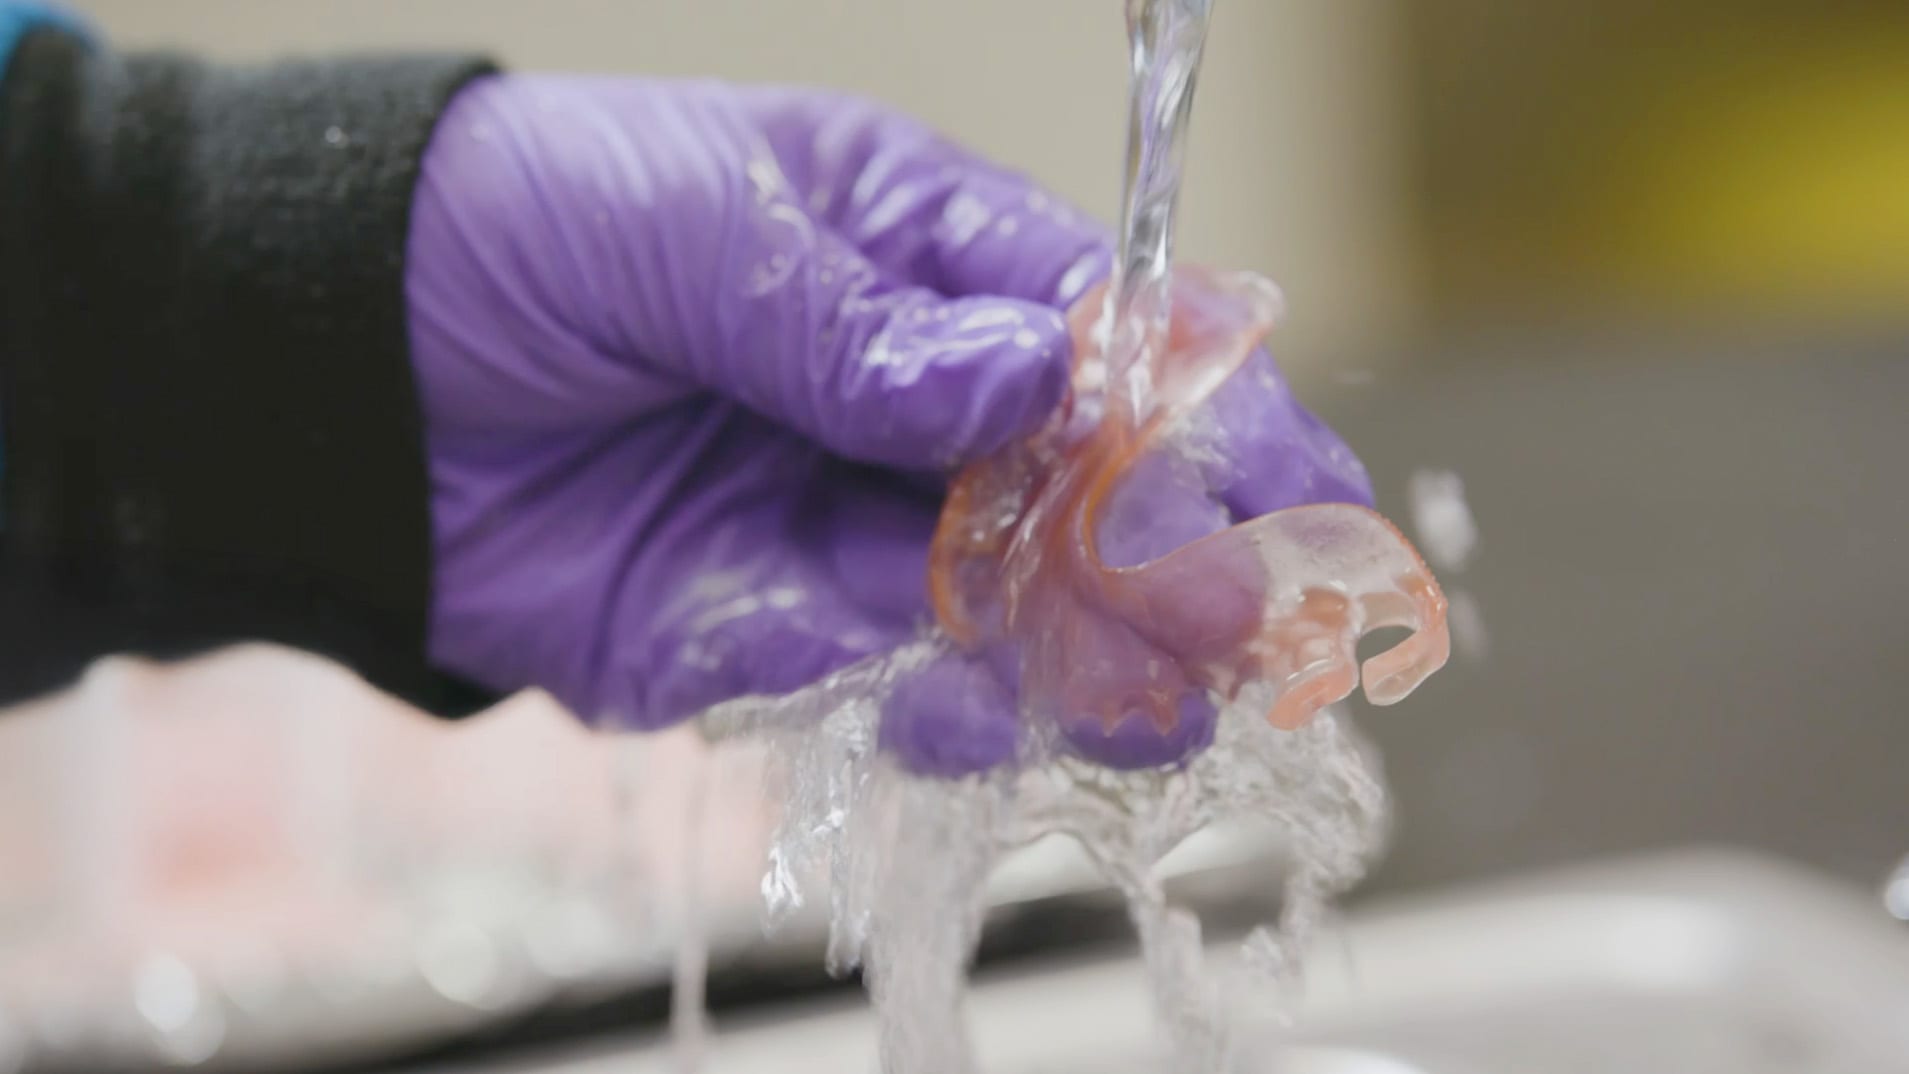
Rinse parts with warm water to remove excess salt from the surface.
- A toothbrush can help remove salt residue, but it is not required.
Dry parts.
- Place parts on a clean surface to dry.
- Alternately, use compressed air to dry parts.
Tooth Bonding and Finishing
FP3D partial dentures require a final UV cure cycle. See step 3 below for more info.
Video
The numbering of the steps below differs from the video above.
Workflow
Finish teeth and base according to your lab's standard practices.
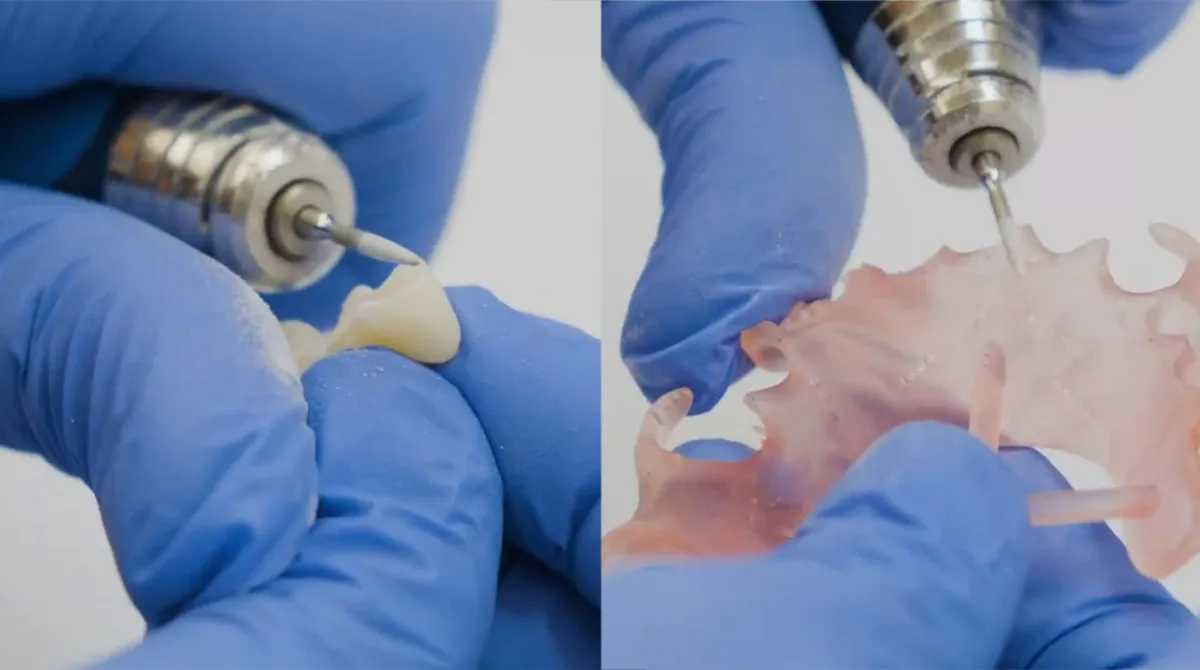
Bond the teeth to the partial denture.
- Follow the tooth bonding instructions for your tooth material of choice.

Perform the final UV cure.
FP3D partial dentures require a final UV cure cycle.
- Cure the assembled denture by following the instructions for your tooth material.
- If the tooth bonding instructions do not include a final UV cure, then consult the table below for final cure instructions.
Cure Unit | Process |
|---|---|
Dreve PCU LED | Program Name: Dhealth 1 • Available in Configuration File 1 18 minutes at 90% intensity, under vacuum. |
Dentsply Sirona Digital Cure | Program: Lucitone 60 minutes at 80º C |
Dentsply Sirona Digital Cure: Large Capacity | Program: Lucitone Digital Appliances Preheat: 30 minutes Cure: 60 minutes at 80º C |
Curing instructions are also available on the IFU.
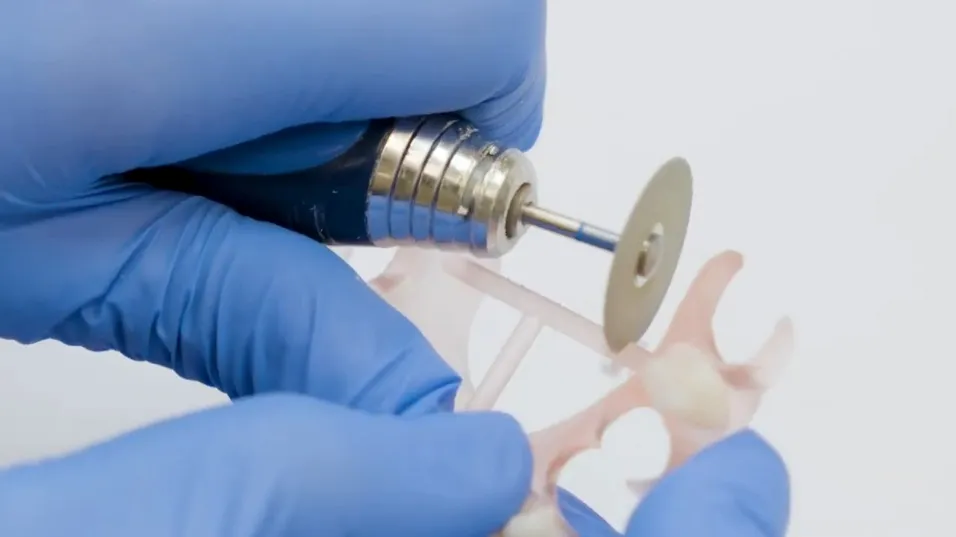
Remove any T-bars and smooth base.

Your partial denture is now complete!

Clinical Handling
FP3D is engineered to respond to intraoral conditions. Avoid aggressive flexing outside of intended use.
Patient Handling Instructions
This medical device is a single-patient, customized, multi-use oral appliance that should be cleaned between usages.
- The patient should clean the appliance with soap and warm water, or any over-the-counter mild cleaning agents indicated for oral devices.
- Dry partial dentures thoroughly overnight if not wearing and do not leave submerged in the cleaner.
Printable Patient Care Instructions