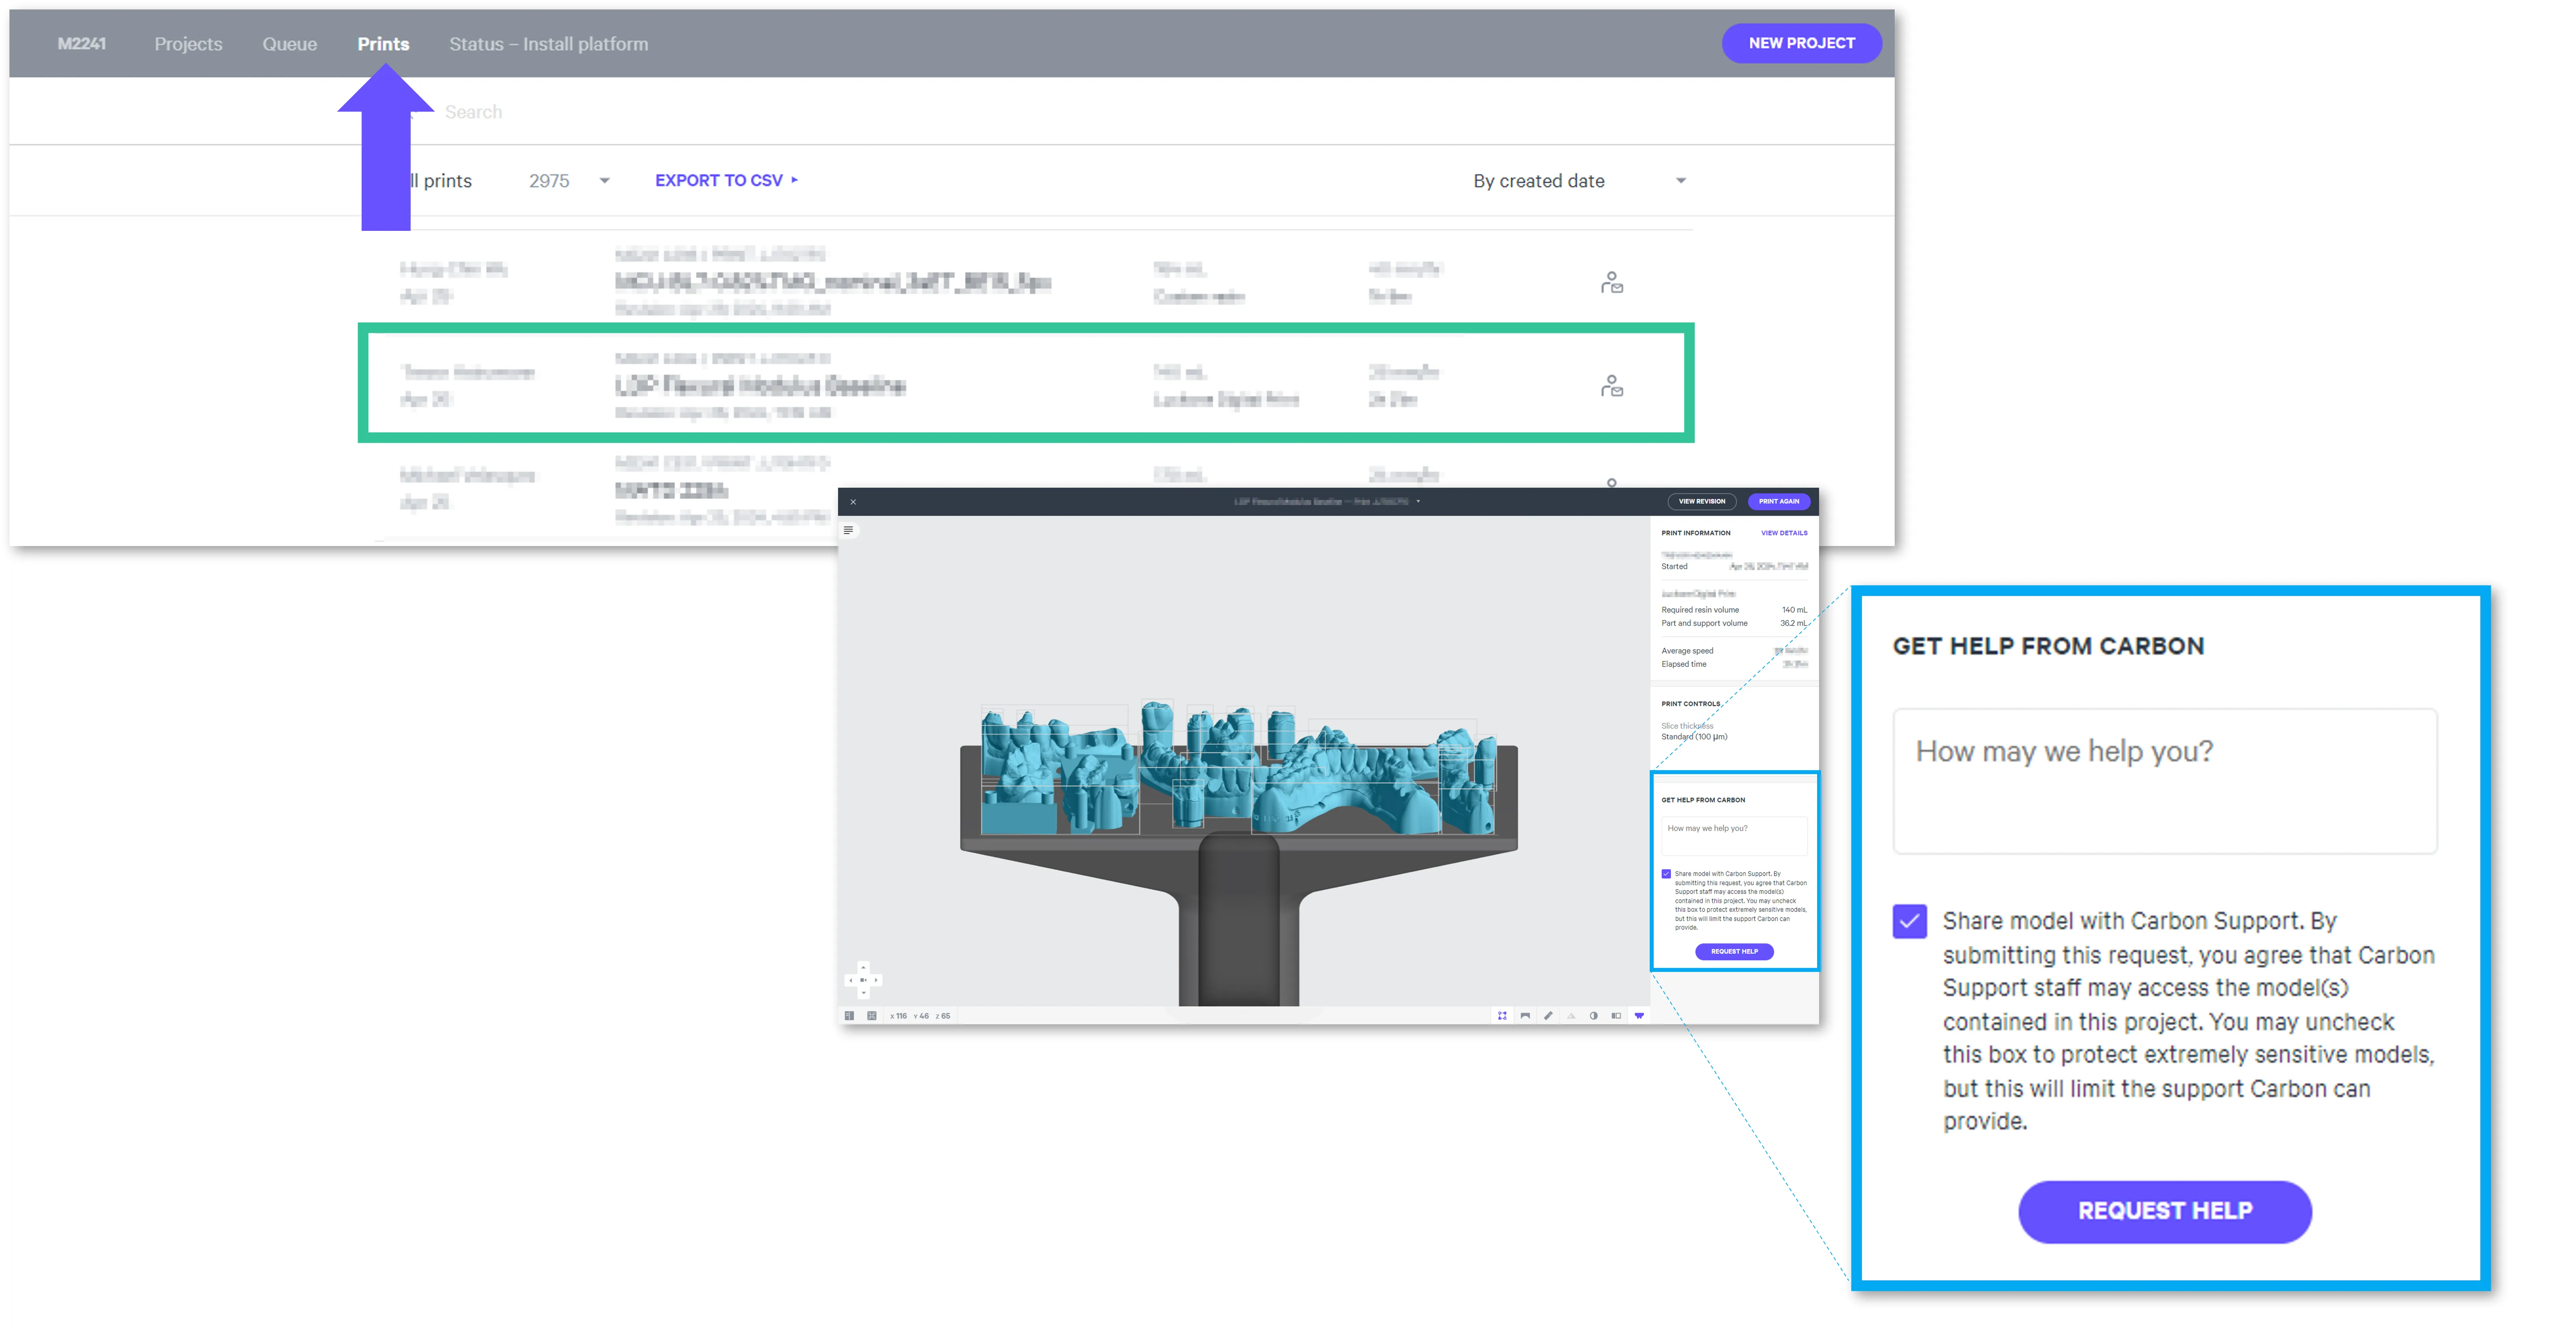
Desktop Health SmileGuard
Overview
Desktop Health™ SmileGuard™ for Carbon® printers is now available to produce splints and night guards. Offering the perfect blend of strength and comfort, this breakthrough light-curable resin formulation delivers stunning clarity and superior quality with optimal strength and shape retention for durable protection coupled with soft flexibility for a comfortable and perfect fit.
This course will cover digital prep of your splints and night guards to properly prepare them for printing.
This resin is compatible with the AO Polishing Cassette.
Resource Links
Protocol
This downloadable handout provides important usage information, including instructions about storage and post-processing. Print it out and bring it into the lab!
Dental Post-Processing Grids
One of our most popular downloads! This table provides washing and curing instructions for all supported dental resins.
Print it and use it in the lab as a quick reference.
German/Deutsch
Spanish/Español
Resin menu options
Select the following option depending on which resin or cassette you are using::
- Desktop Health SmileGuardwhen using the standard C2 (M2) or D1 (M3/M3 Max) cassette.
- AO-Polish Desktop Health SmileGuard when using the AO Polishing Cassette (M2).
- The AO Polish workflow is only compatible with vertically oriented parts.
Design Recommendations
- Carbon® does not make splint design recommendations.
- Carbon encourages users to follow the guidelines of your design software.
- Desktop Health™ has approved a wall thickness ranging from a minimum of 2 mm to a maximum of 3 mm.
- Single-sided splints are easily printed.
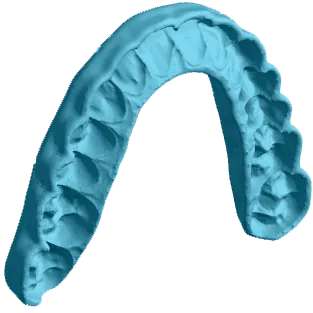
Vertical Orientation and Support
Printing splints in a vertical orientation maximizes the amount of splints that can printed at once.
Splints can also be printed horizontally, which is shown in a later section. Carbon encourages experimenting with both methods to determine which best suits your lab's designs.
Orienting
1. Click on Orient or Shift + O in the top bar in the printer interface.
2. In the lower right corner of the bottom bar, turn on Overhang Detection or V key and set to 40 degrees. Areas that need support will appear red.

3. Orient the splints so they are about parallel to the platform.
4. Rotate the models 90 degrees with the anteriors facing the platform. The models should be standing vertically, perpendicular to the platform.

Surfaces that have overhangs will require supports. Surfaces with supports will require finishing to ensure proper seating.
Supporting
Supports hold up the part during printing. They do this by connecting platform-facing surfaces to the platform.
Review Supports in Printer UI course for more information.
Enter Support mode
- Click Support in the dark gray bar at the top of screen.
- Under Position, select Above Platform to lift parts off the platform.
- Click the Manual tab and make sure Patch is selected.
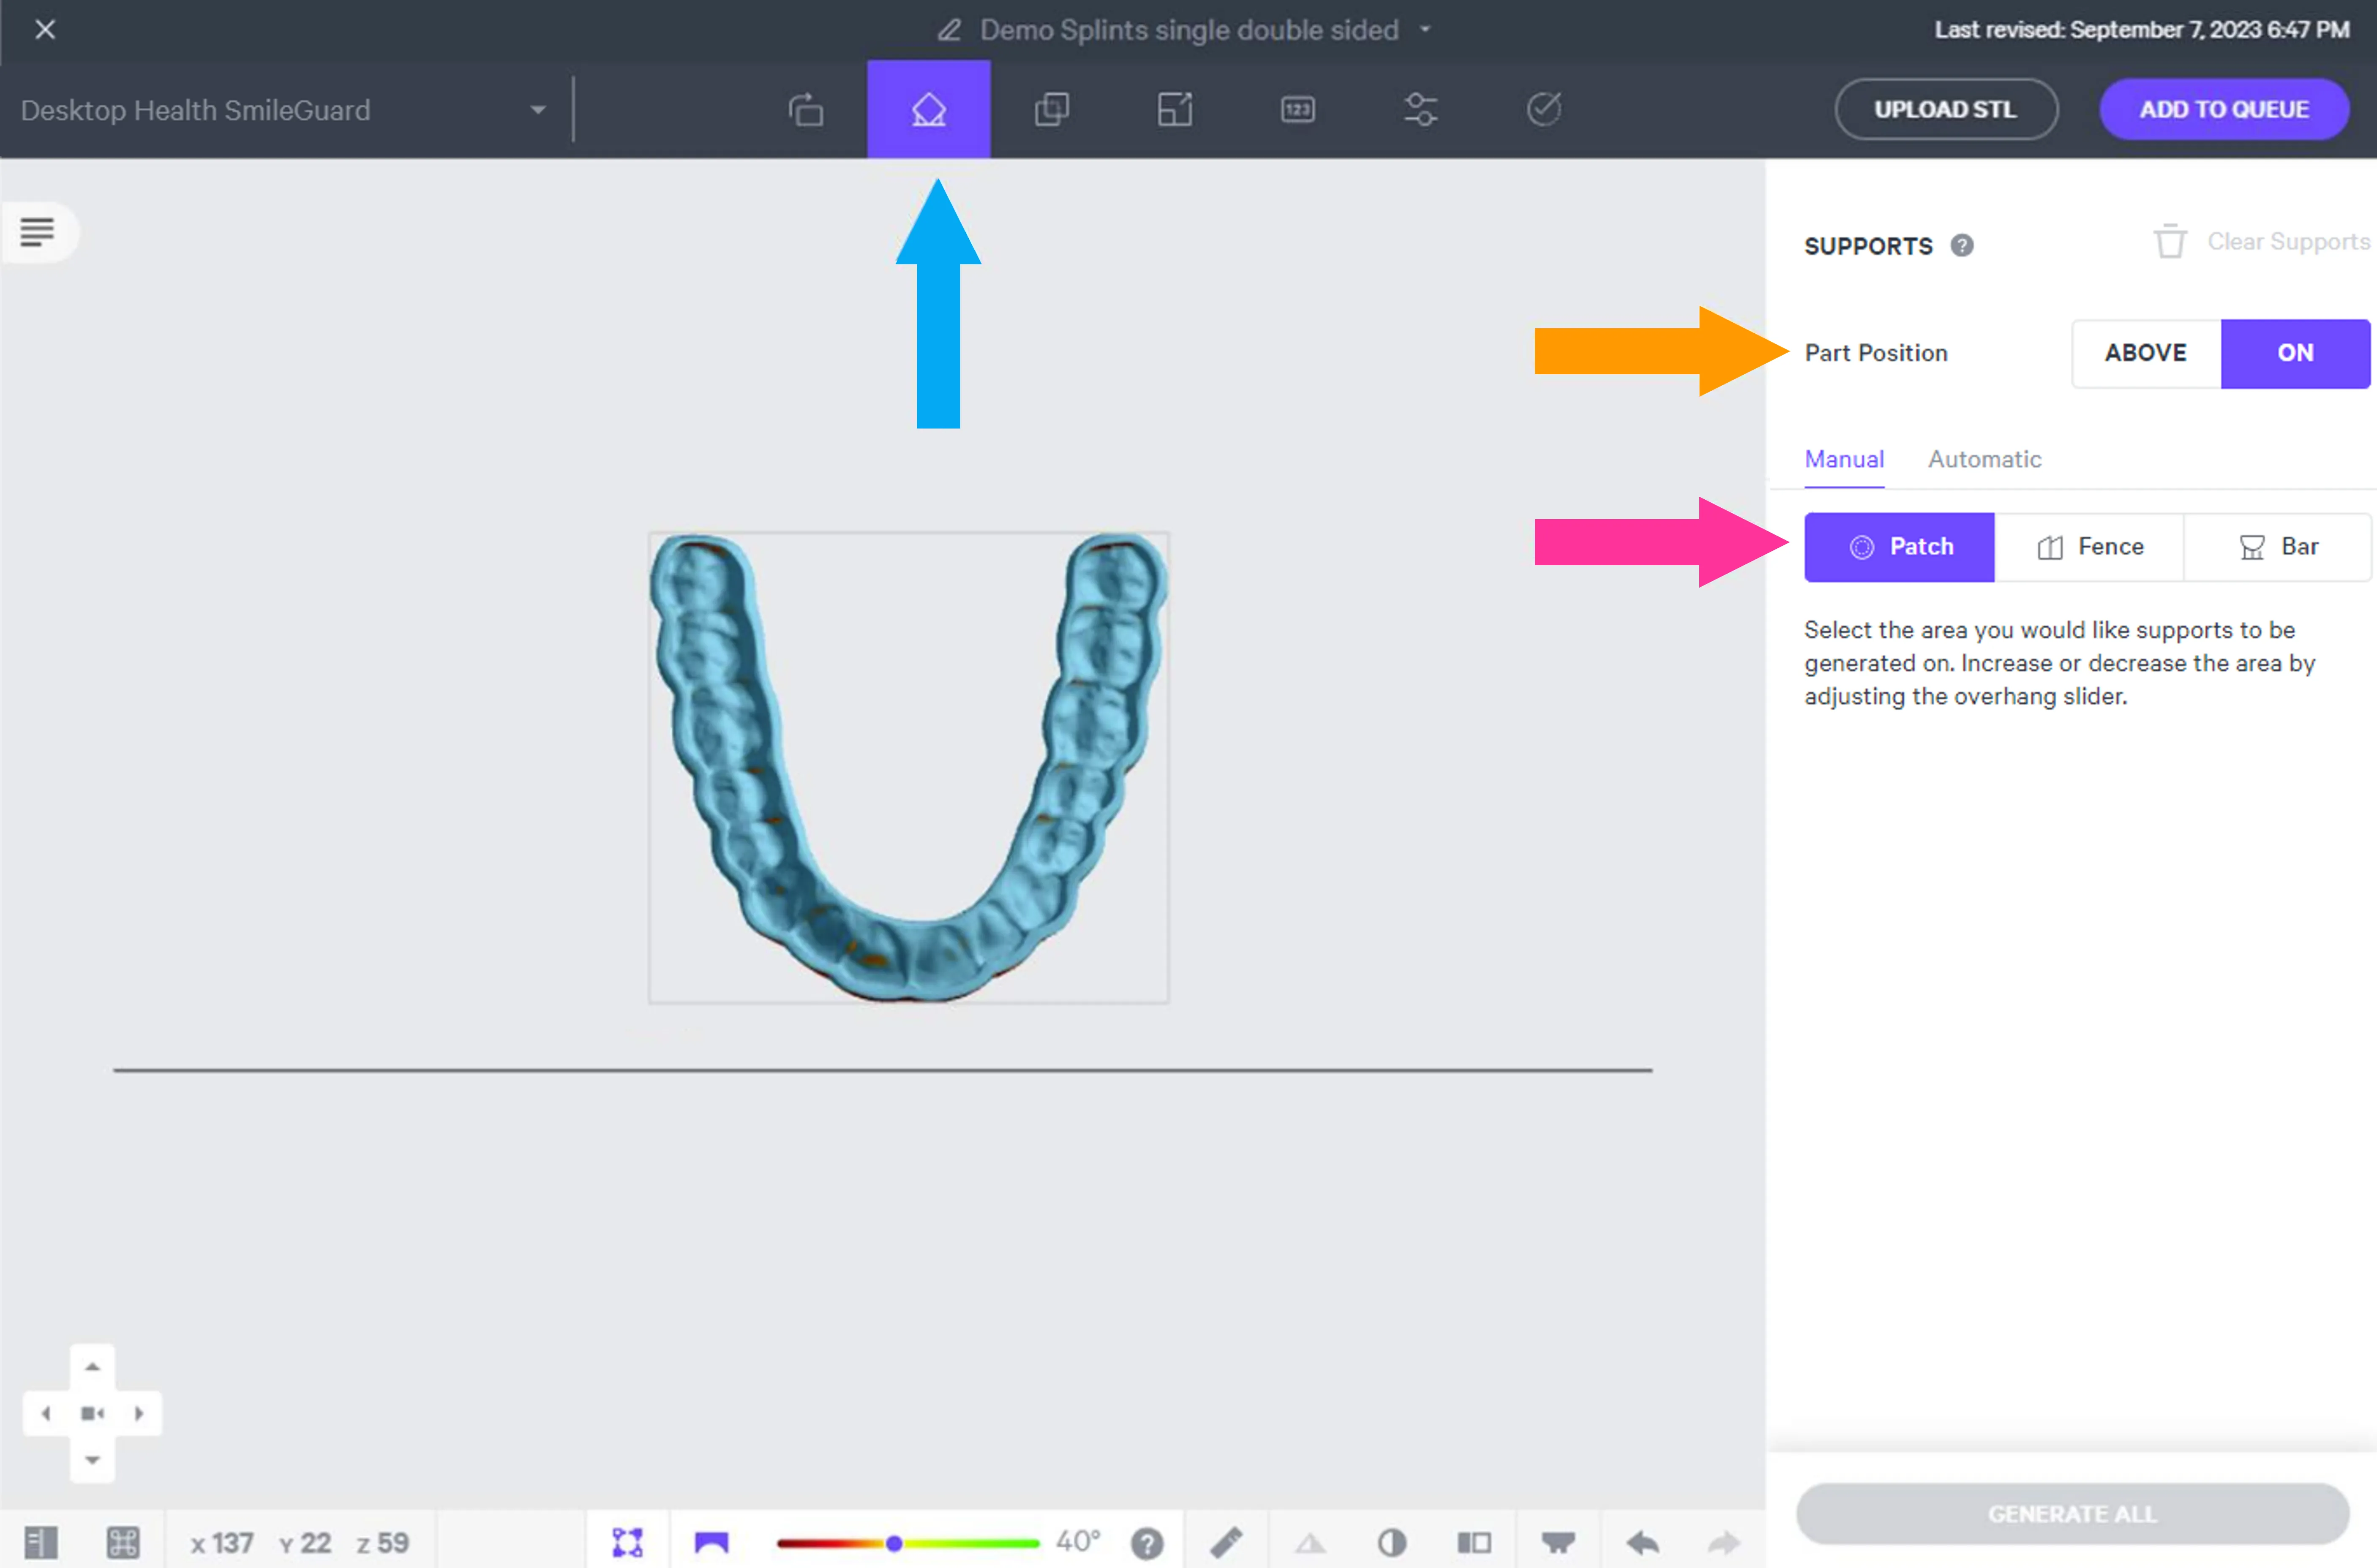
Add supports
- Click on the anterior surface of a splint to select a patch.
- Under the Patch tab, adjust the Overhang to between 40 and 60 degrees.
- Select a value to ensure that the patch covers the six anterior teeth.
- In the Primary Support Type dropdown menu, select Fence. Fences are easier to remove and require less finishing than other support types.
- Enter a Spacing value between 2.5 and 4 mm.
- Make sure the Boundary Fence checkbox is selected.
- Margin value should be 0 mm.
Example of a well-supported splint

Horizontal Orientation and Support
Orienting
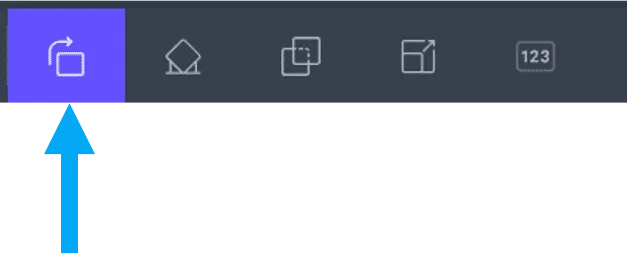
- Click on Orient or Shift + O in the top bar in the printer interface.
- Orient the splint so that the cameo surface is facing the platform.
- Adjust the splint so that it is parallel with the platform.

Supporting
Use fences to support your parts: They are easy to remove and do not increase the footprint of the splint, enabling more to be fit onto the build platform.
Enter Support mode
- Click Support in the dark gray bar at the top of screen.
- Under Position, select Above Platform to lift parts off the platform.
- Skip Auto Support Method as this mode is not recommended.
- Click Manually Add to go to the Support editing interface.
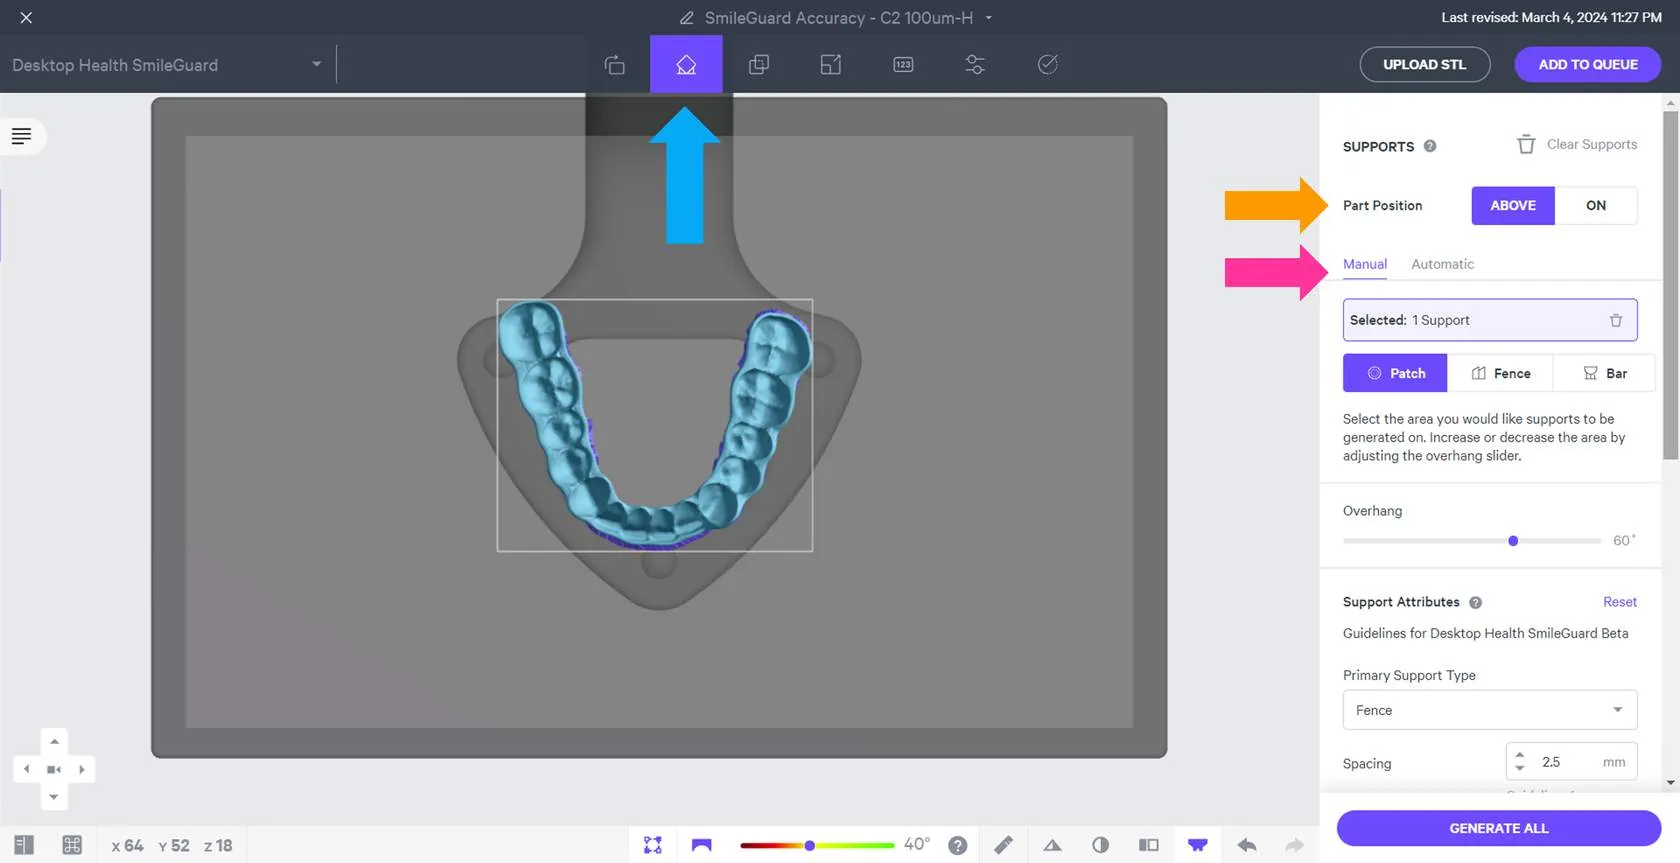
Add supports
- Click on the cameo surface of a splint to select a patch.
- Under the Patch tab, adjust the Overhang to between 40 and 60 degrees.
- Select a value to ensure that the patch covers the splint.
- In the Primary Support Type dropdown menu, select Fence. Fences are easier to remove and require less finishing than other support types.
- Enter a Spacing value between 2.5 and 4 mm.
- Make sure the Boundary Fence checkbox is selected.
- Margin value should be 0 mm.
Nesting

- Select the Layout tab (Shift + L) in the top menu bar.
- Under Auto Layout, select Gen2.
- Gen2 usually gives the most effecient packing for dental devices.
- Enter at least 1 mm in Padding.
- Models require a minimum of 1 mm of space between them.
- Leave Optimize starting rotation unchecked.
- This leaves your parts in their previous orientations.
- Leave Allowed rotations at the default setting.
- This gives the software maximum flexibility to fit the most possible parts on the build platform.
- Press the Auto Layout button to arrange your parts.
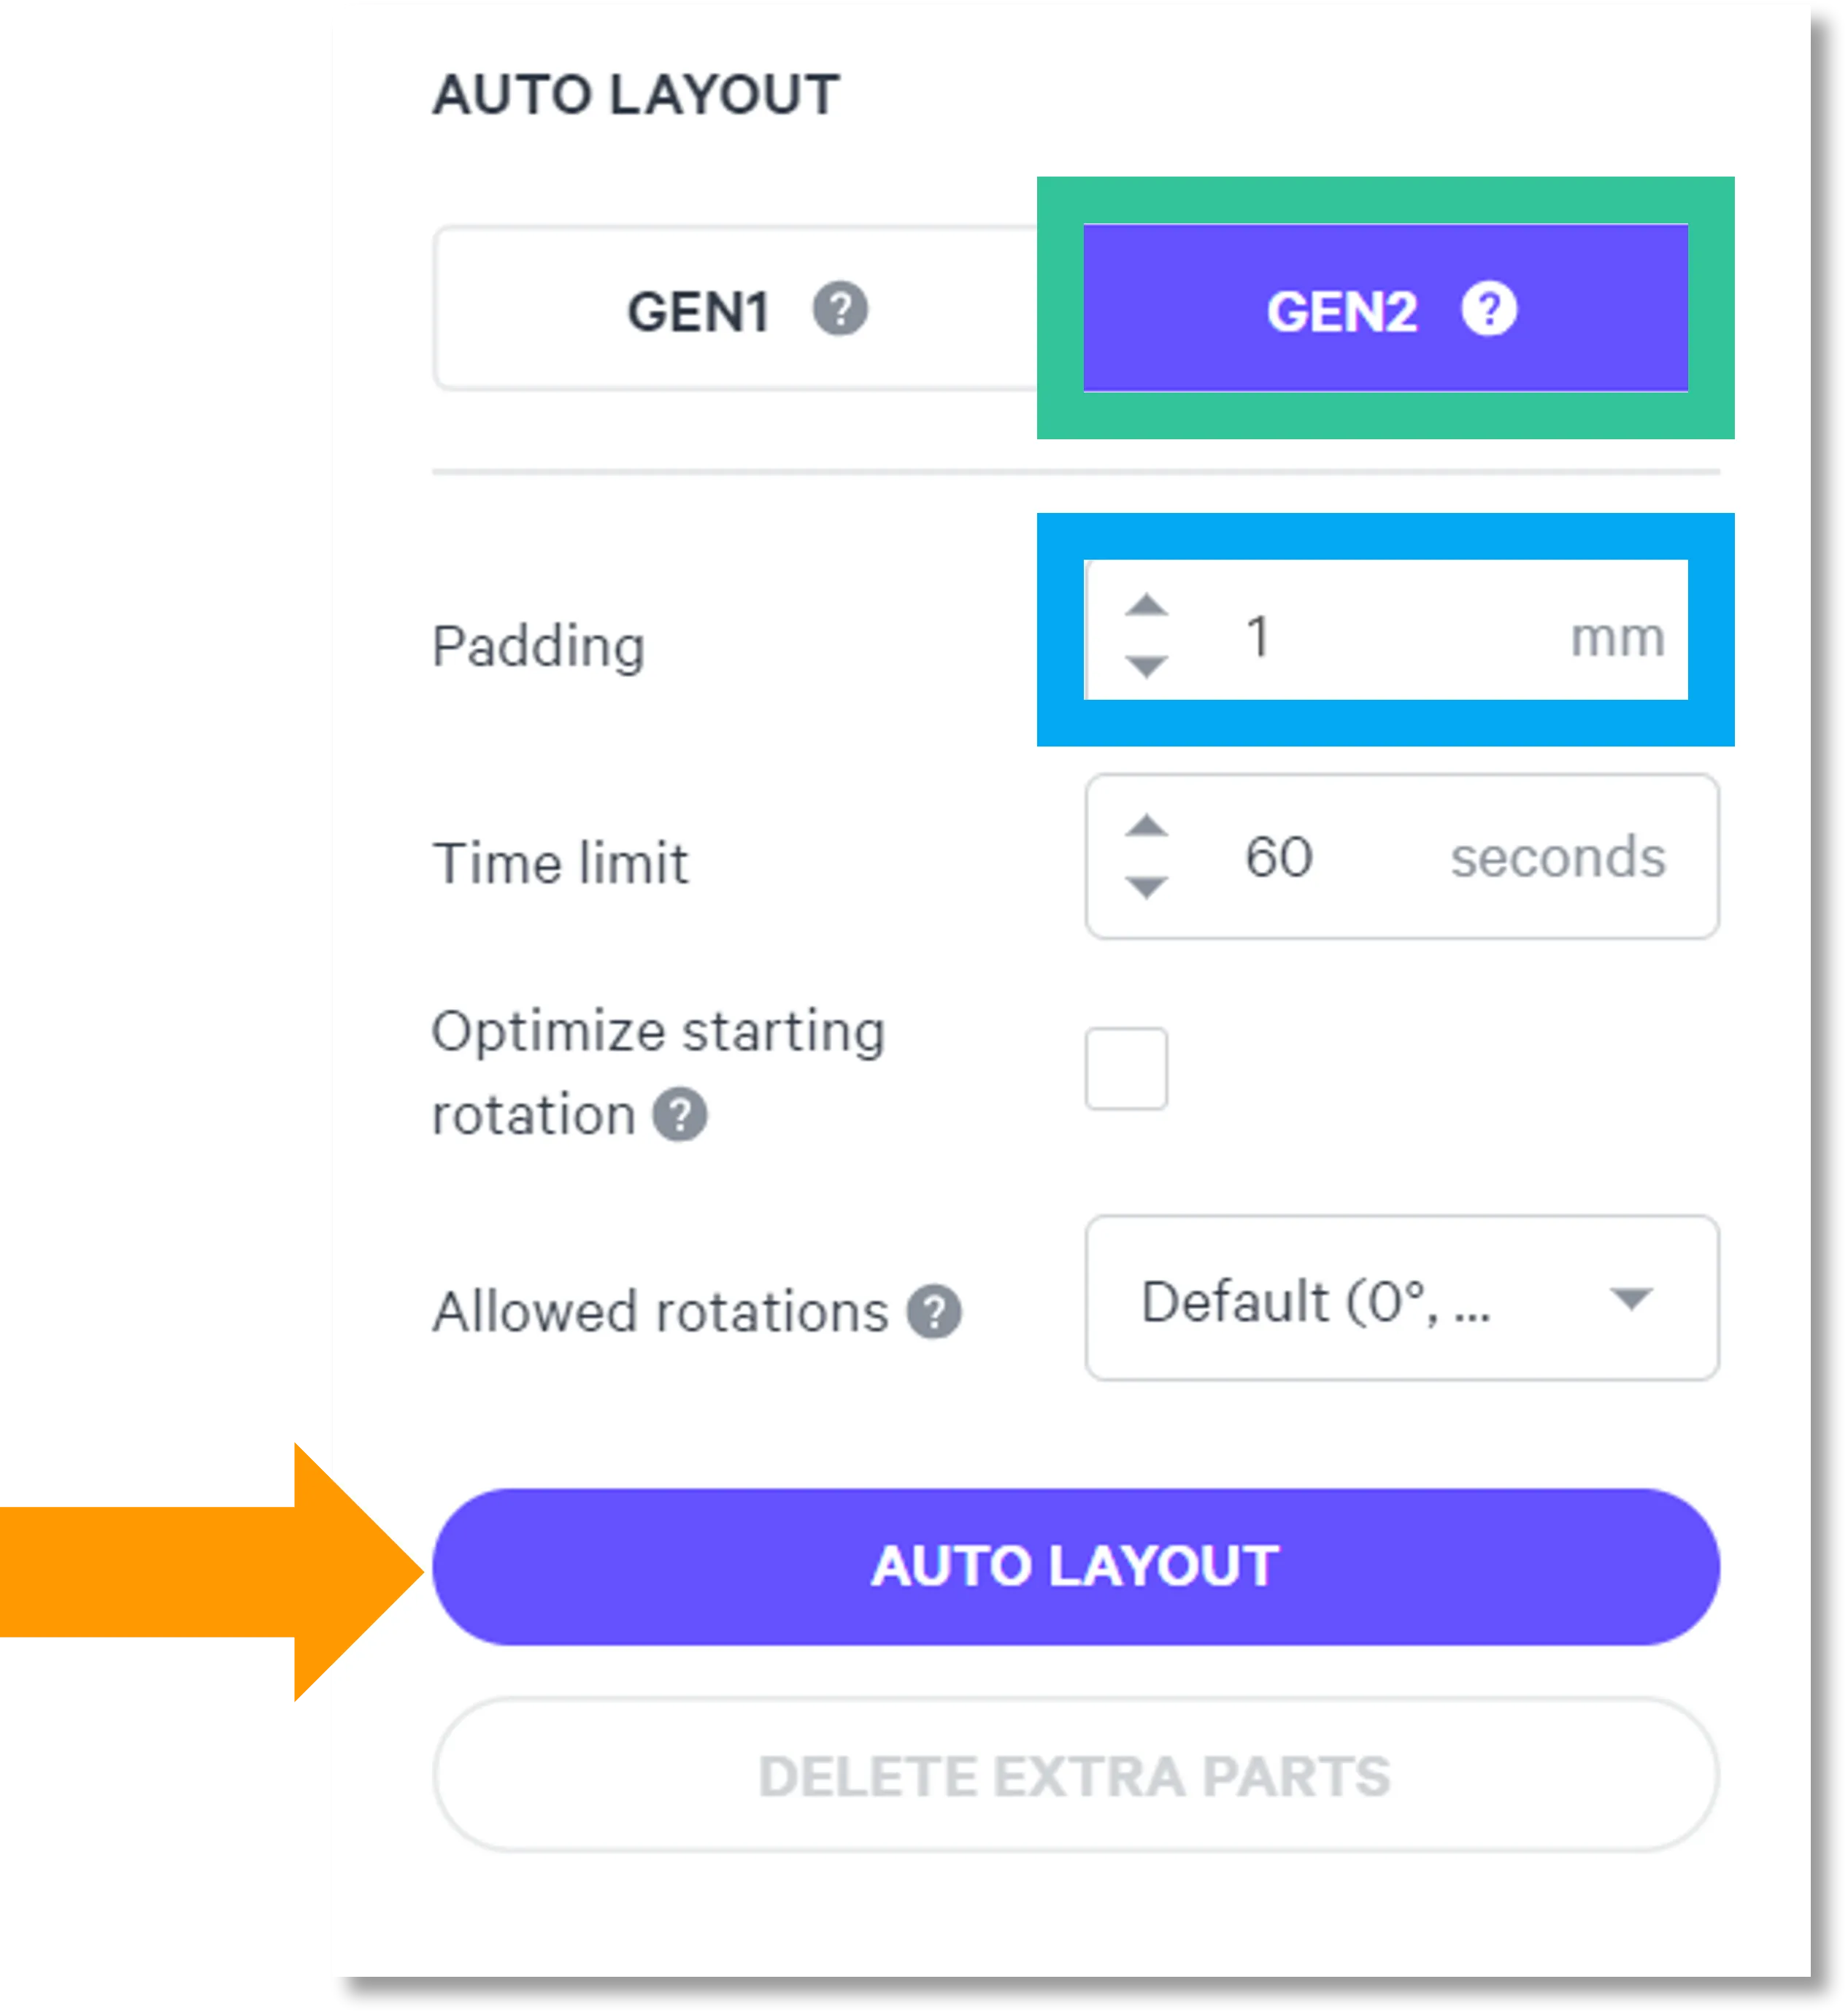
If necessary, nesting can be changed manually:
- Click and drag parts to adjust their position.
- Modify Z rotation by using the Spin tool or manual rotations under the Orient tab (Shift + O).
- Use the Part List tab as needed to more easily select models and focus on them.
Print Controls
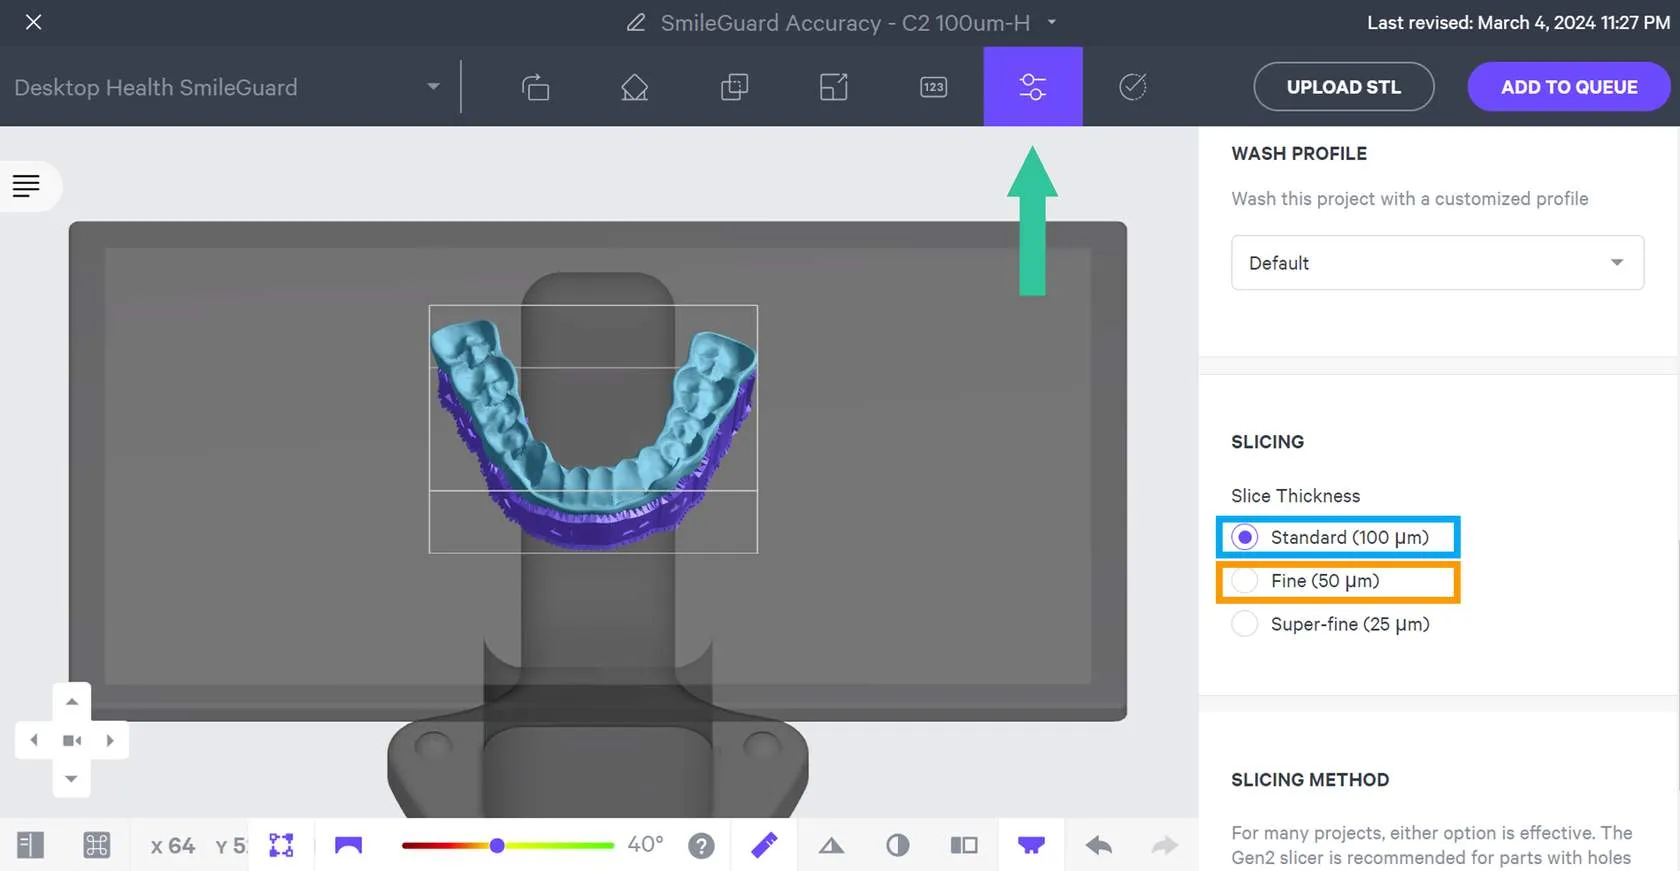
Click Print Controls in the top menu bar.
Carbon recommends these settings to deliver the best results for splint models.
Slicing
- Slice Thickness should be Standard (100 µm)
- Fine (50 µm) slicing has been validated with the AO-Polishing (C4) cassette. Reducing the slice thickness by selecting the Fine (50 µ) will not compromise part quality/accuracy, but it will increase print time.
Manufacturer Instructions for Use
Post-Processing
Please refer to the Desktop Health™ IFU for post-processing information.
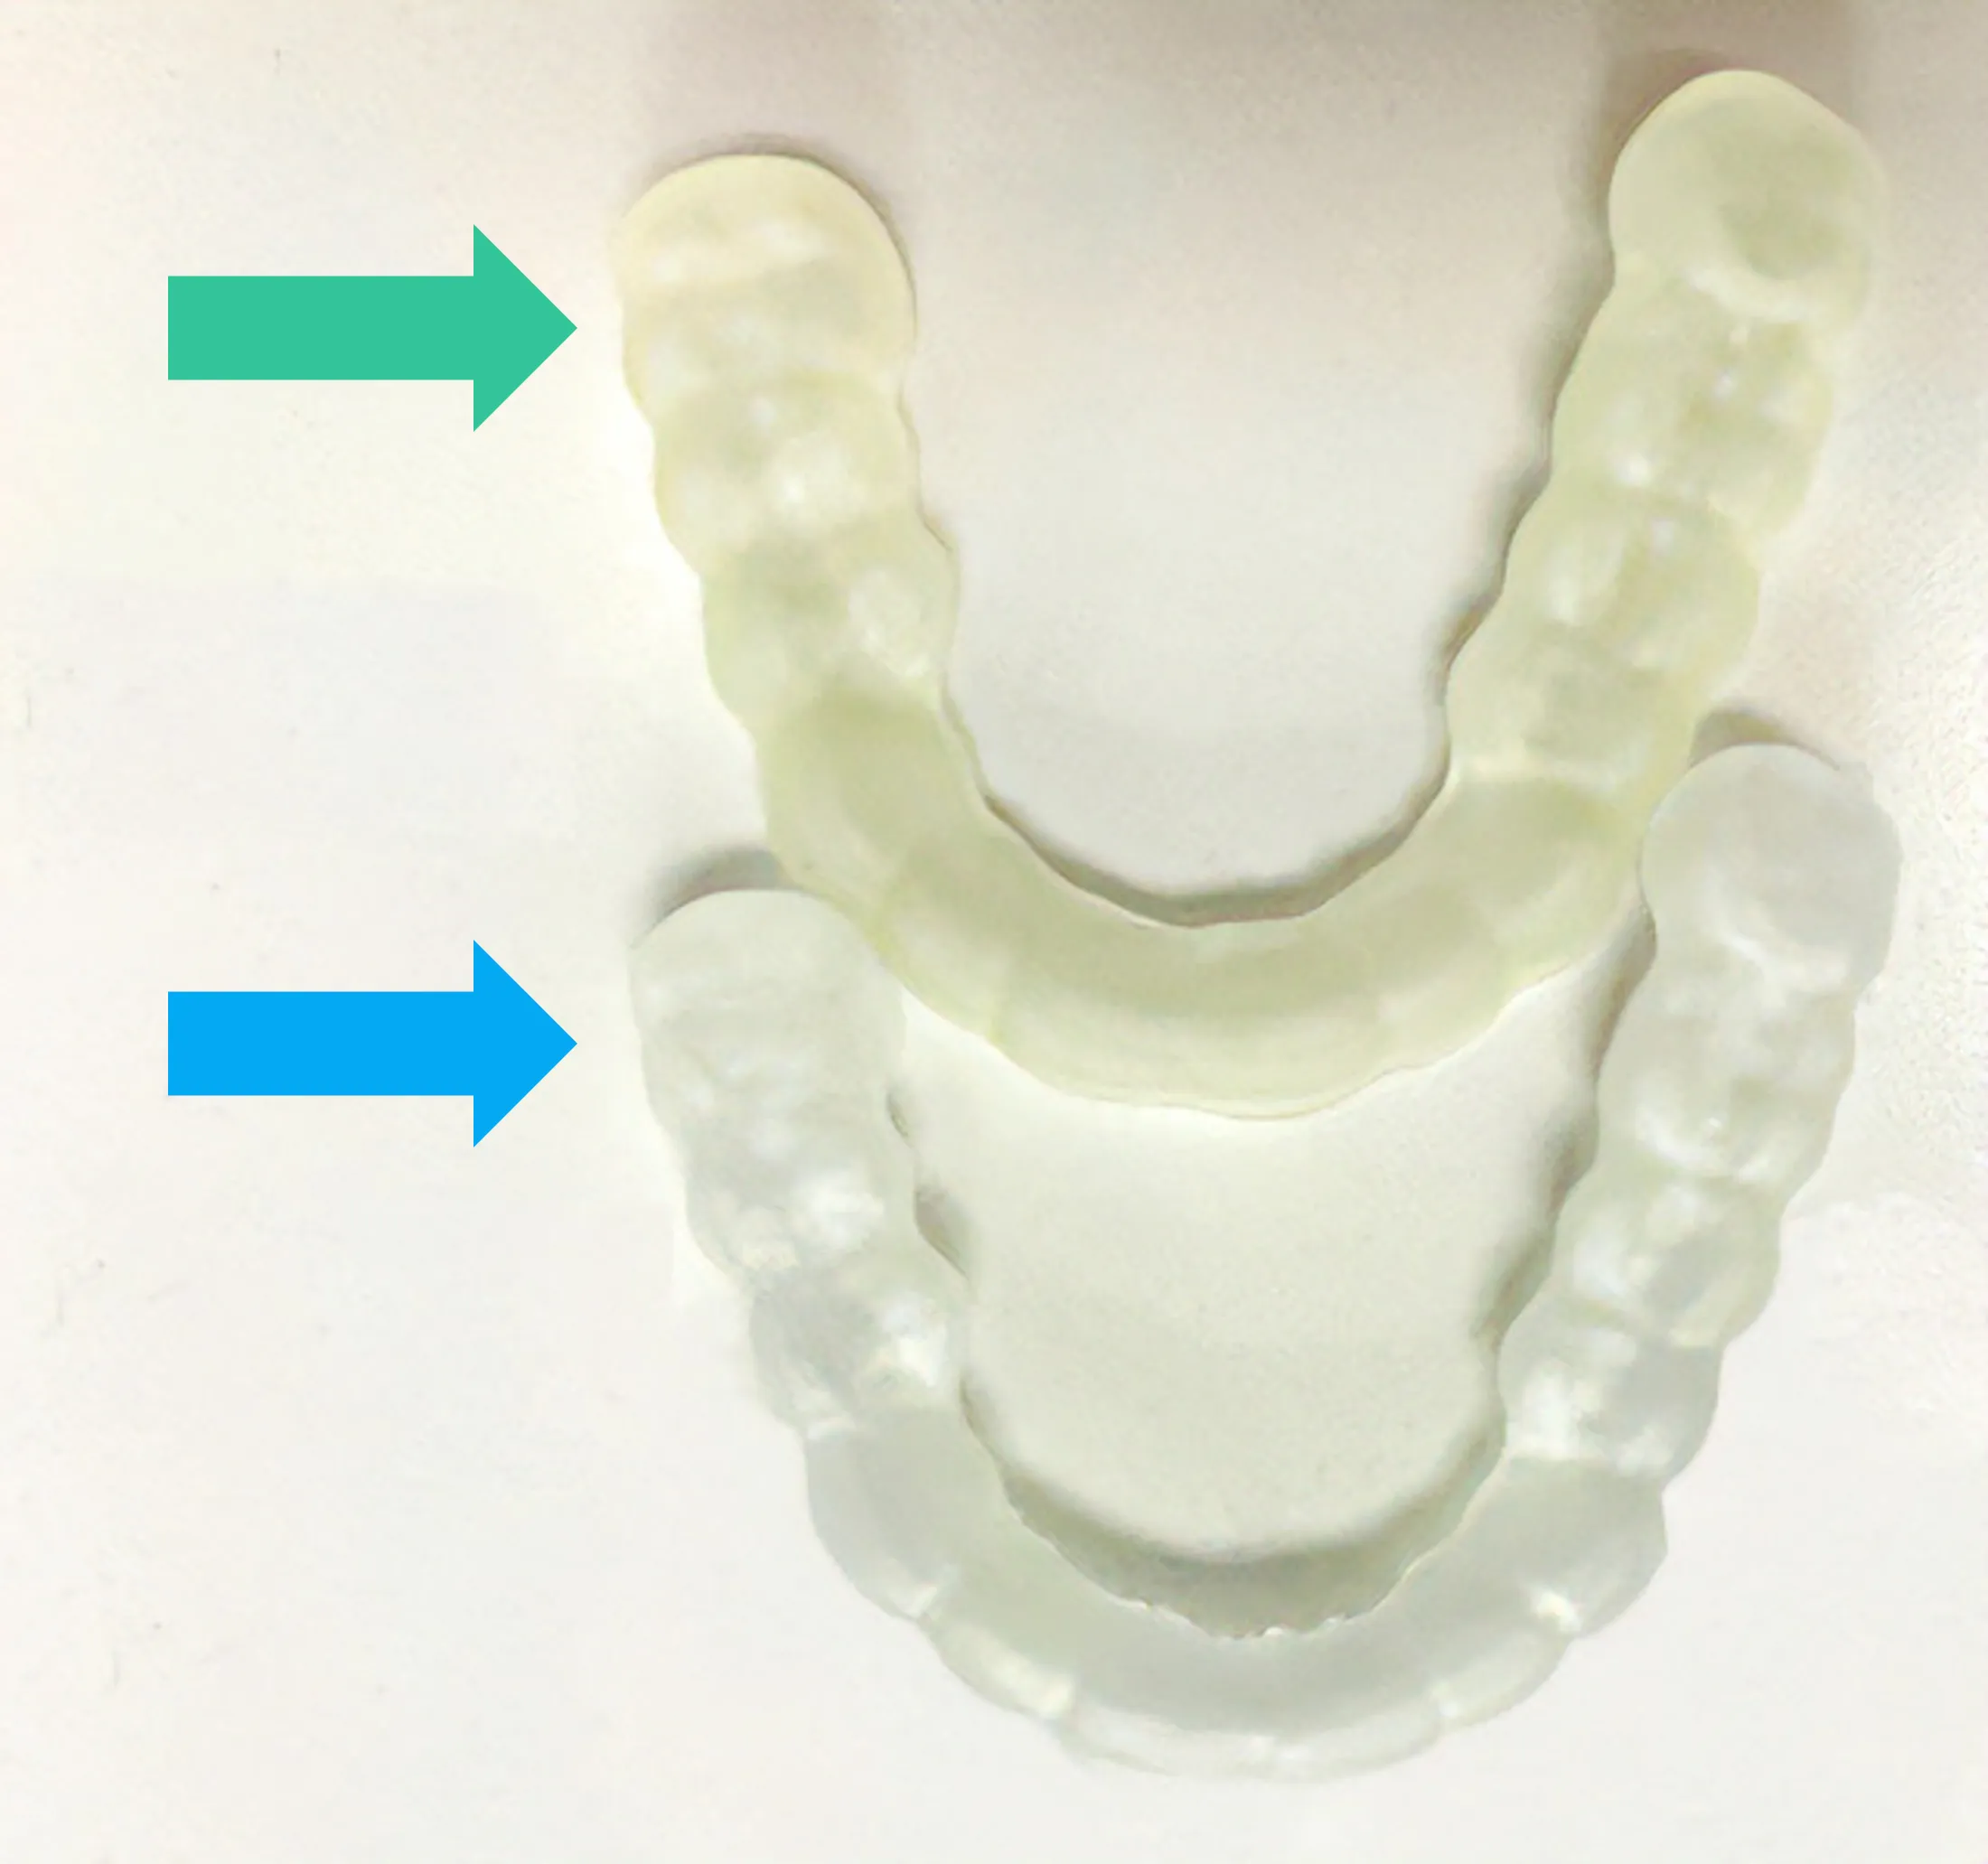
Temporary yellowing with the Dreve PCU LED
- When curing SmileGuard™ resin parts using the Dreve PCU LED, a yellow tint is expected and normal.
- Yellowing does not occur when using the Otoflash G171.
- The yellowish tint will typically fade away within 1 - 3 days.
- If after this time period you are still experiencing issues with discoloration, please contact Carbon Support with a detailed description of the issue.
Questions and Support
For questions about resin properties, printing, washing or curing your denture teeth, please contact Desktop Health Support:
For questions about your Carbon printer or Carbon software settings used for this resin, please contact Carbon:
- Email: [email protected]
- Phone:
- U.S. and Canada 1-650-285-6307 option 2
- Germany +49 6102 5790849
- UK +44 (0) 2082 647484
- Printer UI: On the dashboard, select the Prints tab. Select one of the printed projects. Click Request Help in the lower right corner.