Voids
Voids
Small negative depressions on faces parallel to the platform.

How to Identify
Voids can be diagnosed as follows:
- Voids occur on surfaces parallel to the platform.
- Voids are usually circular or oblong in shape.
- Voids are most common on large cross sections.
Resin Starvation is a defect that can appear similar as it arises from similar circumstances.
Cause - Inconclusive
Cause - Large Cross Section
Solution - Print Preparation or Part Design
Cause - Inconclusive
Cause - Inconclusive
Troubleshooting
It is recommended that you review all the possible solutions before taking action to ensure you are pursuing the best course of action.
If the best course of action is not apparent, try the troubleshooting options in the order listed. Refer here for more tips.
Try the following actions in order.
- Process, Material, and Hardware Checks
- Print Preparation or Part Design Adjustments
Process, Material, and Hardware Checks
If any of these conditions apply to your print, take the corrective action and reprint to see if the problem is resolved.
Print Preparation or Part Design Adjustments
The following solutions will address print or part-related causes of the defects. Choose among the suggested actions below and select the best approach for your application. Usually only one type of adjustment is needed.

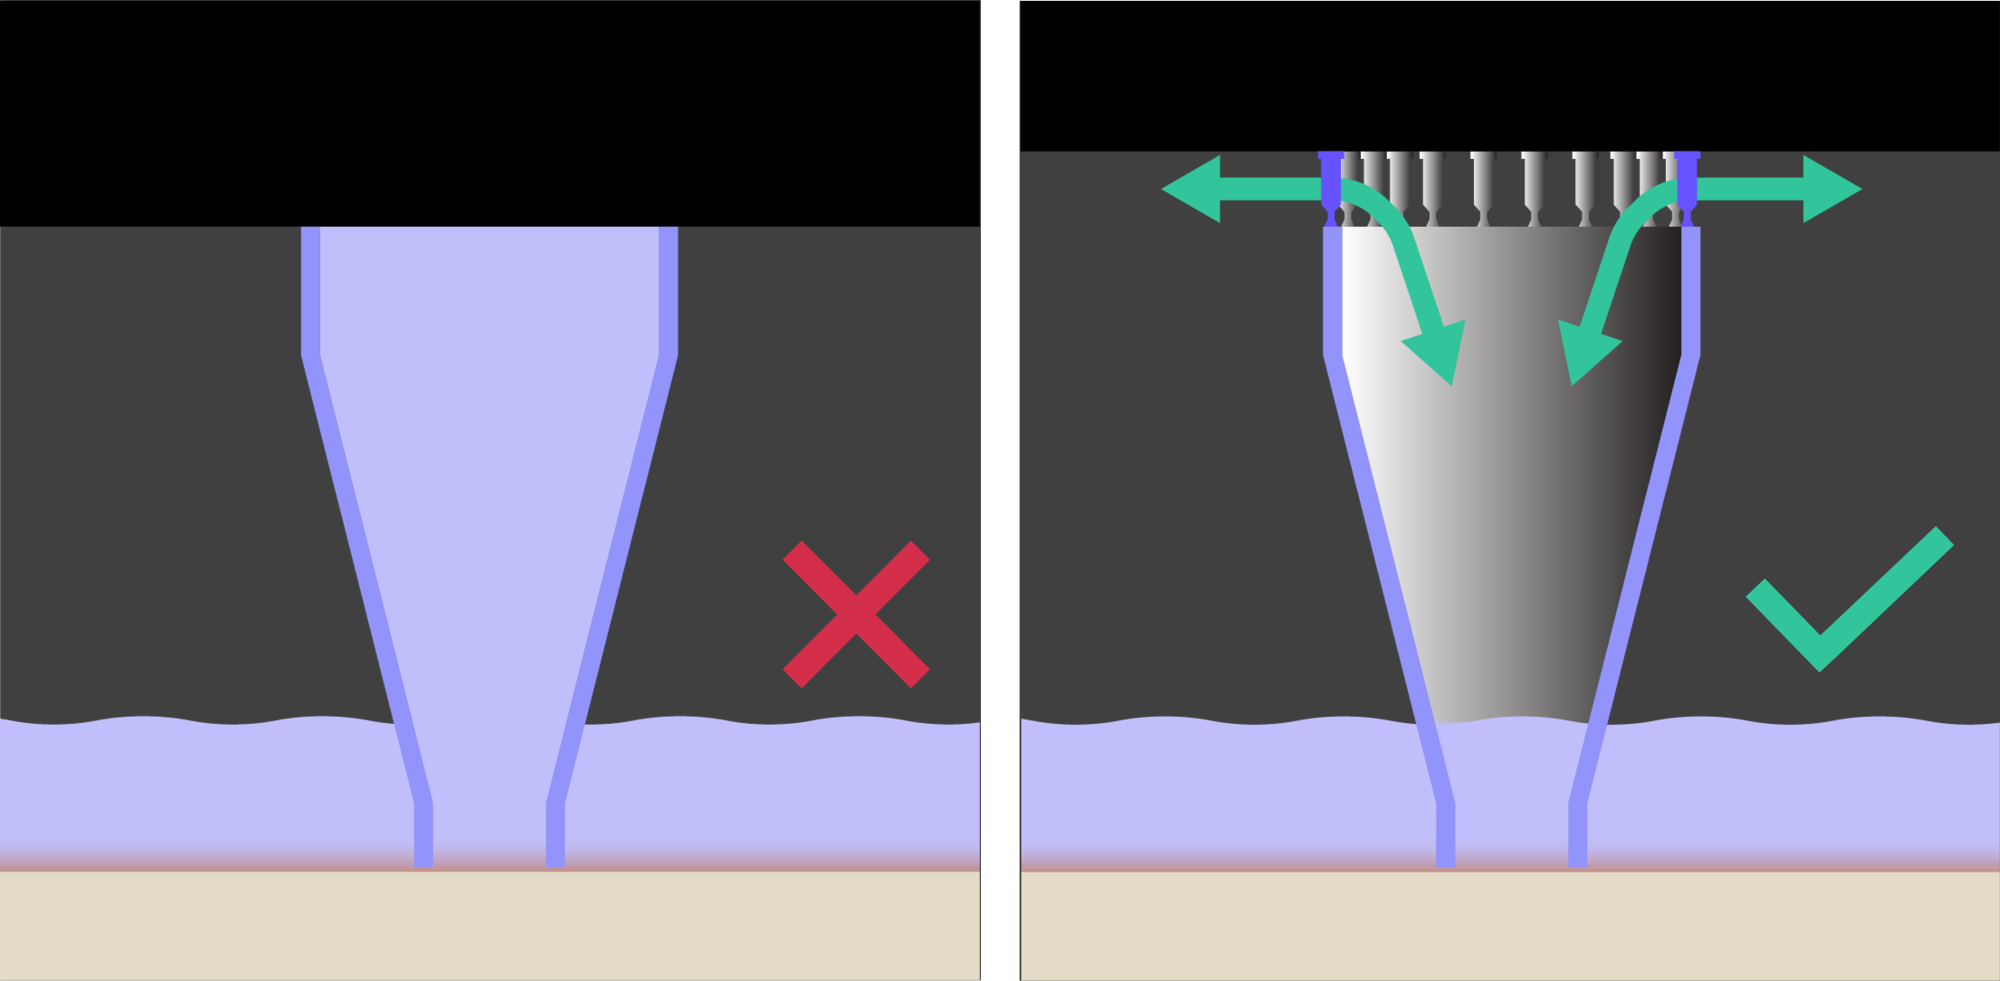
- Unvented volume
- Lift the part above the platform on supports to vent the trapped volume
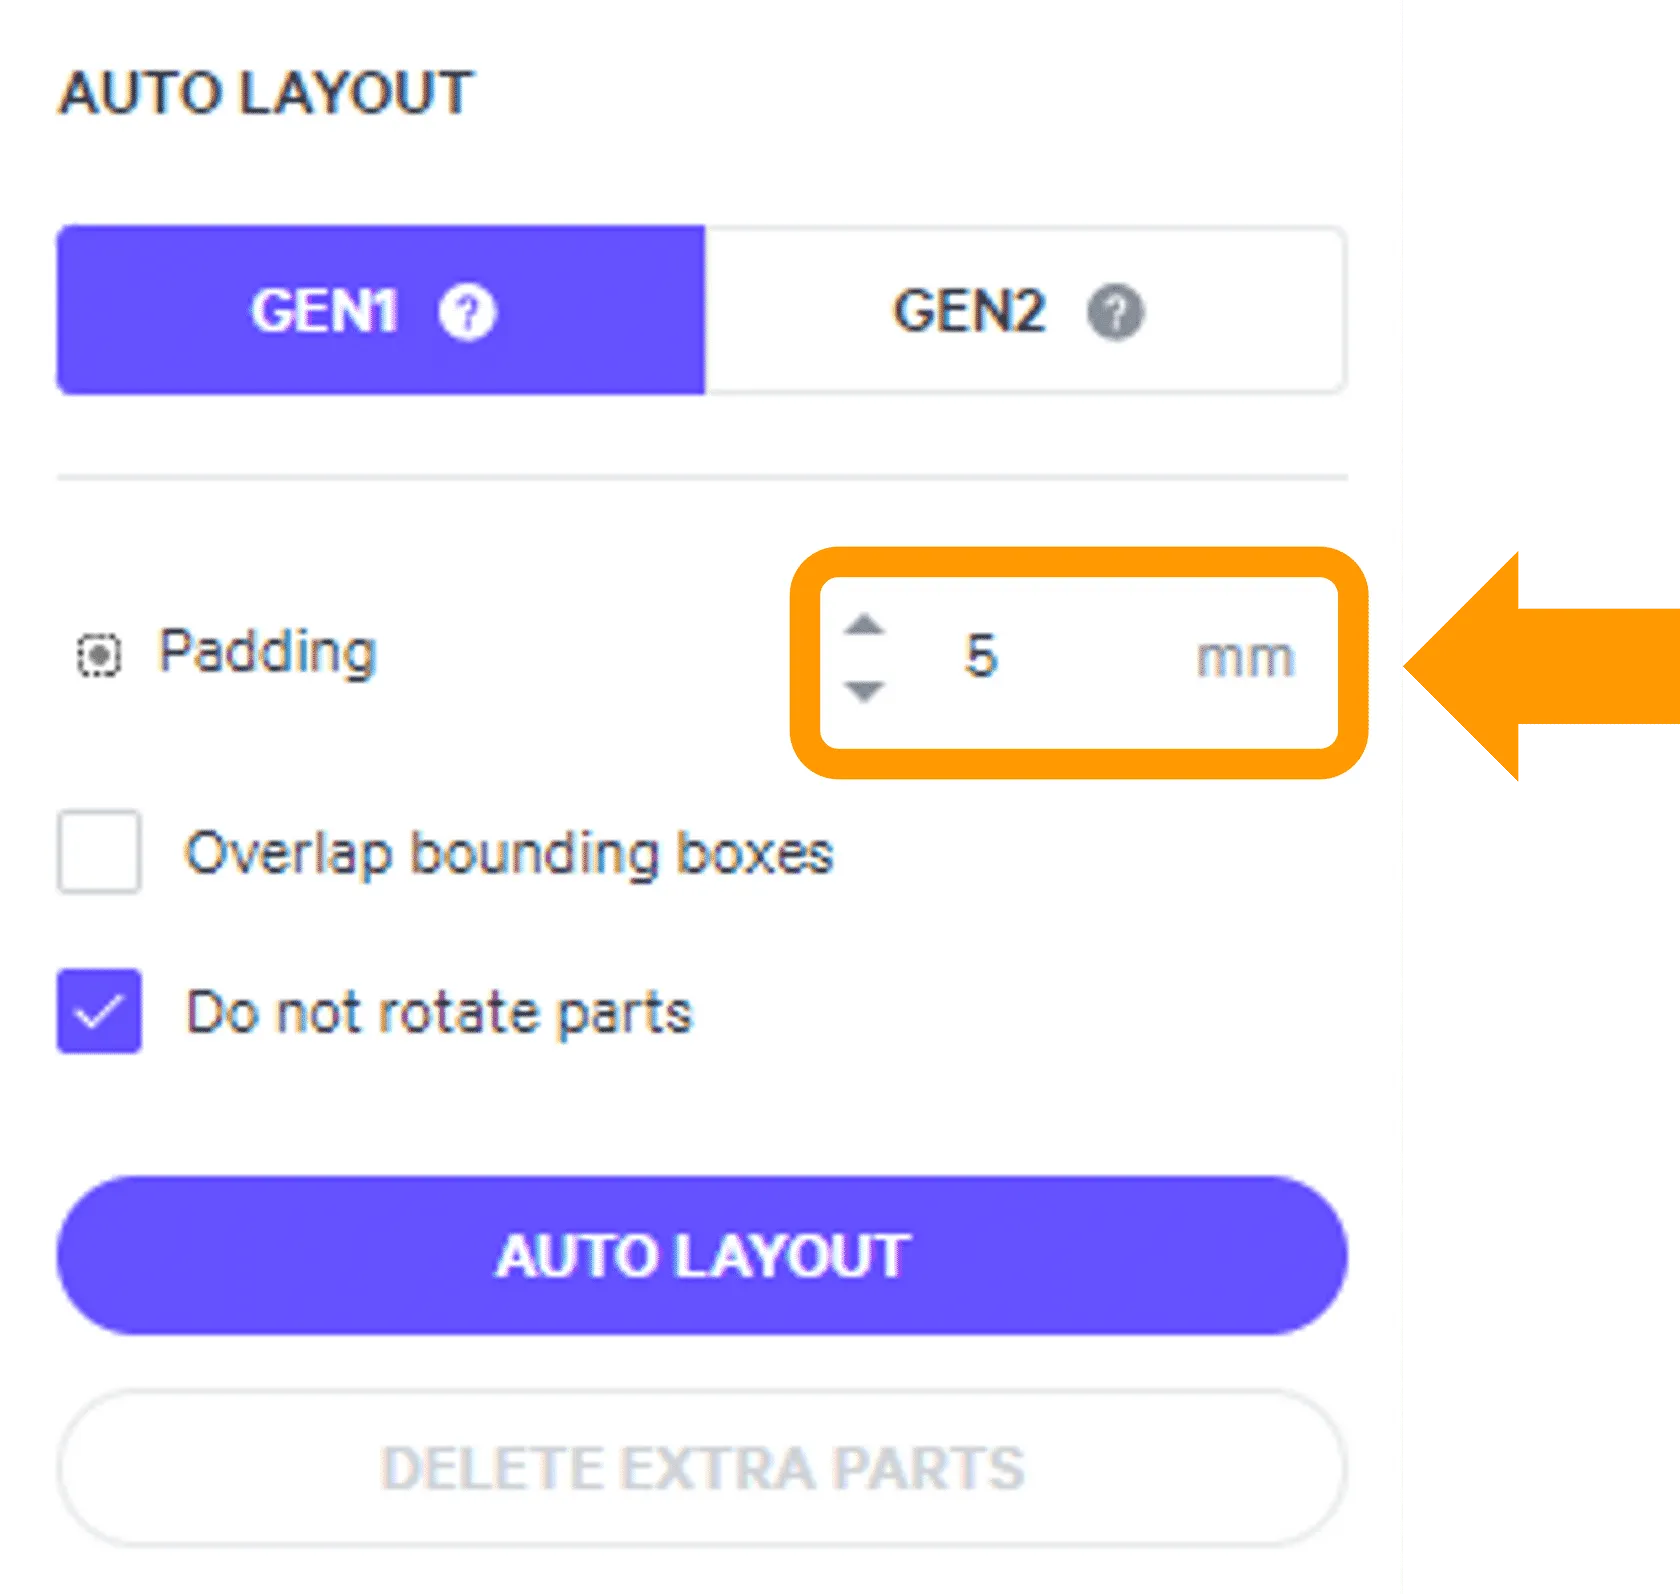
Add more space between parts; increase padding in auto-layout.
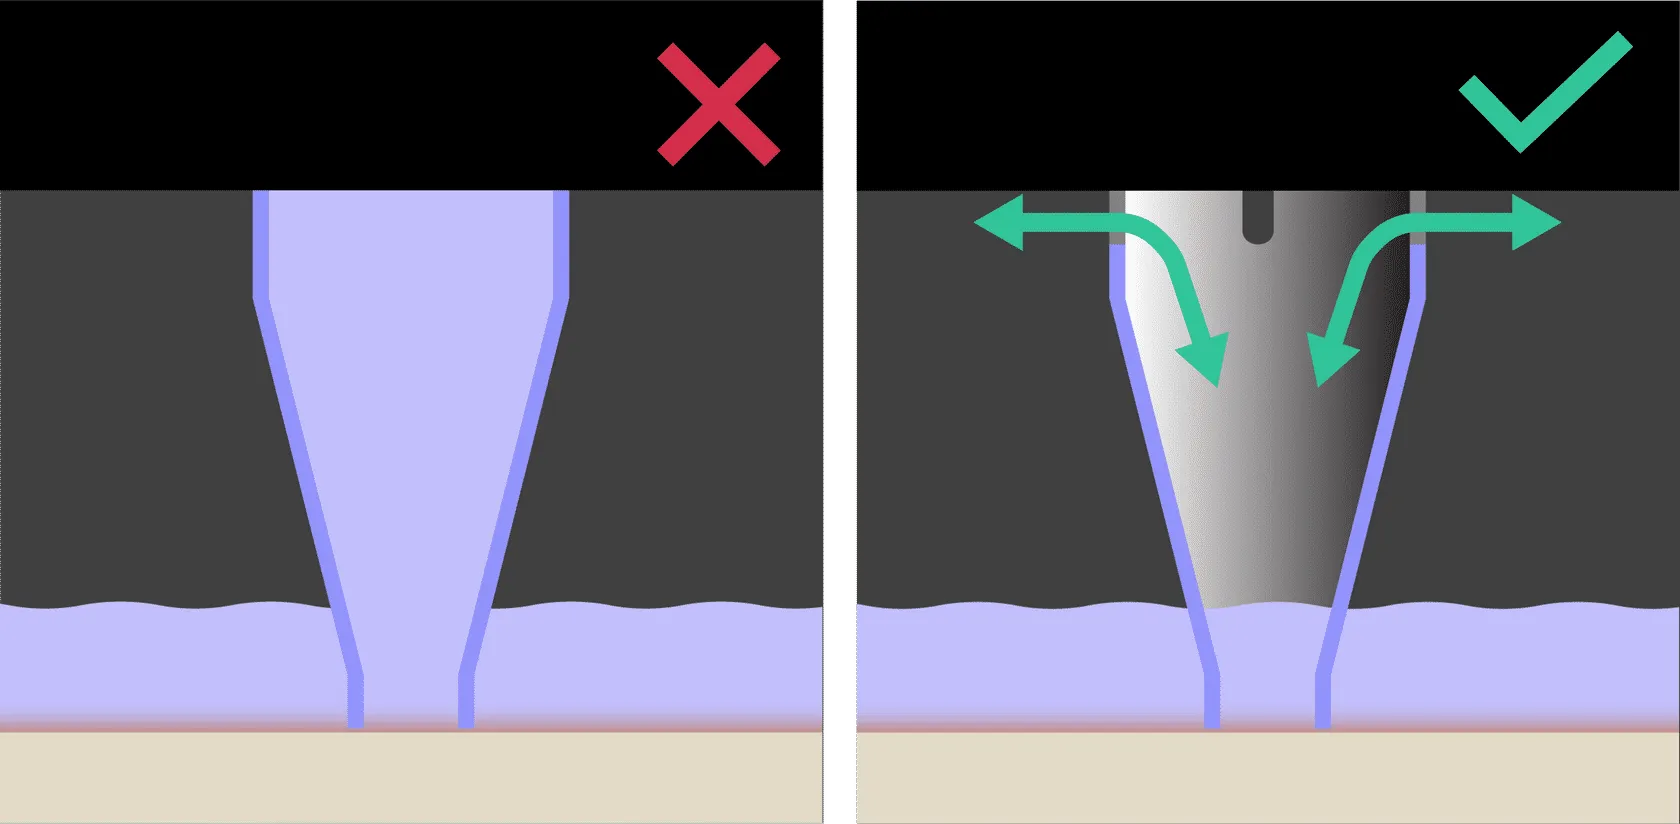
- Unvented Volume
- Add vent holes in the part, at or near the platform, to vent the trapped volume
Reference DLS Design Guidelines for drain/vent hole guidelines.
Default
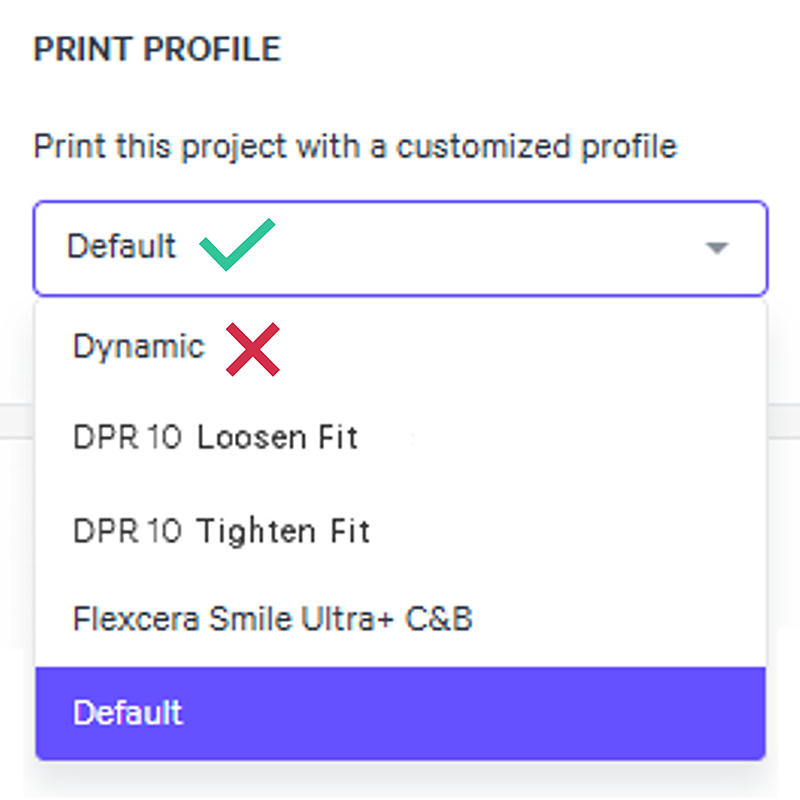
Print using the Default print profile instead of Dynamic to slow down the print. Reference Print Profile.
- Dynamic is a tool for M1 and M2 printers.
- Force feedback (FFB) printers (M3, M3 Max, L1) will see minimal to no difference in print speed with the dynamic print profile, so this troubleshooting option is unlikely to help.
If problems persist, please reach out to Carbon Support.
Explanation & Causes
Explanation
Normal printing requires resin flow to reach the center of the part. This is also known as reaching the deepest pixel. Voids occur when resin does not reach the center. This can happen for a couple of reasons:
- Resin does not have time to completely cover each layer.
- Resin is more viscous than the print planner expects.

Causes
- Print Preparation or Part Design
- Resin
- Print Plan Adjustments
Print Preparation or Part Design
How the part is oriented, supported, or designed is causing the defect.

Root Issue | Problem | Why Defect Presents |
Large Cross Section | | Resin must travel far to reach the deepest pixel and may not enough time to do so. |
Unvented Volume | | Unvented volumes can cause restricted resin flow. |
Layout | Parts are too close together. | If parts are packed too close together, resin flow may be restricted and not reach all parts equally. |
Print Profile | Print too fast in Dynamic | A shortened print gives less time for resin flow to all areas of the build. For M1 and M2 printers |
Resin
Resin
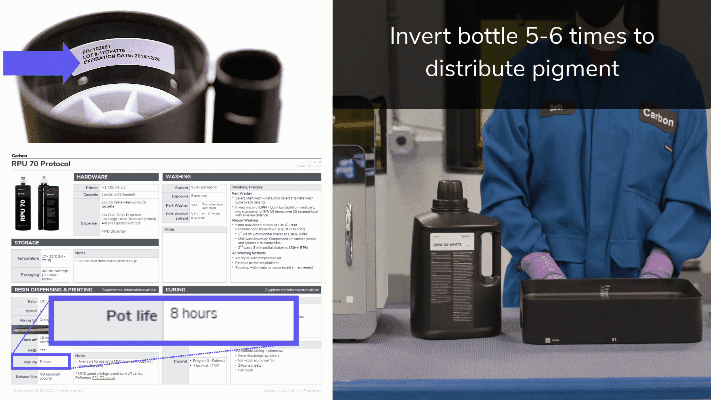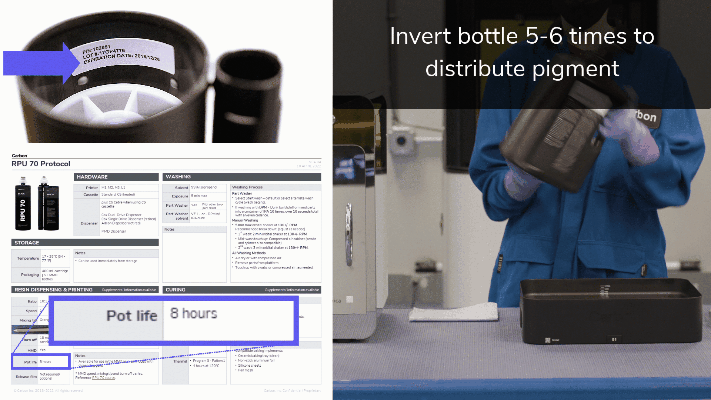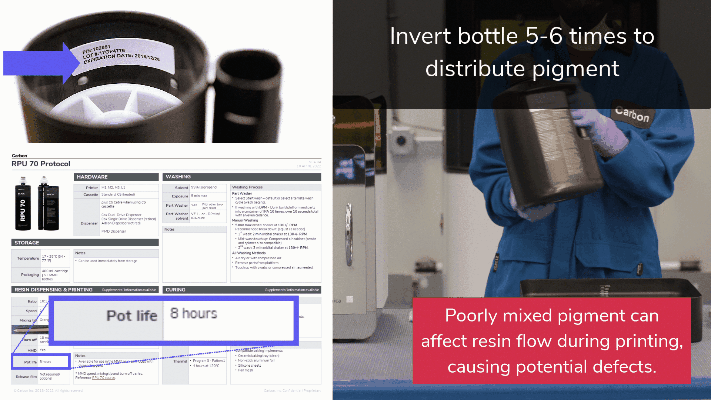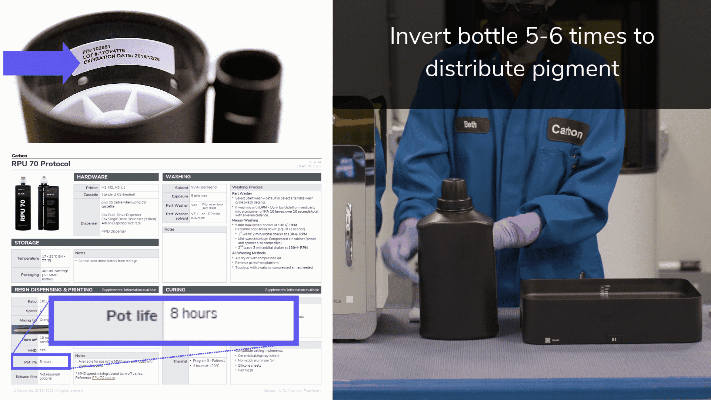
The printing material is expired, beyond the printing range in its pot-life, or has been improperly mixed, causing abnormalities in the print.
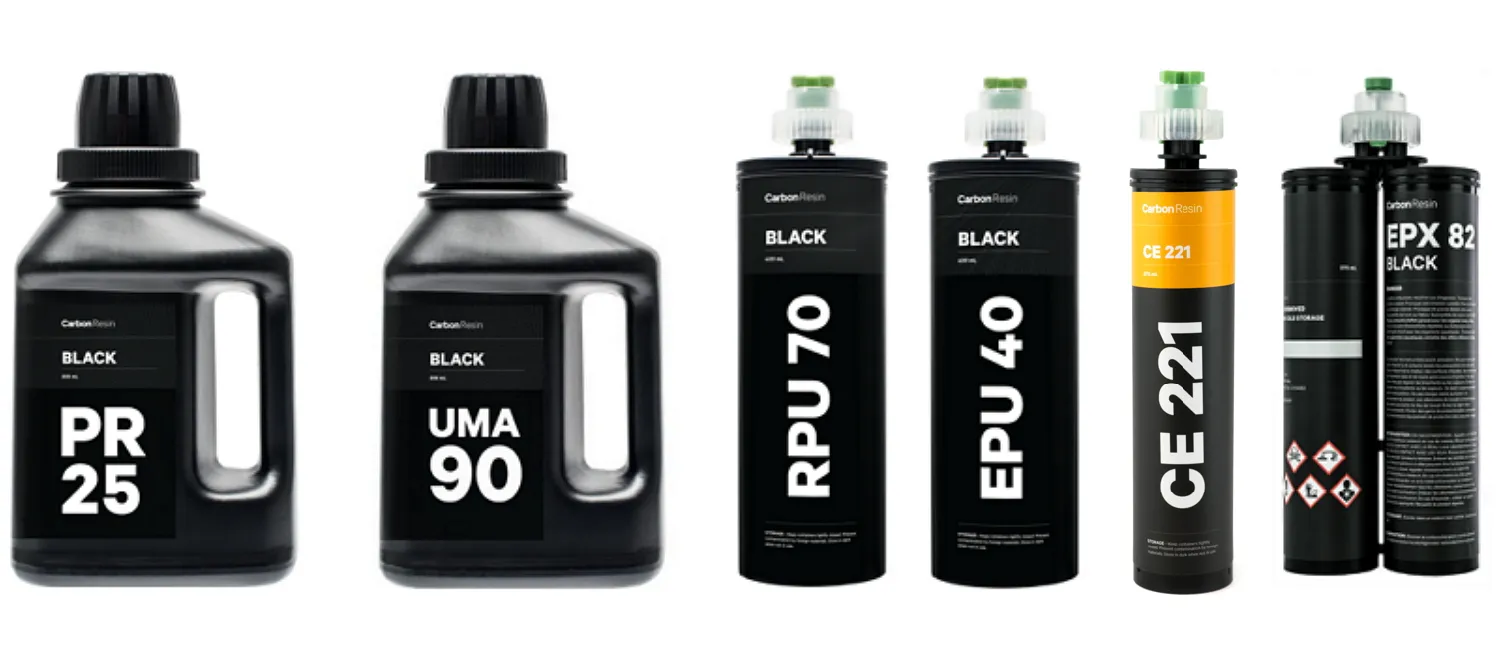
Root Issue | Problem | Why Defect Presents |
Expired | Resin may not be flowing properly. | If resin is too thick to flow as expected, the print plan may not allow enough time for the resin to reach the deepest pixel. |
Print Plan Adjustments
Print Plan Adjustments
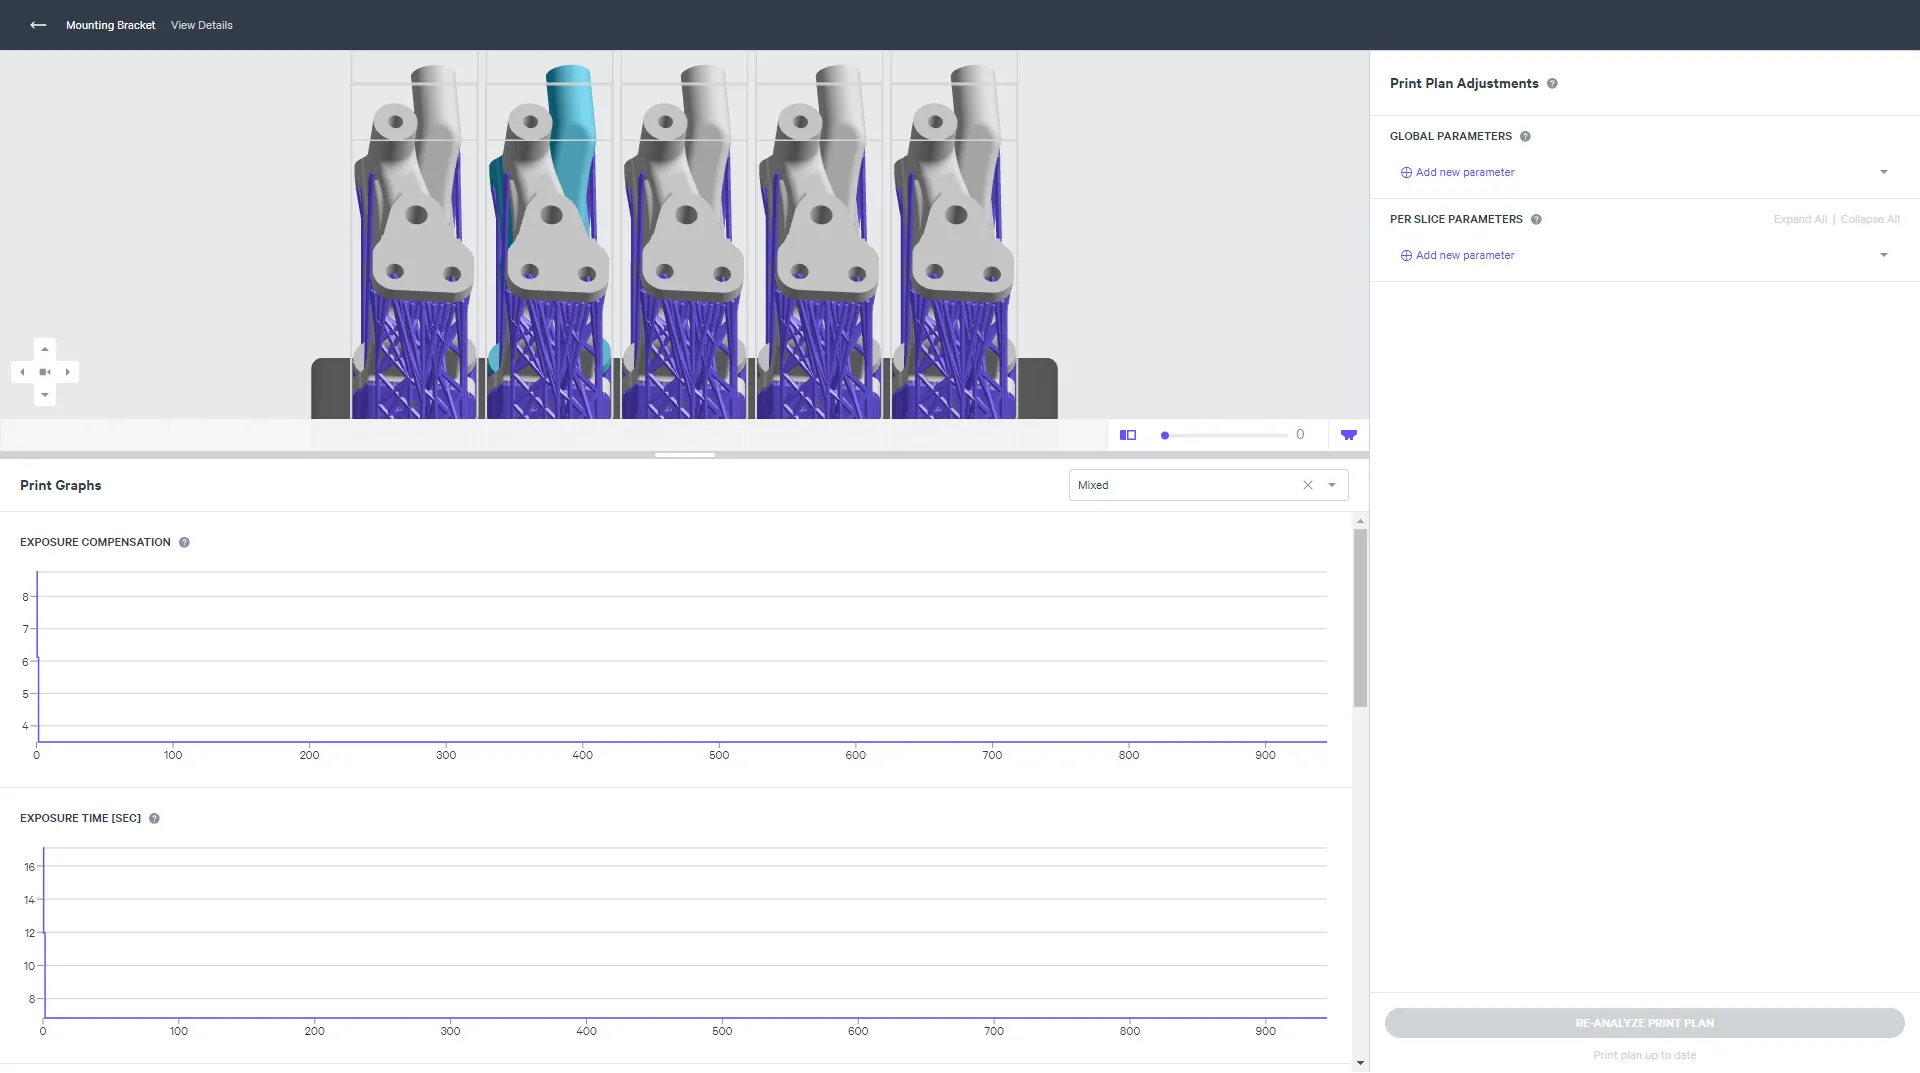
Print Plan Adjustments adjust the print plan to optimize mid to high volume production and/or address part defects.
In doing so, adjustment may both prevent or cause defects. Below are adjustments that can cause this defect.
Printing Stage | Parameter Type | Type of Adjustment | Why Defect Presents |
1 Pump Up | Pump Height | Decrease | A decrease in the pump height can limit how much resin can flow. |
2 Settle Up | Delay Timing | Decrease | A shortened settle up stage limits the amount of time resin can flow. |