Shift Lines
Shift Lines
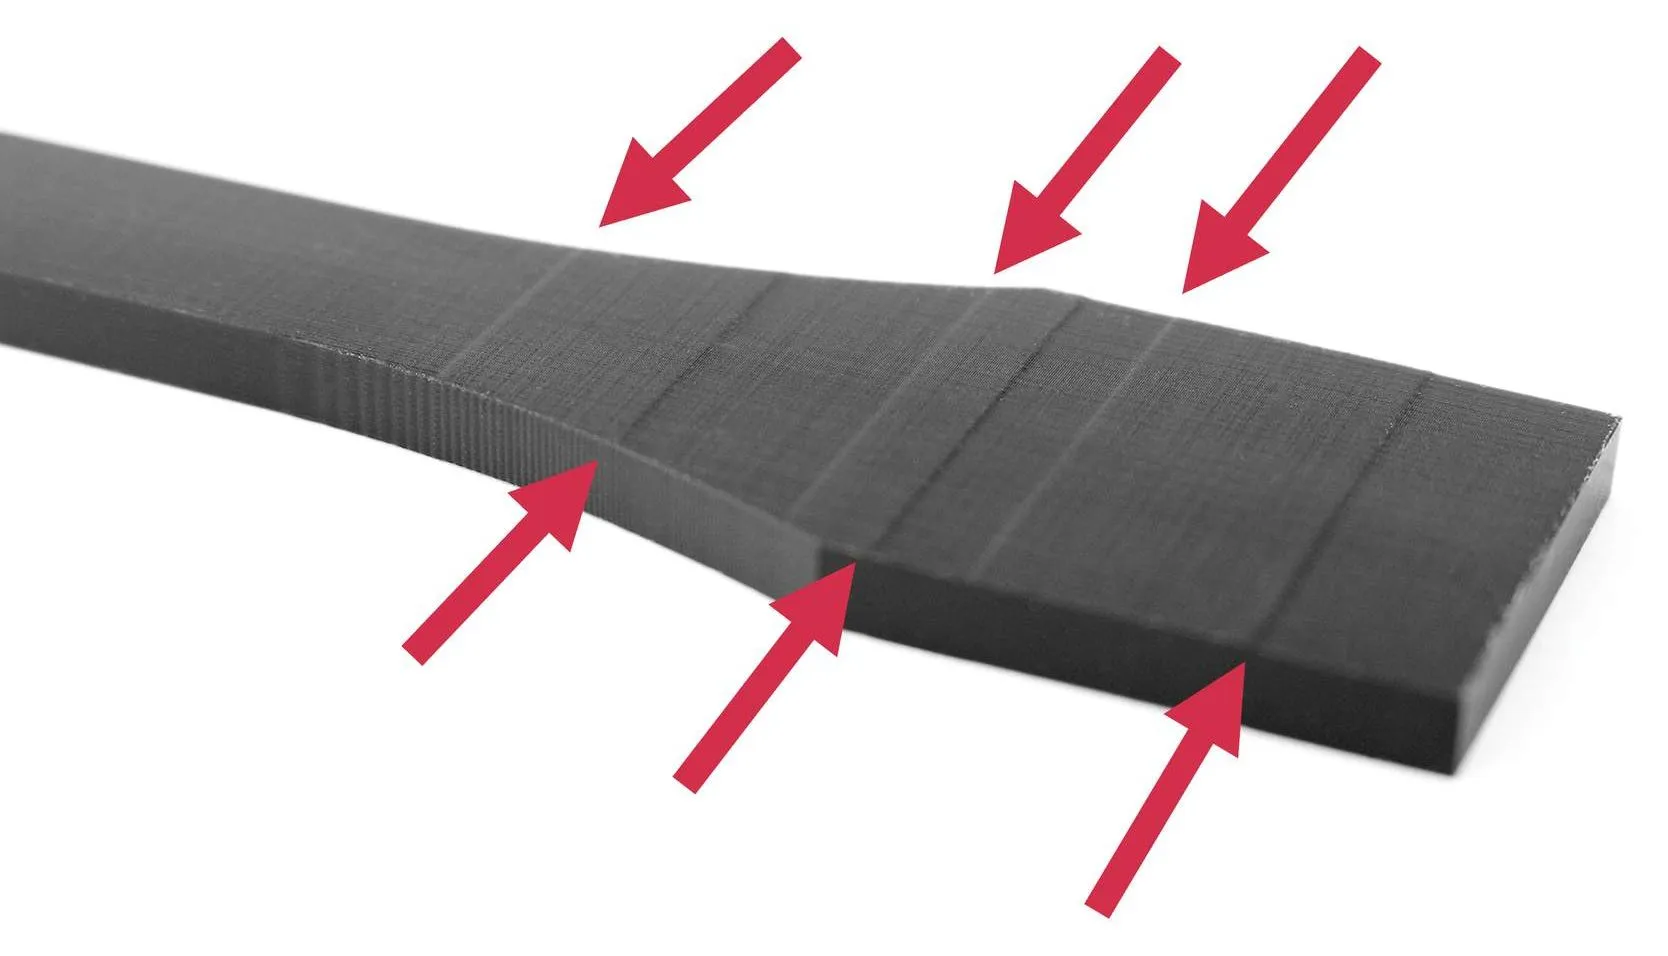
Shift lines can occur when parts move during printing.
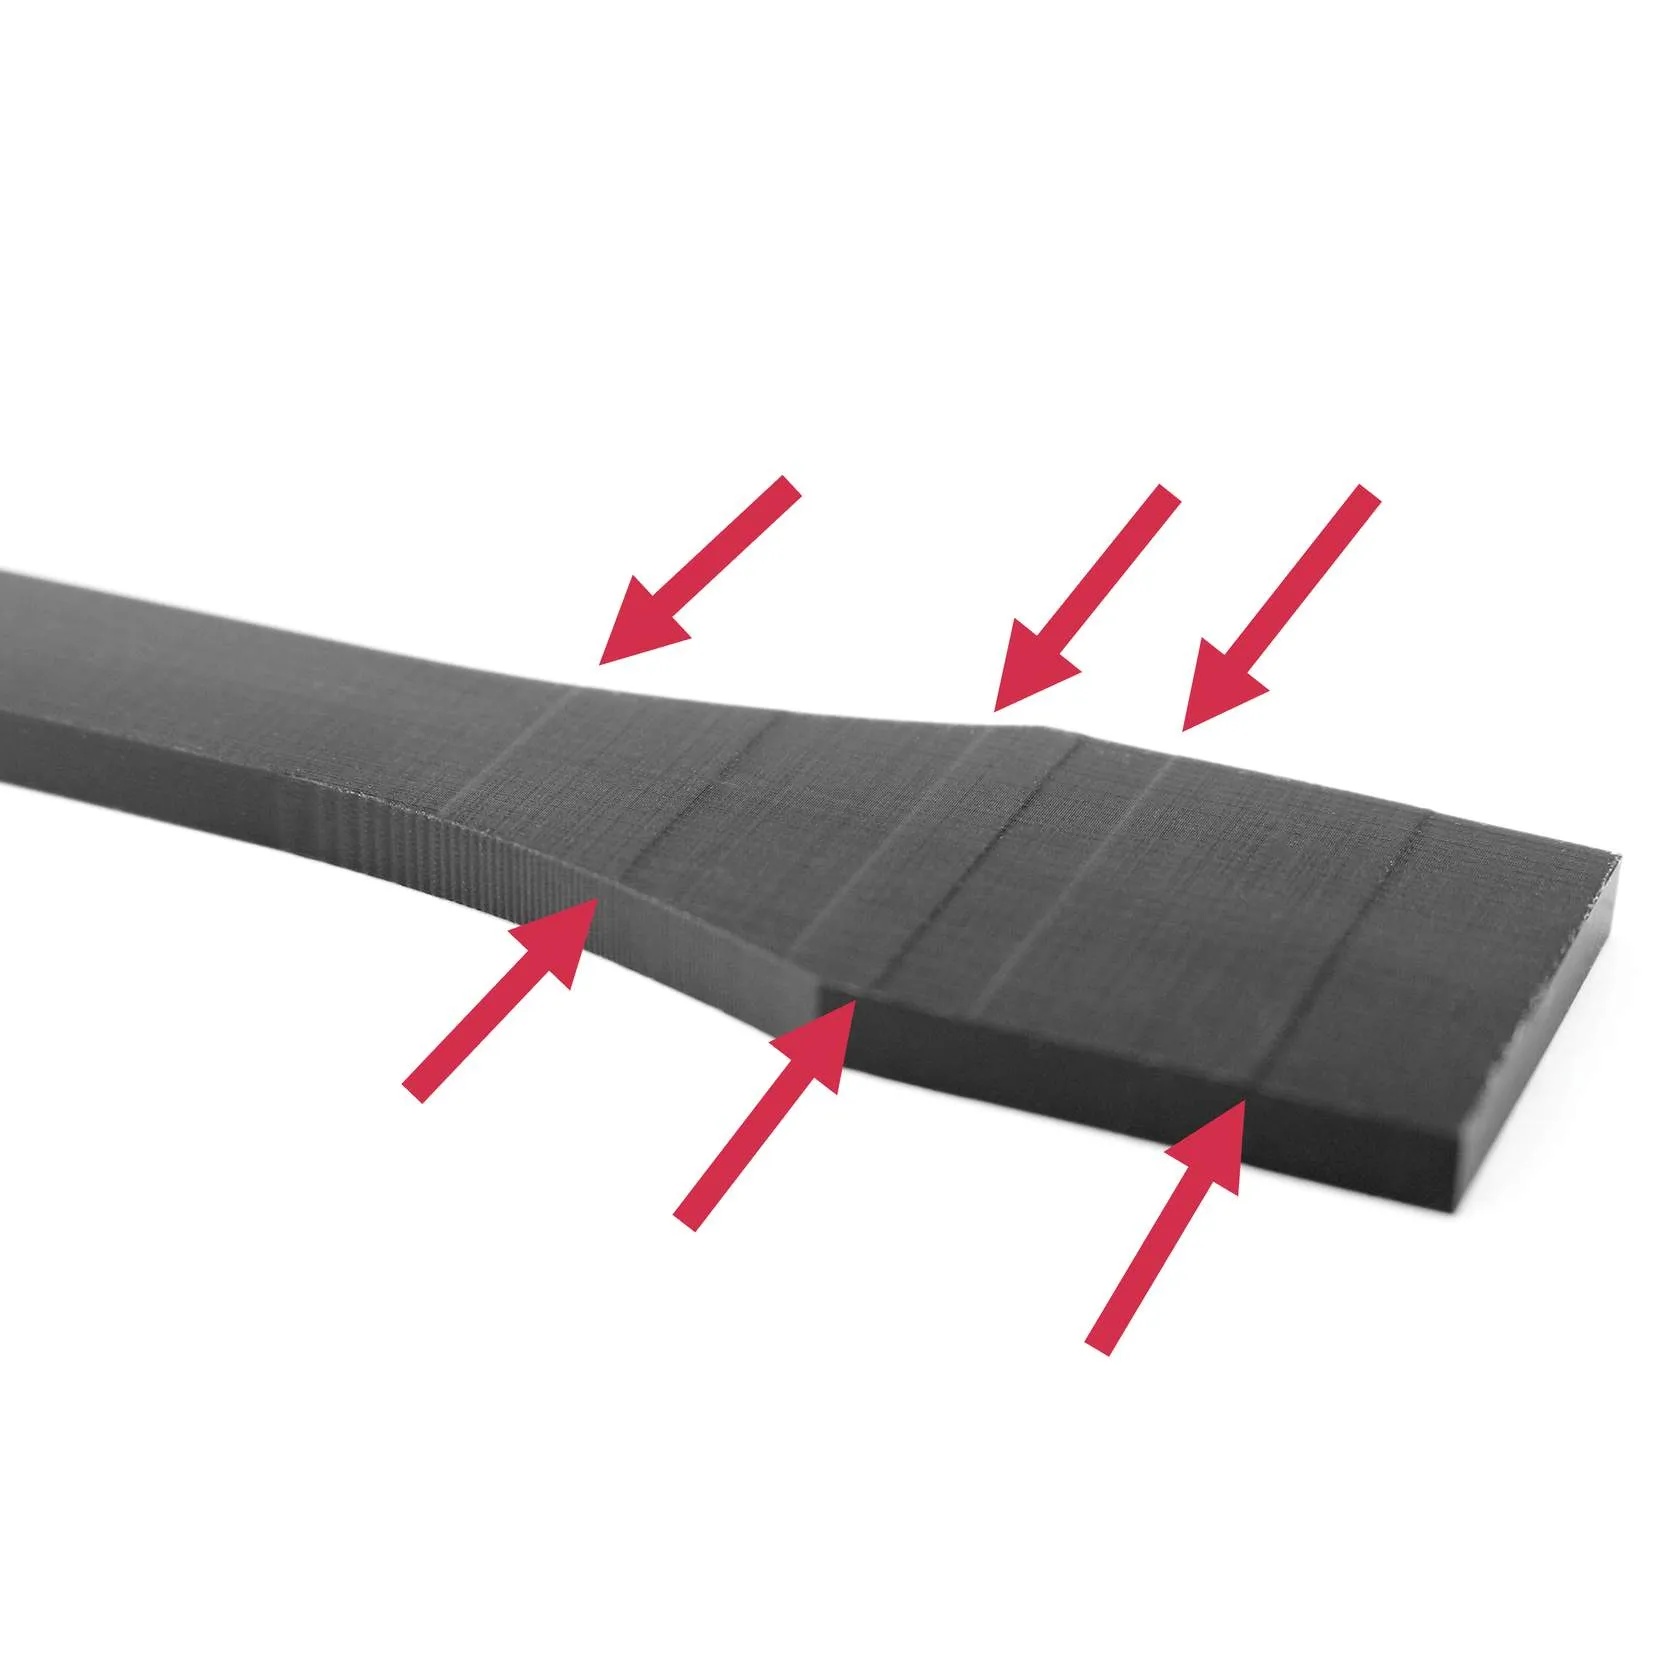
How to Identify
Shift lines can be diagnosed as follows:
- Lines or bands appear horizontal, or parallel to the build platform.
- Shift is directional: Lines appear proud on one side and recessed on the opposite side of the part.
- Lattice struts may not connect properly.
- No material will be missing, just misplaced. This is a key difference from Layering which may appear similar.
Cause - Instability
Solution - Print Preparation or Part Design
Cause - Instability
Solution - Print Preparation or Part Design
Cause - Unknown
Troubleshooting
It is recommended that you review all the possible solutions before taking action to ensure you are pursuing the best course of action.
If the best course of action is not apparent, try the troubleshooting options in the order listed. Refer here for more tips.
Process, Material, and Hardware Checks
If any of these conditions apply to your print, take the corrective action and reprint to see if the problem is resolved.
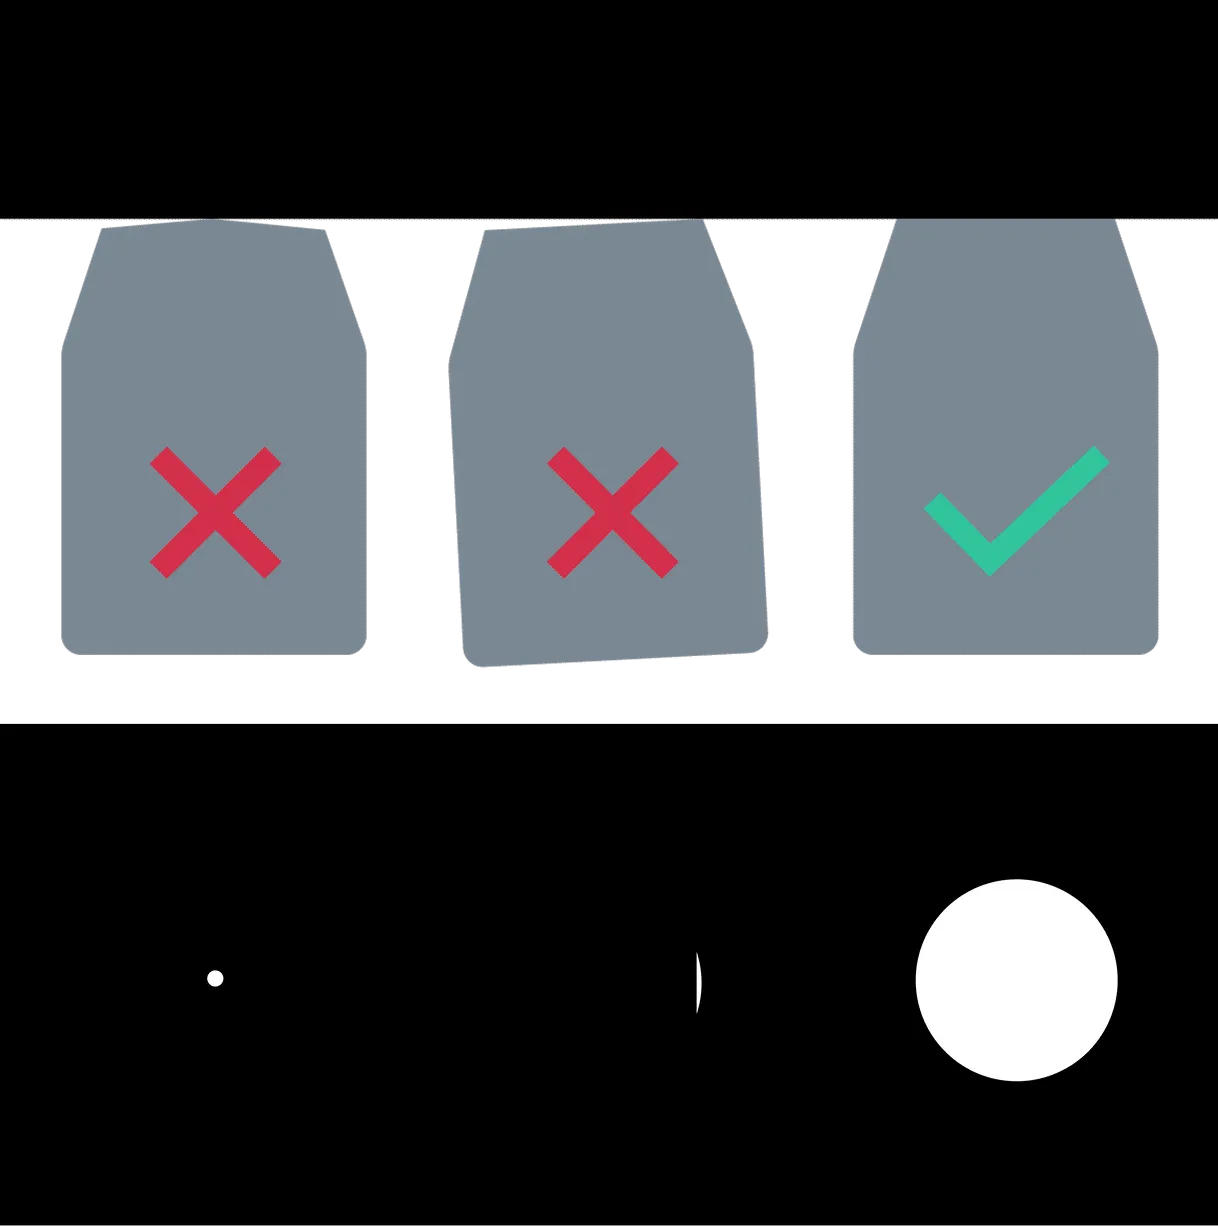
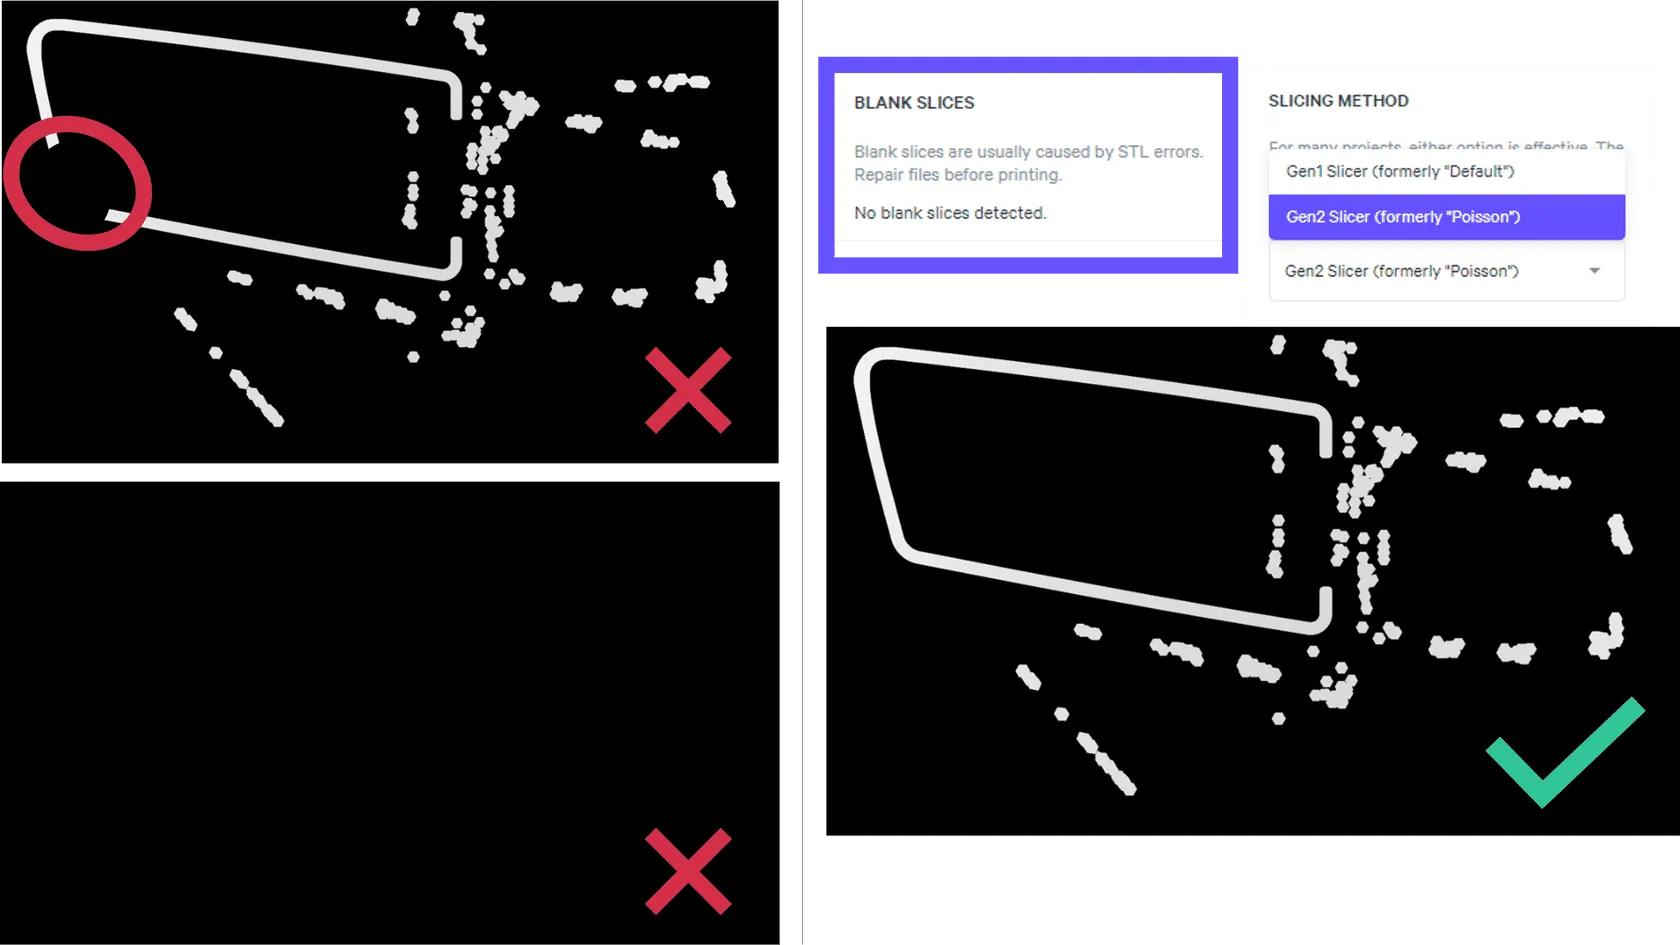
- Check for bad slices
- Look for areas missing in the slice where the defect occurs
- Repair the slicing if bad slices are found
- Repair the part in an stl repair program

Print Preparation or Part Design Adjustments
The following solutions will address print or part-related causes of the defects. Choose among the suggested actions below and select the best approach for your application. Usually only one type of adjustment is needed.


If problems persist, please reach out to Carbon Support.
Explanation & Causes
Explanation
Shift lines occur from instability during printing as a result of print forces and resin moving. When a part is unstable, printing forces can move the part out of position such that when the next slice cures, the slices do not line up properly.
- Parts especially prone to shift movement:
- Tall, thin parts.
- Parts with the center of mass far from the platform and/or off-center with the base slices.
- EPU parts (due to low stiffness).
Shift lines are more common on older printers and less likely on newer models. In order from more likely to less likely:
- M1
- M2
- L1
- M3/ M3 Max
Causes
Print Preparation or Part Design
How the part is oriented, supported, or designed is causing the defect.

Root Issue | Problem | Why Defect Presents |
|---|---|---|
Slices | Flat base not snapped to platform | The part is rotated slightly such that the platform cross section is not fully adhered. Without a stable base, the part can move during printing. |
Slices | Bad slice | A slice or part of a slice is missing which makes the part unstable without its geometry full intact. |
Cross Section | Small to large cross section later in the print | Forces increase later in the print from large cross sections and this can move the part. |
Unstable Geometry | Asymmetrically oriented part | Parts that are susceptible to lateral forces can move during printing. |
Unstable Geometry | Parts with the center of mass far from the platform | Parts that are susceptible to lateral forces can move during printing. |
Tall, Thin Part | | Tall thin parts are inherently less stable and can move if not prepped for printing properly. |
Hardware
The printer, cassette, or platform is dirty or requires maintenance to resolve the defect.
Occasionally, a defect may indicate the printer requires servicing by a Carbon engineer.
Root Issue | Problem | Why Defect Presents |
|---|---|---|
Misalignment | Improper seating | M1 and M2 printers rely on kinematic mounts to keep the part platform properly positioned and stable. If the platform in not seated properly on these mounts, the platform itself can move which in turn moves the part during printing. |
Print Plan Adjustments
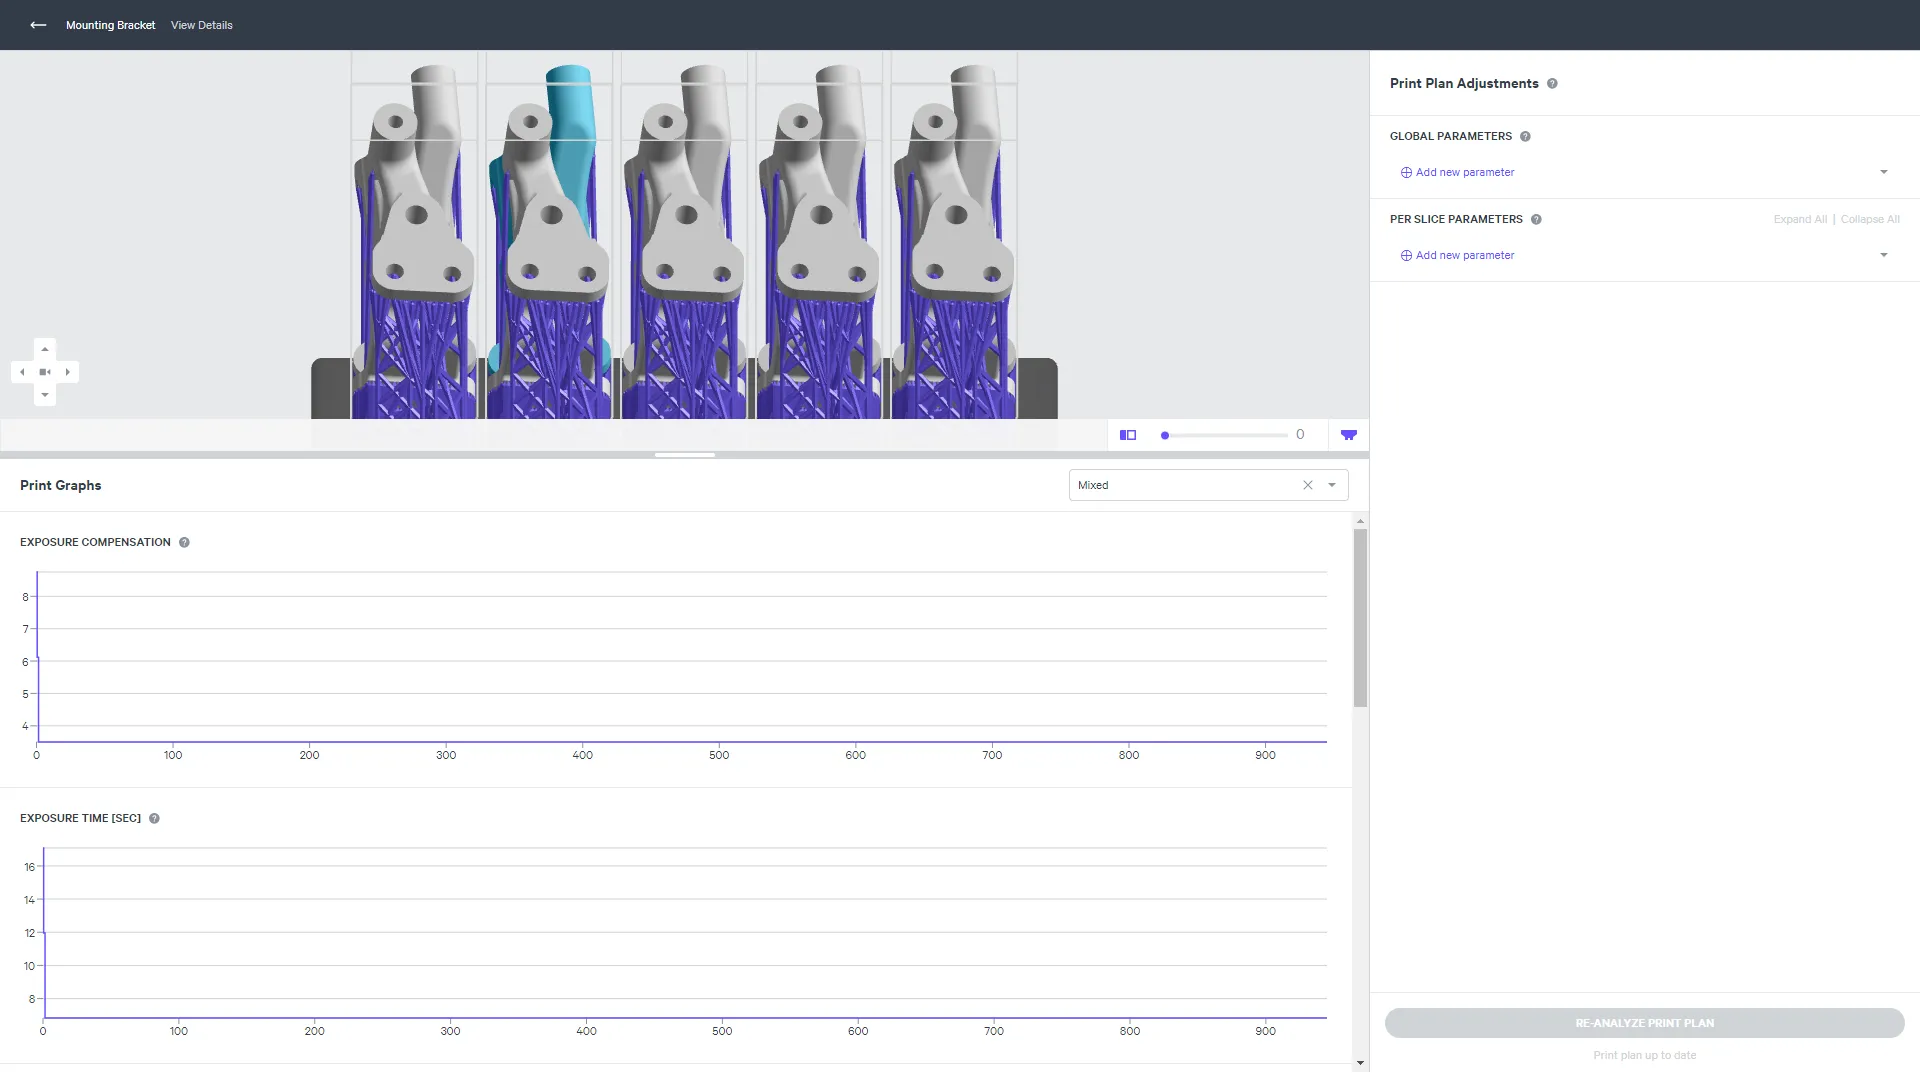
Print Plan Adjustments adjust the print plan to optimize mid to high volume production and/or address part defects.
In doing so, adjustment may both prevent or cause defects. Below are adjustments that can cause this defect.
Printing Stage | Parameter Type | Type of Adjustment | Why Defect Presents |
|---|---|---|---|
3 Pump Down | Platform Speed | Increase | Increased Motor Down Speed increases forces on the part as it moves down to the curing position. |