Caping
Caping
Capes or sheets of resin form on and between parts/features
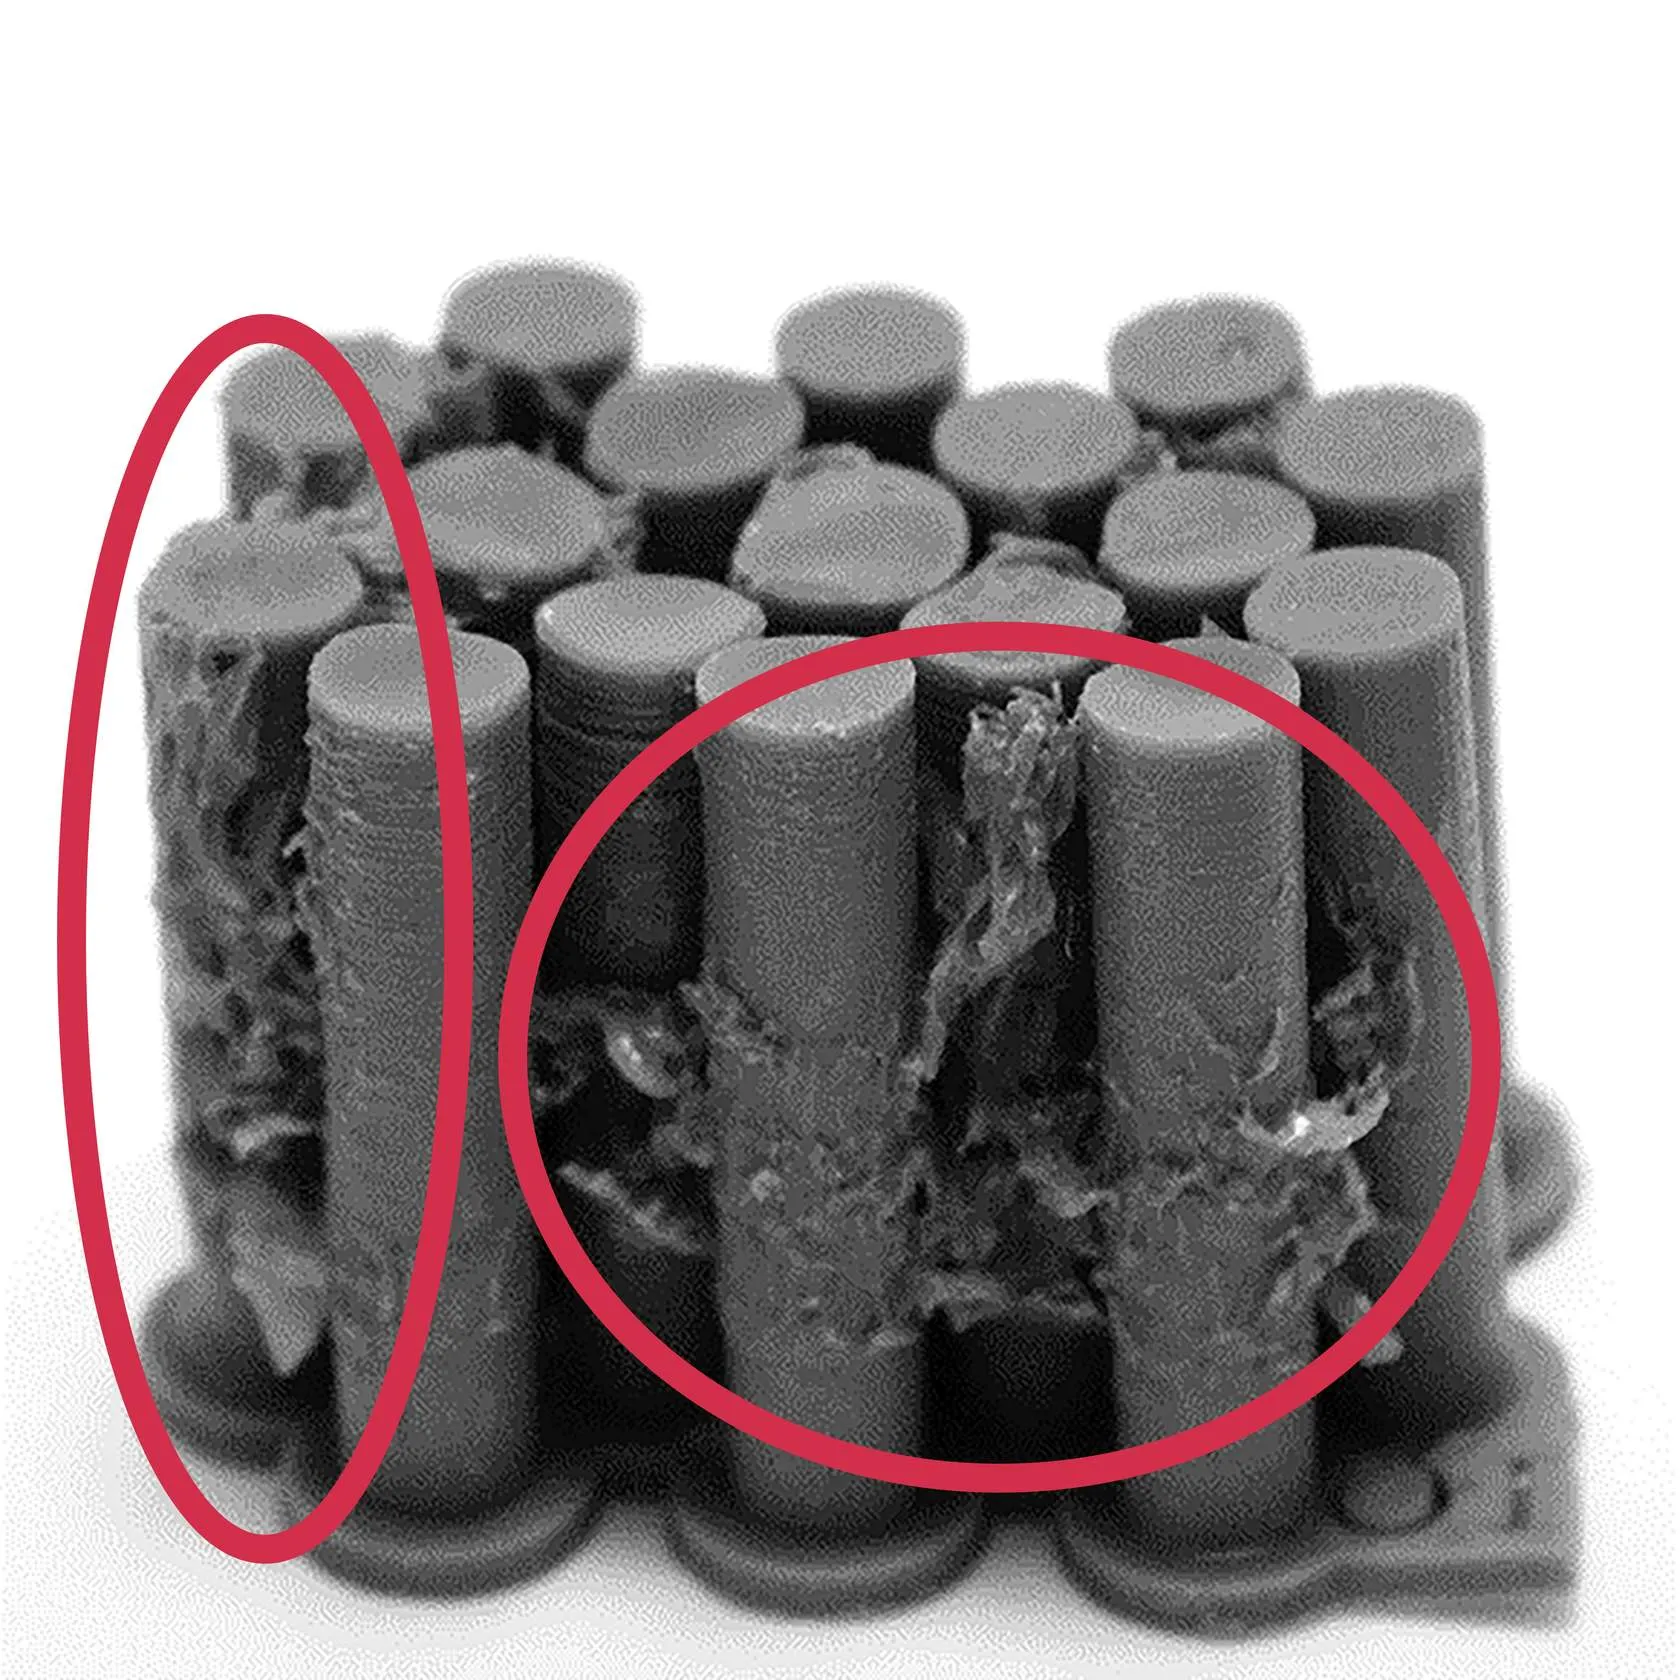
How to Identify
Caping can be diagnosed as follows:
- Irregularly shaped strands/sheets of cured resin on the exterior of and between parts on the build.
- This is an uncommon defect.
- This is an extreme form of Veining.
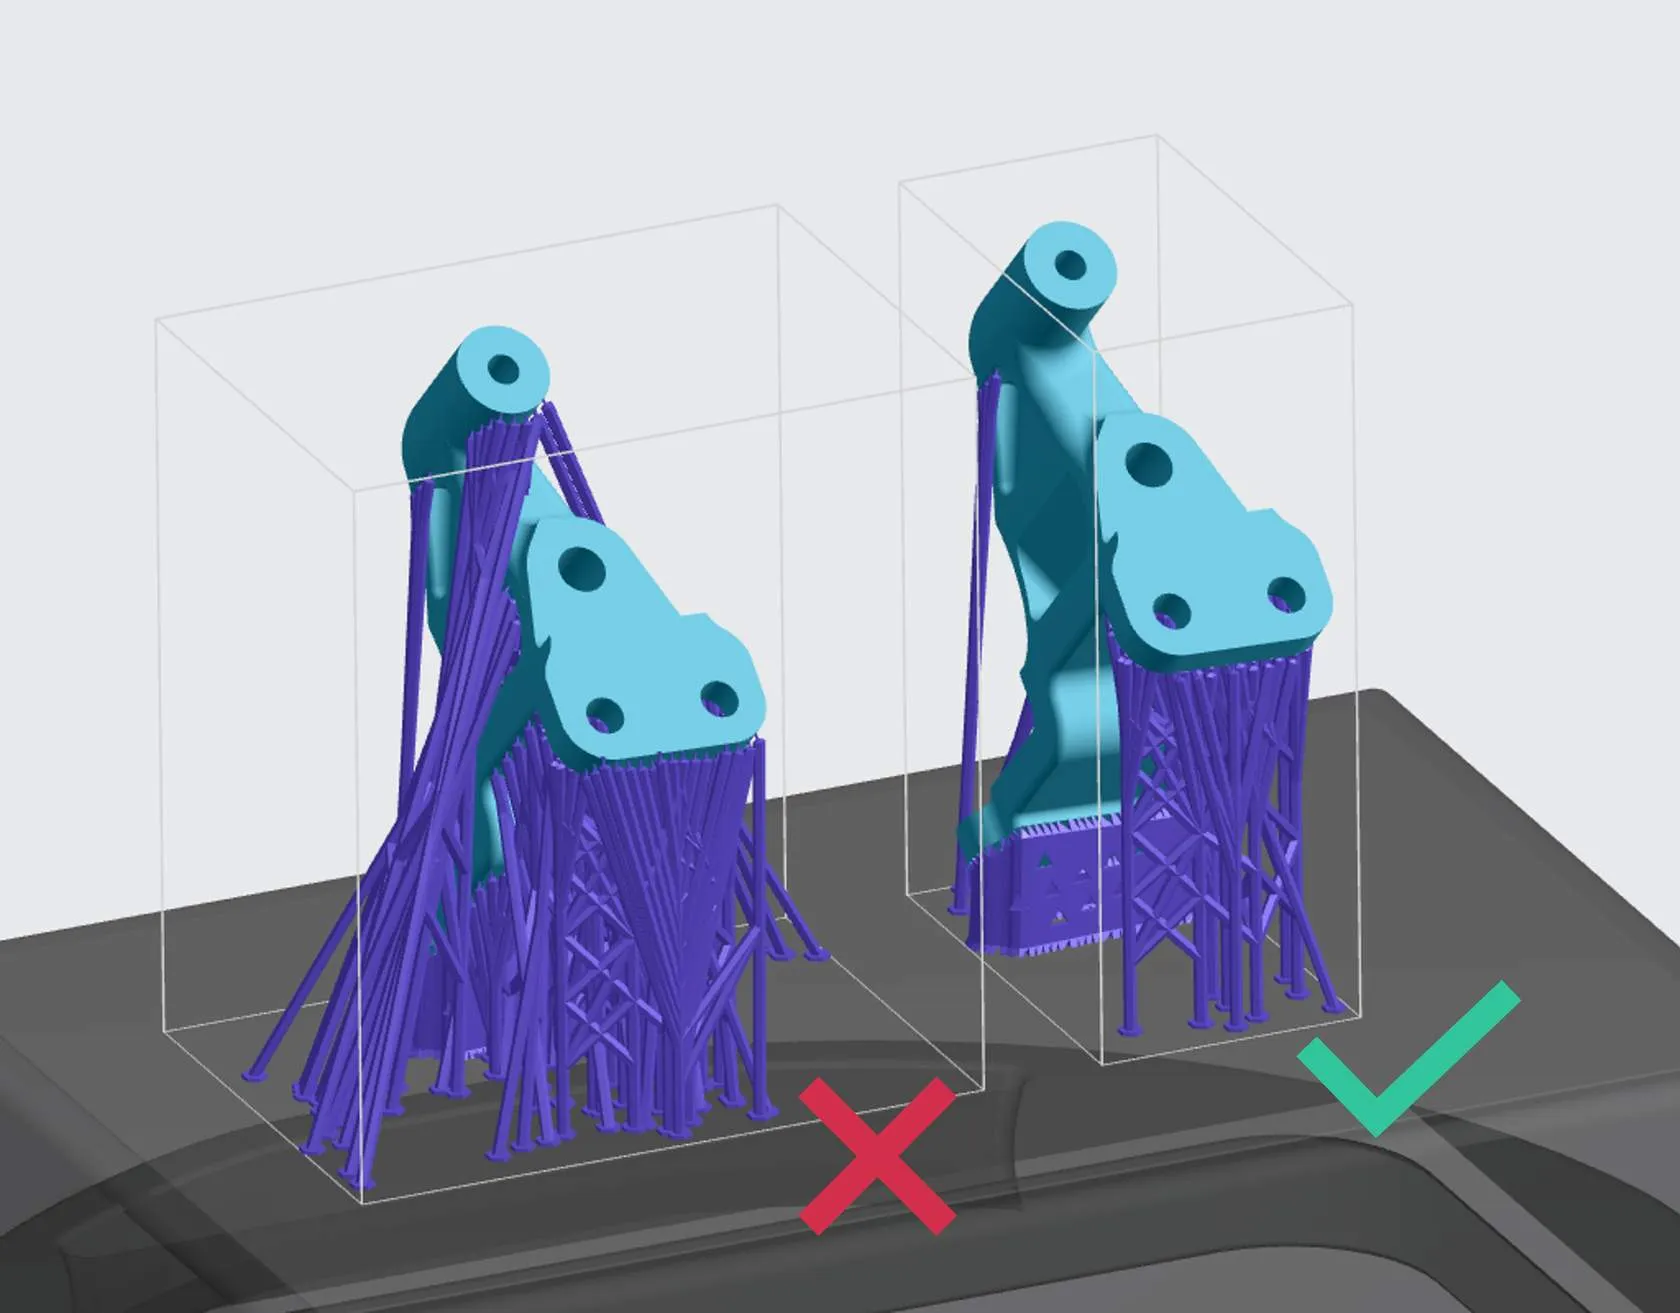
Cause - Layout
Solution - Print Preparation or Part Design
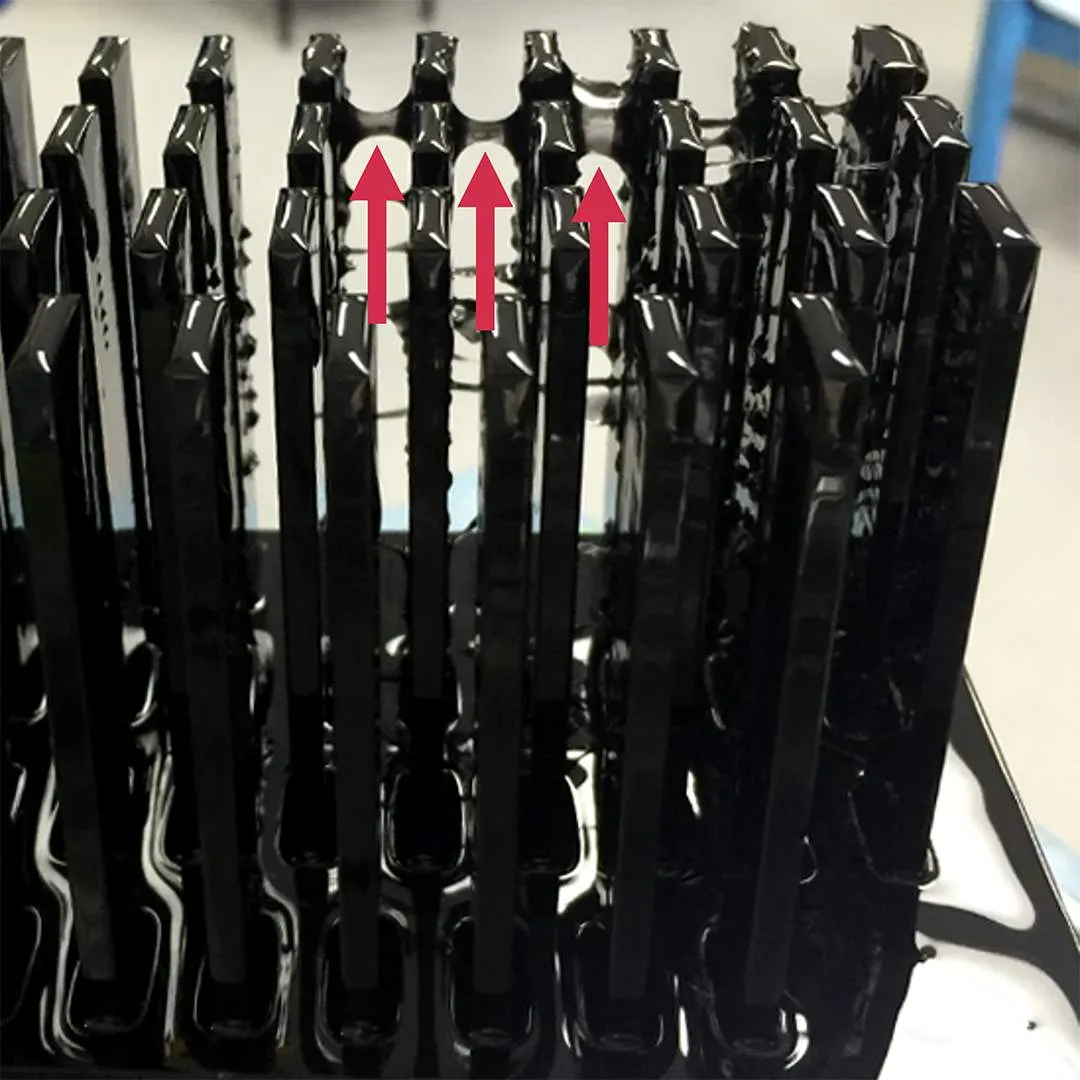
Cause - Inconclusive
Troubleshooting
It is recommended that you review all the possible solutions before taking action to ensure you are pursuing the best course of action.
If the best course of action is not apparent, try the troubleshooting options in the order listed. Refer here for more tips.
Process, Material, and Hardware Checks
If any of these conditions apply to your print, take the corrective action and reprint to see if the problem is resolved.


Diagnostics
If the above checks & actions did not resolve the issue or do not apply to your print, the following diagnostics may further inform what is causing the issue.
Print Preparation or Part Design Adjustments
The following solutions will address print or part-related causes of the defects. Choose among the suggested actions below and select the best approach for your application. Usually only one type of adjustment is needed.
If problems persist, please reach out to Carbon Support.
Explanation & Causes
Explanation
- Stray UV light partially cures a film of resin close to the window. That film eventually attaches to the part and is pulled up as the part builds.
- The build is not receiving the proper dosage of light and/or oxygen.
- Overheated resin disrupting the normal pigment concentration and disbursement.
Causes
Print Preparation or Part Design
How the part is oriented, supported, or designed is causing the defect.

Root Issue | Problem | Why Defect Presents |
|---|---|---|
Supports | Over-supported | Parts that are over-supported provide less space for resin to flow properly throughout the build causing light to scatter. |
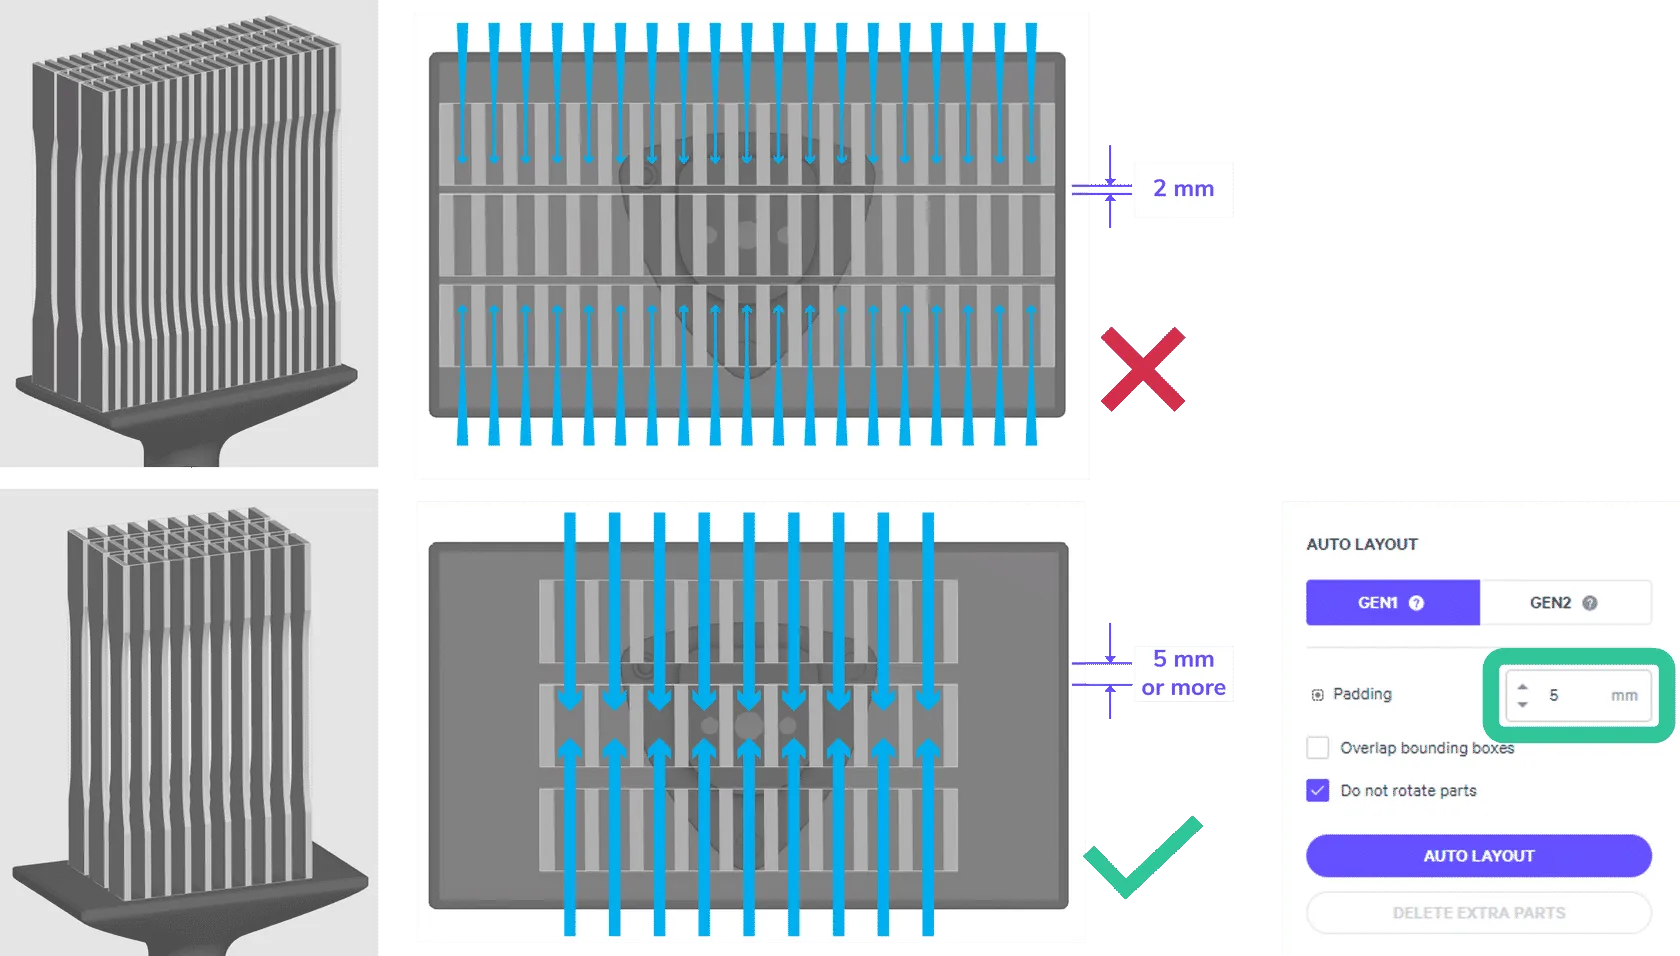
Layout | Parts too dense on platform | Padding between parts is to small for resin to flow properly throughout the build causing light to scatter. |
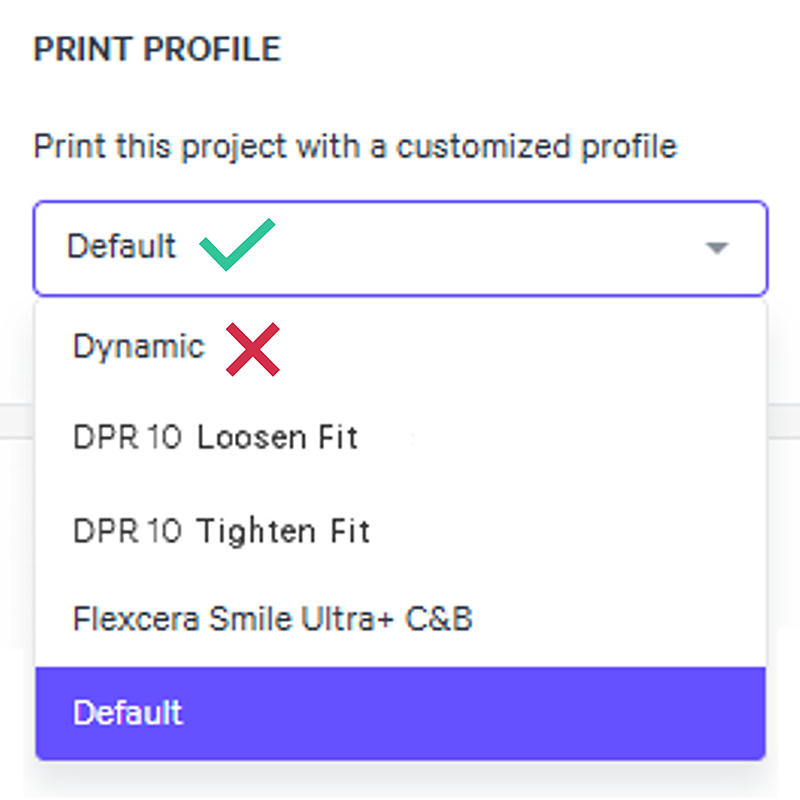
Print Profile | Print too fast in Dynamic | A shortened print gives less time for resin flow to all areas of the build causing light to scatter. For M1 and M2 printers |
Hardware
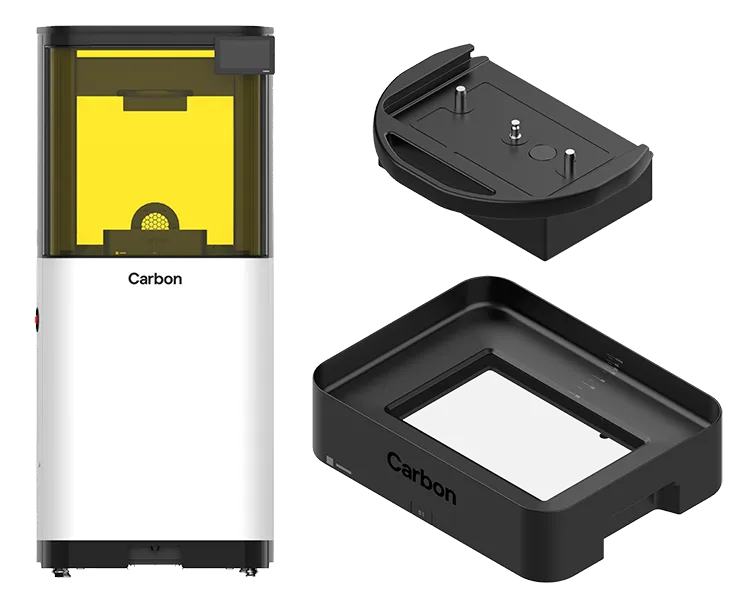
The printer, cassette, or platform is dirty or requires maintenance to resolve the defect.
Occasionally, a defect may indicate the printer requires servicing by a Carbon engineer.
Root Issue | Problem | Why Defect Presents |
|---|---|---|
Cleaning | Cassette window is dirty | A dirty or faulty cassette inhibiting regular light and oxygen flow. |
| Deck glass is dirty (M1/M2) | |
| Projector lens is dirty (M3/M3 Max/L1) | |
Window Damage | | A dirty or faulty cassette inhibiting regular light and oxygen flow. |
Resin
The printing material is expired, beyond the printing range in its pot-life, or has been improperly mixed, causing abnormalities in the print.
Root Issue | Problem | Why Defect Presents |
|---|---|---|
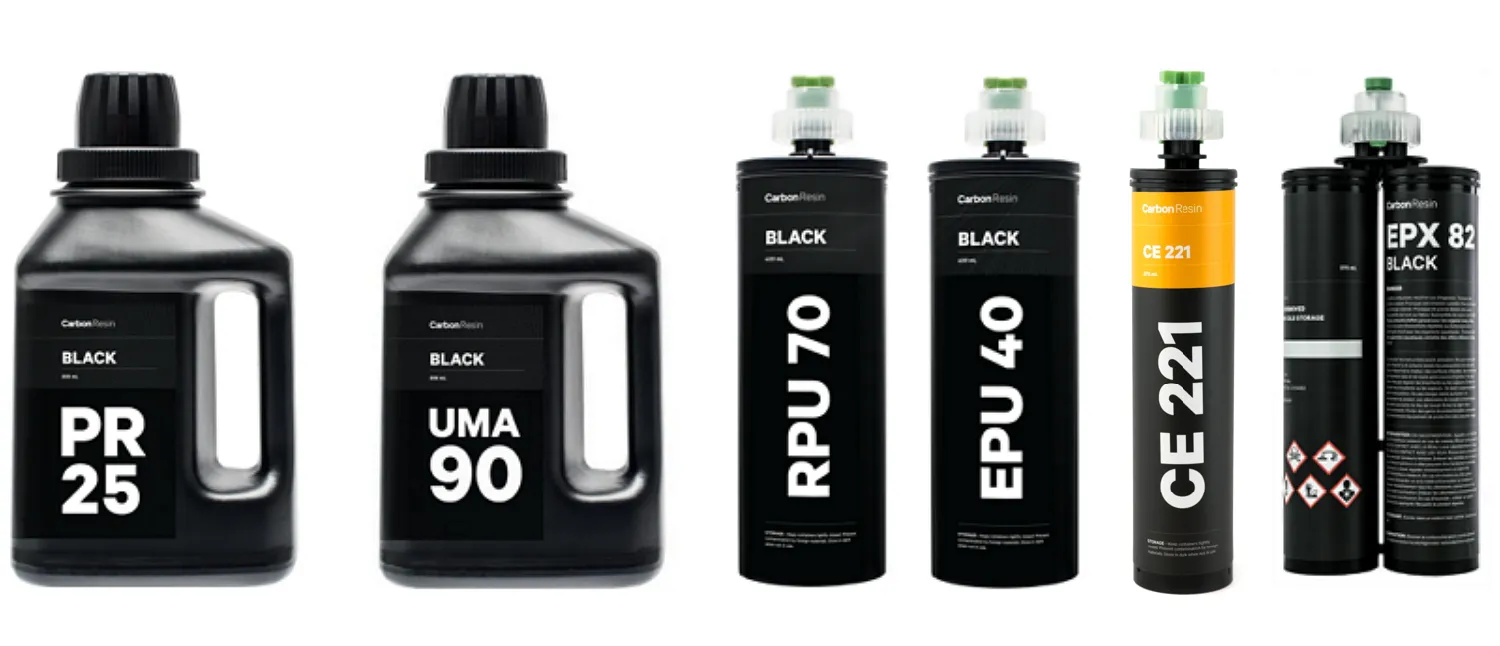
Resin Selection | Wrong resin | The print is not receiving the proper dosage of resin. |
Resin Handling After Printing
| Not checking window between prints
| Not checking the window between prints could leave accidental debris behind for the next print that inhibits proper UV exposure. Additionally, checking the window helps cool down the resin between prints. Overly heated resin can disrupt normal pigment disbursement. |
Print Plan Adjustments
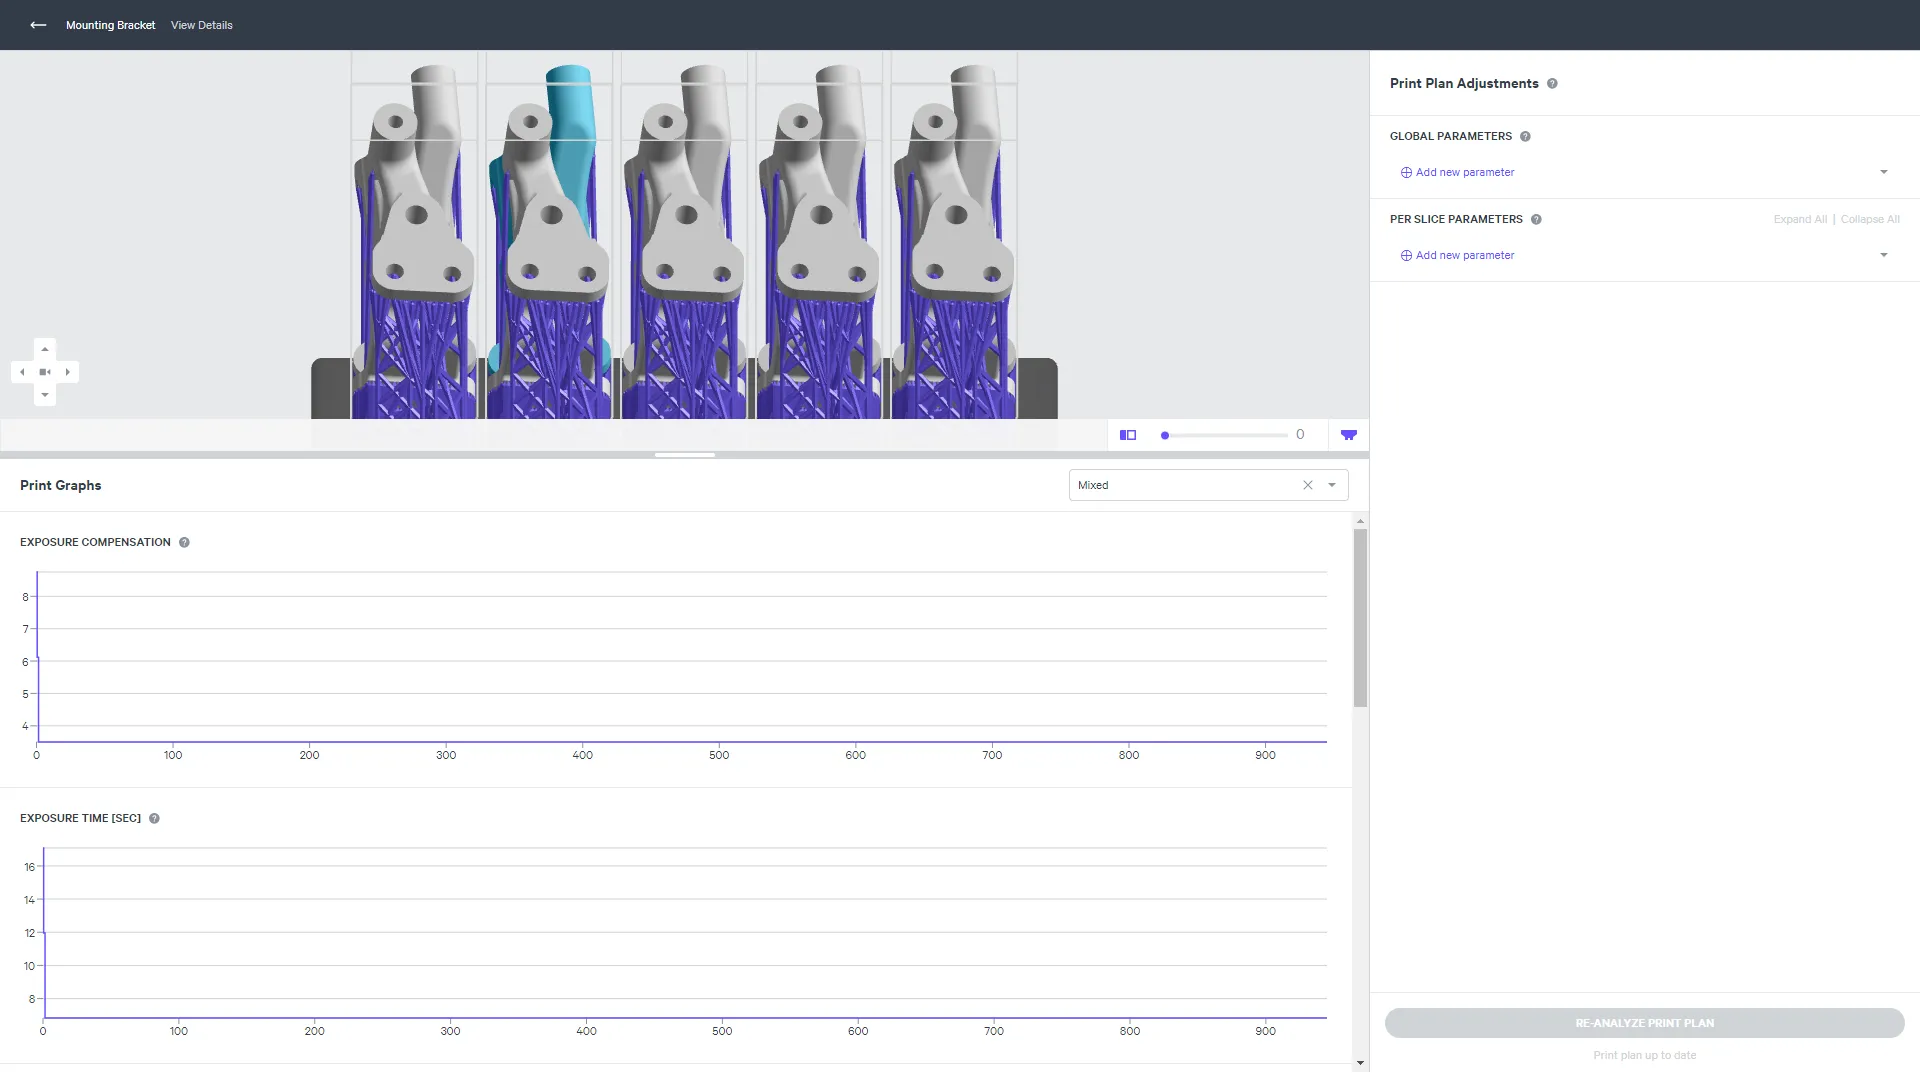
Print Plan Adjustments adjust the print plan to optimize mid to high volume production and/or address part defects.
In doing so, adjustment may both prevent or cause defects. Below are adjustments that can cause this defect.
Printing Stage | Parameter Type | Type of Adjustment | Why Defect Presents |
|---|---|---|---|
4 Settle Down | Delay Timing | Decrease | The settle down phase is too fast for proper resin flow and oxygen recharge, build causing light to scatter. |