Carbon DPR 10
Overview
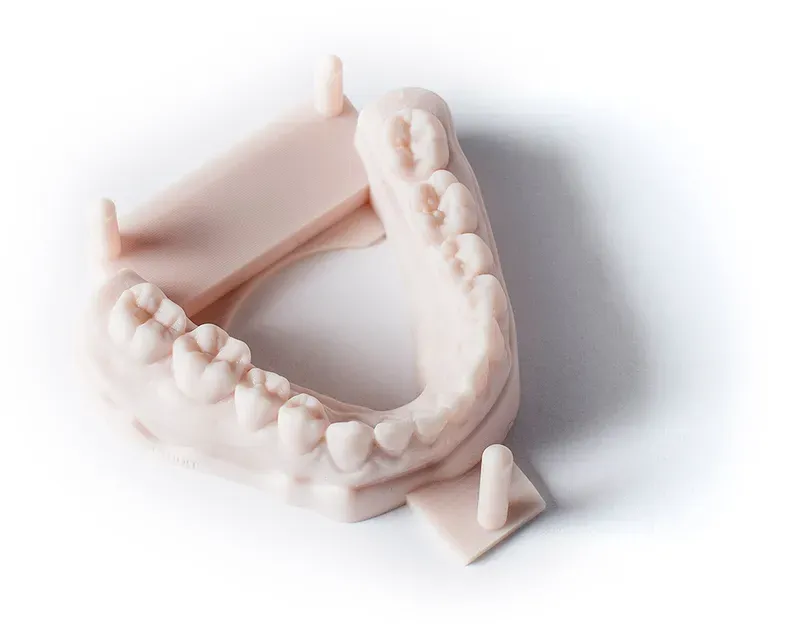
DPR 10 is a fast, accurate material ideally suited for dental models. Its stone color is appropriate for dental and orthodontic applications.
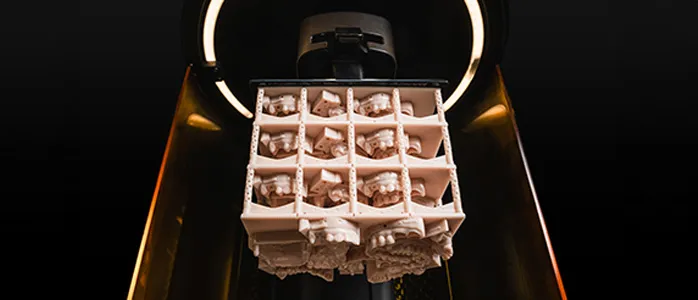
Carbon’s AO Stack workflow is designed to enable labs to produce additional DPR 10 models overnight, without the need for additional operators to handle print turnover.
This resin is not currently compatible with the AO Polishing Cassette.
Resource Links
About the Material Material overview and use cases
Technical Data Sheet Mechanical properties and data
Safety Data Sheet Login required
Protocol Sheet
This downloadable handout provides important usage information, including instructions about storage and post-processing. Print it out and bring it into the lab!
English
German/Deutsch
Spanish/Español
Dental Post-Processing Grids
One of our most popular downloads! This table provides washing and curing instructions for all supported dental resins.
Print it and use it in the lab as a quick reference.
German/Deutsch
Spanish/Español
Workflow
Design
Dental CAD Software
Dental CAD software must be used to modify dental scans and design the production files. Settings to use when printing on a Carbon DLS printer in DPR 10 resin are available for 3Shape (including a DME file) and exocad.
These recommended settings are the best starting point for your models and dies. Adjustment for fit and design preference may be required.
Click the link below to see videos for the CAD software that you use.
Login required
Login required
Full Palate Models
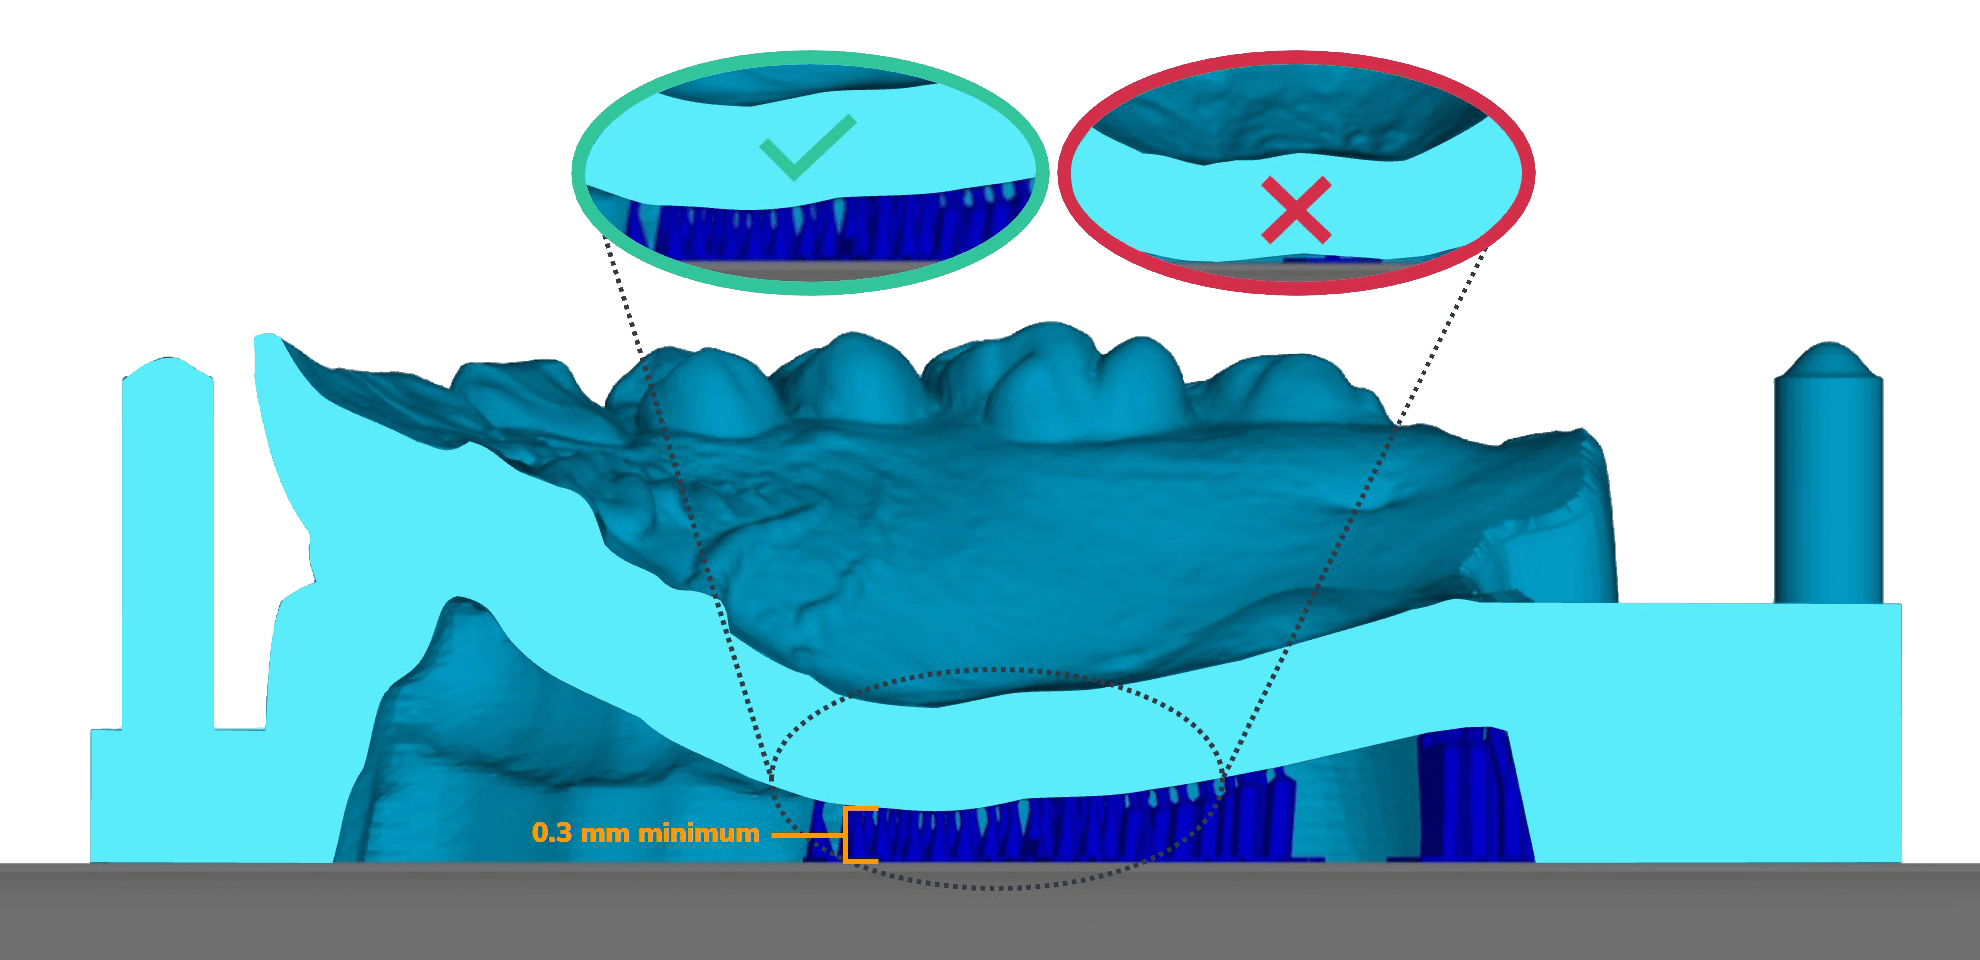
The recommended Carbon DPR 10 settings will result in a proper model height in the majority of cases. In rare cases, full palate models may require an increased height if the palate is especially deep and does not leave enough space for rafted supports.
Increase the height of extra deep palate models to allow a minimum of 0.3 mm between the palate and the platform.
Wall Thickness
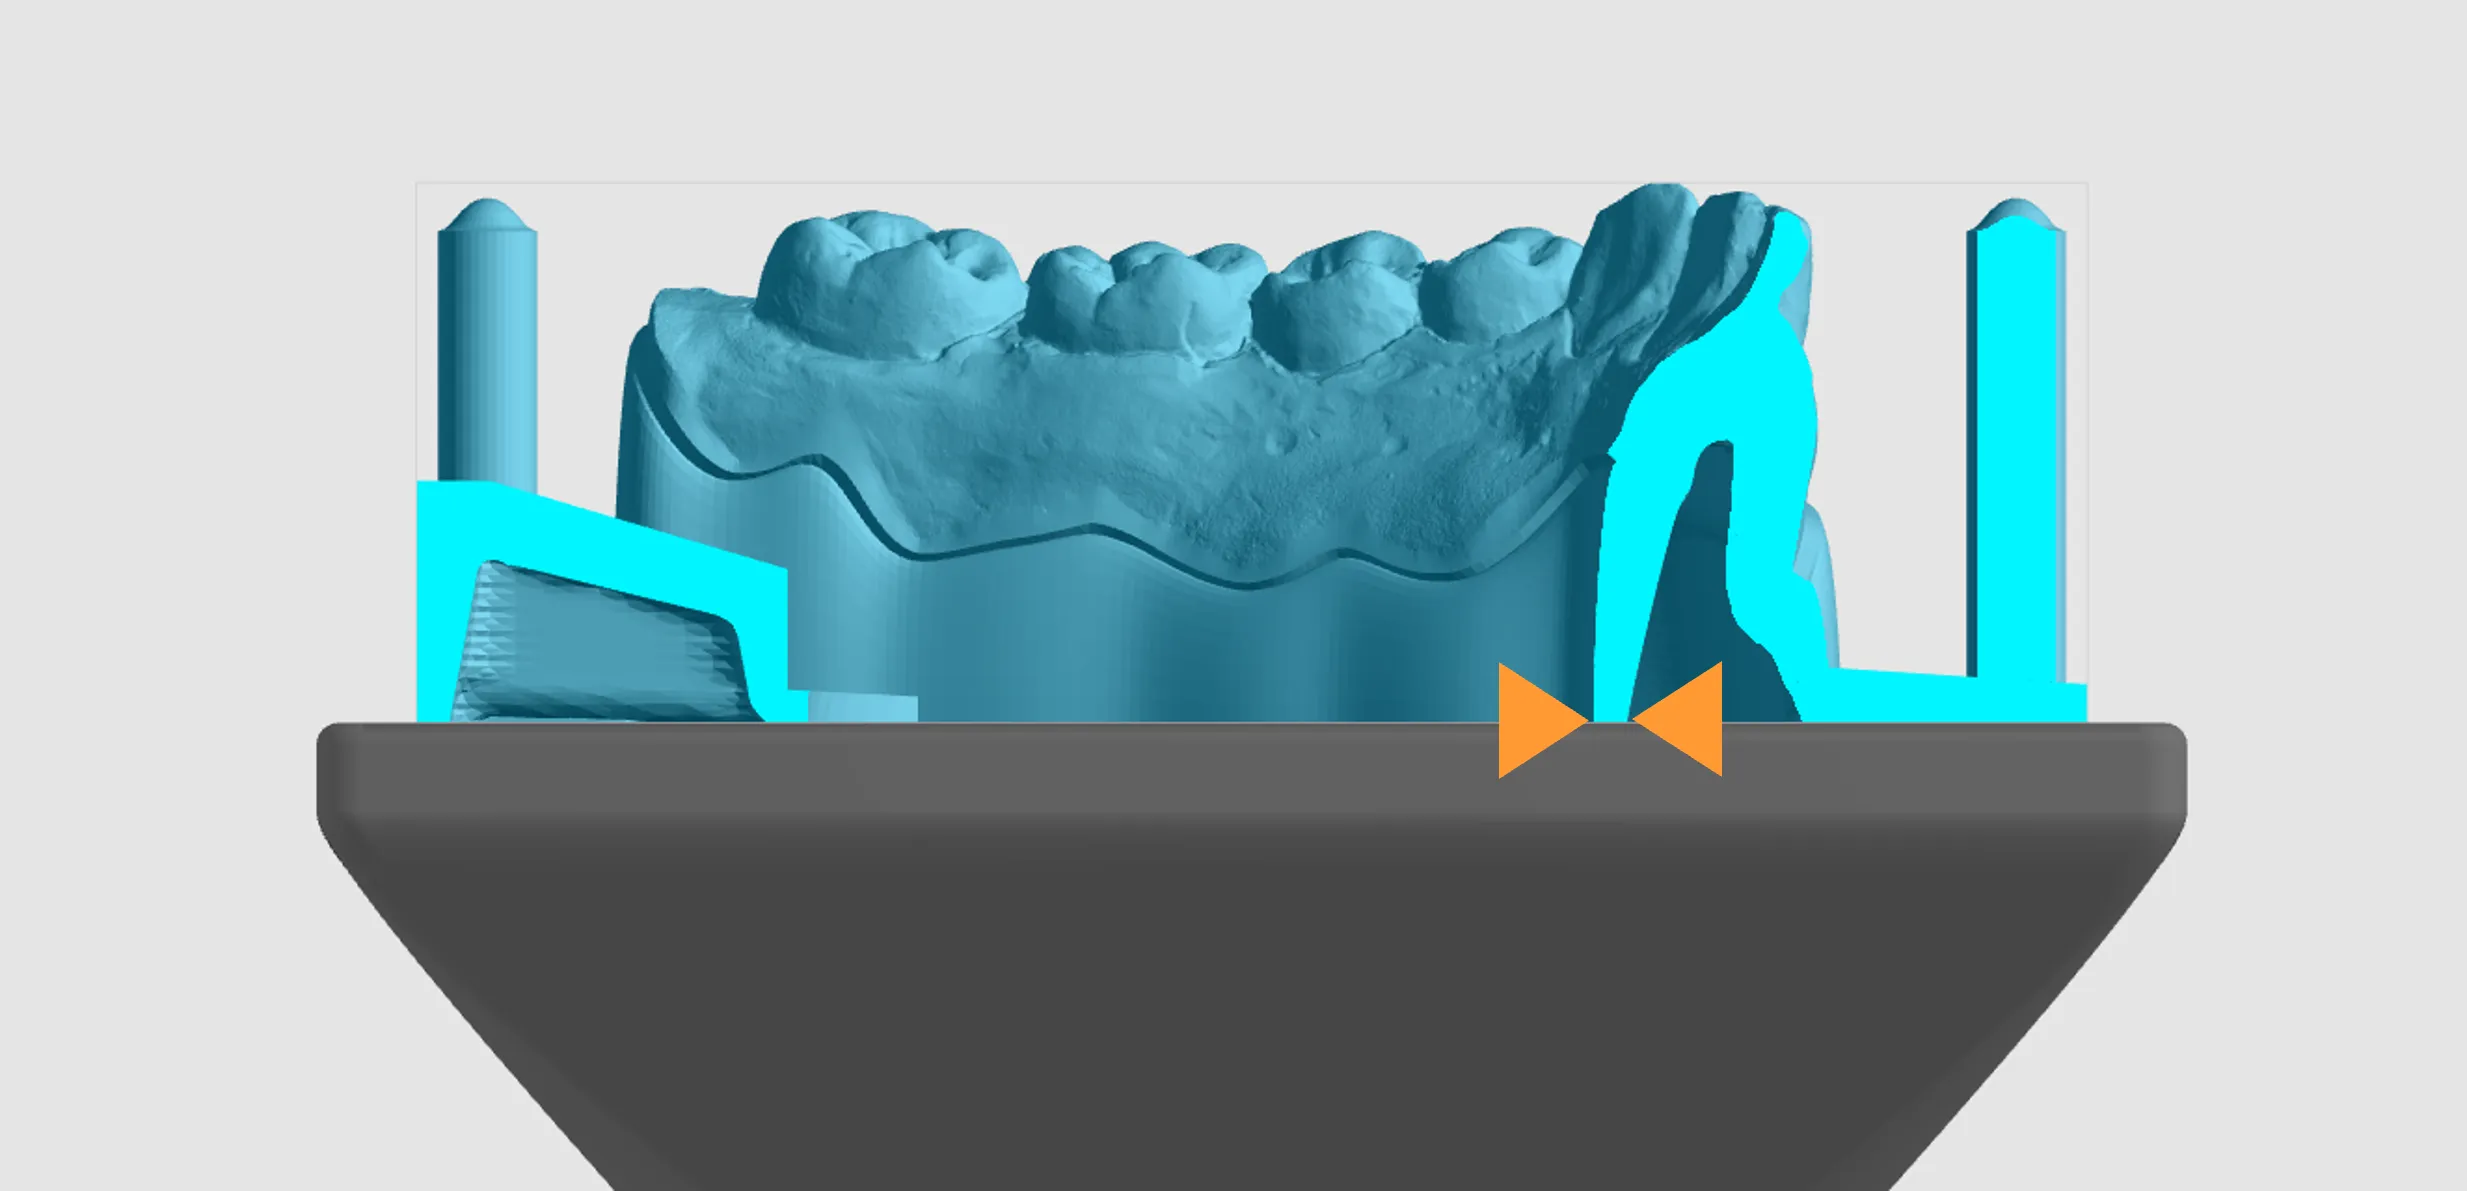
- Recommended wall thickness: 2.5 mm
- This thickness represents a good balance of resin usage, print speed and accuracy.
- Thinner walls could yield less accurate parts that can crack during part removal
- Variable wall thickness functionality is built into dental CAD programs. This feature will thicken walls as the part progresses, yielding fewer islands and more accurate parts.
The Carbon 3Shape DME file will automatically apply this setting.
Vent Creation
After hollowing, parts require vents (known as Side Drain Holes in 3Shape) to allow the free flow of resin and air into the interior of your part during printing. This prevents print failures due to internal vacuum forces within the part, uses less resin, and speeds up prints.
- 2-3 mm in diameter.
- Located at least 1 mm above the platform.
The Carbon 3Shape DME file will automatically apply these settings.
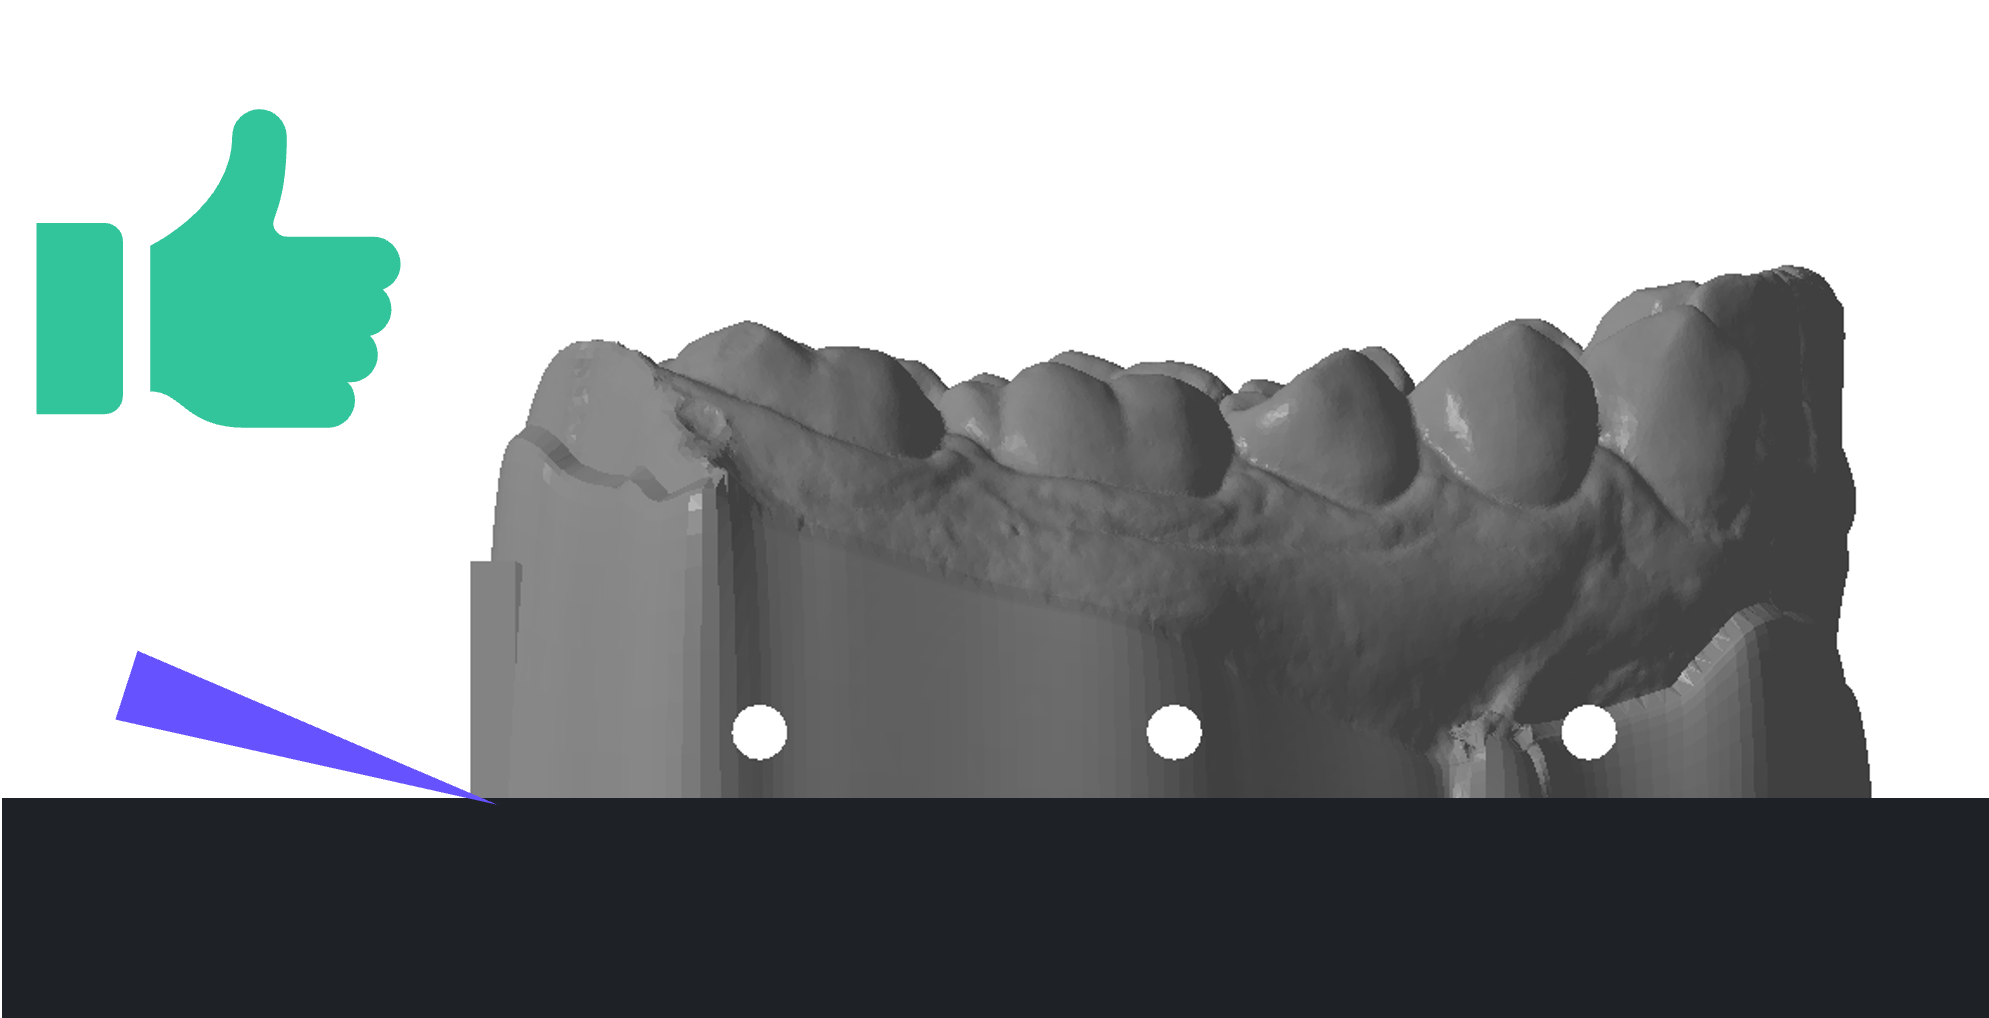
Vents above platform
- Part is stronger at platform
- Lower chances of cracking during removal from platform
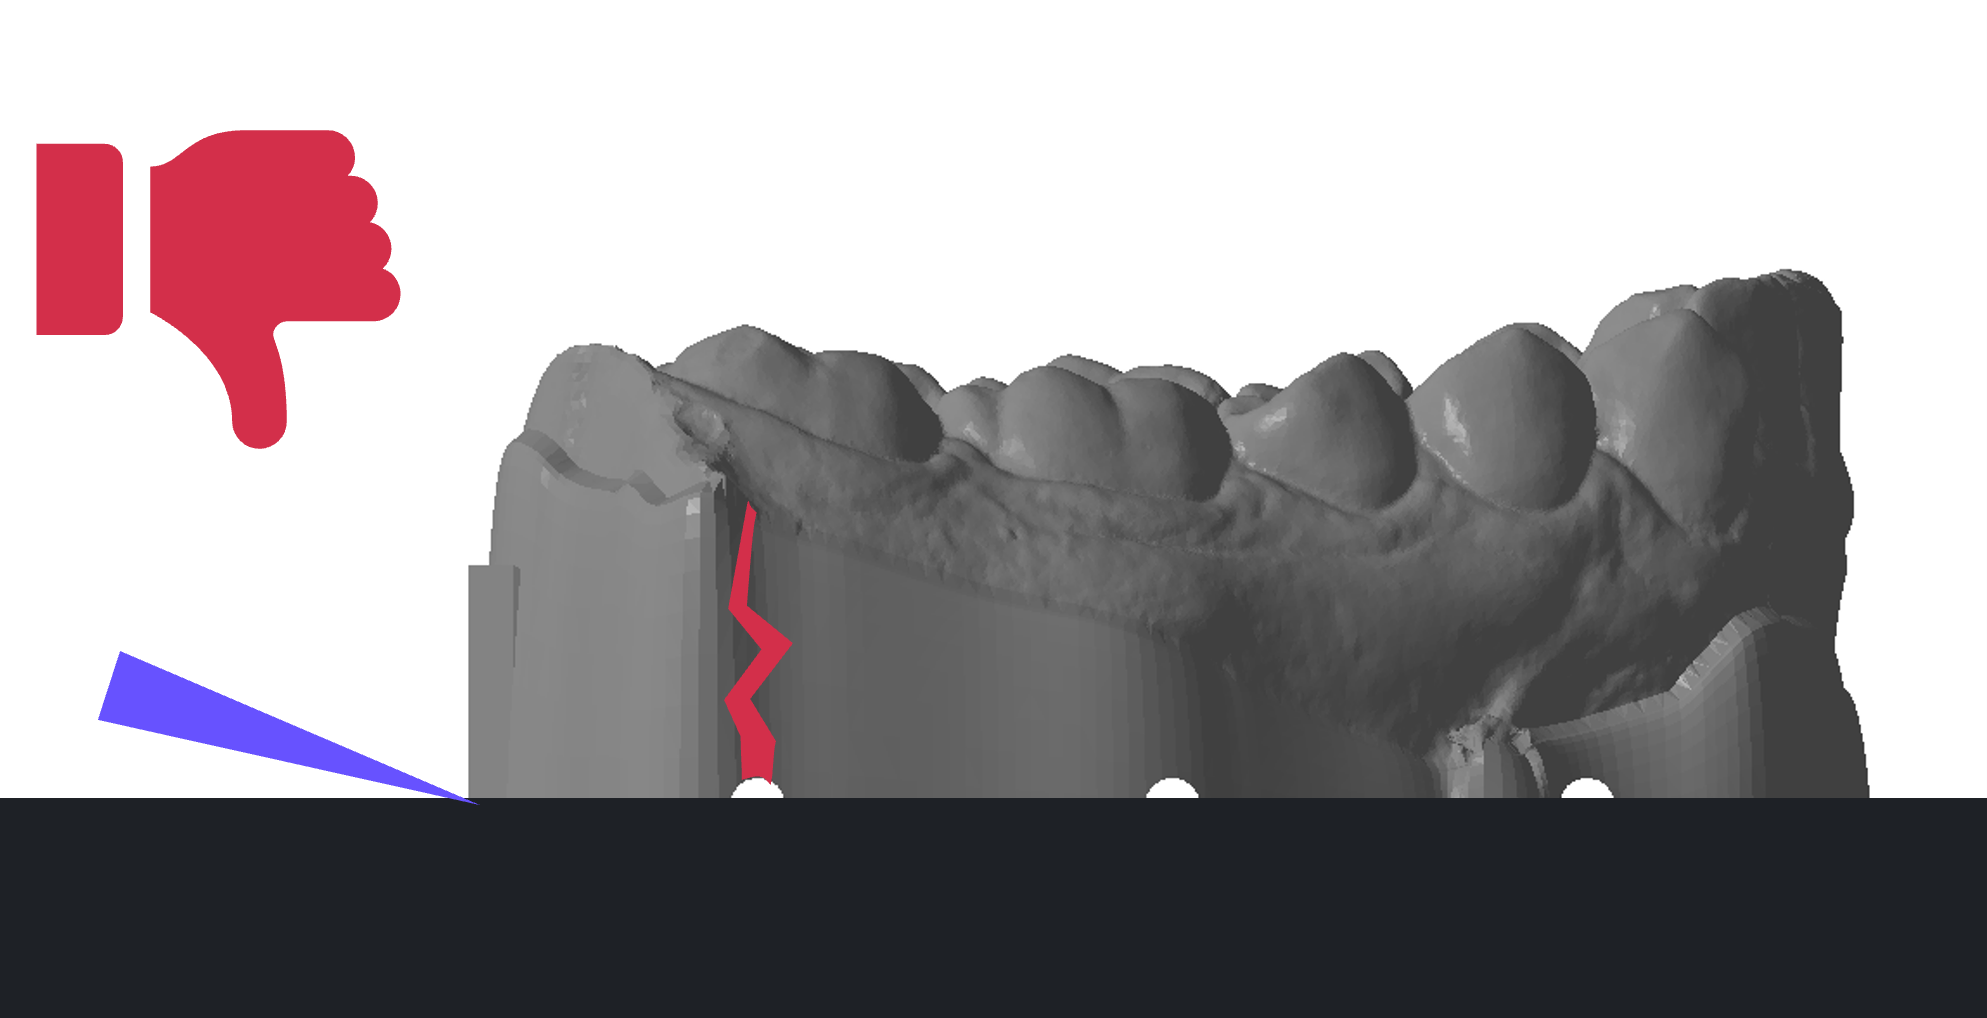
Vents at platform
- Vent can become point of failure during removal from platform
- Chances of cracking increase during removal from platform
Carbon Customer Support and HIPAA
HIPAA (Health Insurance Portability and Accountability Act of 1996) is United States legislation that provides data privacy and security provisions for safeguarding medical information.
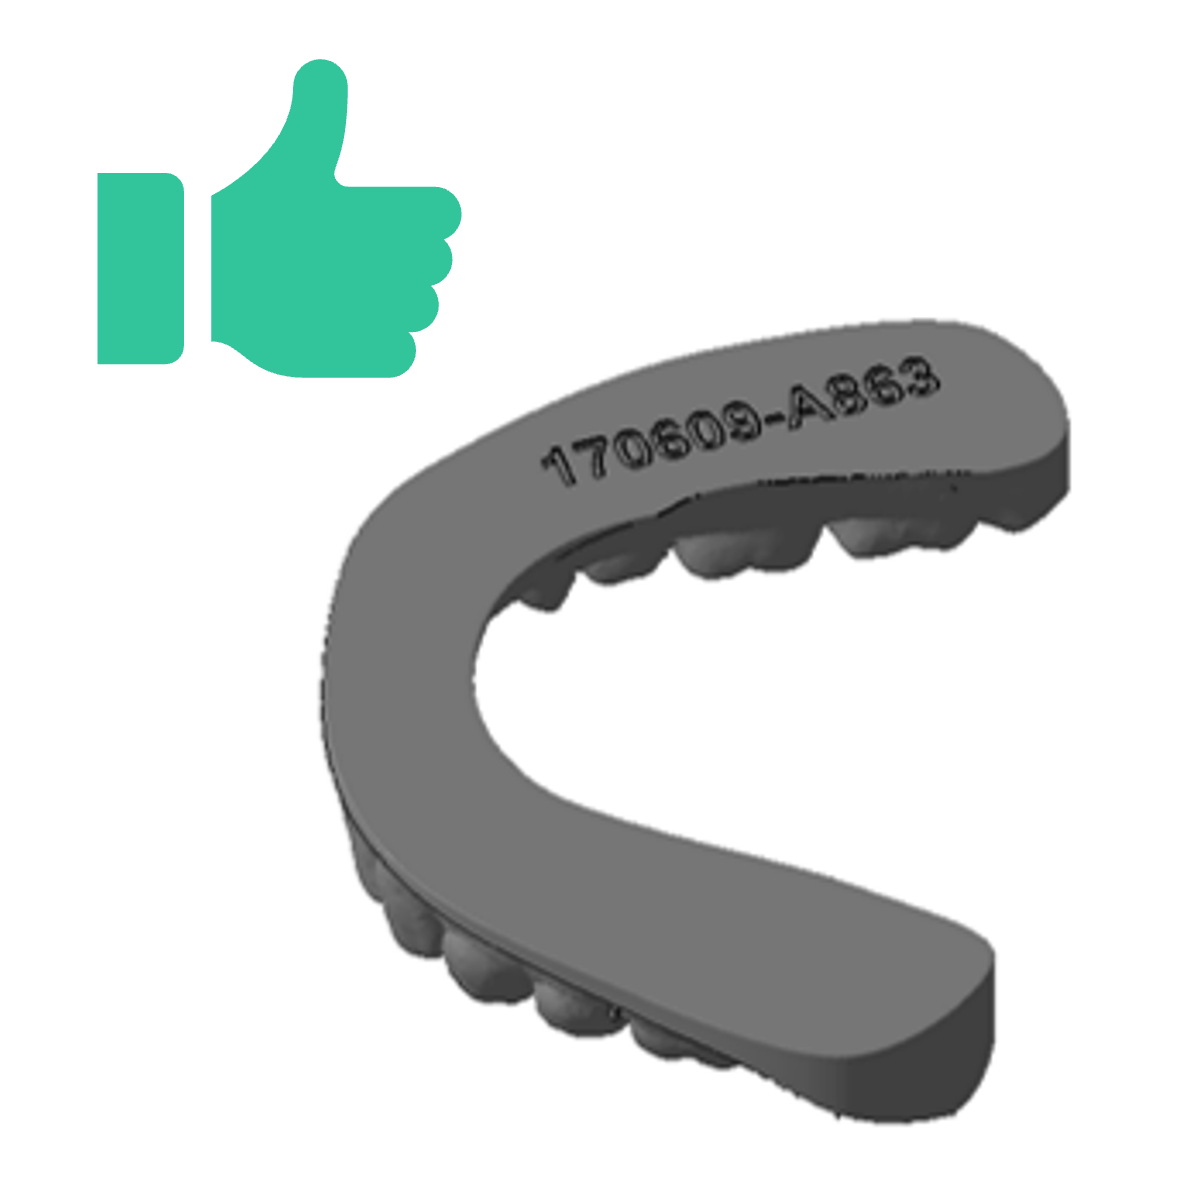
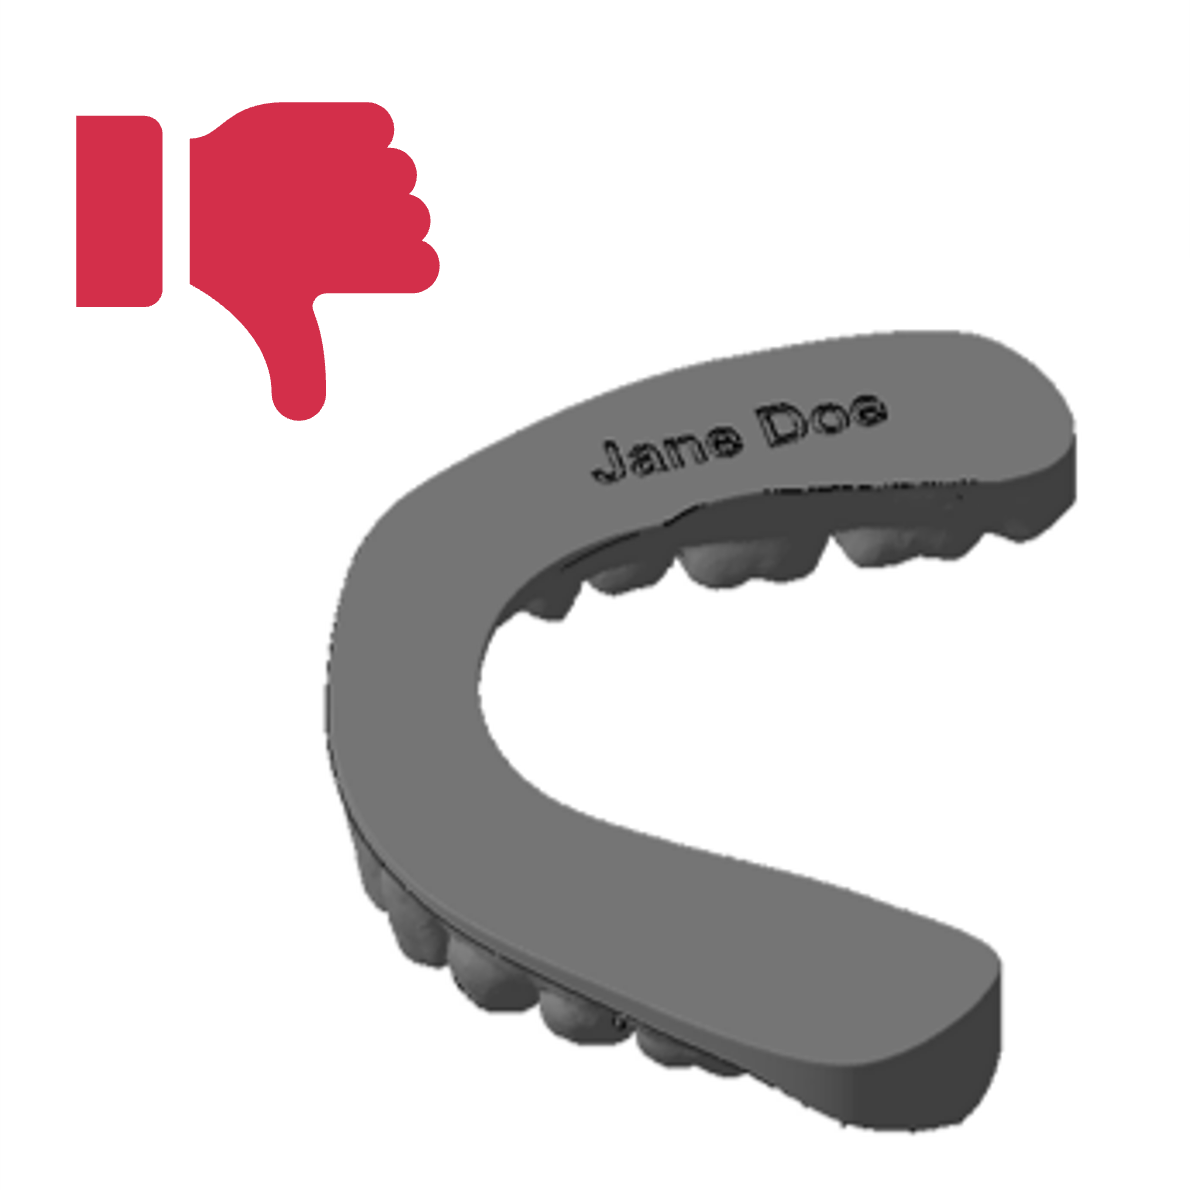
- Due to HIPAA regulations, Carbon cannot receive files that have patient names in the file name or imprinted on the geometry.
If you need to send files to Carbon for technical support, remove the patient name from the file name and from the geometry.
General Orientation & Support Information
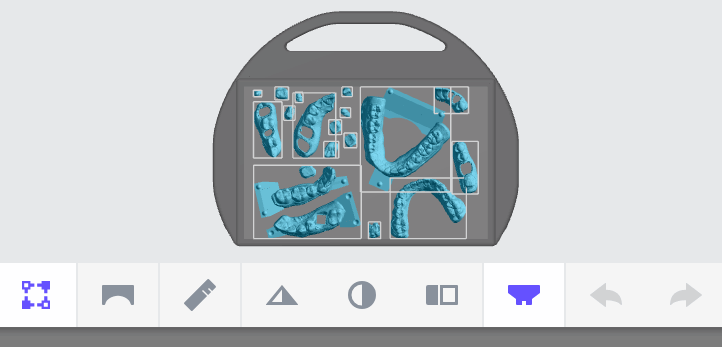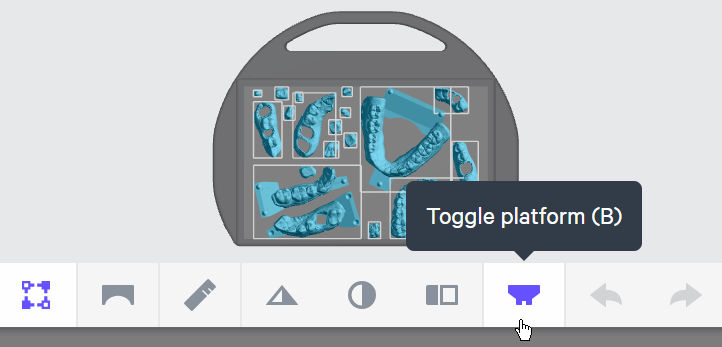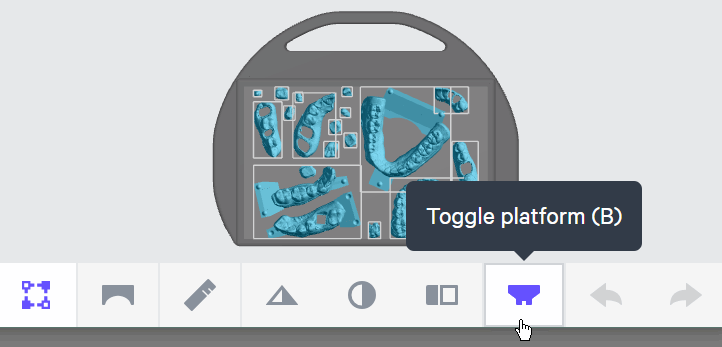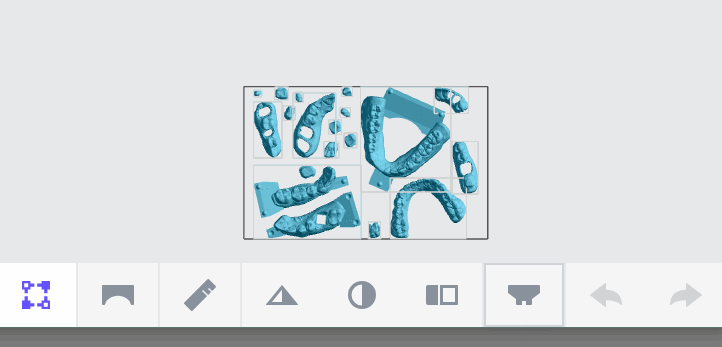
Hide the Platform
Use Toggle platform (or press B) to hide the platform before orienting parts. This will make it easier to see overhangs and place supports.
Patch tool
- The Patch tool speeds up support creation by automatically supporting an area with just a few clicks. It is useful for supporting larger areas of overhang that would take longer to support manually.
- It is often useful to support your parts with this tool before manually adding supports.
Support Creation Workflows
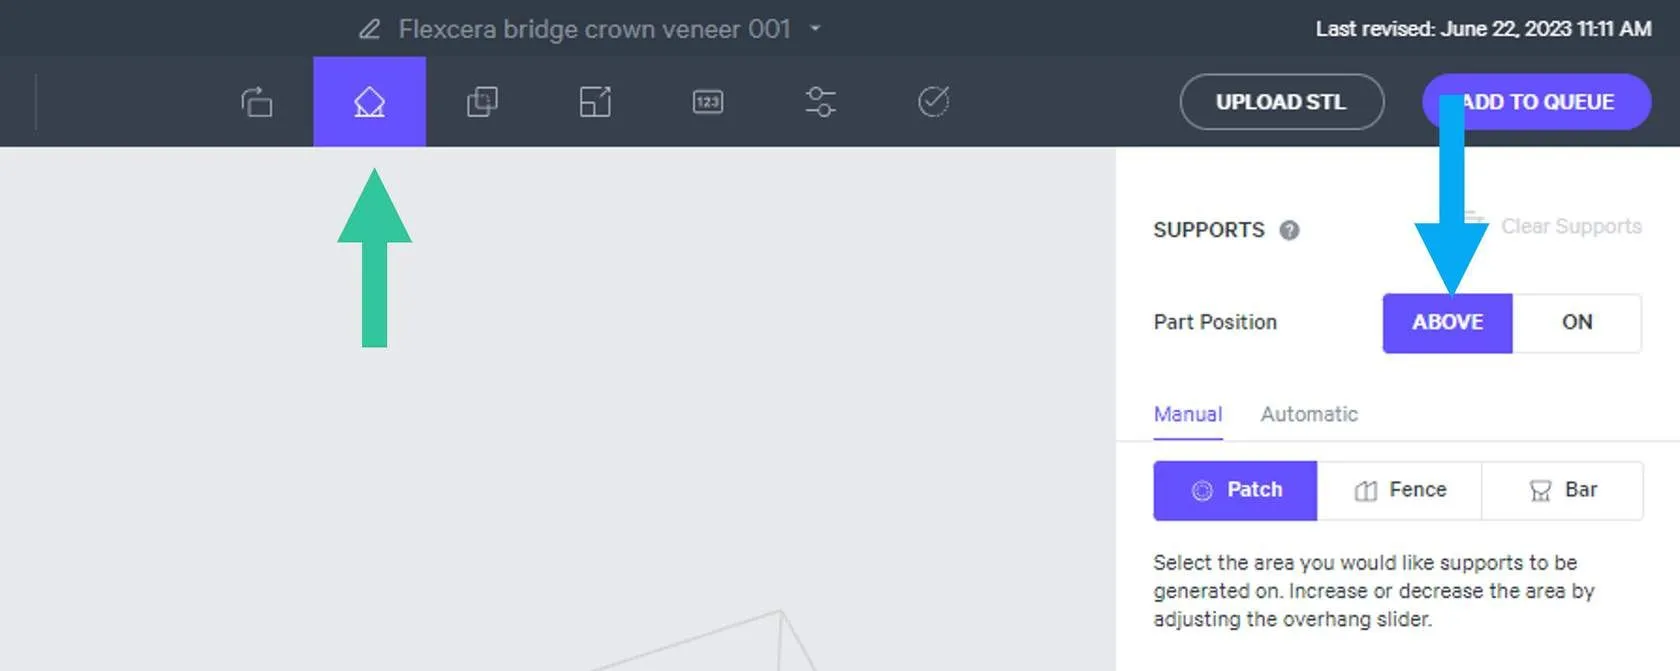
Enter Support mode
- Click Support tab or Shift + S in the top bar.
- Select the part you want to support.
- Under Part Position, select On to keep parts on the platform. This setting is useful for most dental models because they have flat bases/edges that adhere to the platform.
Patch workflow
- Select the part to be supported.
- Orient the camera so that the overhangs are clearly visible.
- Check that Patch is selected.
- Click on each large overhang to select it. A green patch will appear over each overhang. Repeat until all the large overhangs are selected.
- Under Support Attributes → Primary Support Type, select Bar.
- The other Support Attributes should remain their default values.
- Click Generate All to create the supports.
Never use fence supports for models that will be printed in Automatic Mode on the AO Backpack. Automatic Mode models require bar supports with base rafts. See Supporting Models for Automatic Mode for more information.
Review Supports in Printer UI course for more information.
Digital Prep
Setup your Print
Connect to Printer
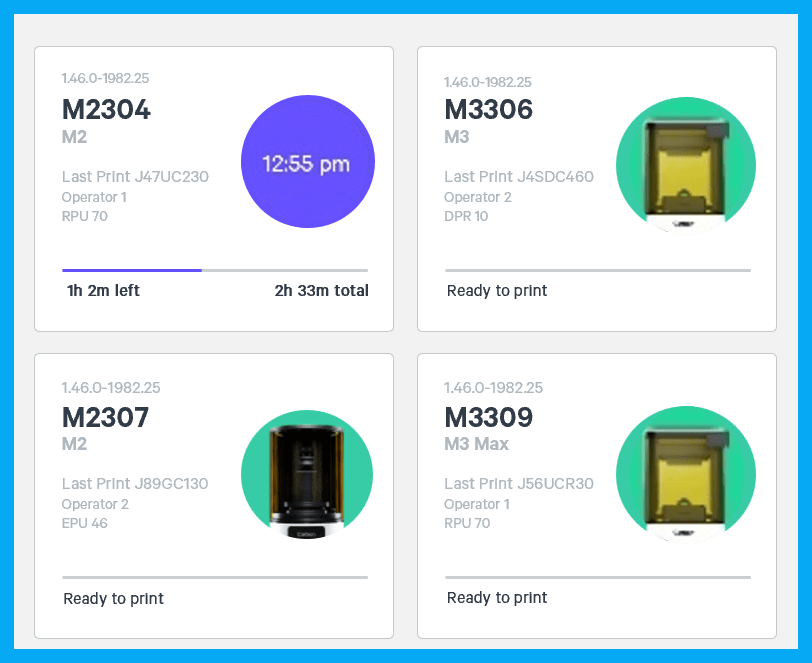
Connect to the printer software using your web browser.
Create project
After you have chosen the printer, you must create a new project.
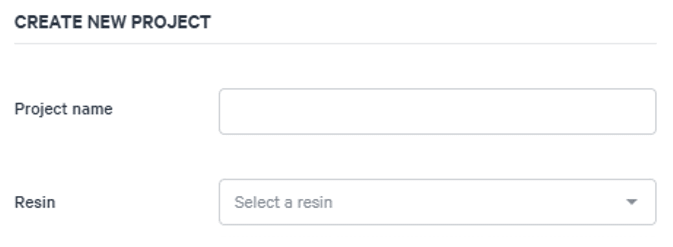
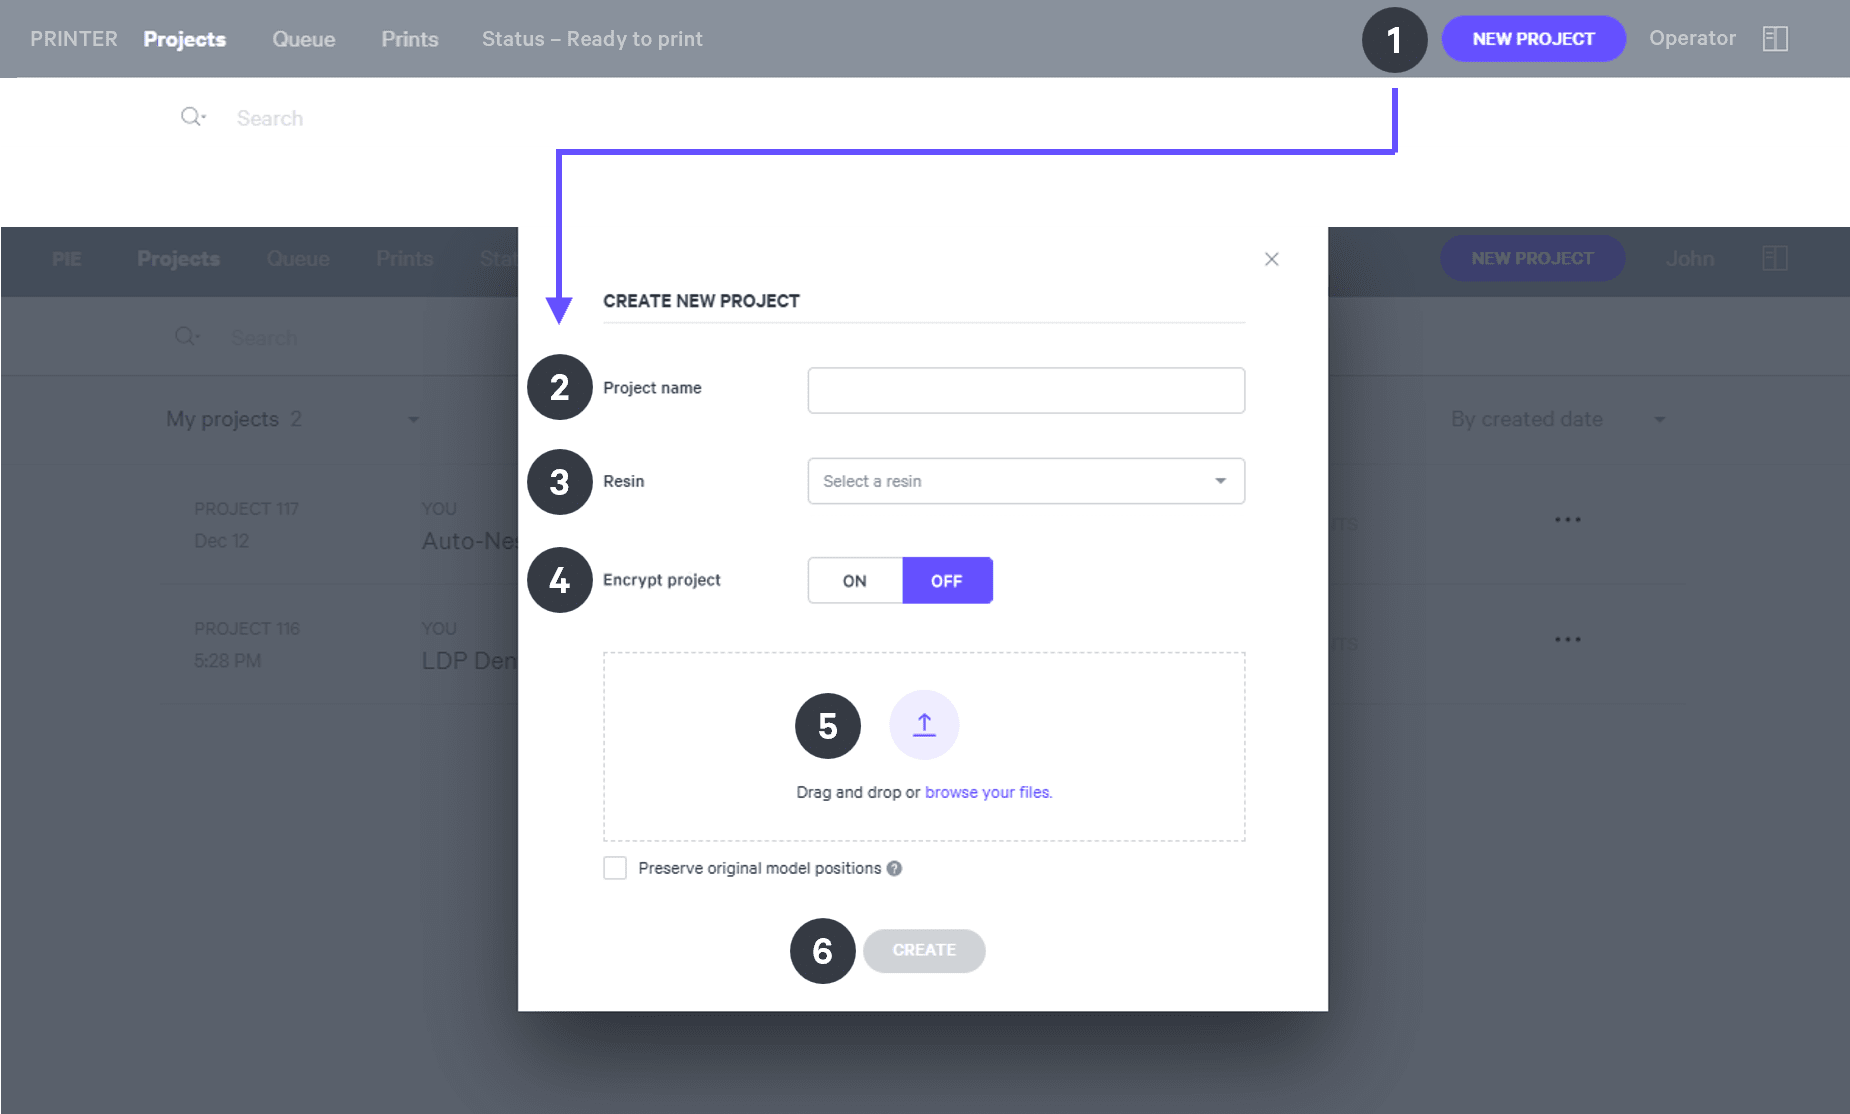
Proper orientation of models and dies is critcal to achieve the required accuracy. Failure to orient these files according to these instructions may impact accuracy and part quality.
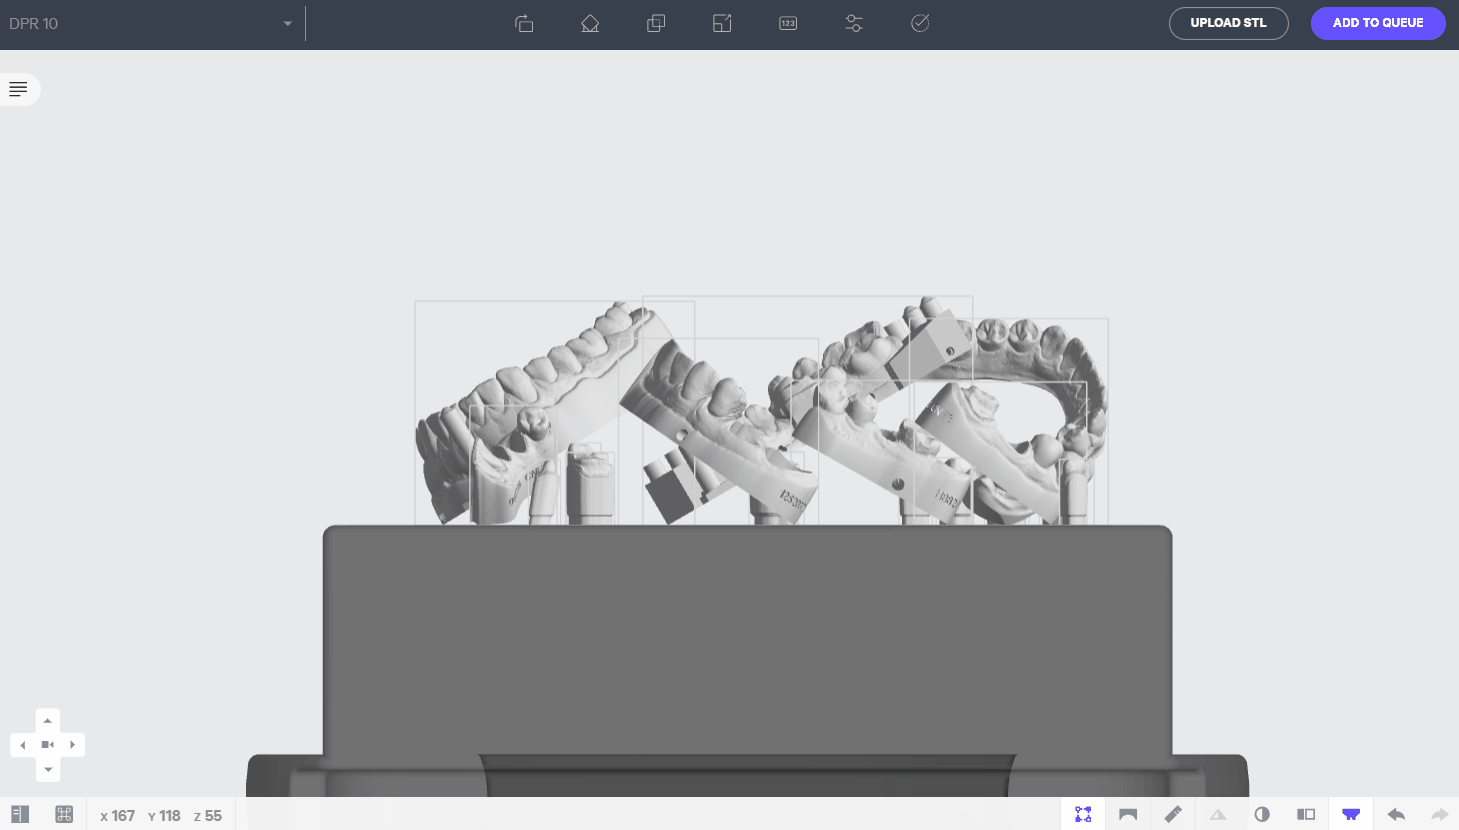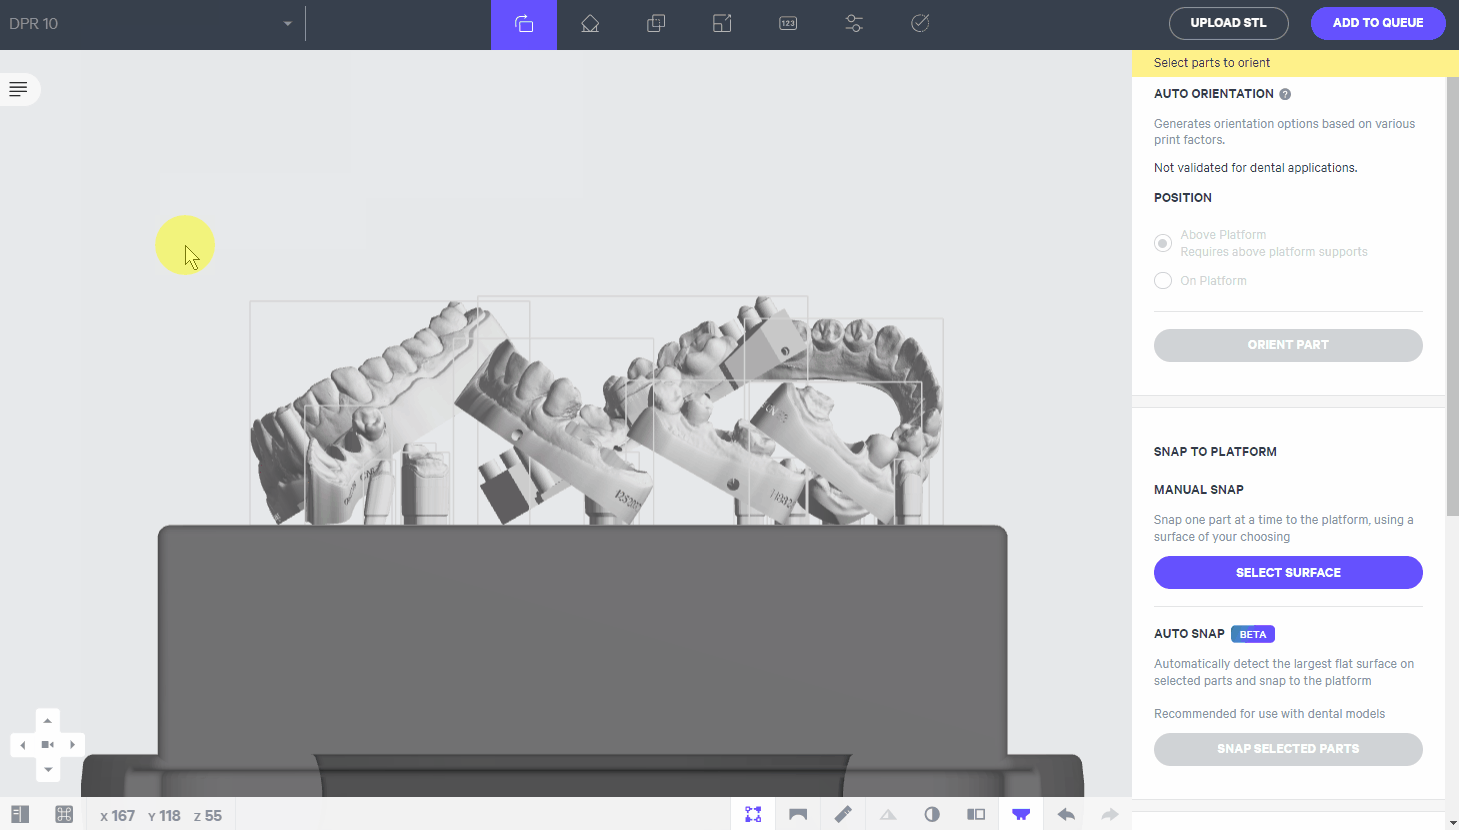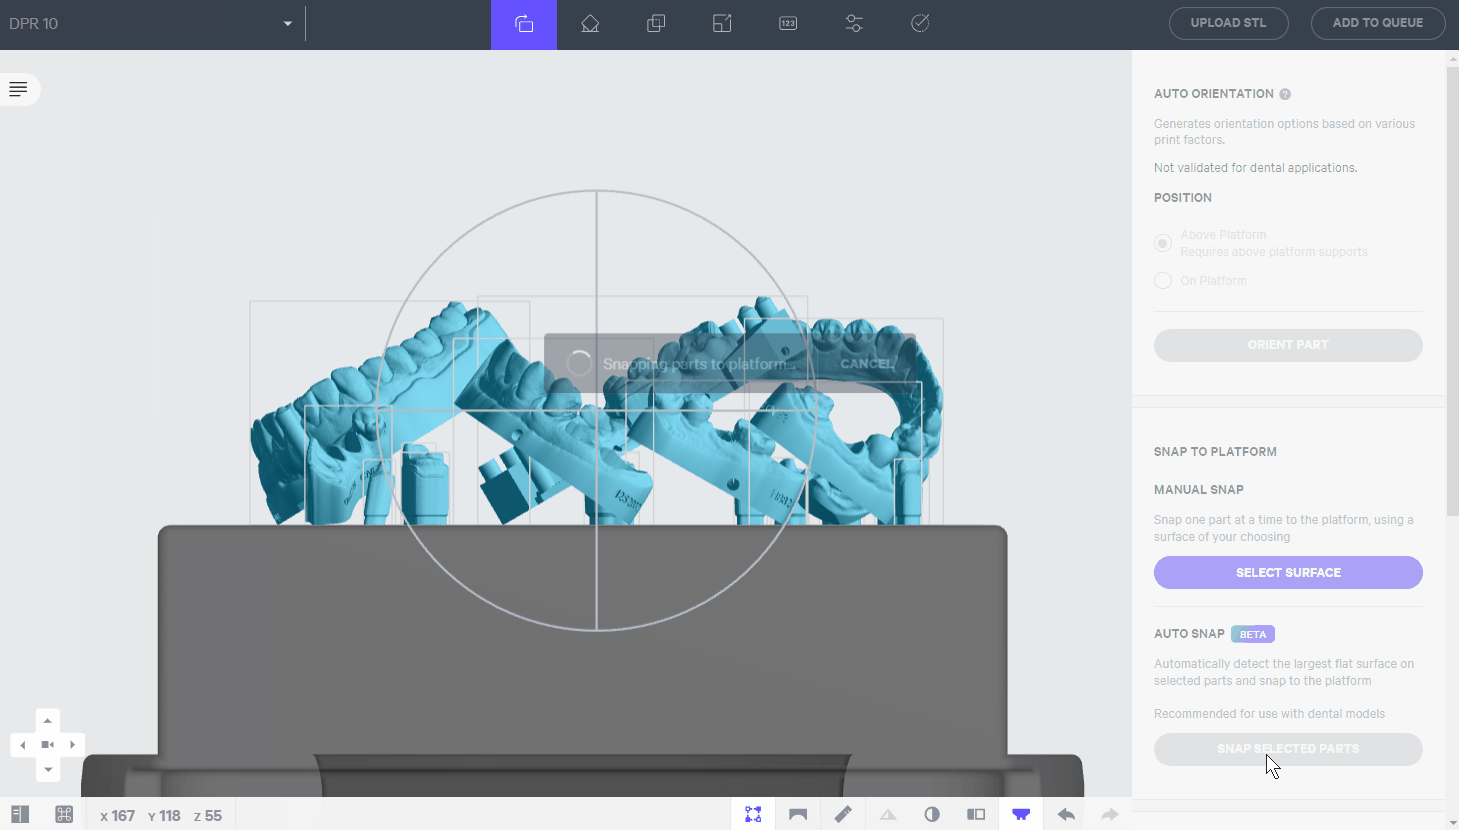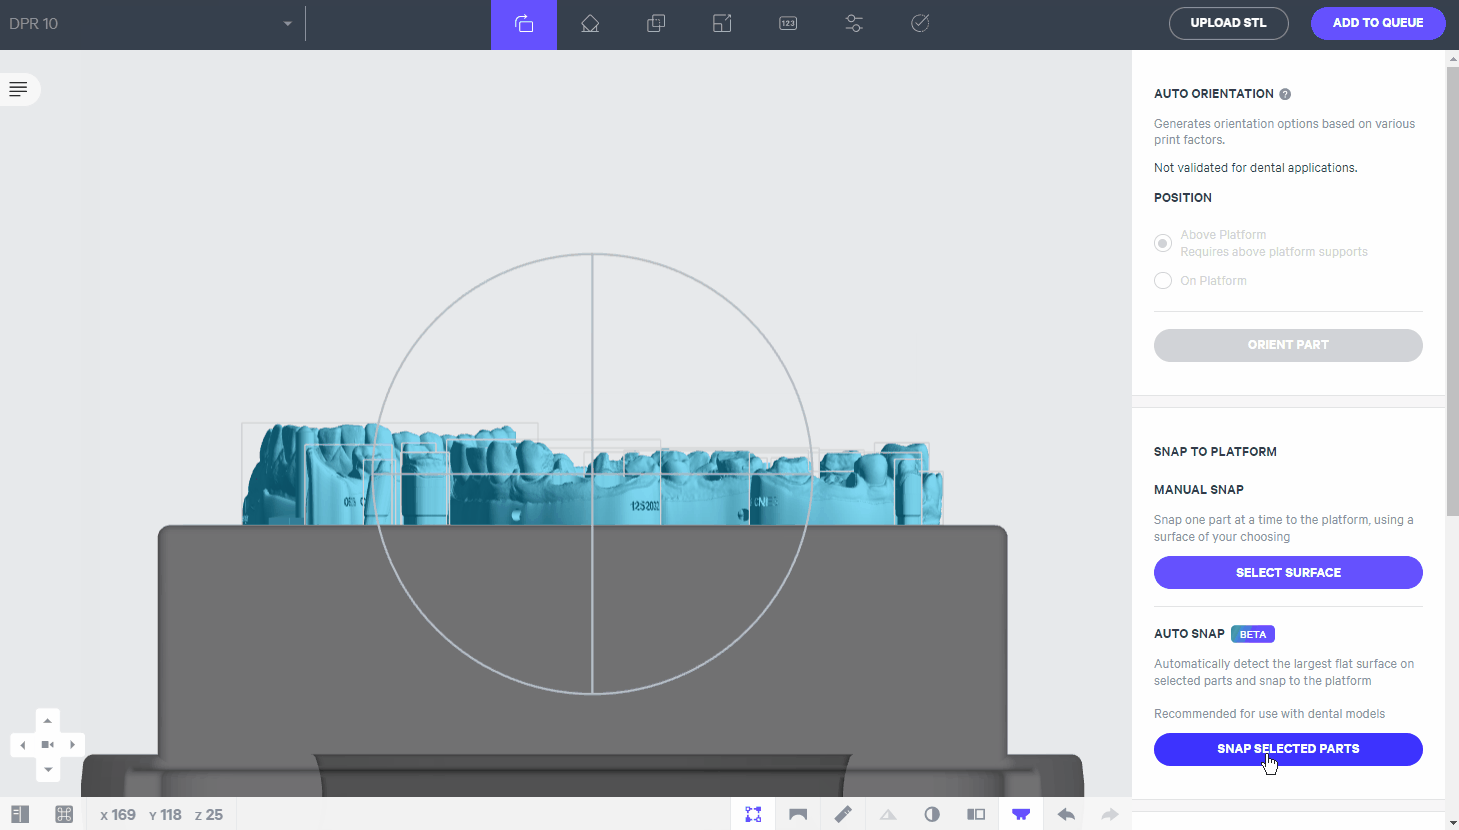
Most dental models (arches, quads and dies) have flat bases that can be printed directly on the platform.
- Click the Orient tab in the menu bar or press Shift + O.
- Select the parts.
- Click Snap Selected Parts.
- After a short time, the models should all be oriented with their flat bases parallel with the platform.
- Be sure to check that each model is properly oriented.
Full arch models, quads and dies designed using Carbon's 3Shape DME settings do not require supports because they are printed directly on the platform.
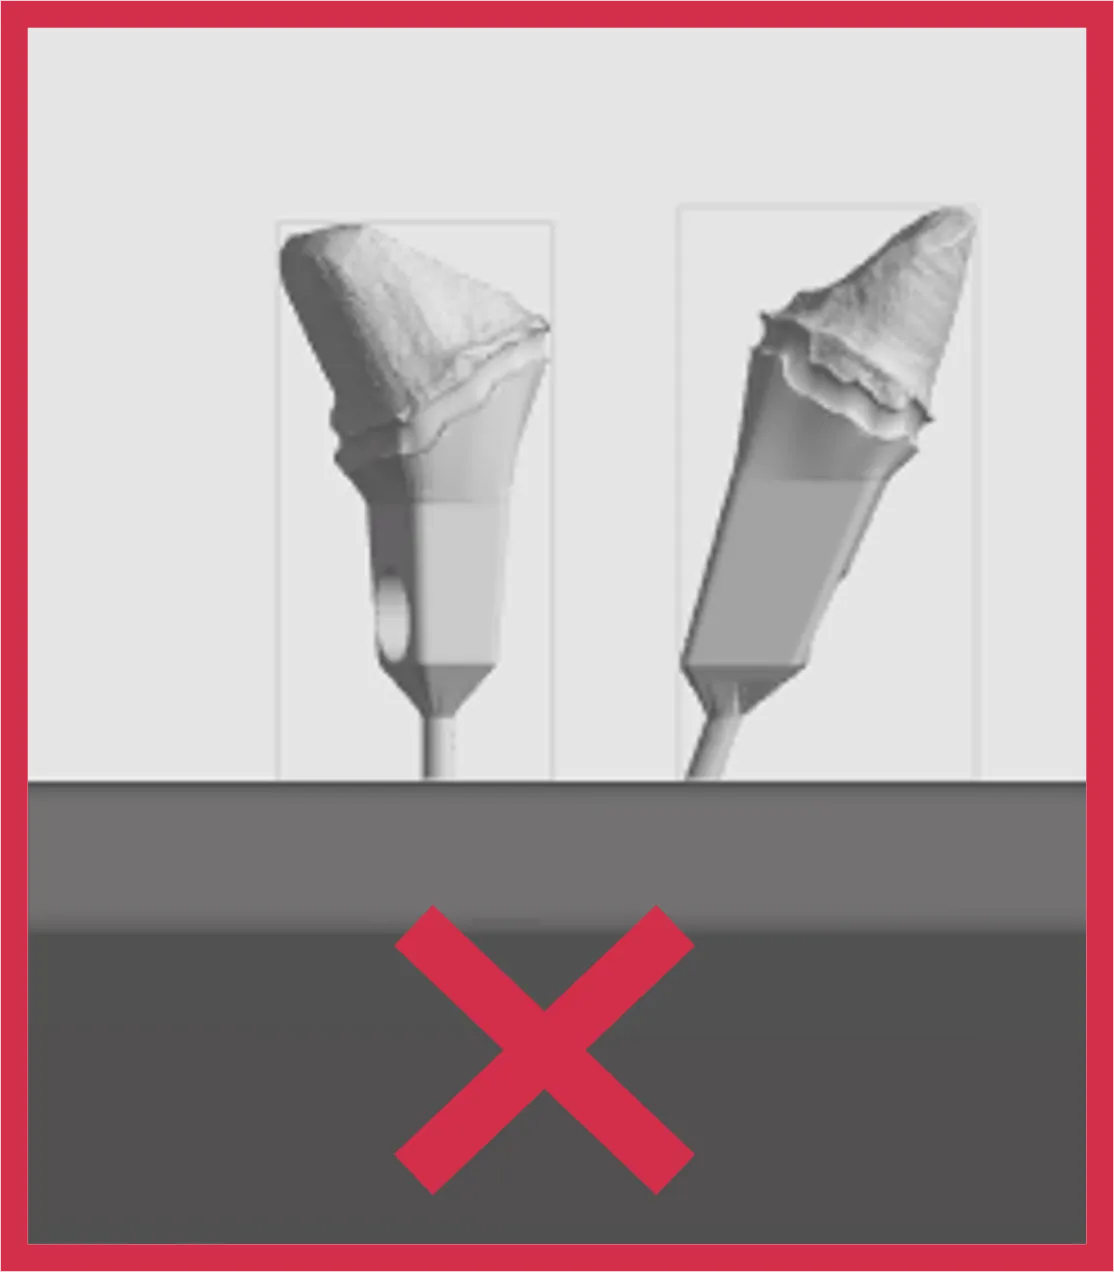
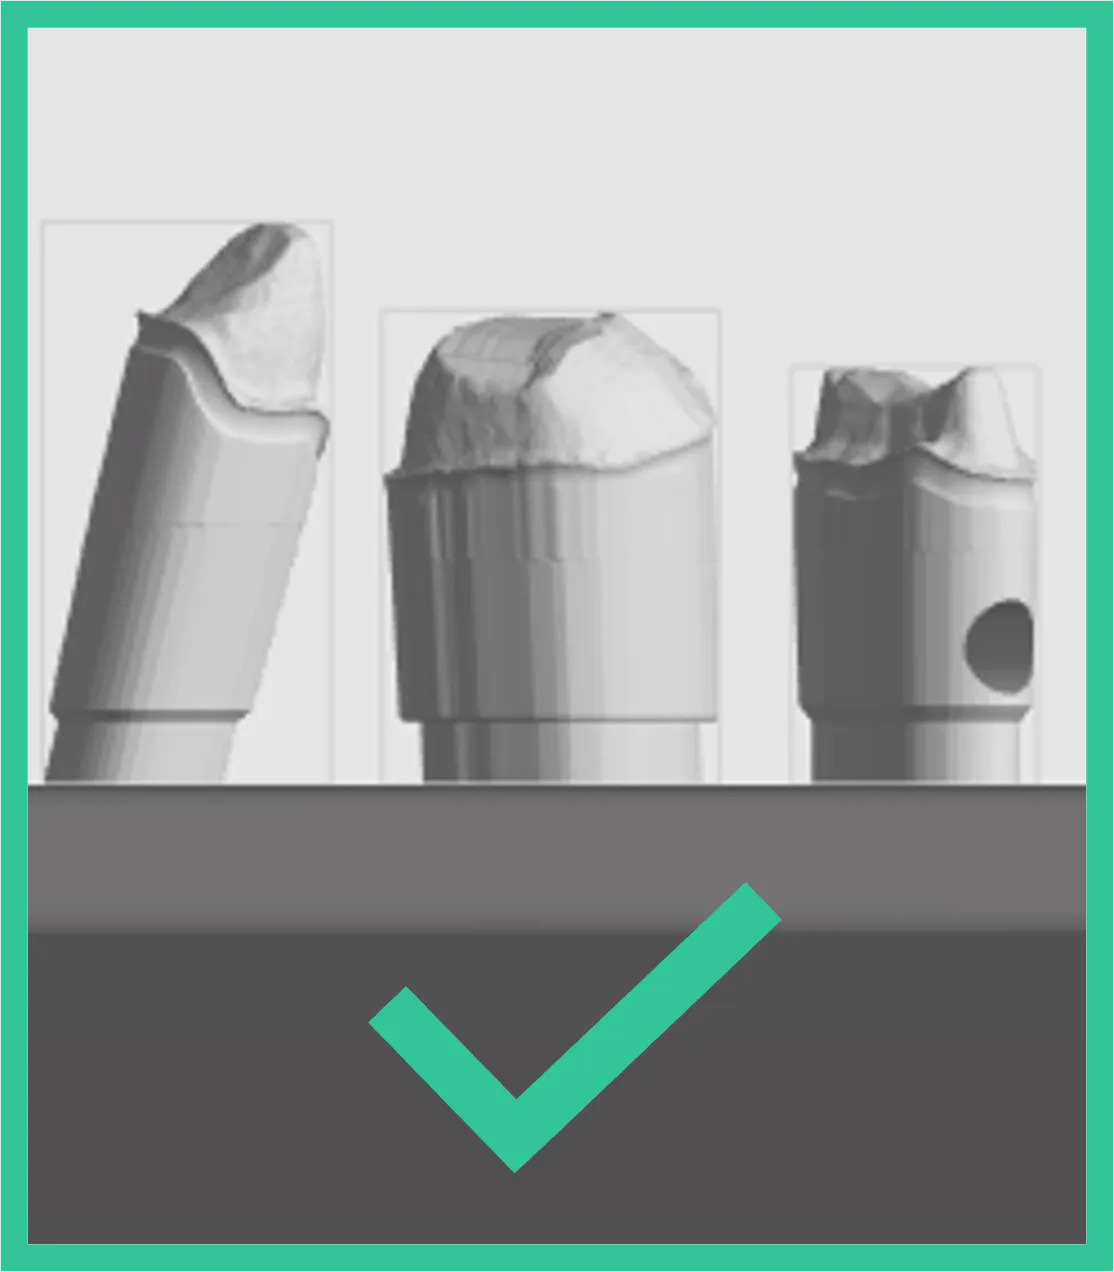
Dies with small cylindrical pins should not be printed as they can easily detach from the platform during printing and lead to failed prints and potentially cause cassette damage.
Dies designed without Carbon's 3Shape DME
Dies designed with Carbon's 3Shape DME
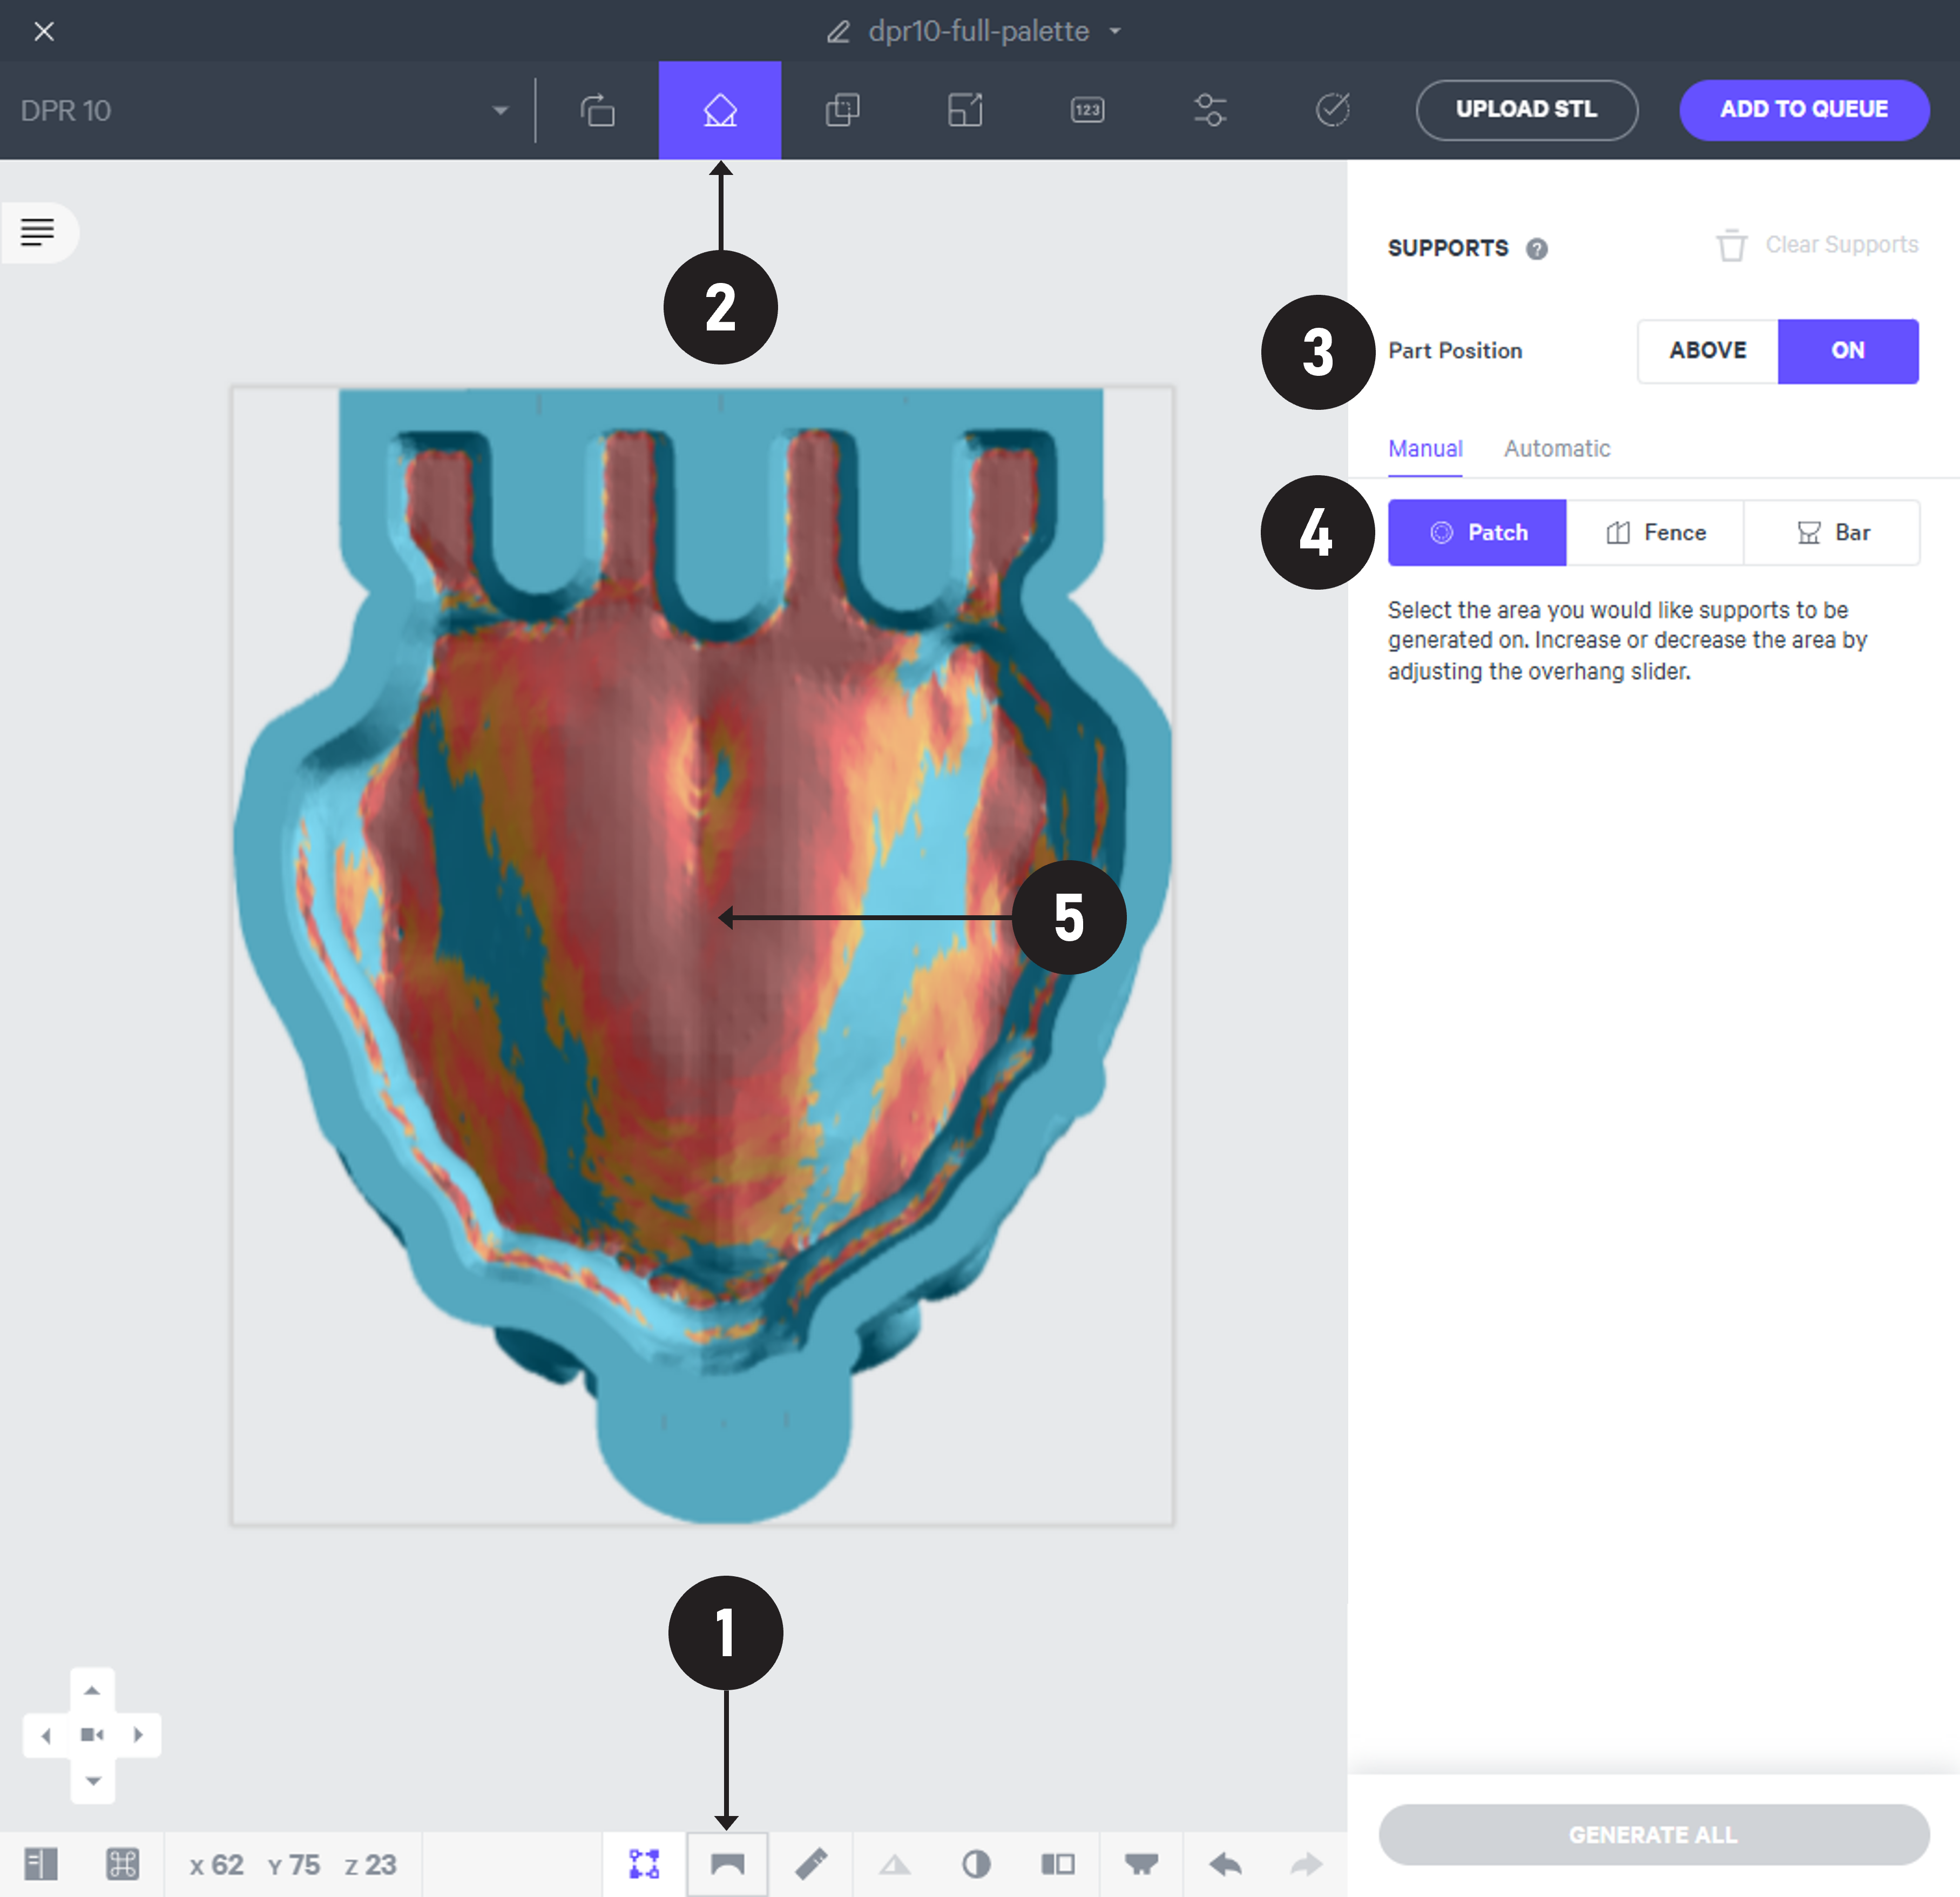
The palette surface typically requires supports. Use the Patch tool to quickly add supports.
Select a patch
- In the bottom tool bar, click Overhang detection (or press V) to highlight areas that may require supports.
- Click the Supports tab in the menu bar or press Shift + S. The Supports menu will appear on the right.
- Under Part Position, select On to keep the model positioned directly on the platform for printing.
- Under the Manual tab select Patch.
- Click on a large area of overhang to select a patch. This will create a green highlighted area.
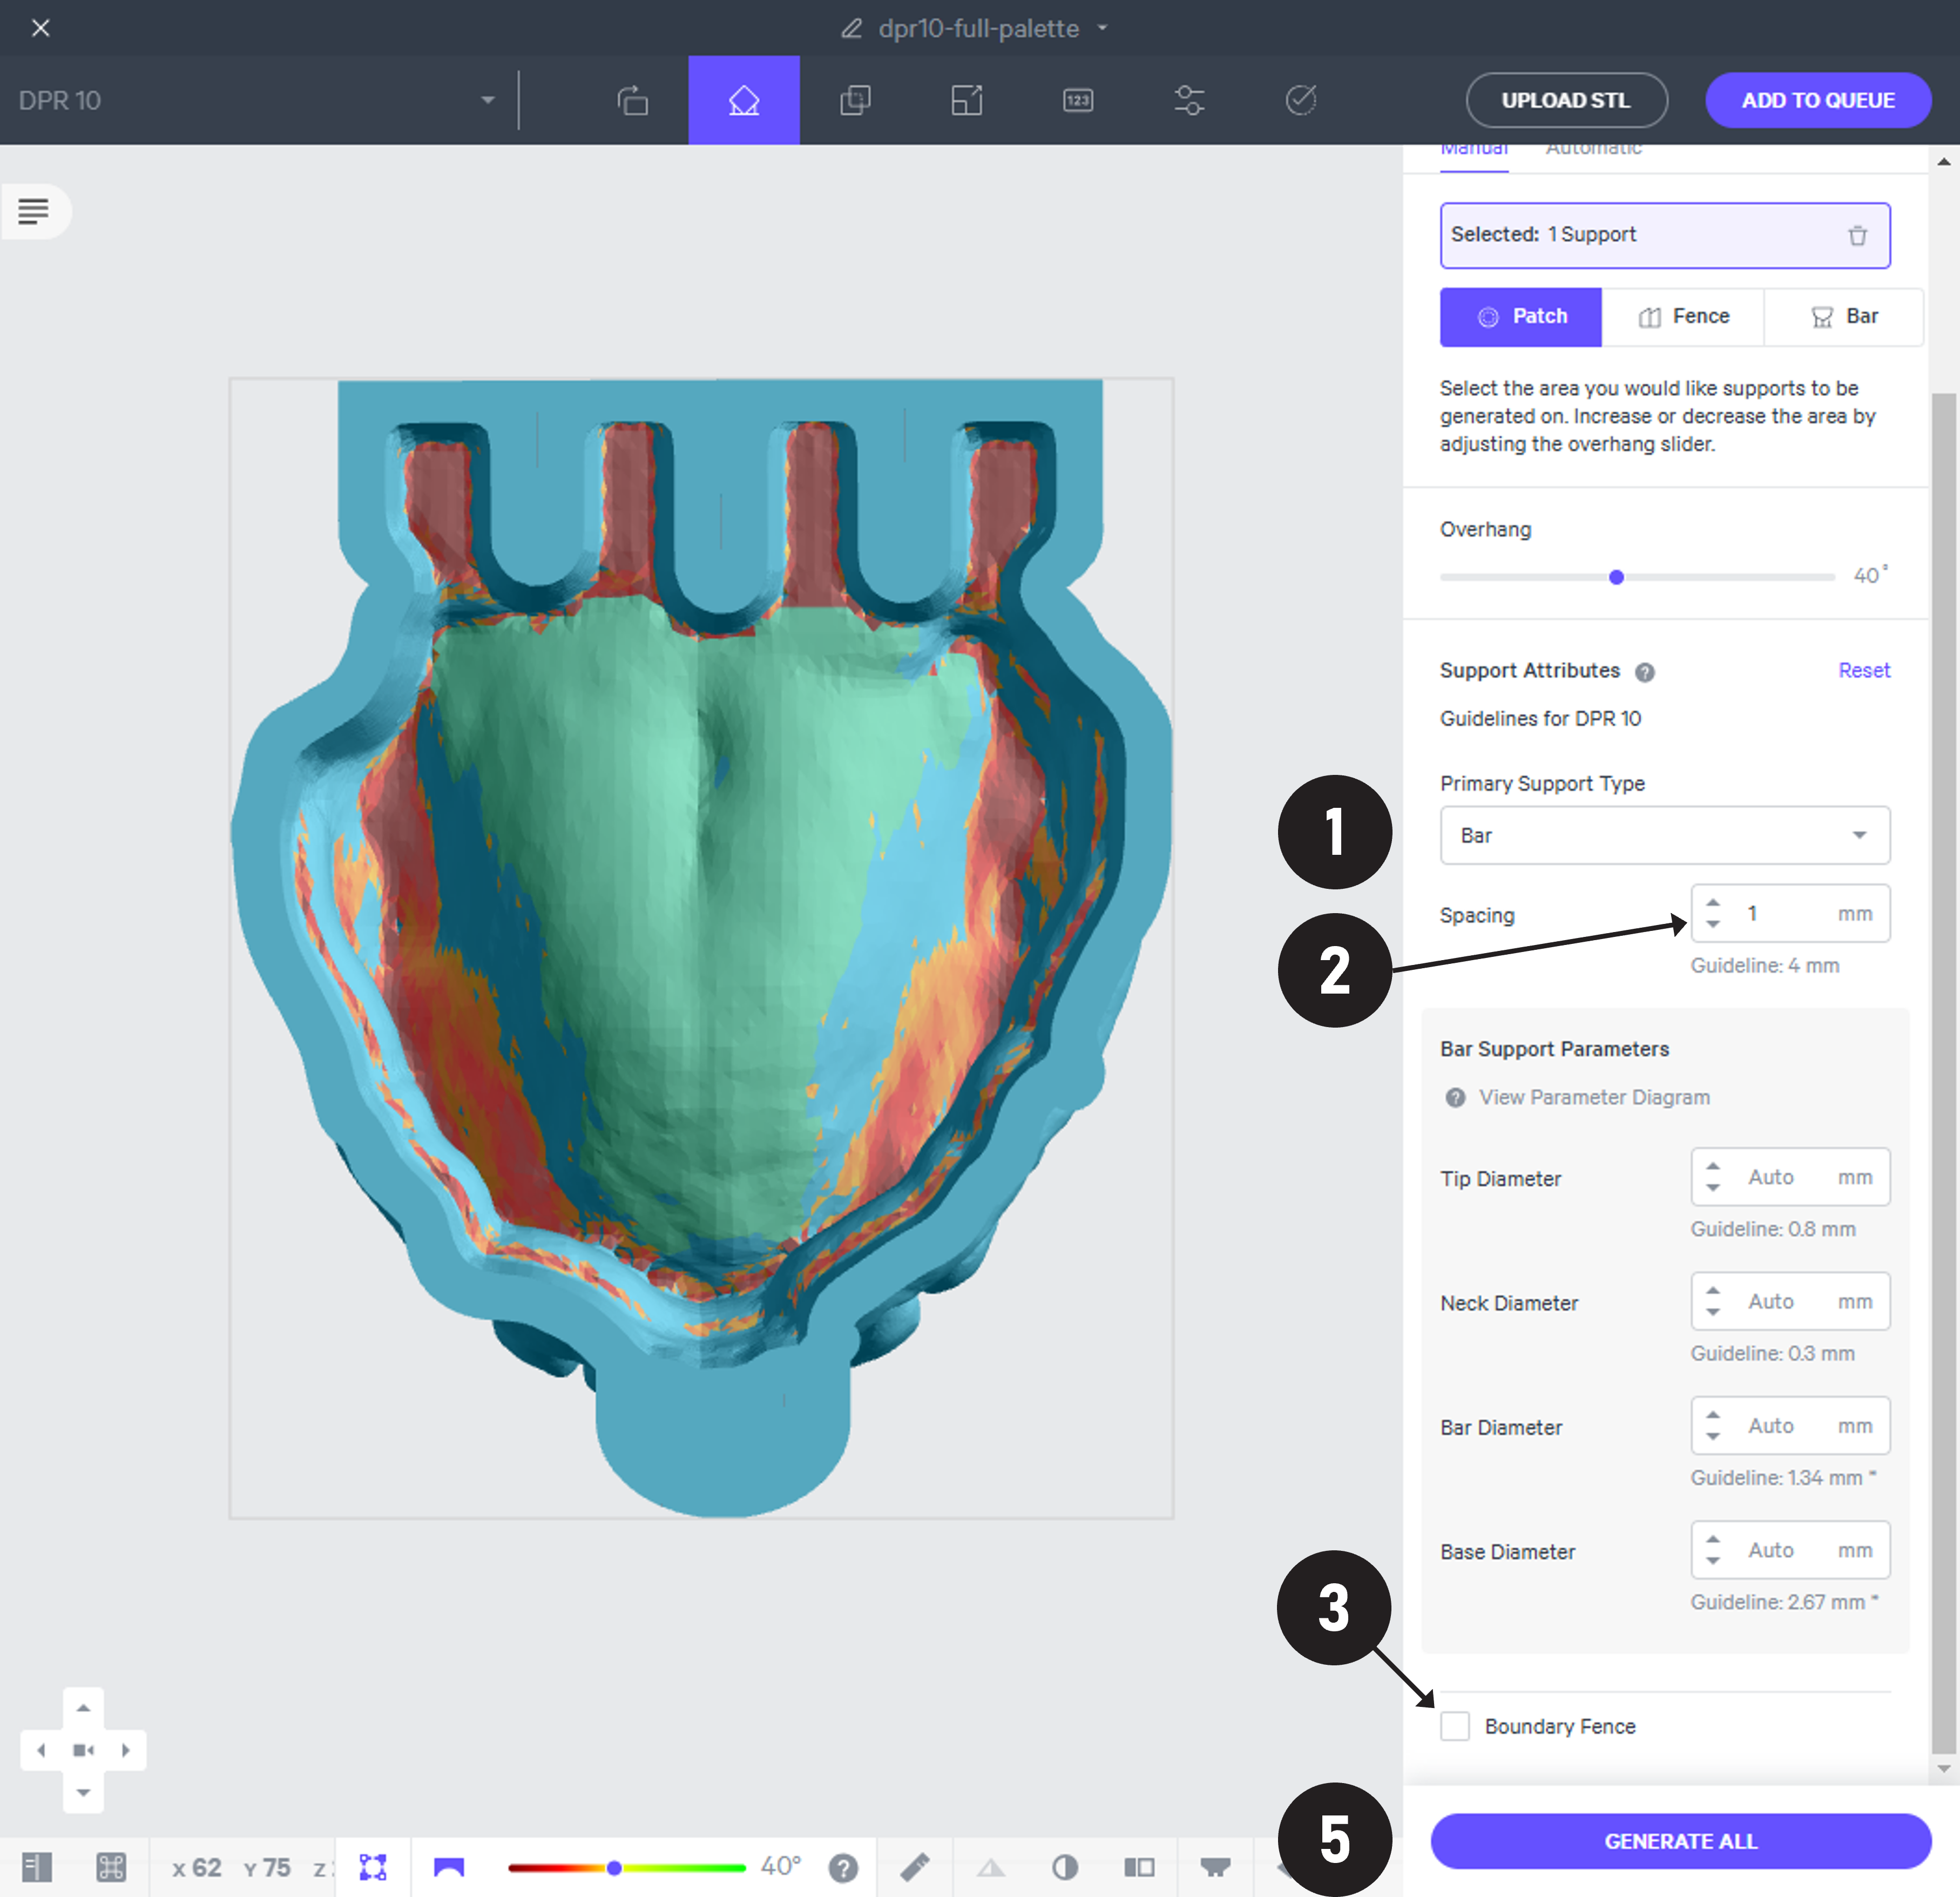
Adjust Patch Settings
- In the Supports menu, under Primary Support Type select Bar.
- Under Spacing, type or use the arrows to set 1 mm.
- Uncheck Boundary Fence.
- If necessary, select more patches.
- Click Generate All in the lower right corner to create supports.
Never use fence supports for models that will be printed in Automatic Mode on the AO Backpack. Automatic Mode models require bar supports with base rafts.
See Supporting Models for Automatic Mode for more information.
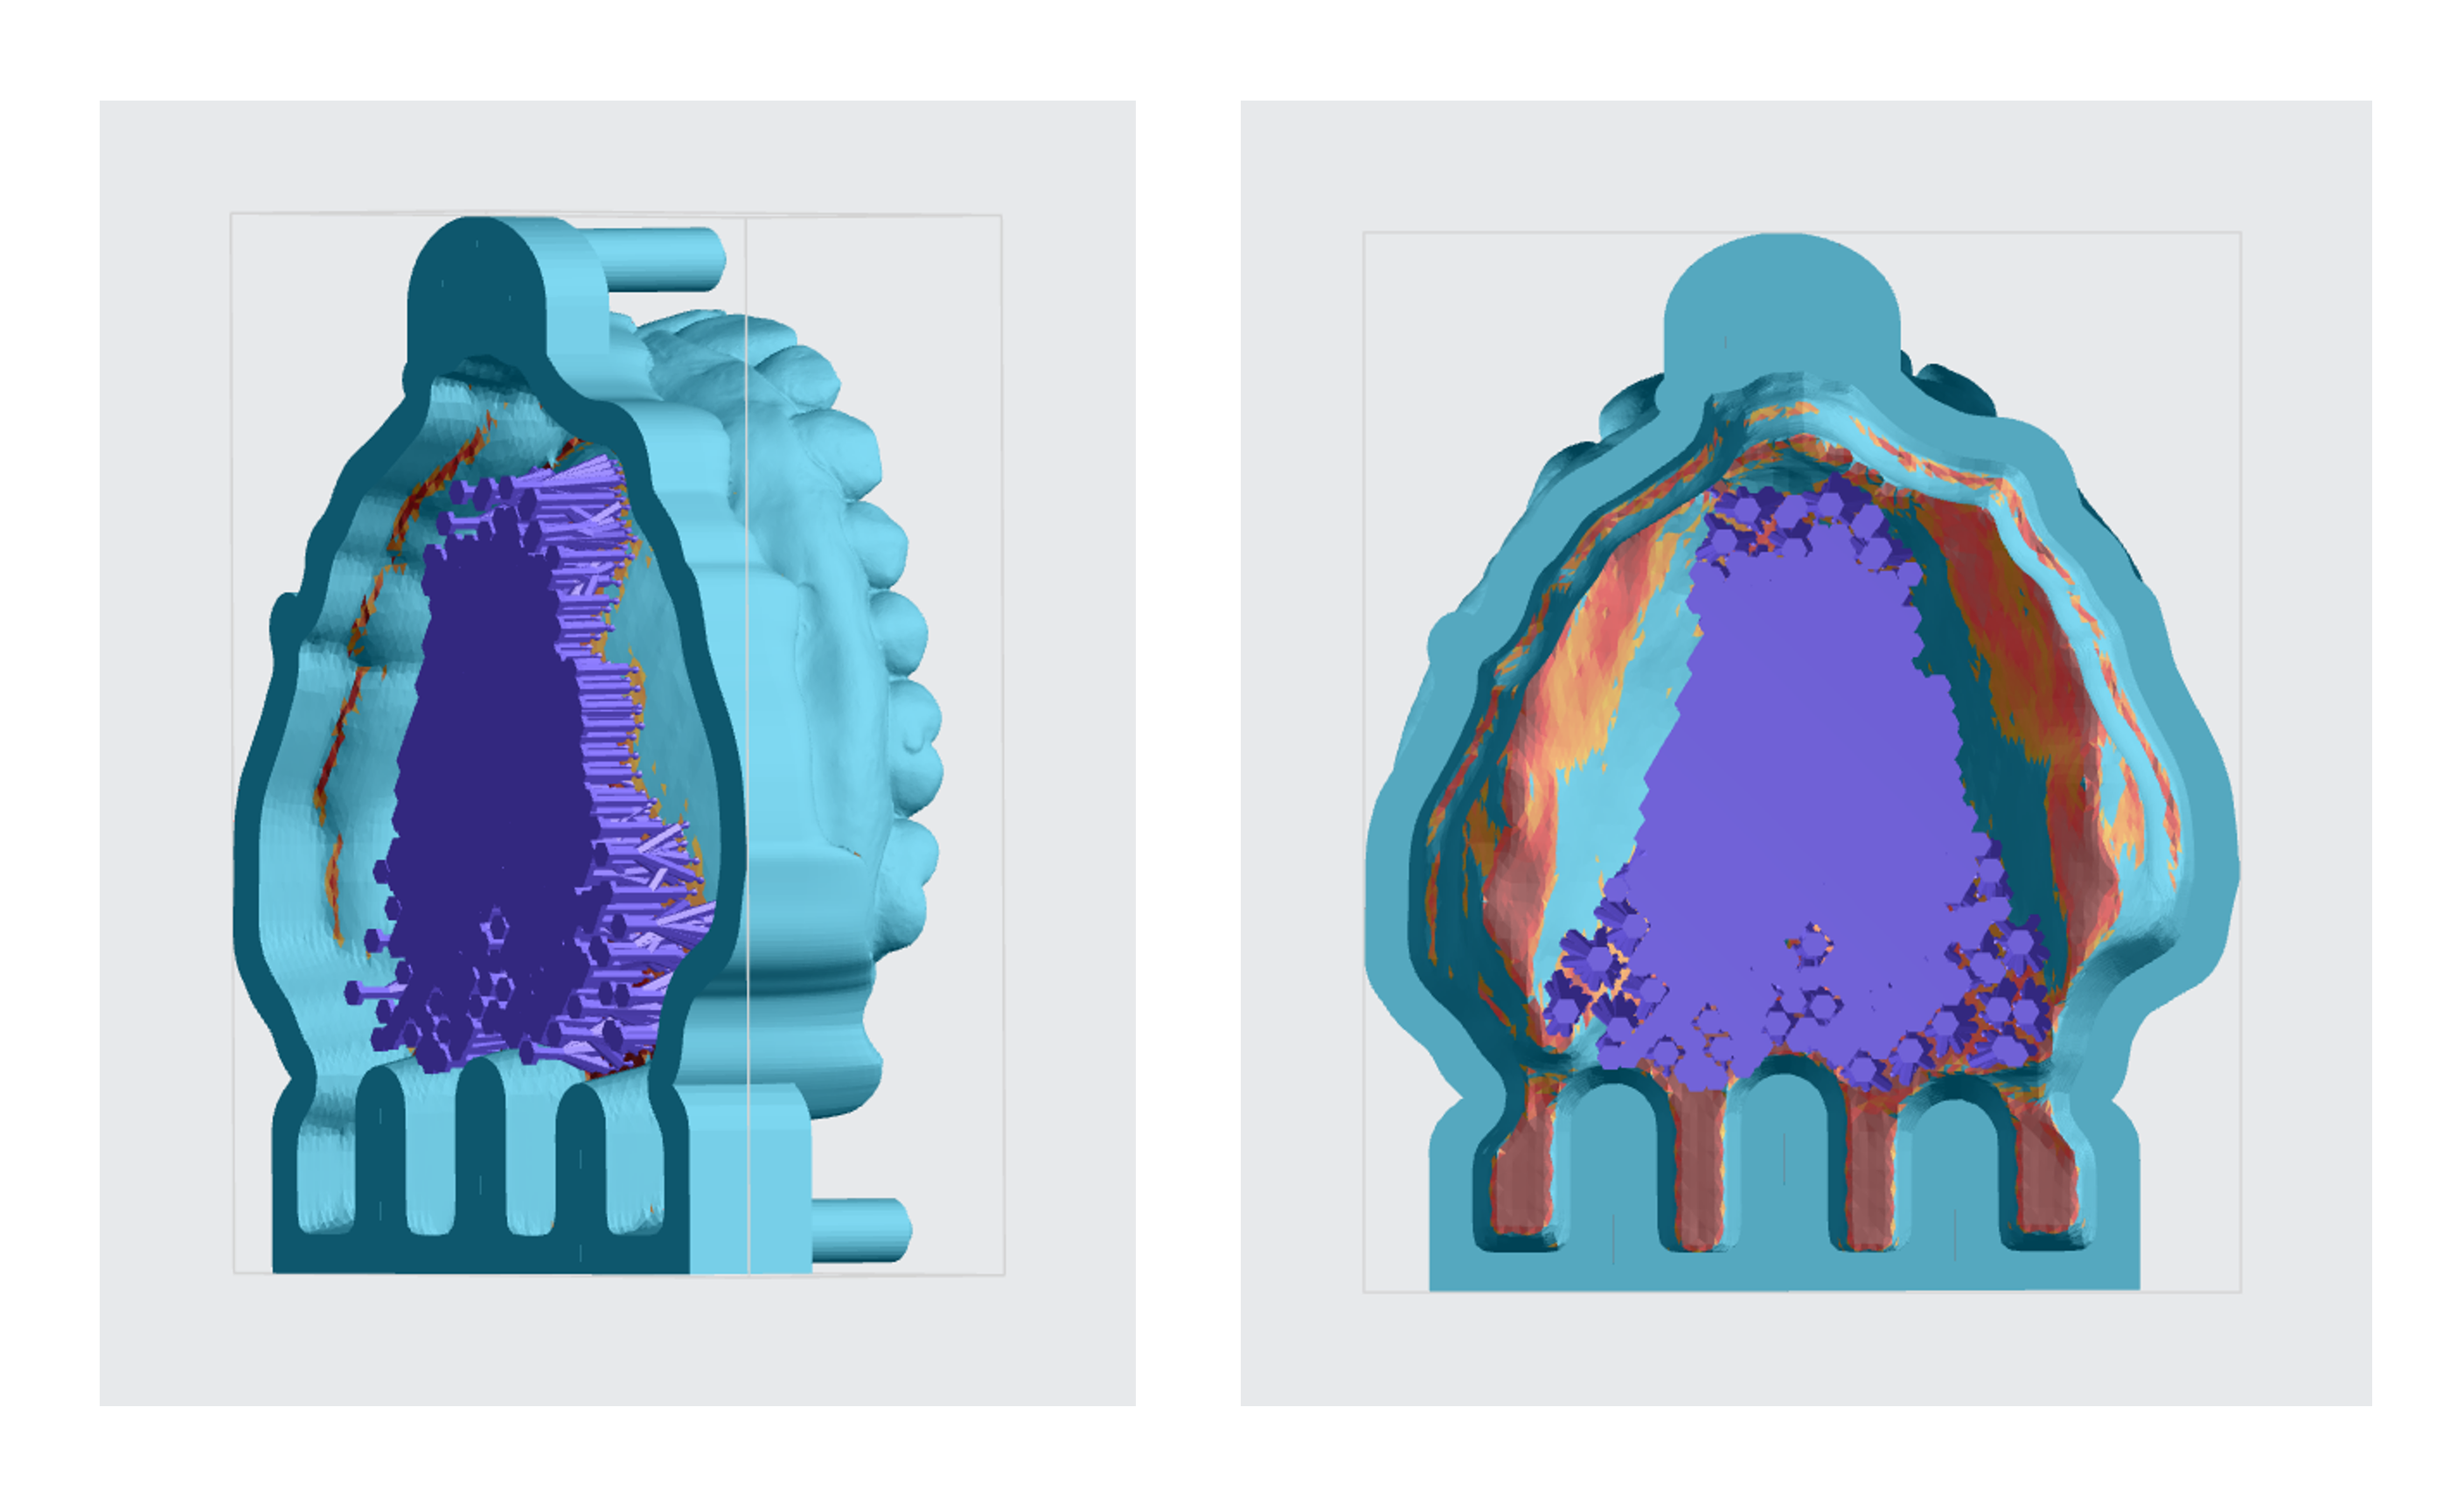
Properly Supported Full Palette Model
Nesting

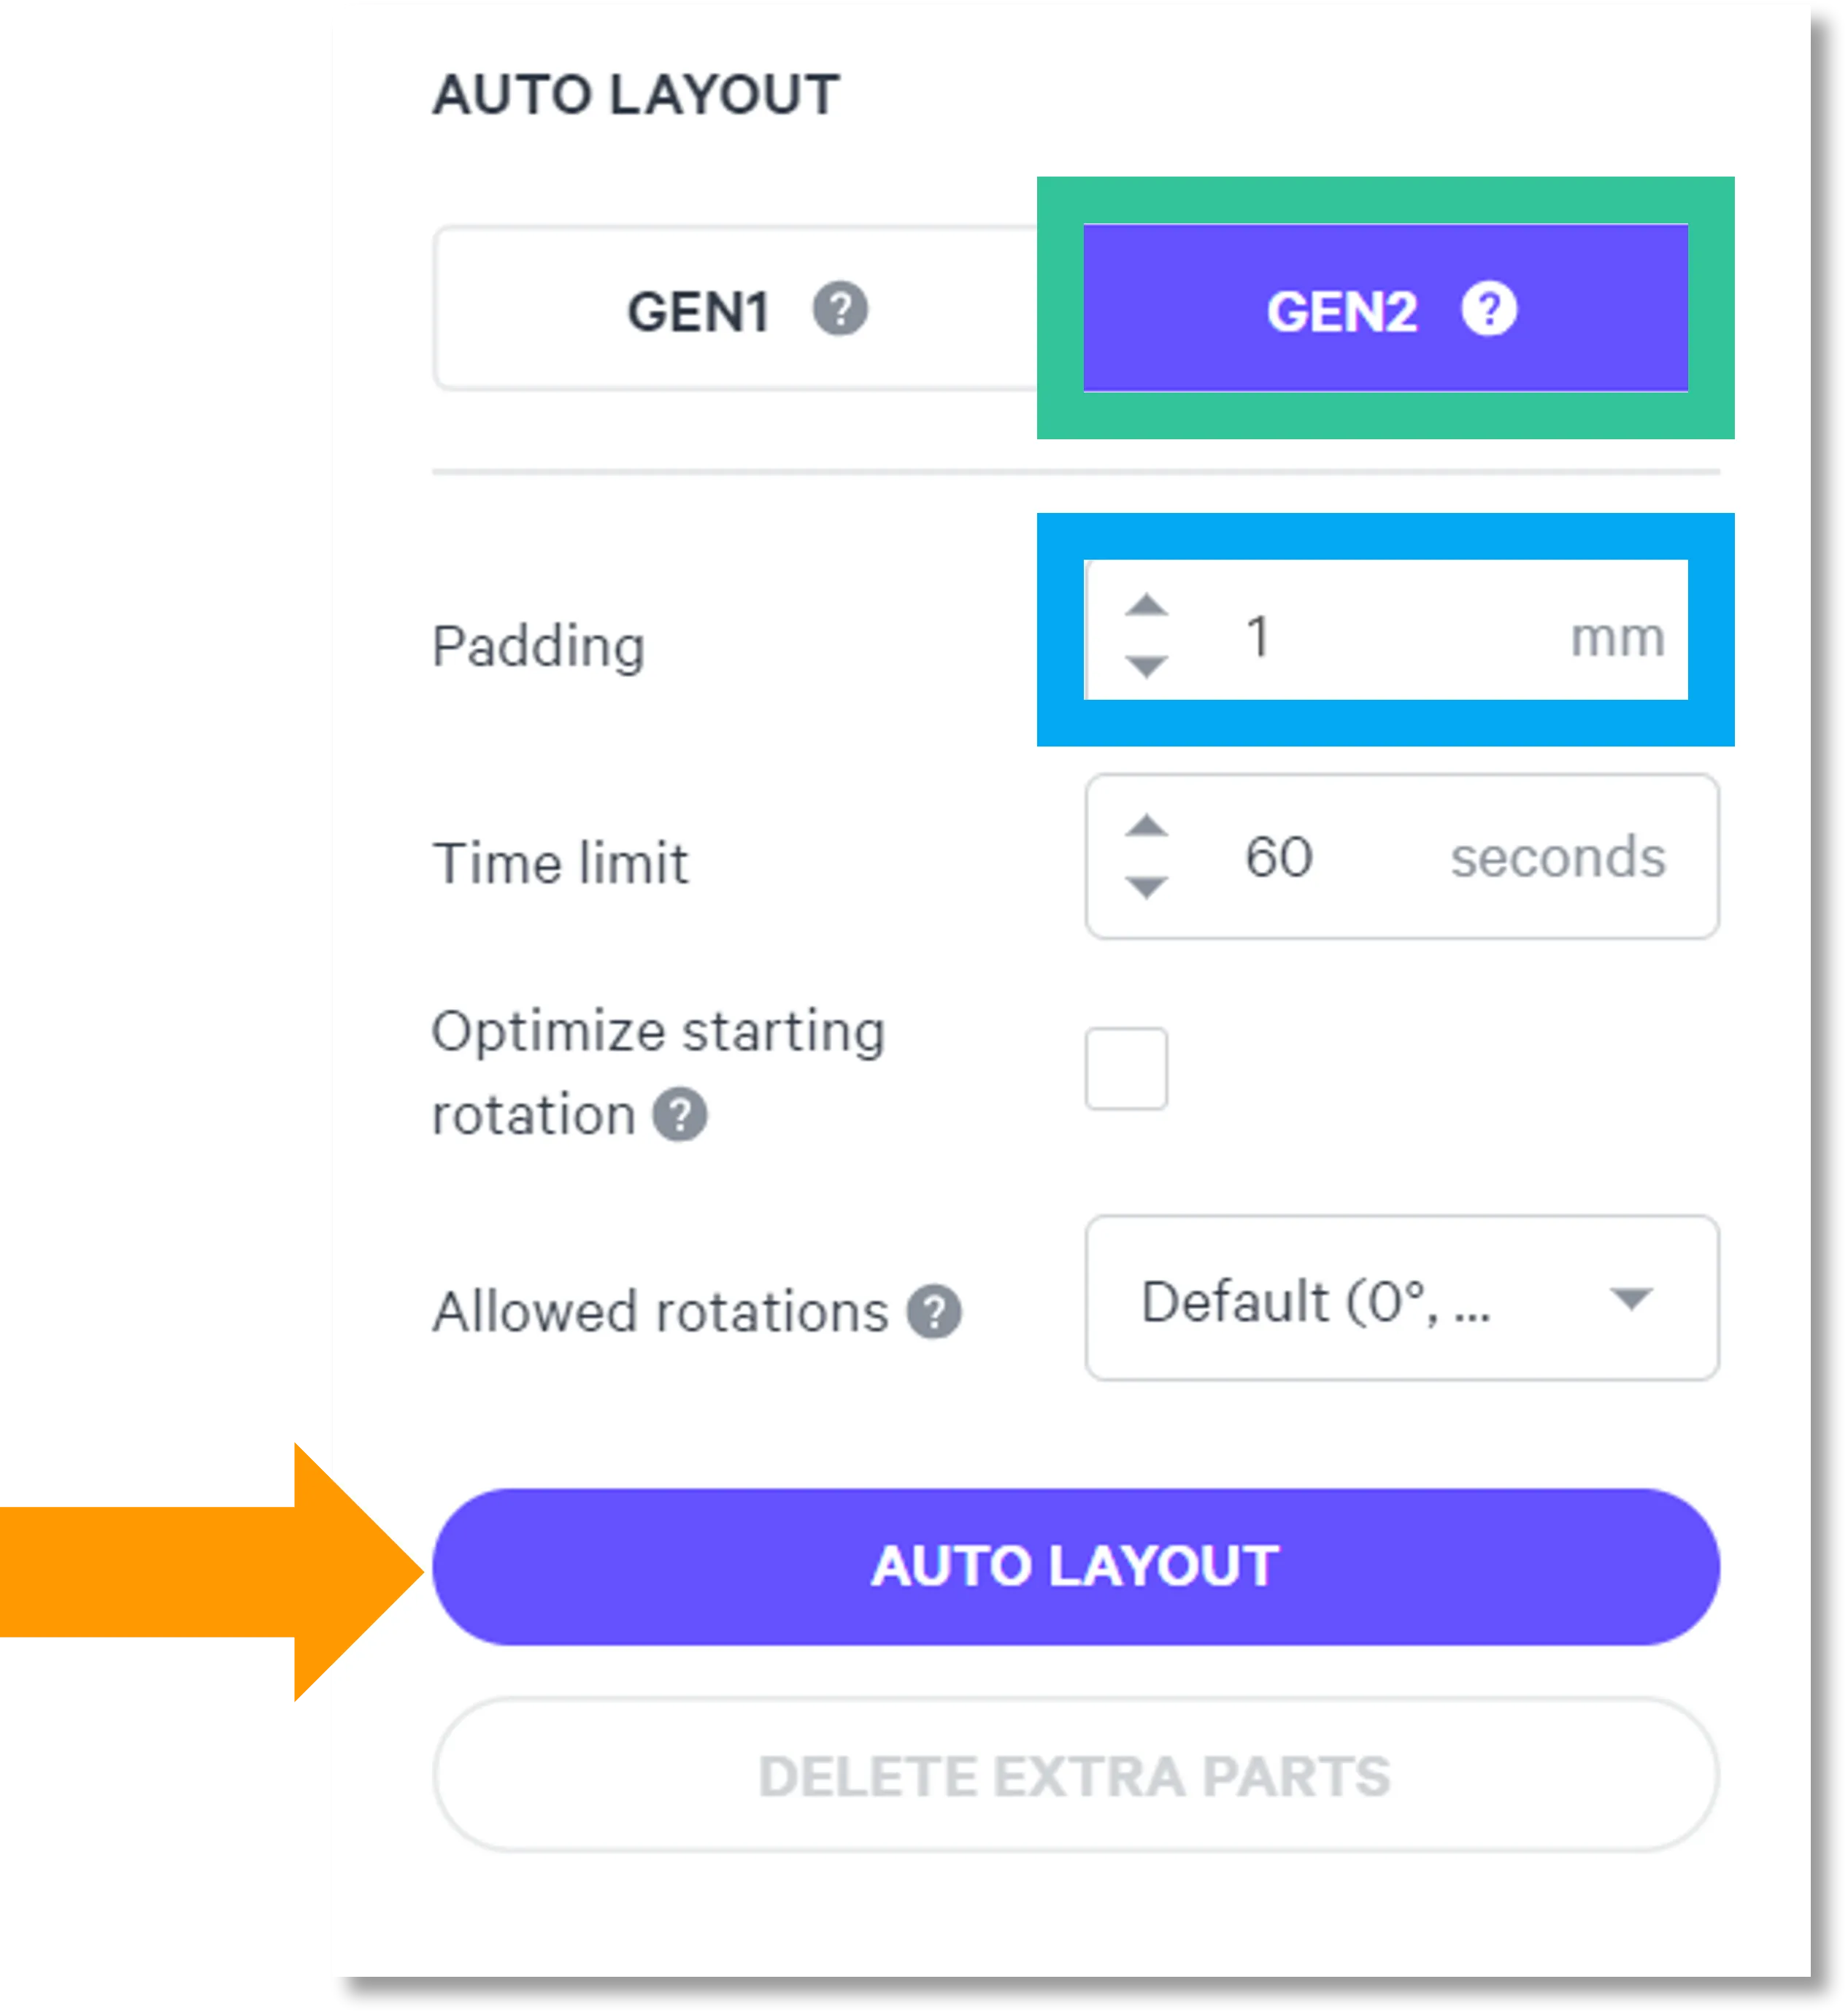
- Select the Layout tab (Shift + L) in the top menu bar.
- Under Auto Layout, select Gen2.
- Gen2 usually gives the most effecient packing for dental devices.
- Enter at least 0.5 mm in Padding.
- Models require a minimum of 0.1 mm of space between them.
- Optimize starting rotation
- ON for models only or mixed builds
- OFF for dies only
- Leave Allowed rotations at the default setting.
- This gives the software maximum flexibility to fit the most possible parts on the build platform.
- Press the Auto Layout button to arrange your parts.
If necessary, nesting can be changed manually:
- Click and drag parts to adjust their position.
- Modify Z rotation by using the Spin tool or manual rotations under the Orient tab (Shift + O).
- Use the Part List tab as needed to more easily select models and focus on them.
Print Preparation
Print Controls
Click Print Controls or Shift + P in the top menu bar.
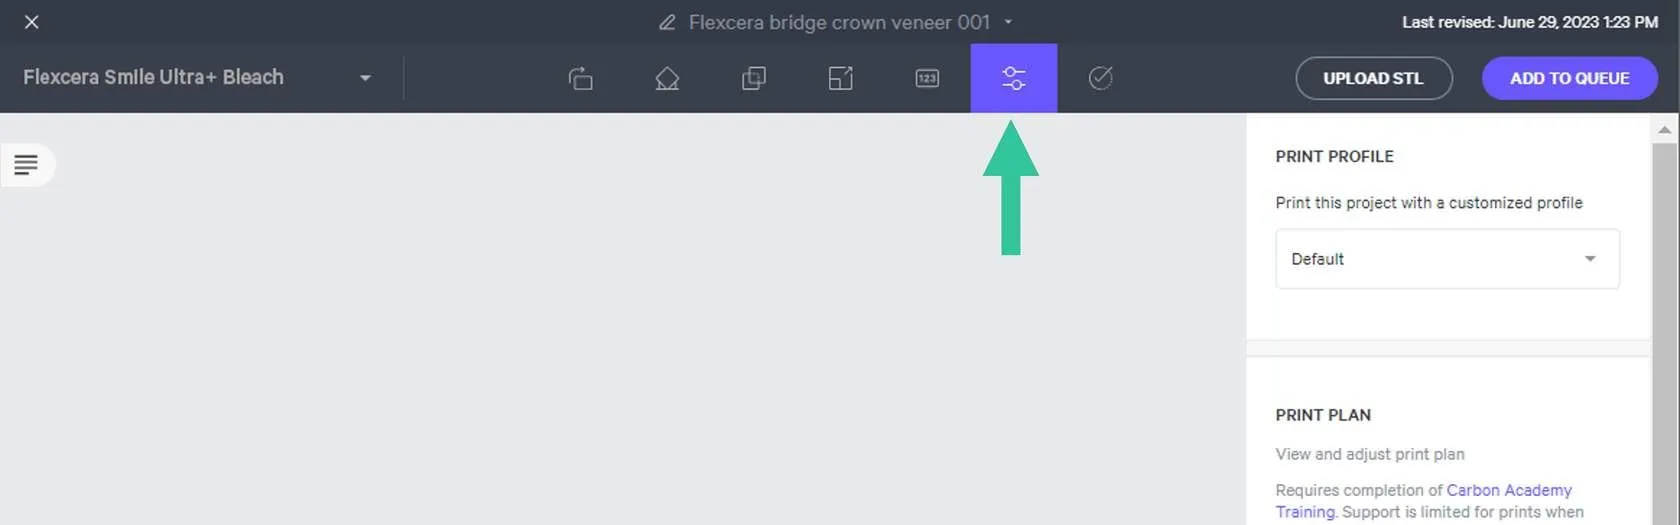
Print Profiles
Two print profiles for use with DPR 10 are available to all customers to provide Dental Labs with more control over print outcomes: DPR 10 Loosen Fit and DPR 10 Tighten Fit.
Reference Print Controls for more information.
Slicing
For standard models, Carbon recommends a Slice Thickness of Standard (100 µ).
For crown and bridge, die fit, and analog implant models, Carbon recommends a Slice Thickness of Fine (50 µ).
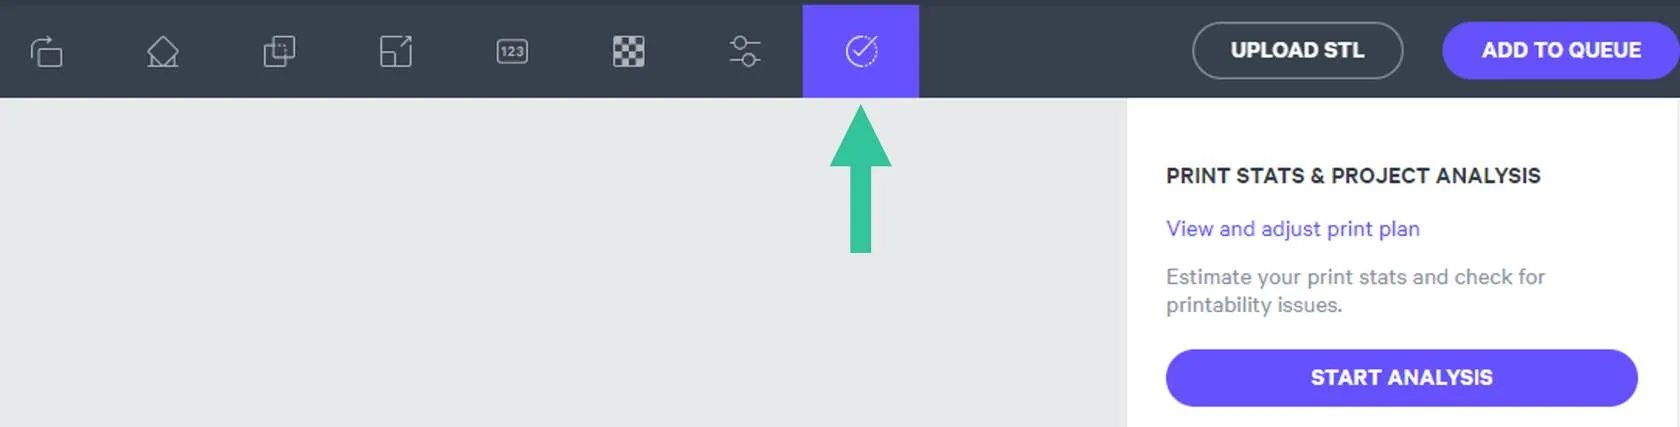
Project Analysis
- Select the Project Analysis tab.
- Click Start Analysis and wait for the processing to complete.
- Note the required resin volume and print time.
- Click Add to Queue.
Printing
Consult the protocol sheet for information about resin storage, dispensing, washing and curing.
Tips
If you have an AO Backpack, see Operation for information about using Automatic Mode for unattended printing.
Washing
Remove Parts from the Platform before Manual Washing
To facilitate part cleaning, be sure to remove parts from the platform before washing.
Tip: Removing arches from the platform
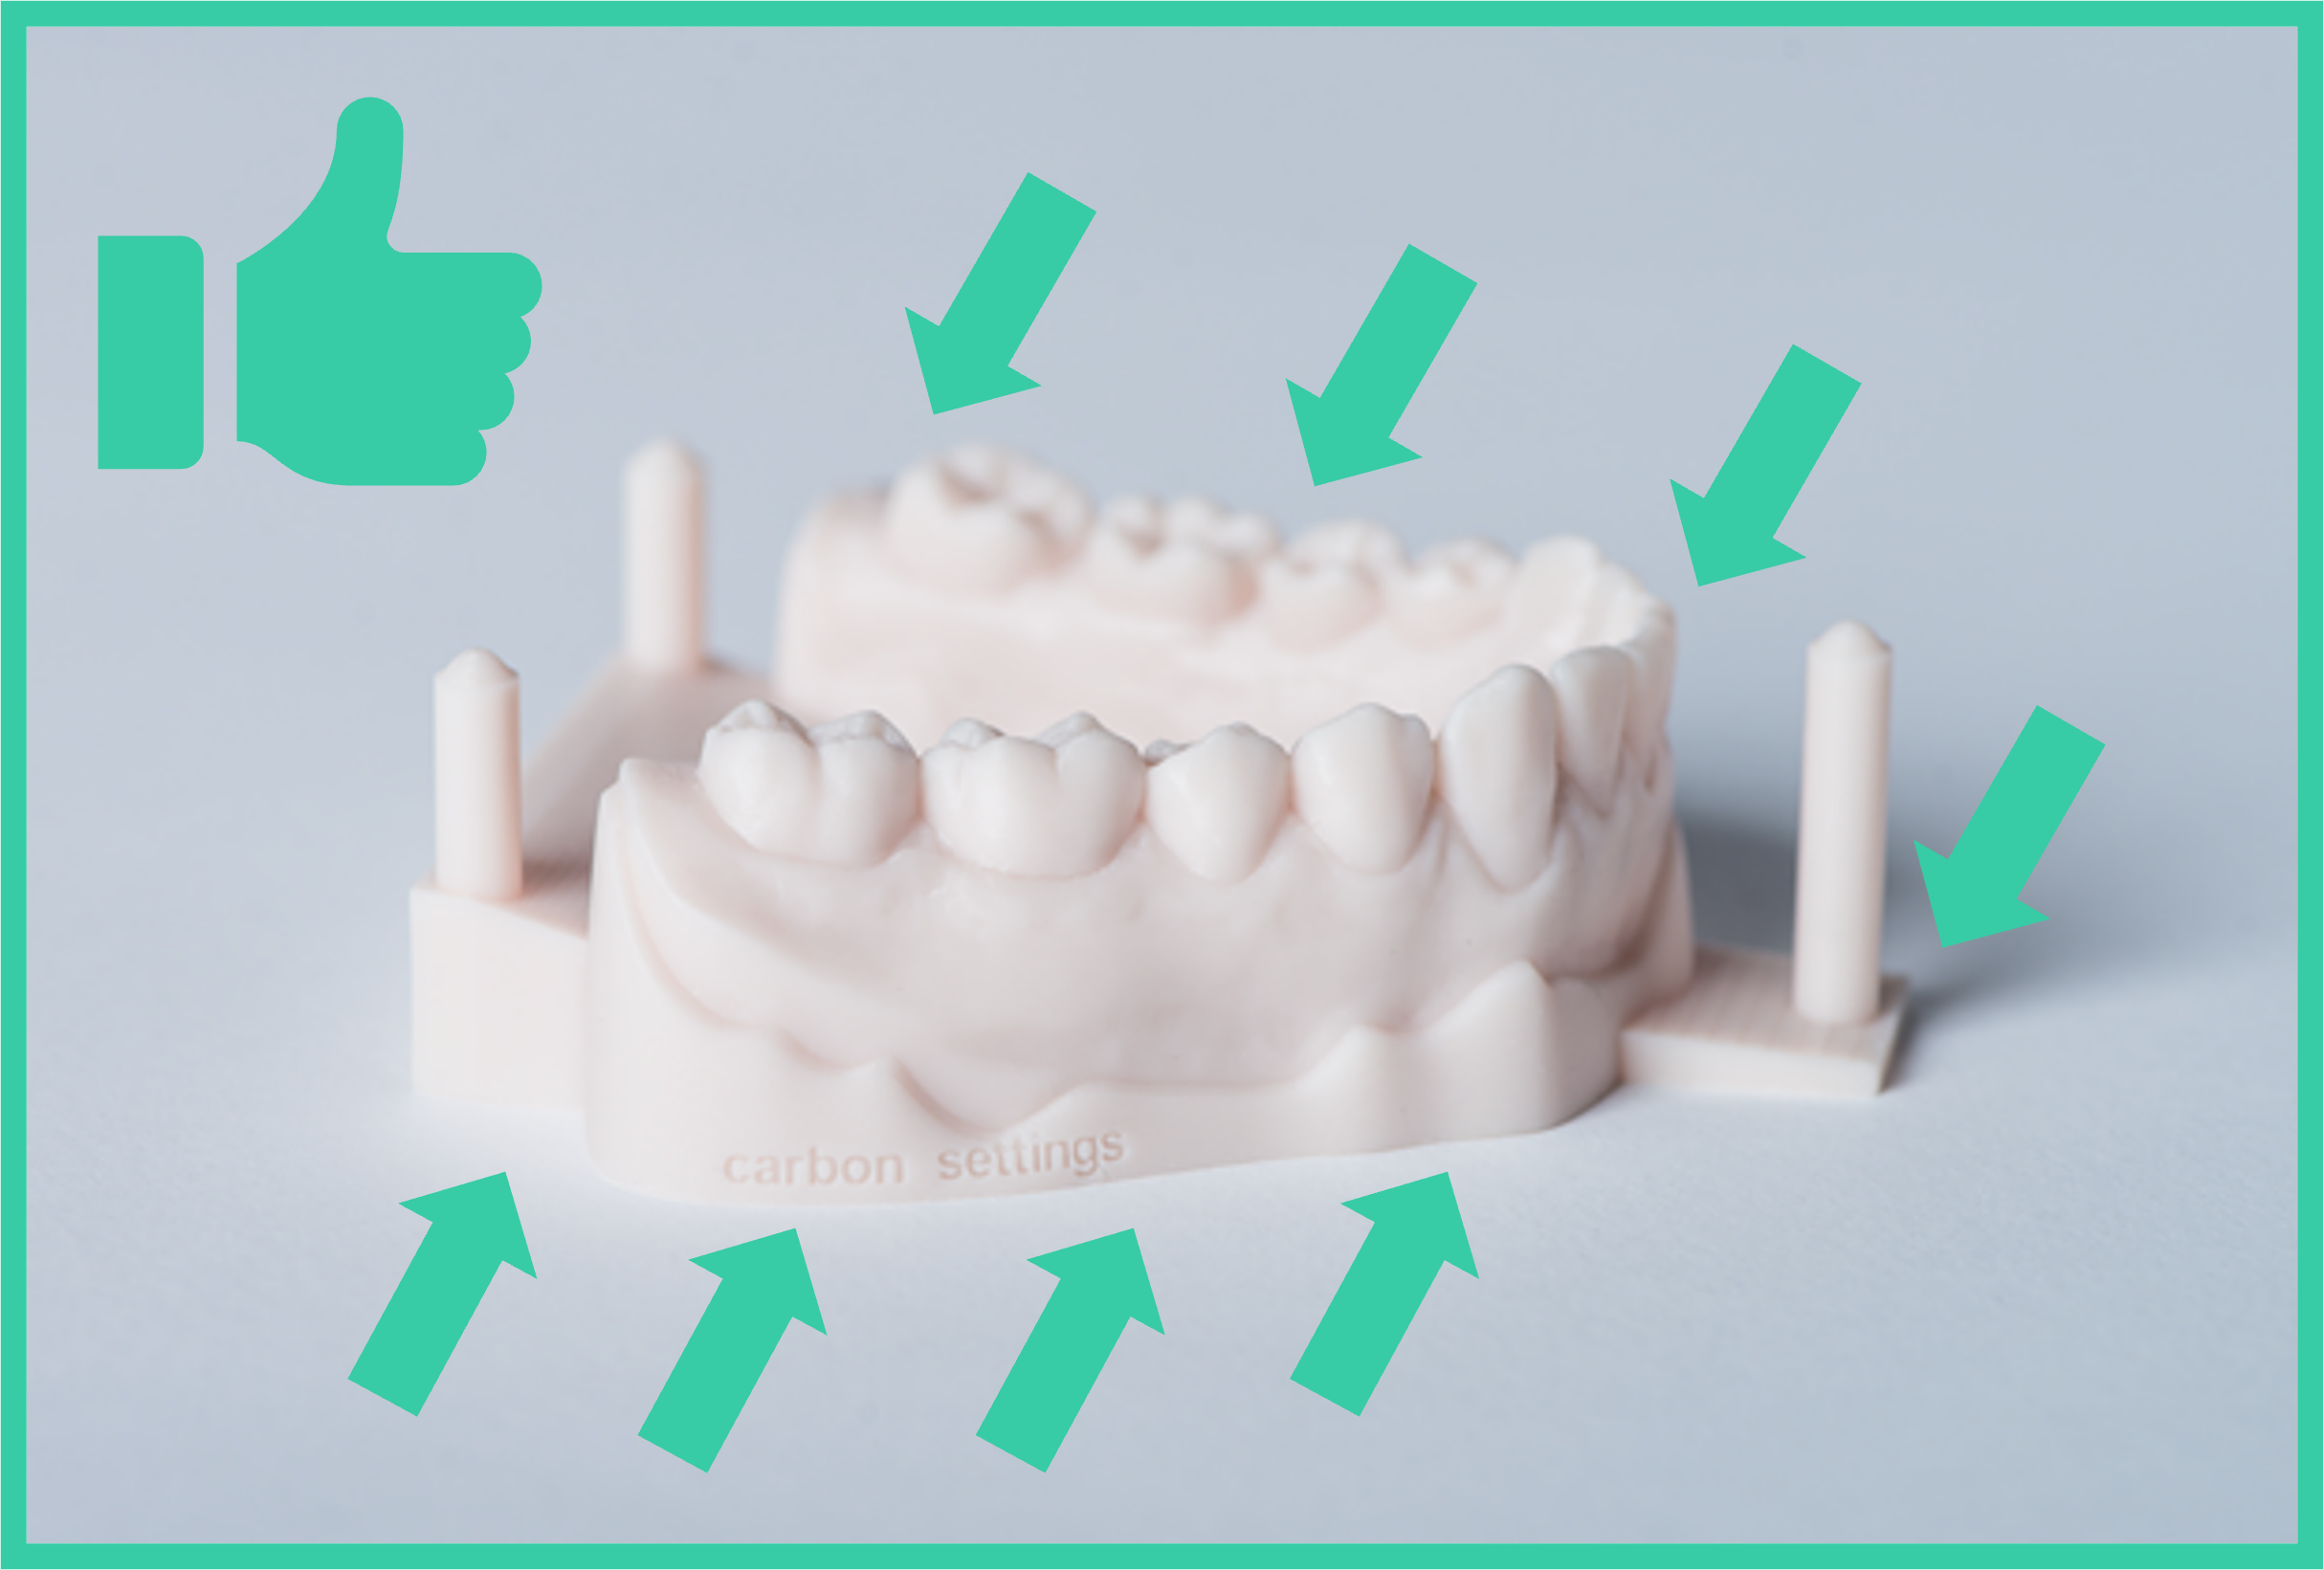
Remove arches by putting the scraper under thick, strong features. The sides of this model are the thickest and strongest part with the smallest chance of breaking.
Apply less force at several locations rather than a large force at one location.
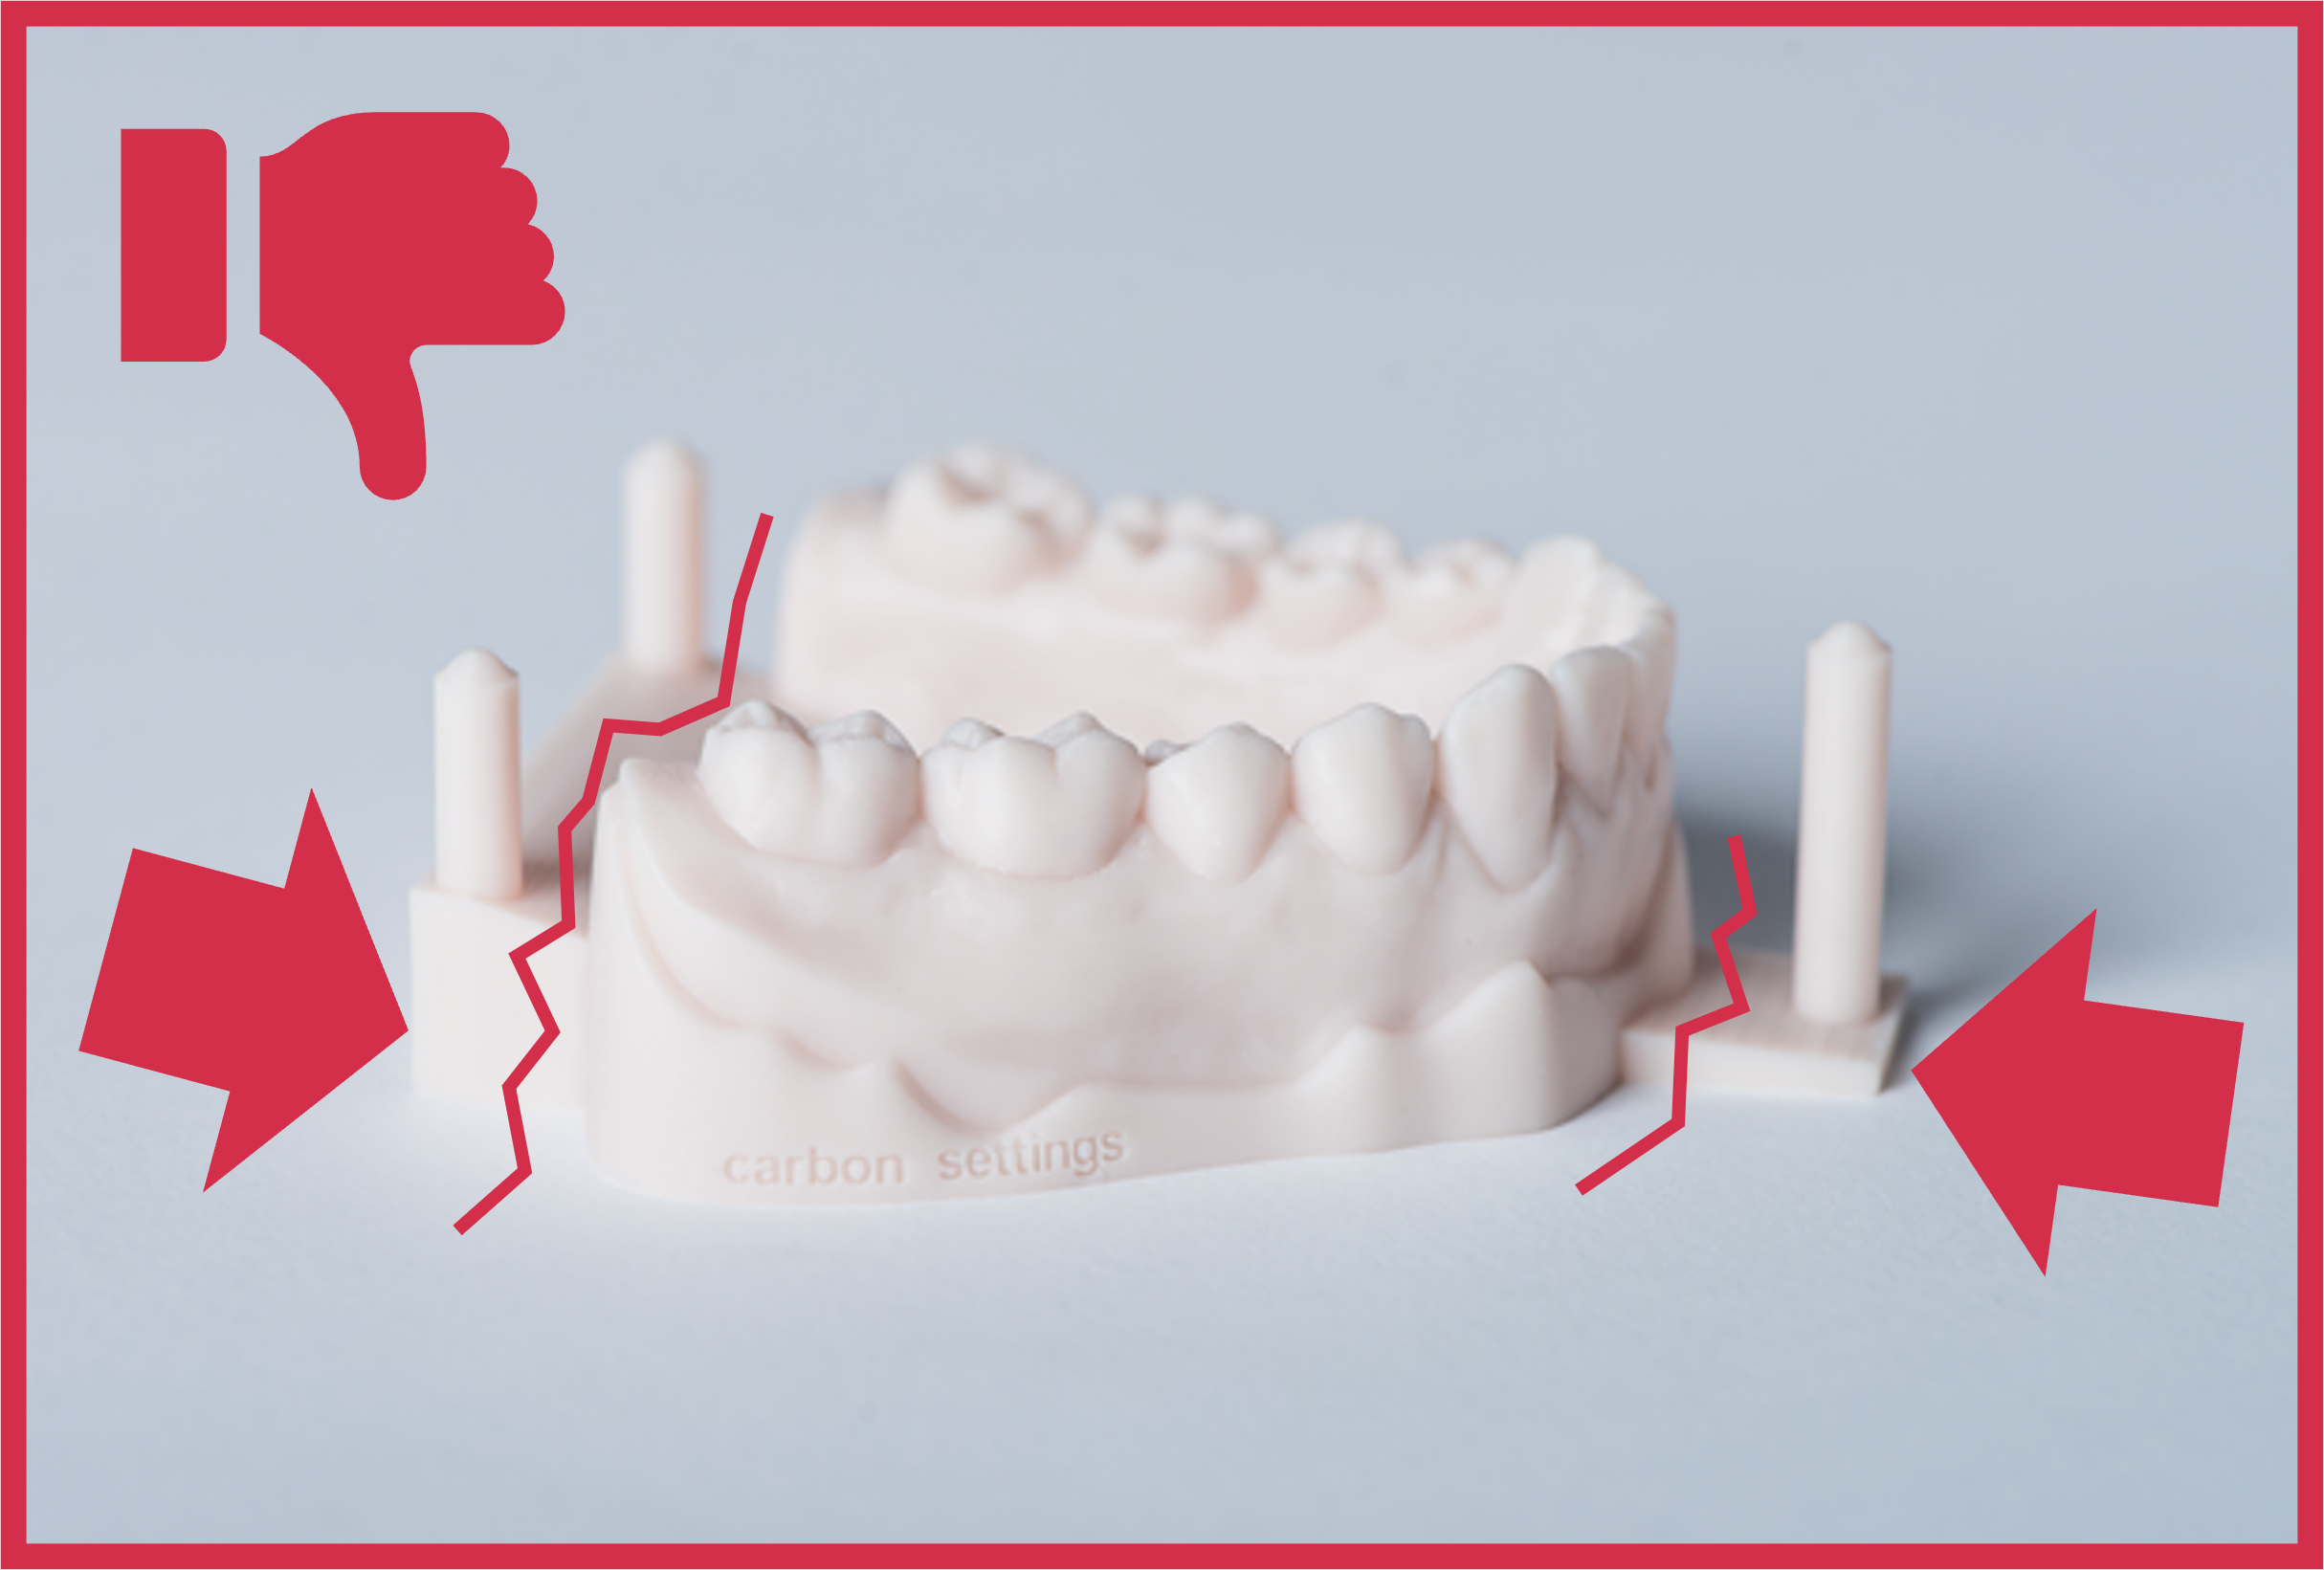
Be patient when removing models by putting the scraper blade under delicate features, as they can break during part removal.
Washing Process
Solvent Swapping for Manual Washing
Cleaning DPR 10 models with an orbital shaker requires two washes:
- First wash: 3 minutes in Container 1 with used IPA
- Second wash: 2 minutes in Container 2 with fresh IPA
"Used IPA" has cleaned one full platform of models.
Carbon recommends the following process for manual washing:
- First build of the day
- Fill both containers with fresh IPA.
- Perform both washes.
- Next build (see graphic below)
- Use Container 2 for first wash.
- Dispose of the used IPA from Container 1, refill with fresh IPA and use for second wash.
- Subsequent builds
- Continue the process from step 2 above.
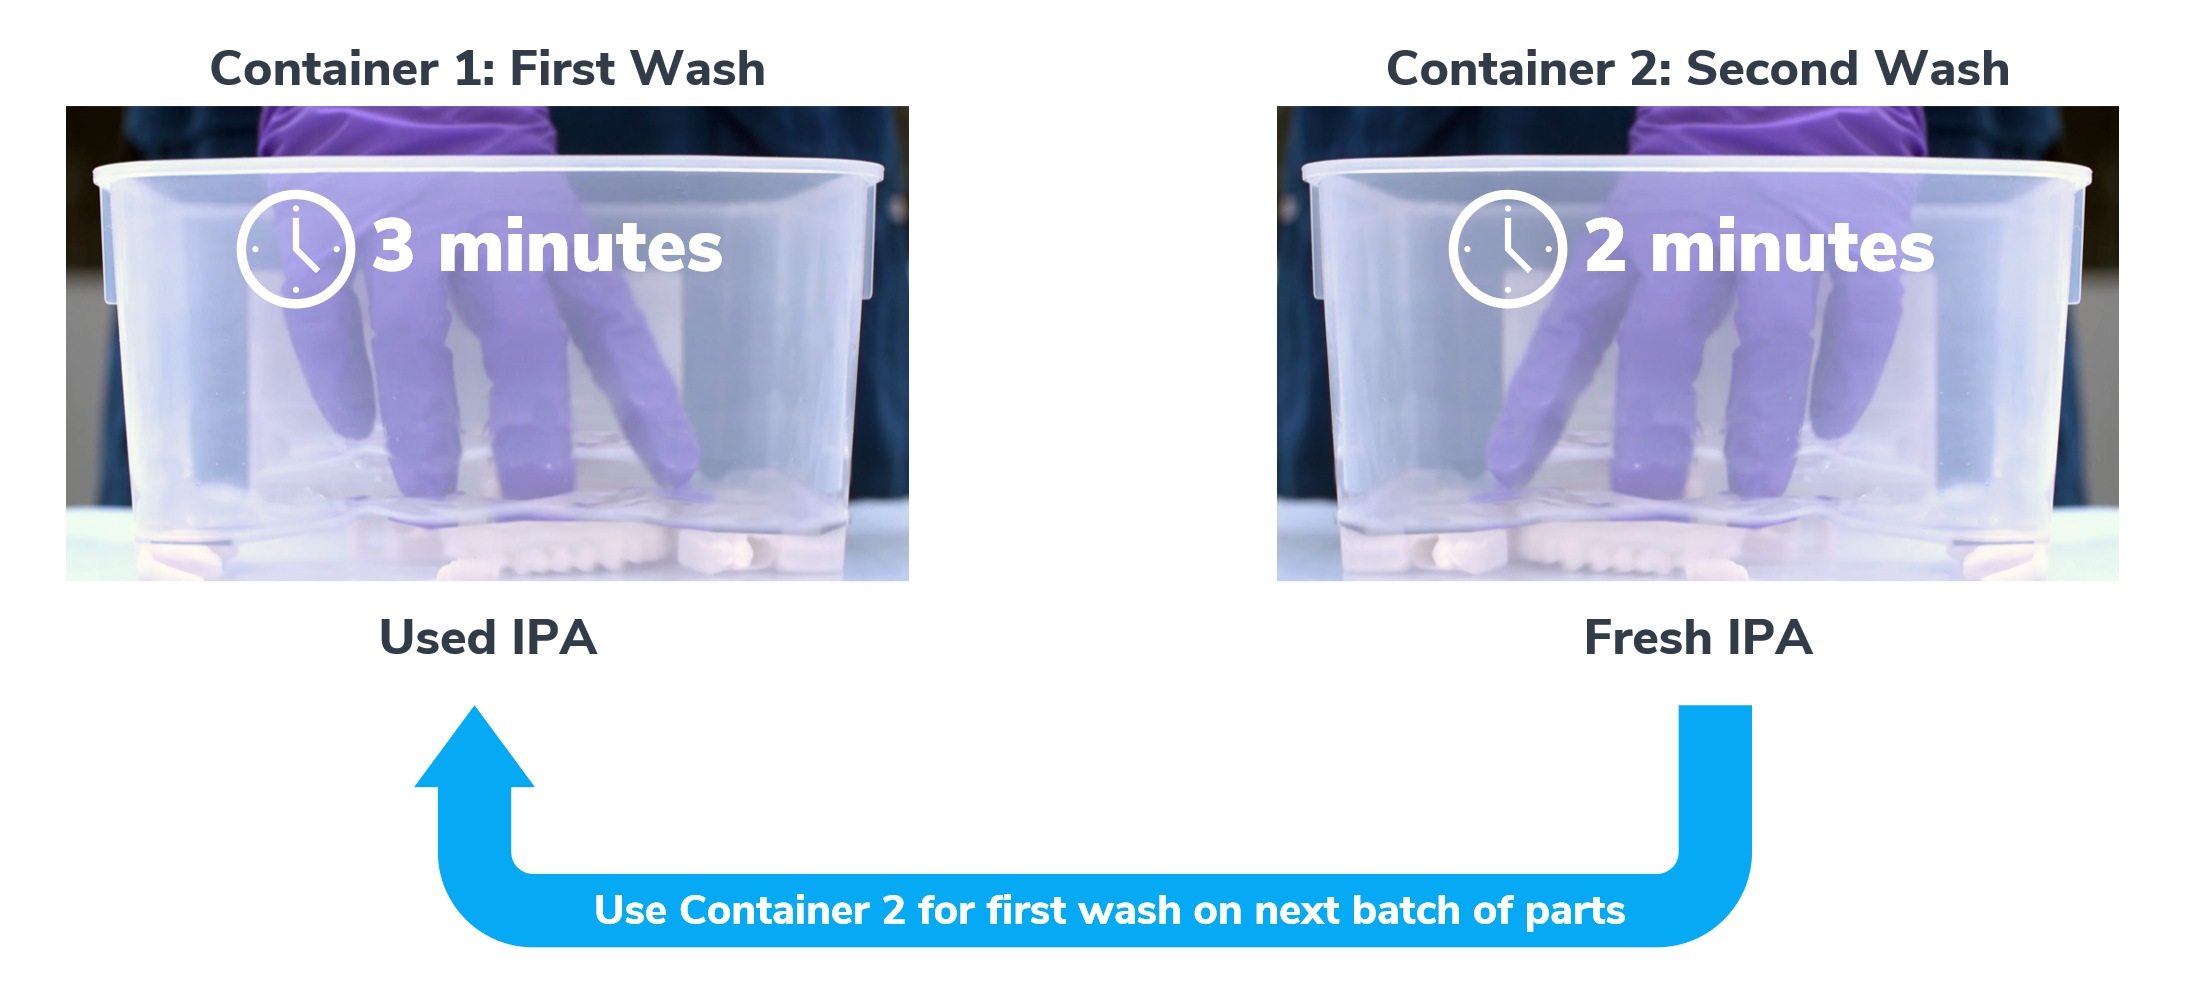
Dispose of used IPA according to local regulations.
Curing
Curing Process for Dreve PCU LED
Reclaiming Resin with the Pour Stand
The following video demonstrates resin reclamation using an M2 cassette with the M2 Pour Stand.
For instructions on using the newest accessory, go to M Series Pour Stand.